What Is a High Visibility Vest Manufacturer Factory?

A High Visibility Vest Manufacturer Factory is more than a sewing workshop. It is a controlled production environment where visibility, comfort, durability, and traceability meet. This introduction explains how such a factory turns reflective fabric, fluorescent materials, and technical specifications into dependable safety garments.

A professional factory usually manages fabric inspection, pattern cutting, heat-transfer application, stitching, reflective-tape placement, and final quality checks. Workers may test color consistency under bright lamps. They may also examine tape alignment across shoulders, chest, and back. Small details matter. A loose seam can weaken user confidence. Poor sizing can reduce visibility when the vest hangs incorrectly.

Dr. David Michaels, former Assistant Secretary of Labor for Occupational Safety and Health, has repeatedly emphasized the importance of prevention in workplace safety. His practical message can be expressed simply: “Prevention should guide every safety decision.” That principle applies directly to a High Visibility Vest Manufacturer Factory. The factory should not treat compliance as the finish line. It should build safety into material selection, production records, worker training, and inspection routines.

Experienced manufacturers also understand that one vest cannot suit every workplace. Road crews, warehouse operators, airport teams, and emergency personnel face different movement and weather conditions. A factory must listen carefully to users. It must test products in realistic situations, not only on a clean sample table. Some processes may still need improvement. That honest weakness matters. Reliable production grows through documented checks, supplier evaluation, customer feedback, and continuous review. The strongest factory is not the one claiming perfection. It is the one proving consistency, correcting mistakes, and protecting visibility in practical daily use.
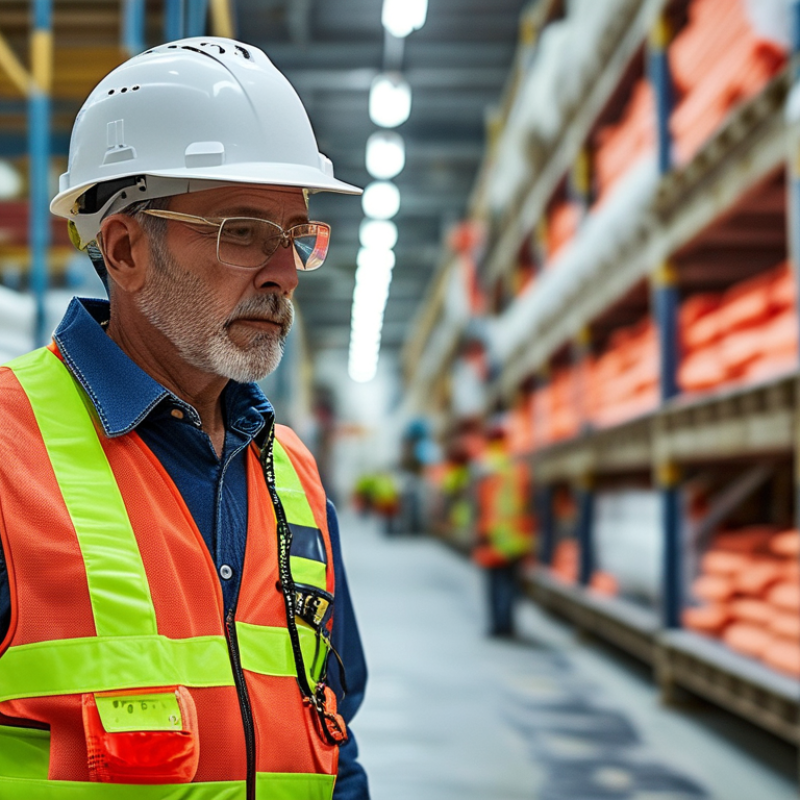
What Is a High Visibility Vest Manufacturer Factory?

Definition and Role of a High Visibility Vest Manufacturer Factory

A high visibility vest manufacturer factory is a production facility that designs, makes, and checks reflective safety vests. Its role extends beyond sewing fabric together. The factory selects fluorescent materials, reflective tape, strong stitching, and suitable closures for demanding work environments. Skilled teams convert safety requirements into wearable products for road crews, warehouse staff, construction workers, and emergency personnel. They also create samples, adjust sizing, and manage bulk production. A reliable factory keeps material records and provides clear testing information. That evidence helps buyers judge product performance with confidence.

Manufacturing quality depends on practical experience. Workers inspect tape alignment, seam strength, color consistency, and fastening performance. Factories may test visibility under different lighting conditions and inspect finished vests before packing. Small defects can matter. A loose thread or poorly placed strip may reduce comfort or visibility. No factory is perfect, though. Good manufacturers review mistakes, listen to user feedback, and improve their process instead of hiding weak results. This attitude supports long-term reliability.

Tips: Ask about fabric weight, reflective tape performance, size grading, and inspection procedures. Request samples before placing a large order. Check whether test reports match the actual materials used. Consider comfort, ventilation, and pocket placement, not only bright color. A vest that looks excellent but feels awkward may be ignored during a long shift. Also, confirm production capacity and delivery control. Delays can disrupt site planning.

What Is a High Visibility Vest Manufacturer Factory? - Definition and Role of a High Visibility Vest Manufacturer Factory
Data Dimension Definition, Capability, or Typical Data Practical Role in High Visibility Vest Manufacturing
Factory Definition A high visibility vest manufacturer factory is a production facility that develops, cuts, sews, assembles, inspects, and packs garments designed to make workers more noticeable in daylight and low-light conditions. Converts fabric, reflective materials, trims, and design specifications into finished safety garments.
Primary Product Types Safety vests Mesh vests Two-tone vests Reflective jackets Traffic-control garments Provides garment options for roadwork, construction, logistics, utilities, emergency response, and industrial operations.
High-Visibility Materials Common fluorescent background colors include yellow, orange, and red. These colors are selected to create strong contrast against surrounding environments during daytime work. Improves daytime conspicuity when workers operate near vehicles, equipment, or changing backgrounds.
Retroreflective Components Retroreflective tape or segmented reflective trim is placed on the torso, shoulders, chest, back, or waist. It returns light toward its source, such as vehicle headlights. Supports worker visibility in darkness, poor weather, tunnels, warehouses, and other low-light environments.
Applicable Standards Depending on the target market and garment classification, factories may work with requirements such as ANSI/ISEA 107 in the United States or EN ISO 20471 in Europe. The applicable standard should be confirmed for the intended use and market. Guides garment design, visibility areas, material performance, labeling, and conformity documentation.
Design and Development Typical development activities include pattern making, size grading, color selection, reflective tape placement, pocket configuration, closure selection, logo-area planning, and sample preparation. Balances visibility requirements with comfort, mobility, storage, weather conditions, and job-specific needs.
Production Process A standard workflow may include material inspection, fabric cutting, reflective-trim preparation, sewing, attachment of closures and pockets, thread trimming, final pressing, inspection, and packing. Creates a repeatable manufacturing system that supports consistent fit, appearance, and construction quality.
Quality Control Points Key checks can include fabric color, reflective tape position, seam strength, stitch density, zipper or hook-and-loop function, size measurements, loose threads, stains, and packaging accuracy. Reduces defects and verifies that finished garments match approved samples and purchase specifications.
Performance Testing Depending on the required standard, testing may address background-material color, retroreflective performance, dimensional stability, colorfastness, and physical durability. Testing should be conducted through appropriate qualified facilities. Provides evidence that the materials and finished garment are suitable for the stated performance requirements.
Customization Options Factories may offer custom colors, reflective configurations, pocket layouts, closure systems, size ranges, fabric weights, warning messages, and private-label packaging without displaying brand information in general product data. Adapts the vest to workplace procedures, procurement specifications, climate, and user preferences.
Material Choices Common vest fabrics include polyester woven fabric, polyester mesh, and blended textiles. The appropriate choice depends on breathability, durability, climate, intended use, and required compliance criteria. Determines comfort, ventilation, abrasion resistance, weight, appearance, and service life.
Factory Equipment Typical equipment includes fabric-cutting machines, industrial sewing machines, overlock machines, reflective-tape applicators or sewing stations, inspection tables, pressing equipment, and packing tools. Supports accurate cutting, secure assembly, efficient production, and repeatable quality inspection.
Production Capacity Factors Output depends on order quantity, product complexity, number of sewing lines, material availability, sampling requirements, inspection procedures, and packaging specifications. Helps buyers evaluate whether a factory can meet required quantities and delivery schedules.
Workplace Applications High visibility vests are commonly used in construction, road maintenance, transportation, warehousing, airports, rail operations, utilities, waste management, event operations, and emergency services. Improves the chance that workers can be detected by drivers, machine operators, colleagues, and supervisors.
Buyer Evaluation Criteria Important evaluation factors include material traceability, sample approval, measurement consistency, quality-control procedures, testing documentation, production lead time, packaging accuracy, and communication capability. Helps purchasers compare manufacturers using objective production and compliance information rather than appearance alone.
Factory’s Overall Role The factory connects safety requirements, garment engineering, material sourcing, production management, inspection, and delivery into one controlled manufacturing process. Ensures that high visibility vests are designed and produced for their intended working environment and applicable market requirements.

How High Visibility Vests Are Designed and Produced

A high visibility vest manufacturer factory turns safety requirements into a wearable, tested product. Design usually begins with the work environment. Road crews need visibility from several angles, while warehouse workers need freedom of movement. Designers select fluorescent yellow, orange, or red backgrounds, then add retroreflective tape for headlights and low-light conditions.

Standards guide the pattern. ANSI/ISEA 107 classifies garments by risk, visible material, and design features. ISO 20471 also evaluates background and retroreflective performance. These details affect pocket placement, seam strength, and tape width. A good factory creates prototypes before cutting bulk fabric. Workers inspect fit by lifting their arms, bending, and wearing winter layers. Small problems appear quickly.

Production starts with fabric inspection and controlled cutting. Sewing teams attach reflective bands with consistent spacing and reinforced stitches. Heat, washing, and abrasion can reduce performance, so factories use light meters, tensile tests, and repeated laundering checks. The U.S. Bureau of Labor Statistics reported 1,942 fatal occupational injuries from transportation incidents in 2023, representing 36.8% of all workplace fatalities. Visibility cannot prevent every collision, but it supports safer recognition. A vest may look bright under factory lighting and perform poorly outdoors. That gap deserves attention. Quality teams should test real scenes, not only perfect samples. Worker feedback remains essential, although it is sometimes collected too late.

Materials, Safety Standards, and Quality Control

What Is a High Visibility Vest Manufacturer Factory?

A high visibility vest manufacturer factory turns safety requirements into wearable protection. Material selection begins with fluorescent polyester, mesh, or breathable knitted fabric. Fluorescent yellow, orange, and red shades improve daytime recognition. Reflective tape helps workers remain visible under headlights or low light. The tape should stay flexible after repeated washing. Cheap tape may crack, peel, or lose brightness too soon.

A responsible factory checks applicable safety standards for each target market. EN ISO 20471 and ANSI/ISEA 107 define visibility classes, design areas, and performance expectations. These requirements can differ by garment type and working environment. Technicians test color, retroreflection, seam strength, and dimensional stability. They also inspect tape placement around the torso and shoulders. Small errors matter. A misplaced strip can reduce visibility during movement.

Quality control should continue from incoming fabric to final packing. Inspectors measure fabric weight, examine stitching, and test closures such as zippers or snaps. Sample vests may undergo washing and abrasion tests. Production records should identify batches, operators, and inspection results. In practice, even careful factories miss details sometimes. A loose thread or uneven tape line can escape one inspection. Rechecking high-risk areas is necessary, especially before shipment. Reliable manufacturers train workers, keep test evidence, and adjust production when results fall short.

Key Equipment and Departments Within the Factory

What Is a High Visibility Vest Manufacturer Factory?

A high visibility vest manufacturer factory combines textile production with safety engineering. Its purpose is not merely sewing colored fabric. The ILO reported nearly three million work-related deaths and 395 million non-fatal injuries worldwide each year. That figure gives factories a serious responsibility: visibility products must perform in real working environments.

Key Equipment and Departments Within the Factory

The product design department converts site requirements into patterns, size charts, and technical drawings. It checks fluorescent fabric, reflective tape width, closure placement, and pocket strength against ANSI/ISEA 107-2020 or EN ISO 20471 requirements. The cutting department uses computerized machines for consistent panels, although manual checks remain useful when fabric rolls contain flaws. Sewing lines then assemble shoulder seams, binding, zippers, and reinforced stress points. Production managers should watch needle tension closely. Small defects can weaken an entire vest.

The reflective-material department applies heat-transfer or stitched tape with controlled temperature and pressure. Testing technicians measure color performance, dimensional stability, and reflective brightness. A quality report should record batch numbers, wash results, inspection samples, and corrective actions. The UK Health and Safety Executive recorded 664,000 workplace injuries in 2023/24, showing why dependable protective clothing matters. Warehousing staff protect finished vests from moisture, dust, and compression. Factories can still miss hidden seam failures. Regular sampling, worker feedback, and independent testing remain necessary.

How to Evaluate and Choose a Reliable Manufacturer Factory

What Is a High Visibility Vest Manufacturer Factory?

How to Evaluate and Choose a Reliable Manufacturer Factory

A high visibility vest manufacturer factory produces safety garments with reflective materials, bright fabrics, and controlled stitching processes. A reliable factory should explain its production flow clearly. Ask for fabric specifications, reflective tape performance, size charts, and washing test results. Ask for evidence. Product samples should show even seams, secure pockets, clean edges, and readable labels. Details matter.

During a factory evaluation, inspect quality control at several stages. Check incoming fabric records, cutting accuracy, sewing inspections, and final packing procedures. A professional manufacturer can provide test reports from qualified laboratories and explain how those reports match the finished vest. Traceability is also important. Each batch should connect to material records, inspection notes, and shipment documents. This reduces confusion when a problem appears later.

Capacity deserves careful attention. A factory may promise large orders, yet struggle during busy seasons. Request realistic production schedules and ask how workers manage urgent changes. Clear communication usually reveals operational maturity. I have seen attractive samples hide weak stitching on later batches, so one sample is never enough. Request pre-production samples and random checks. No factory is perfect. Small gaps matter. A reliable partner admits limitations, documents corrective actions, and welcomes reasonable inspections. The final choice should balance quality, delivery control, communication, and consistent evidence rather than a low quotation alone.

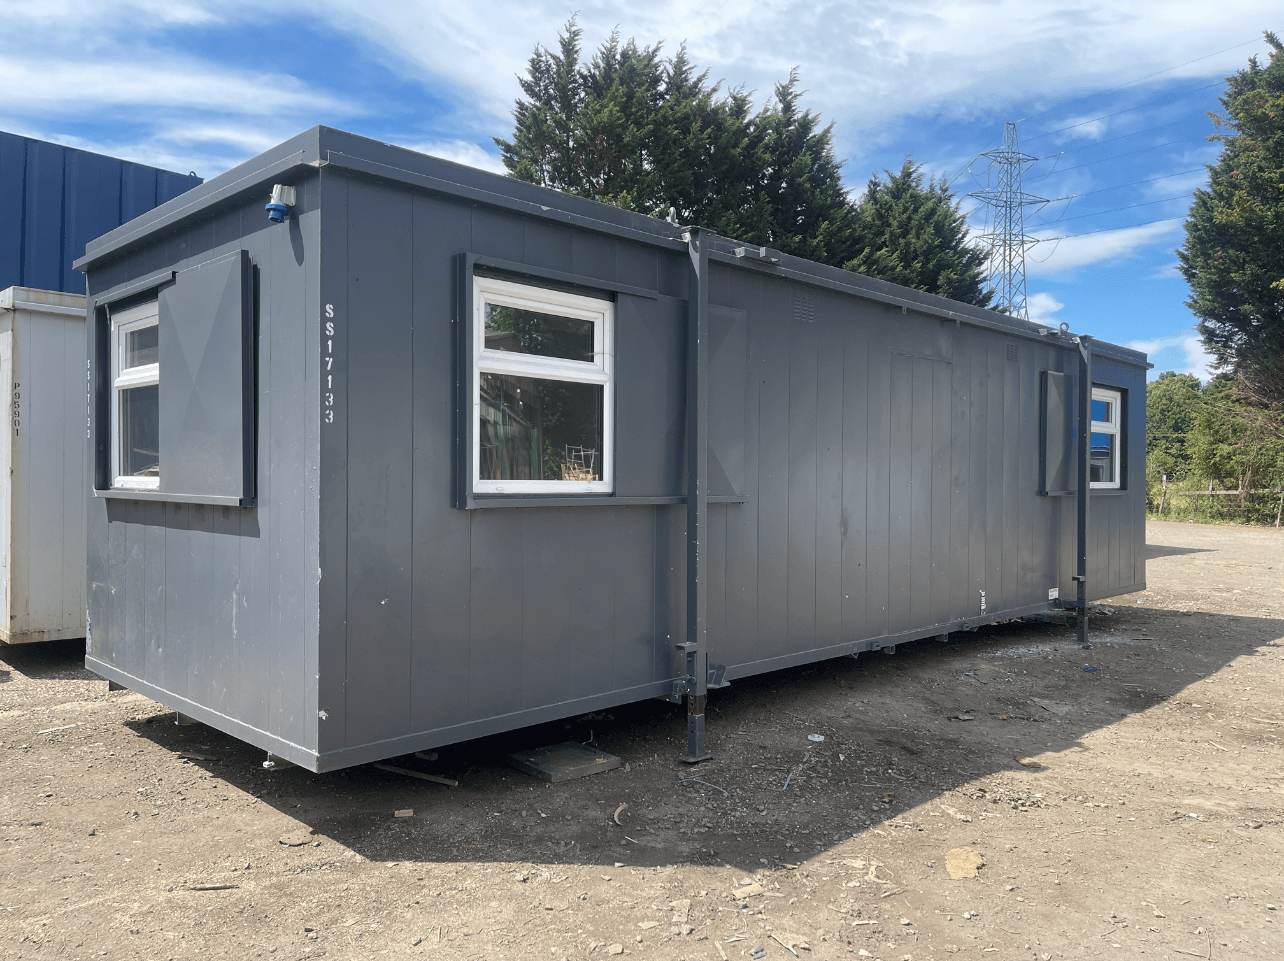
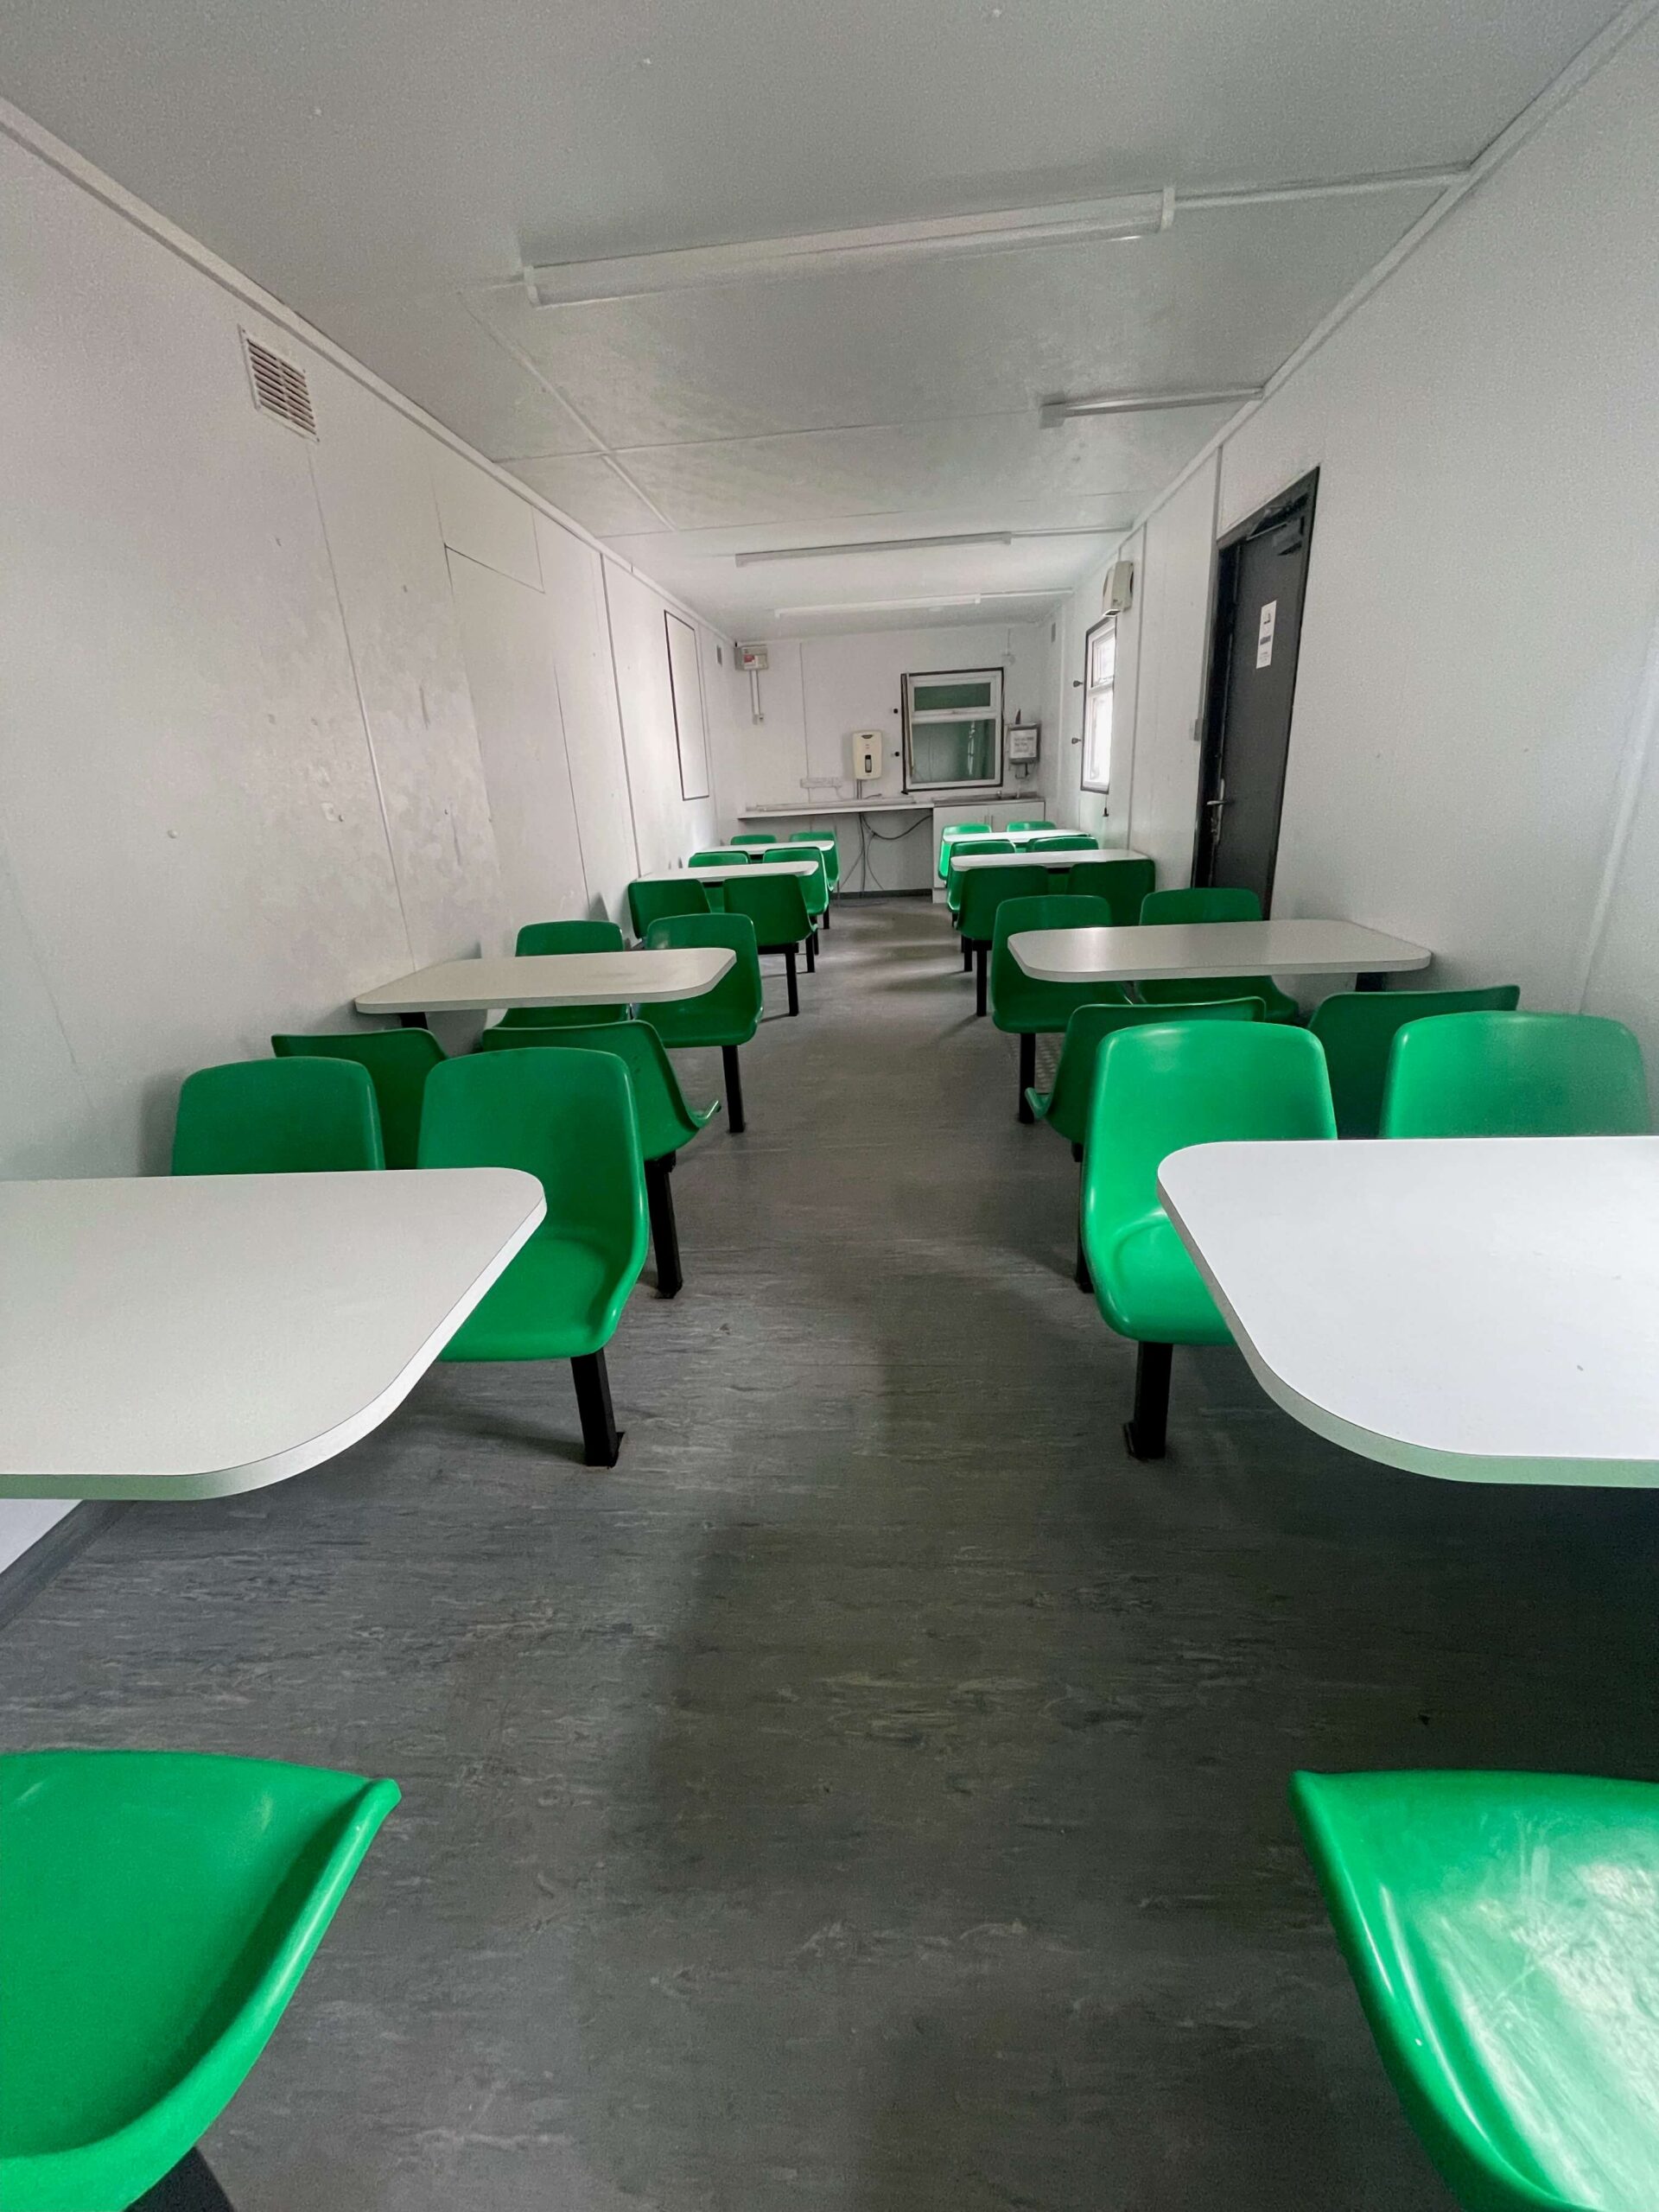
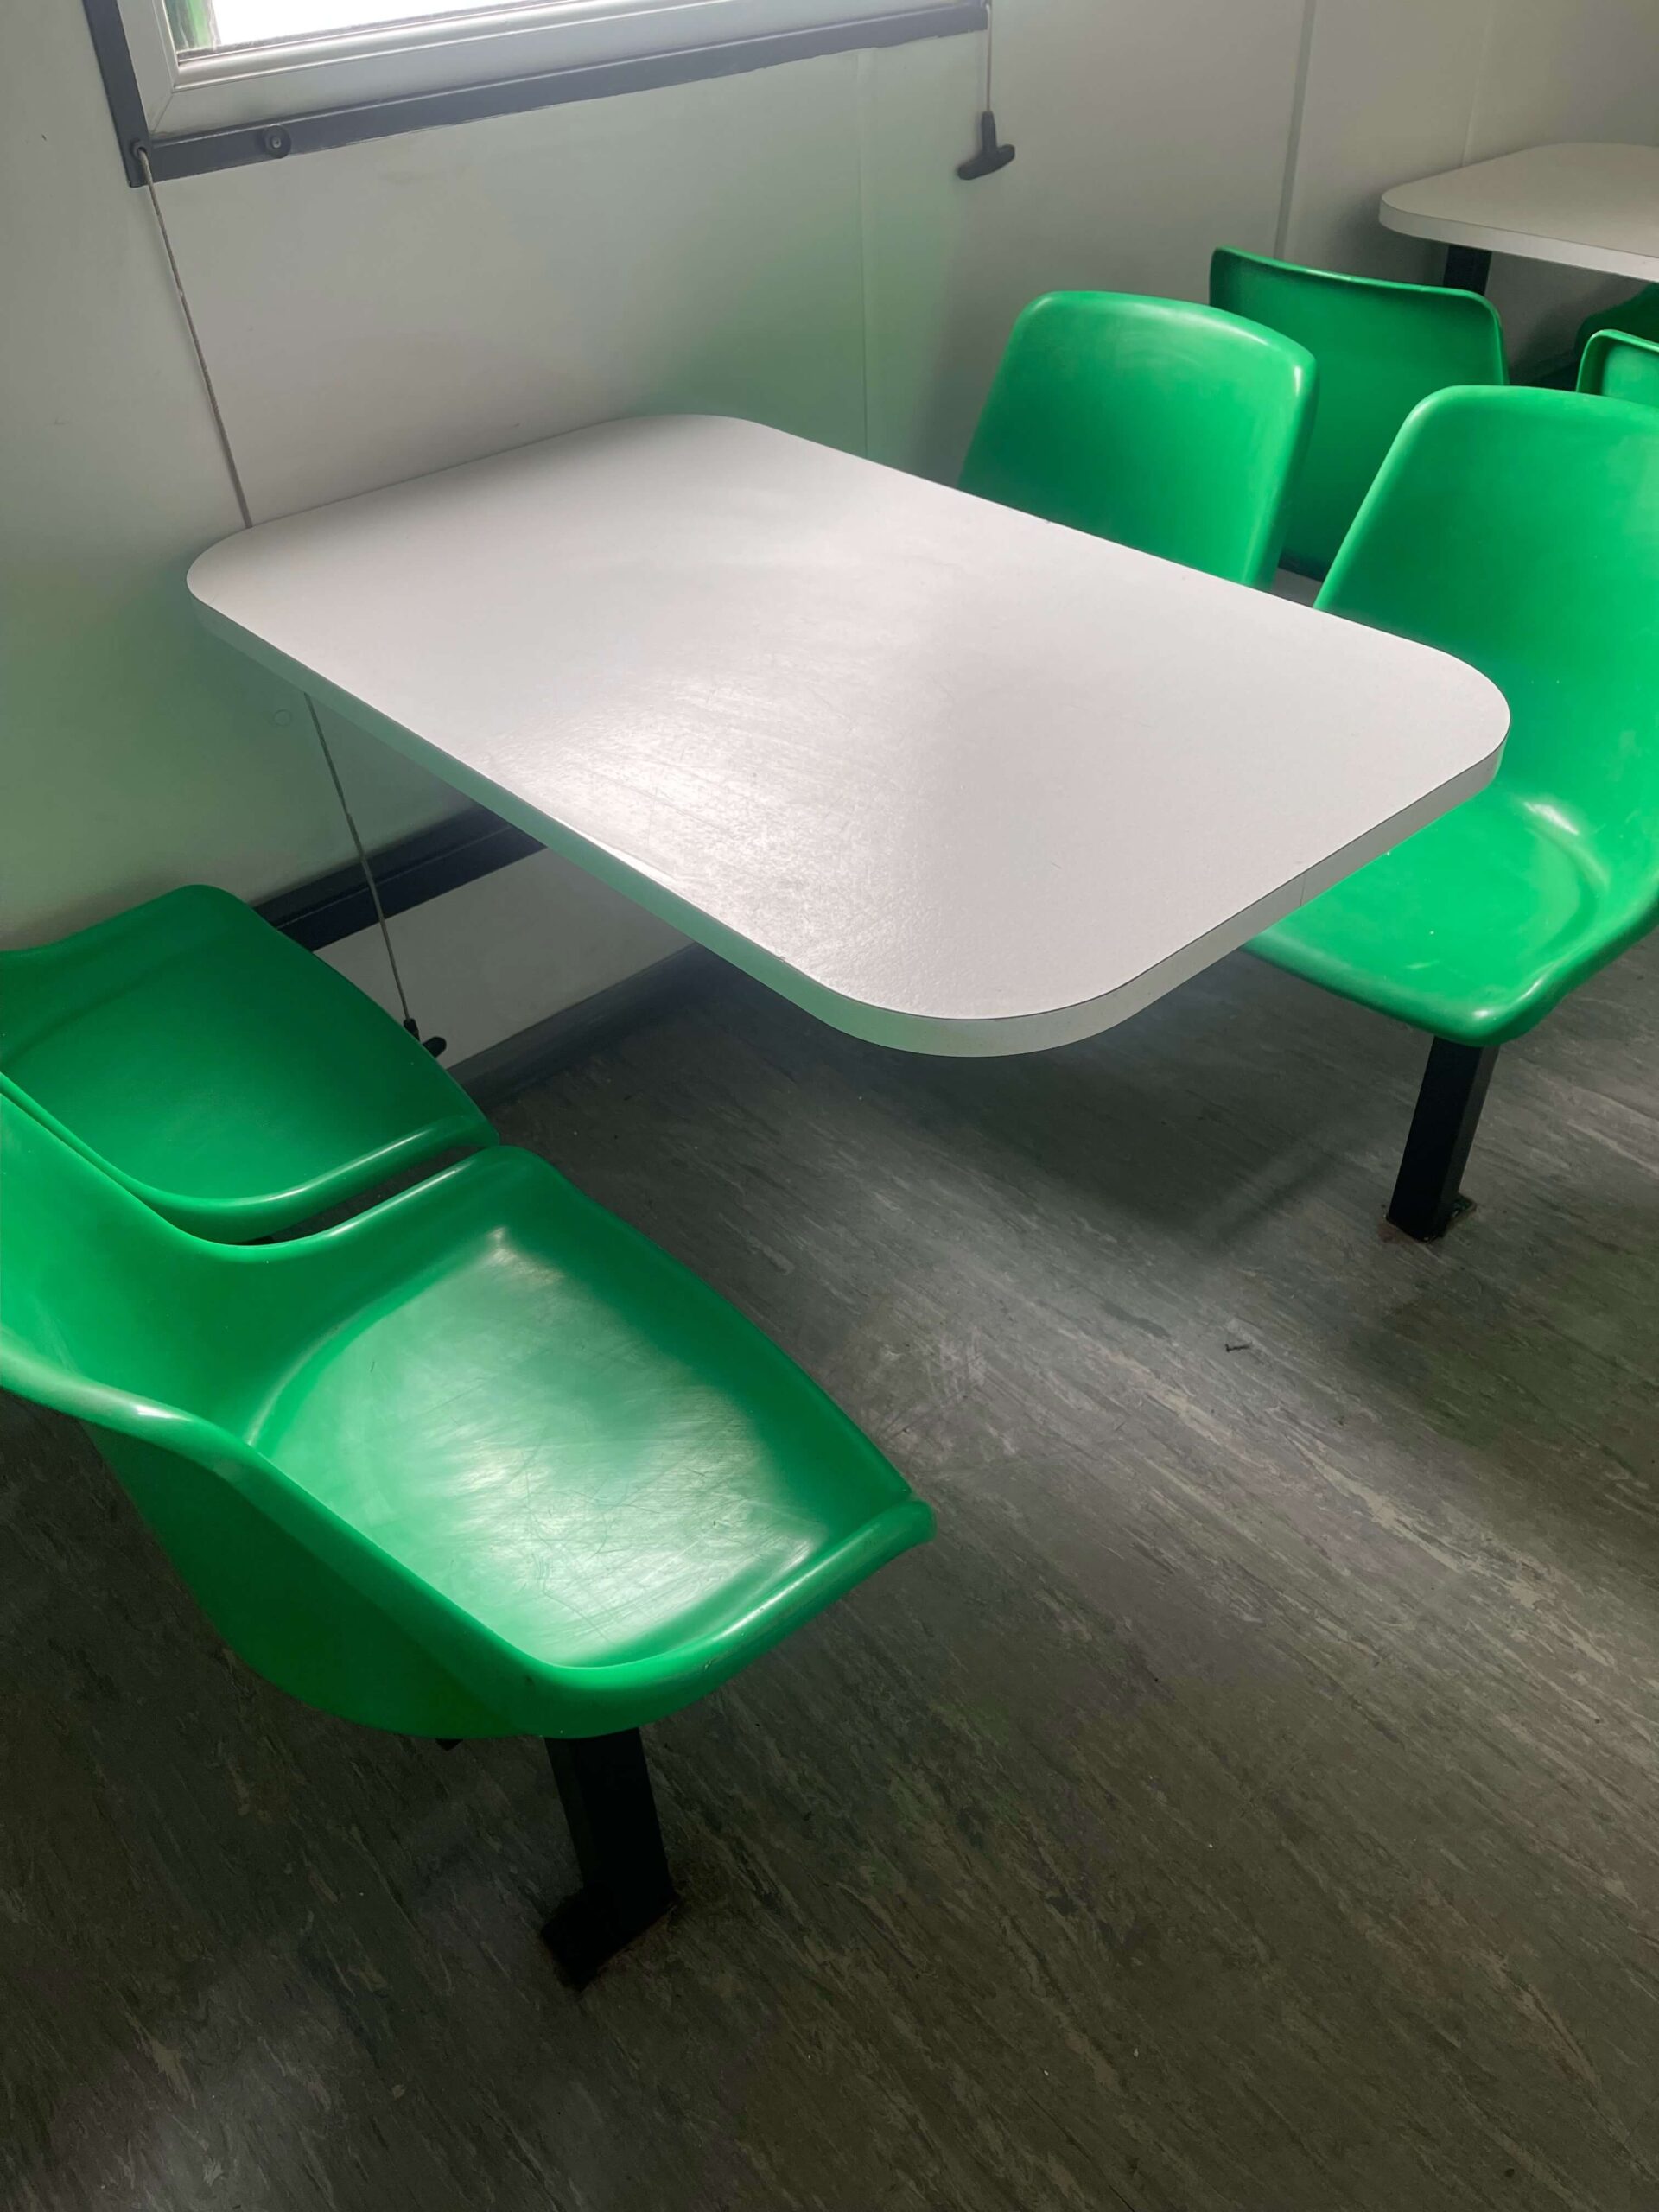
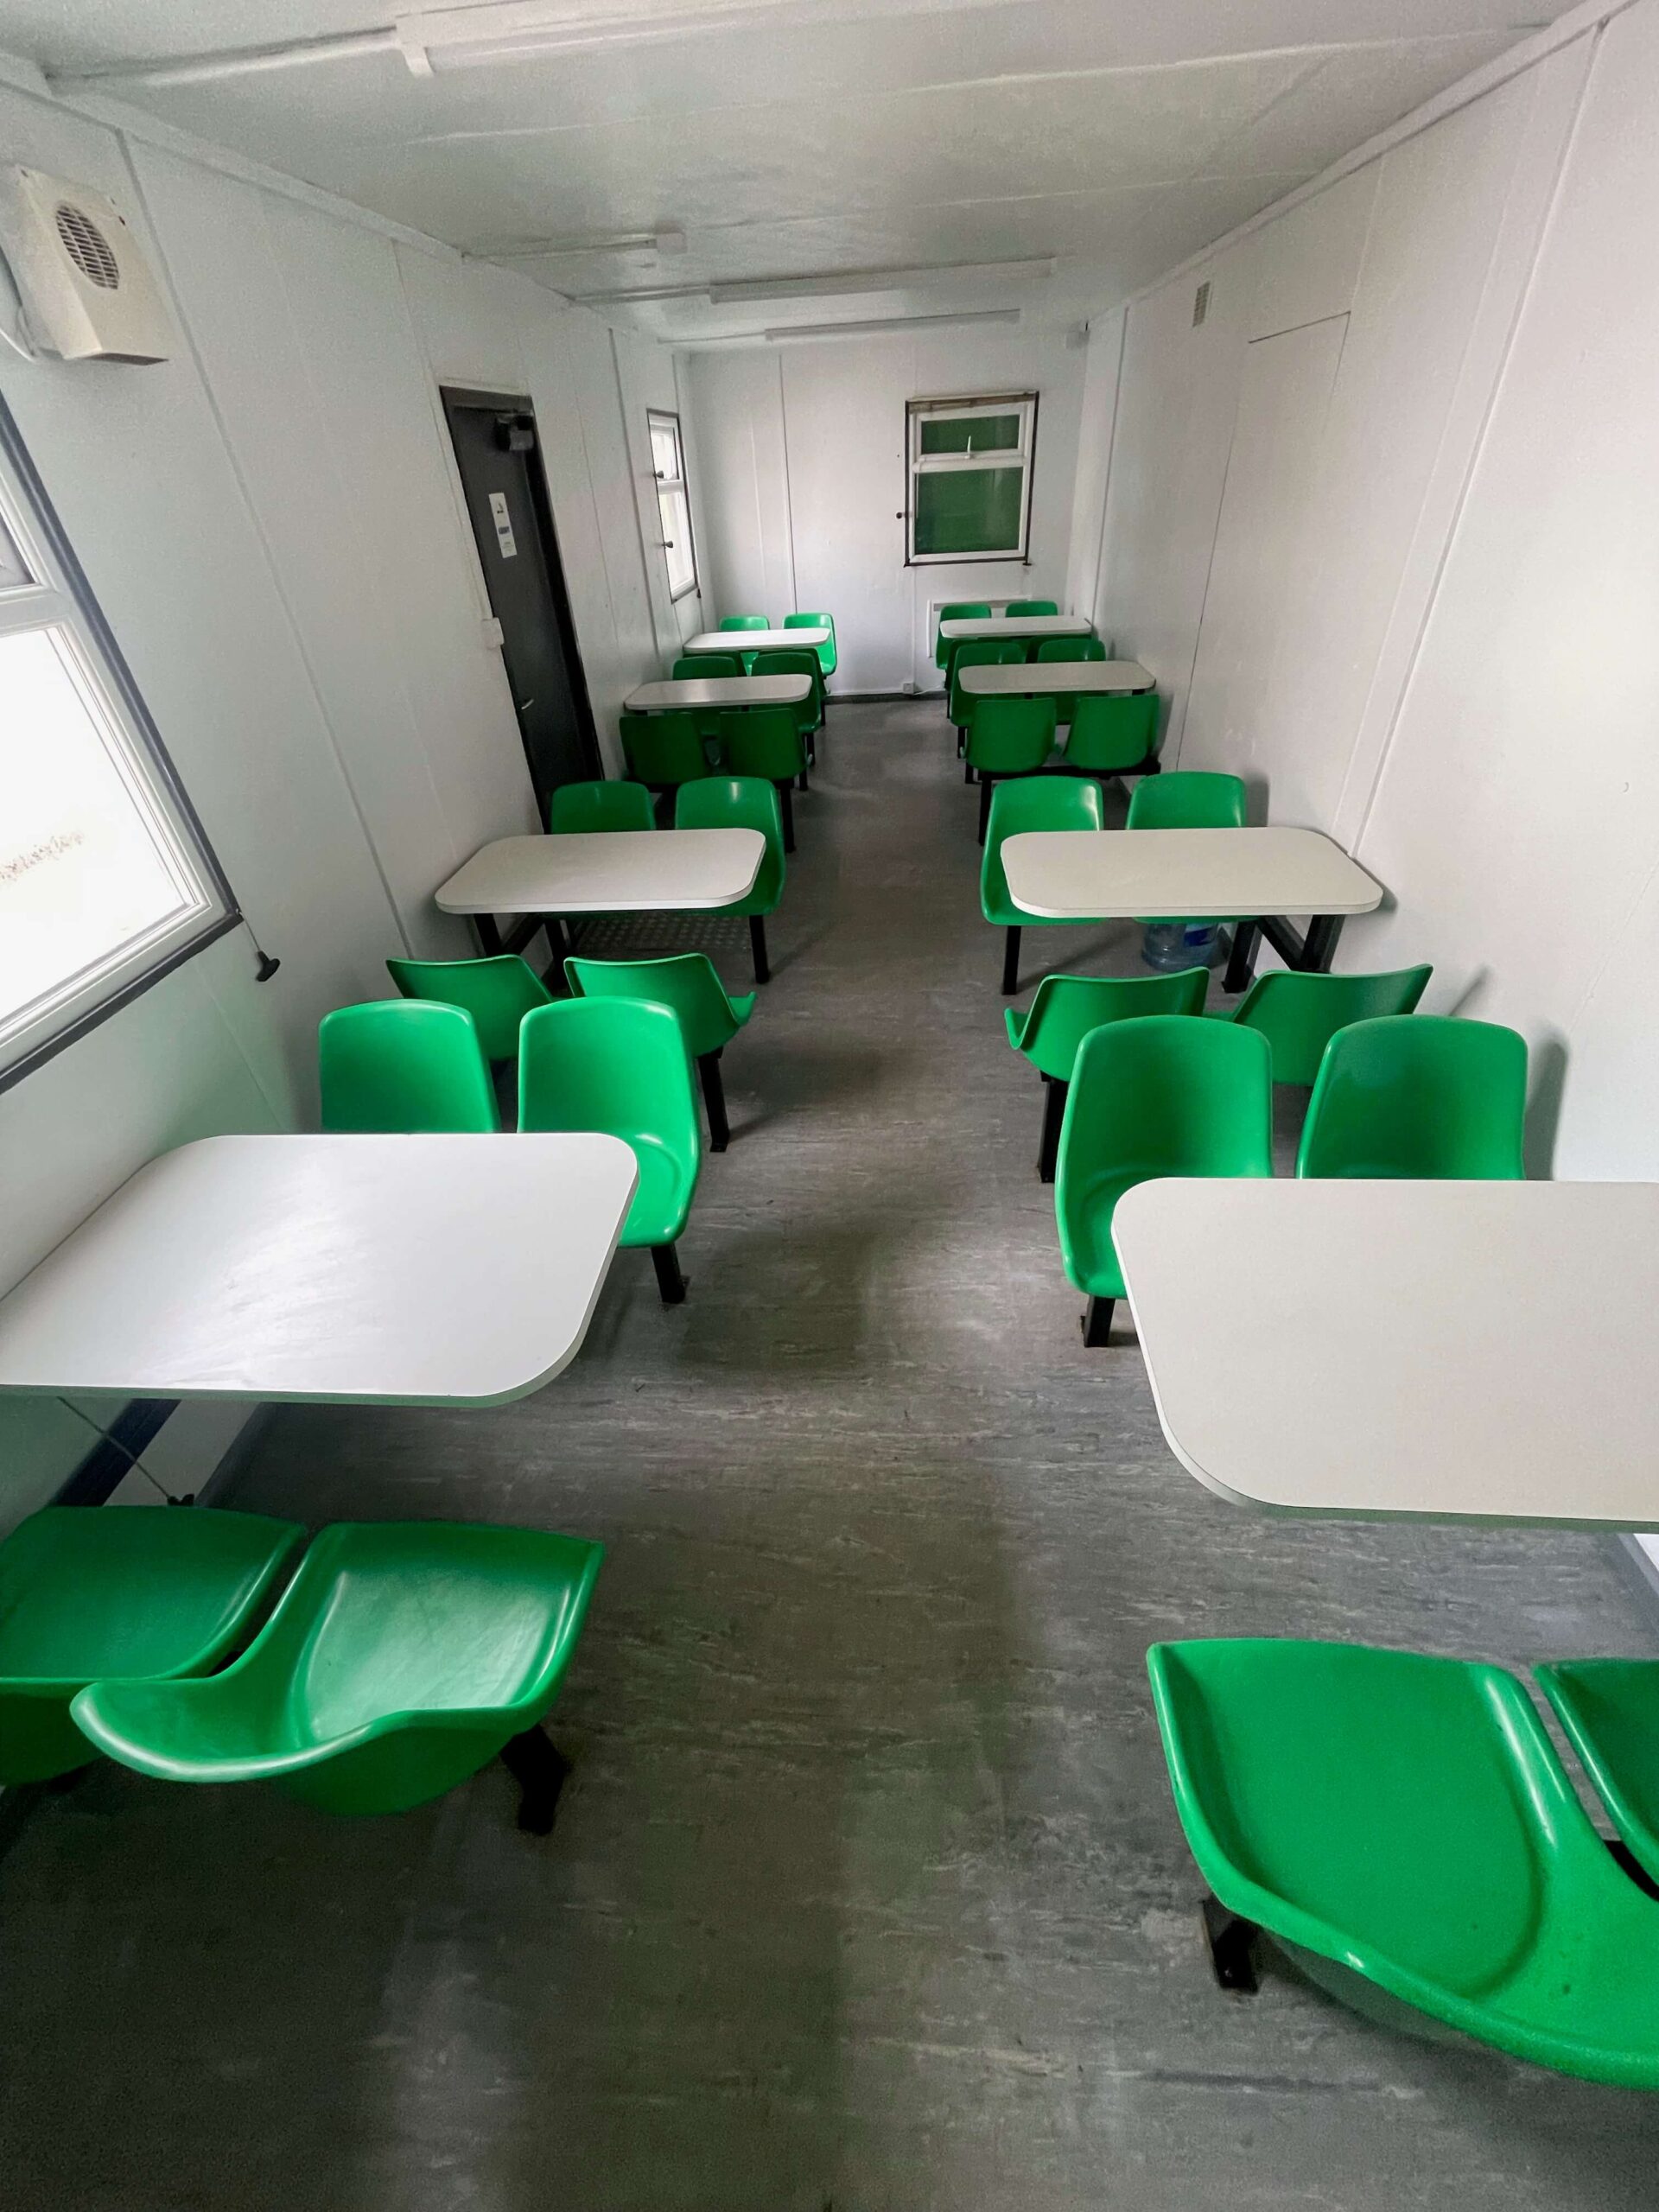
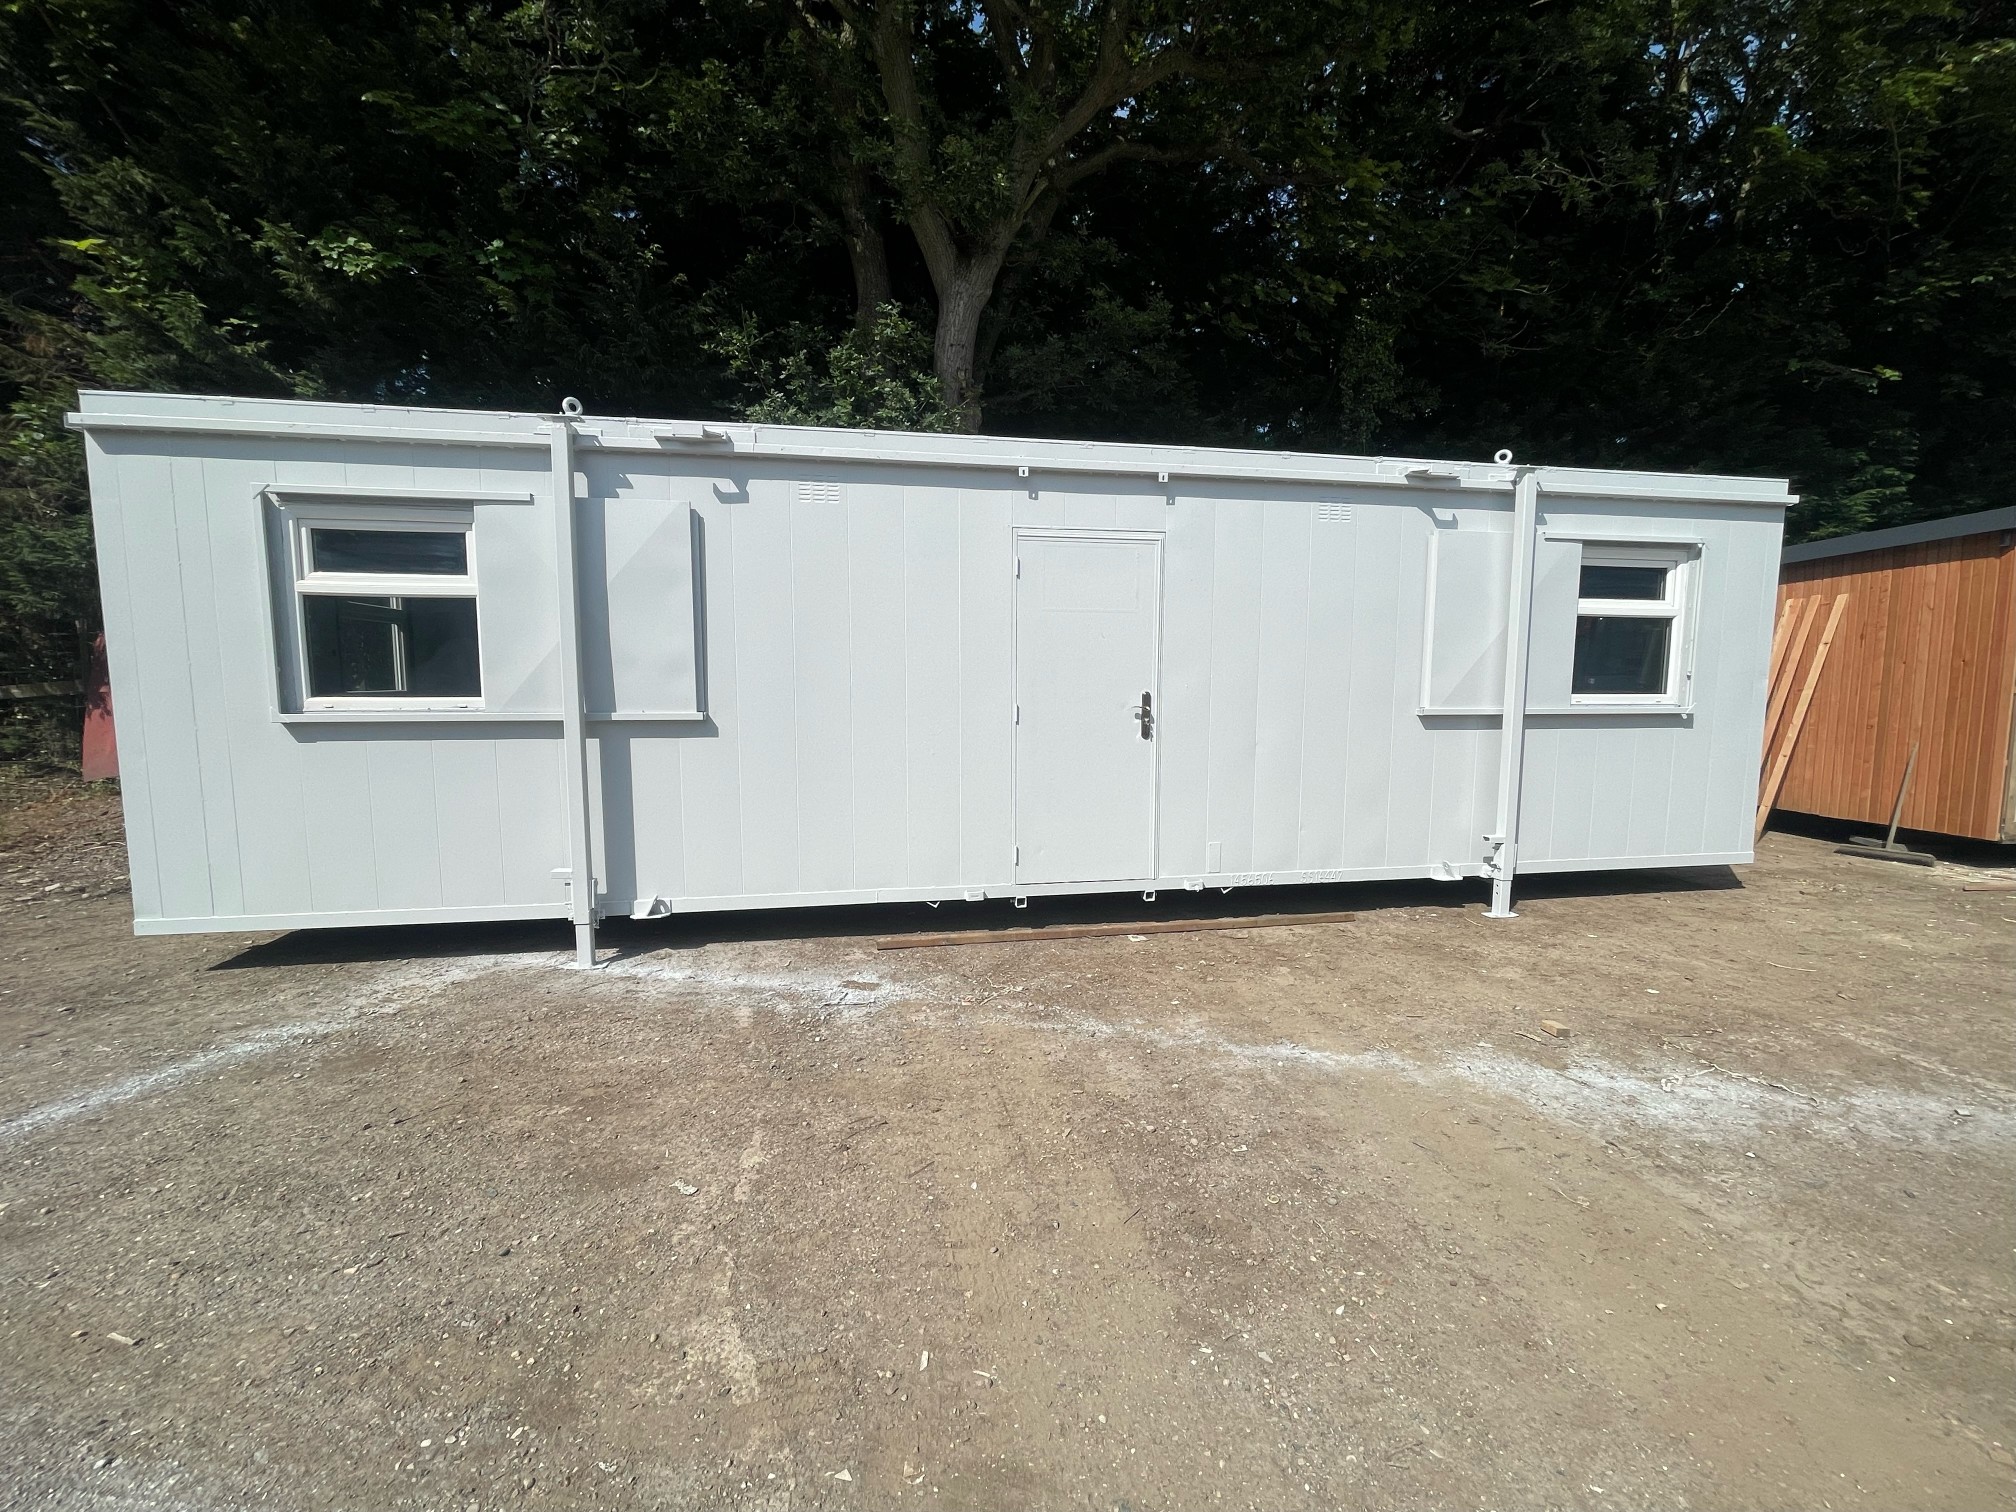
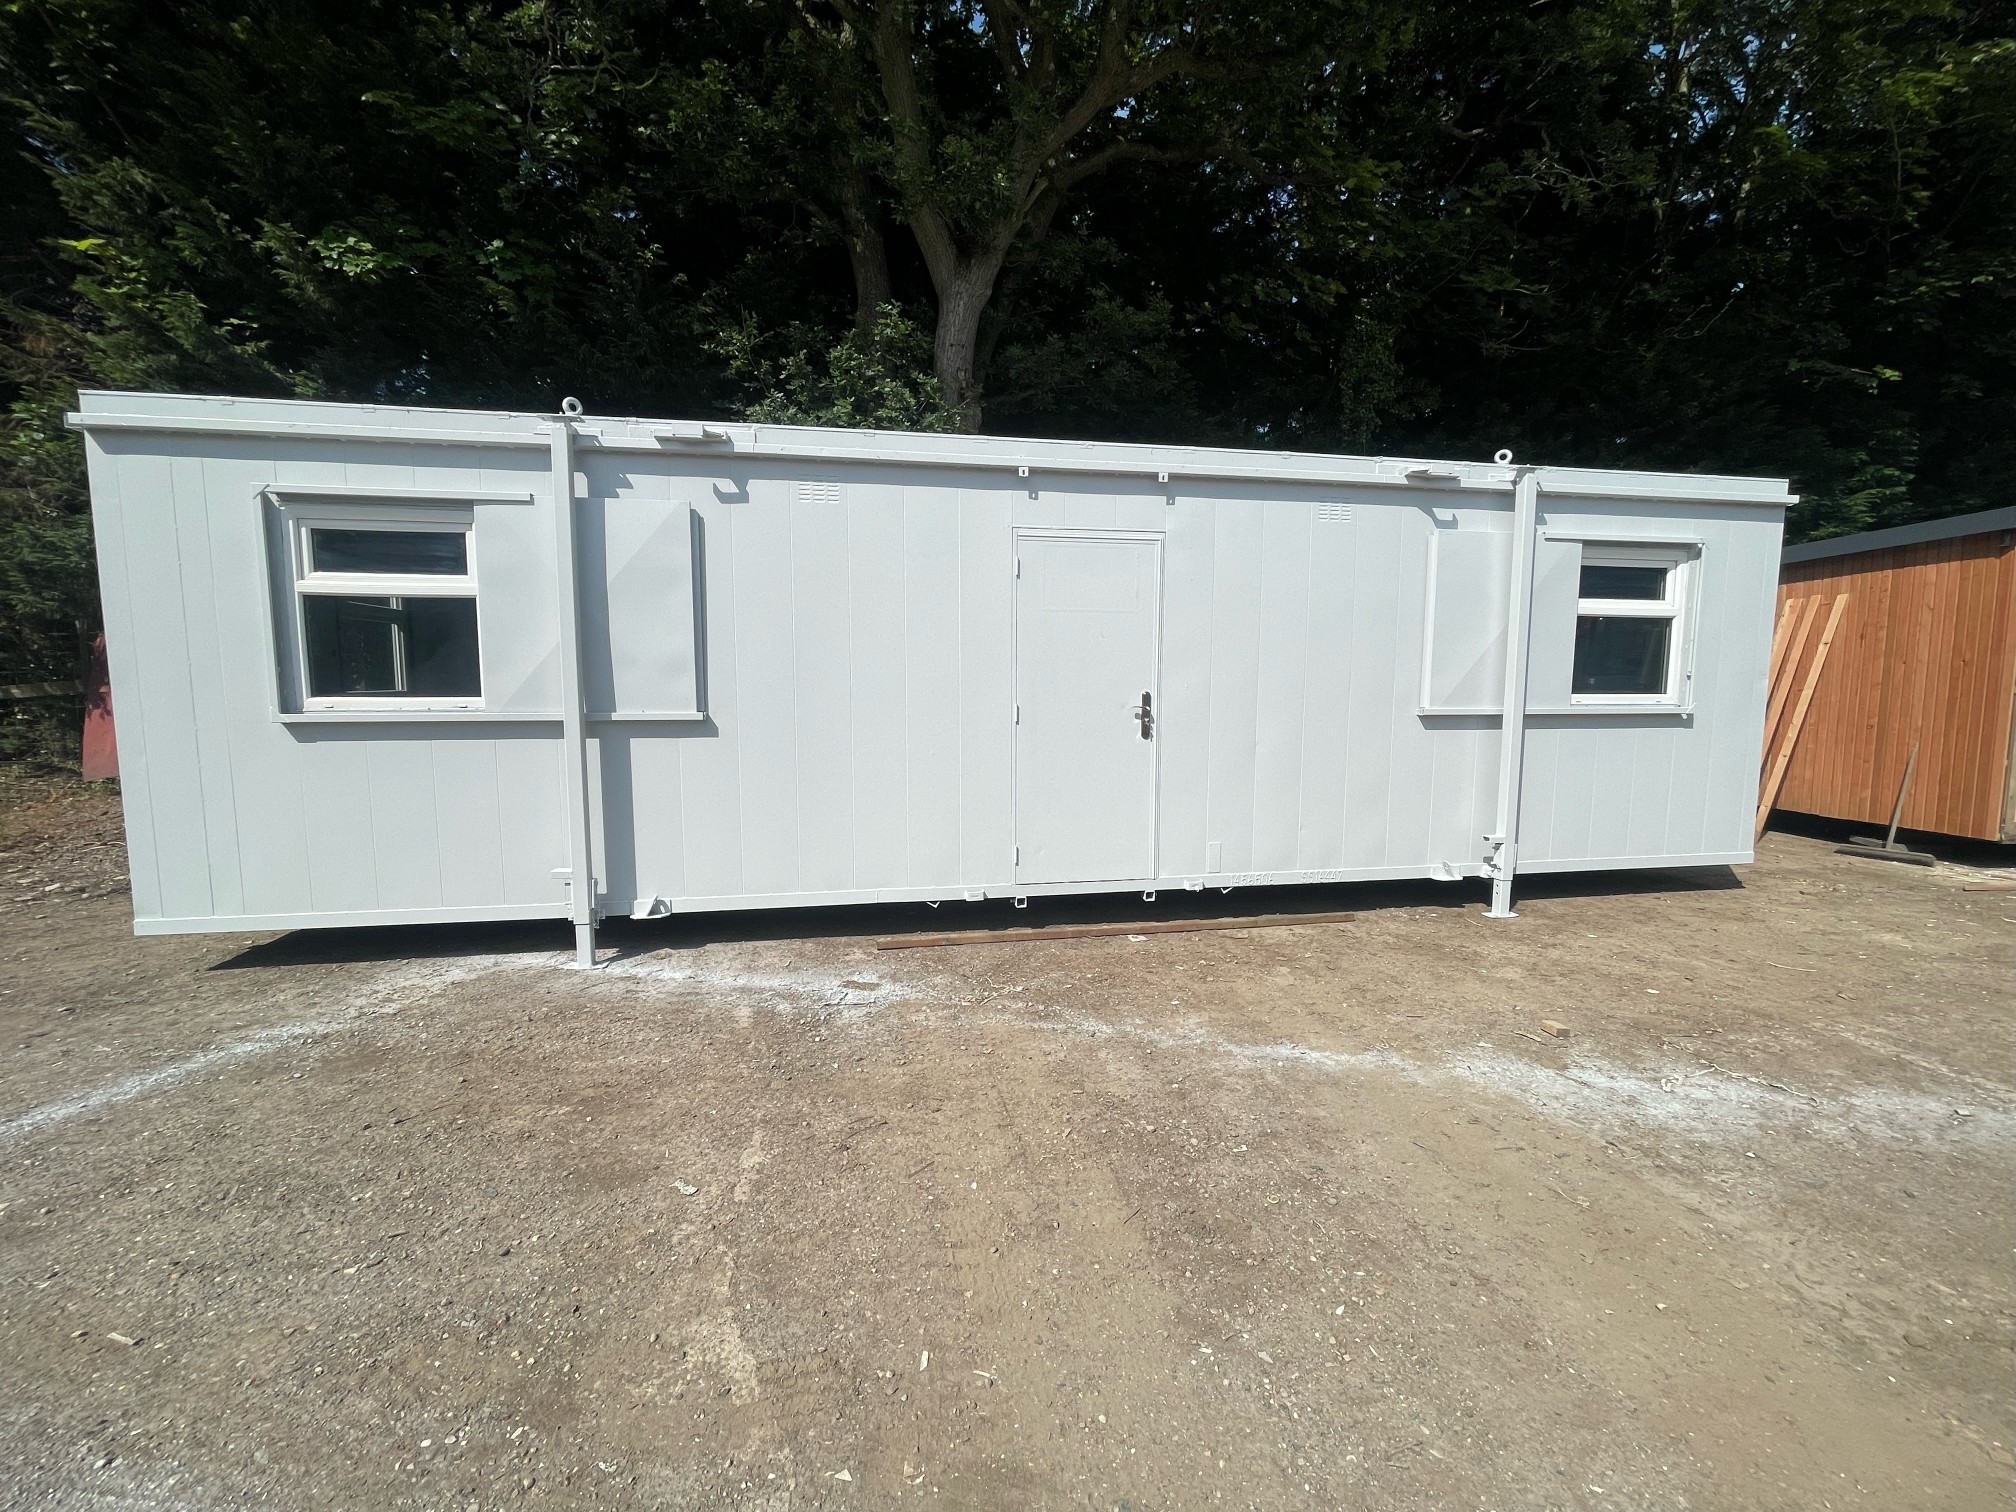
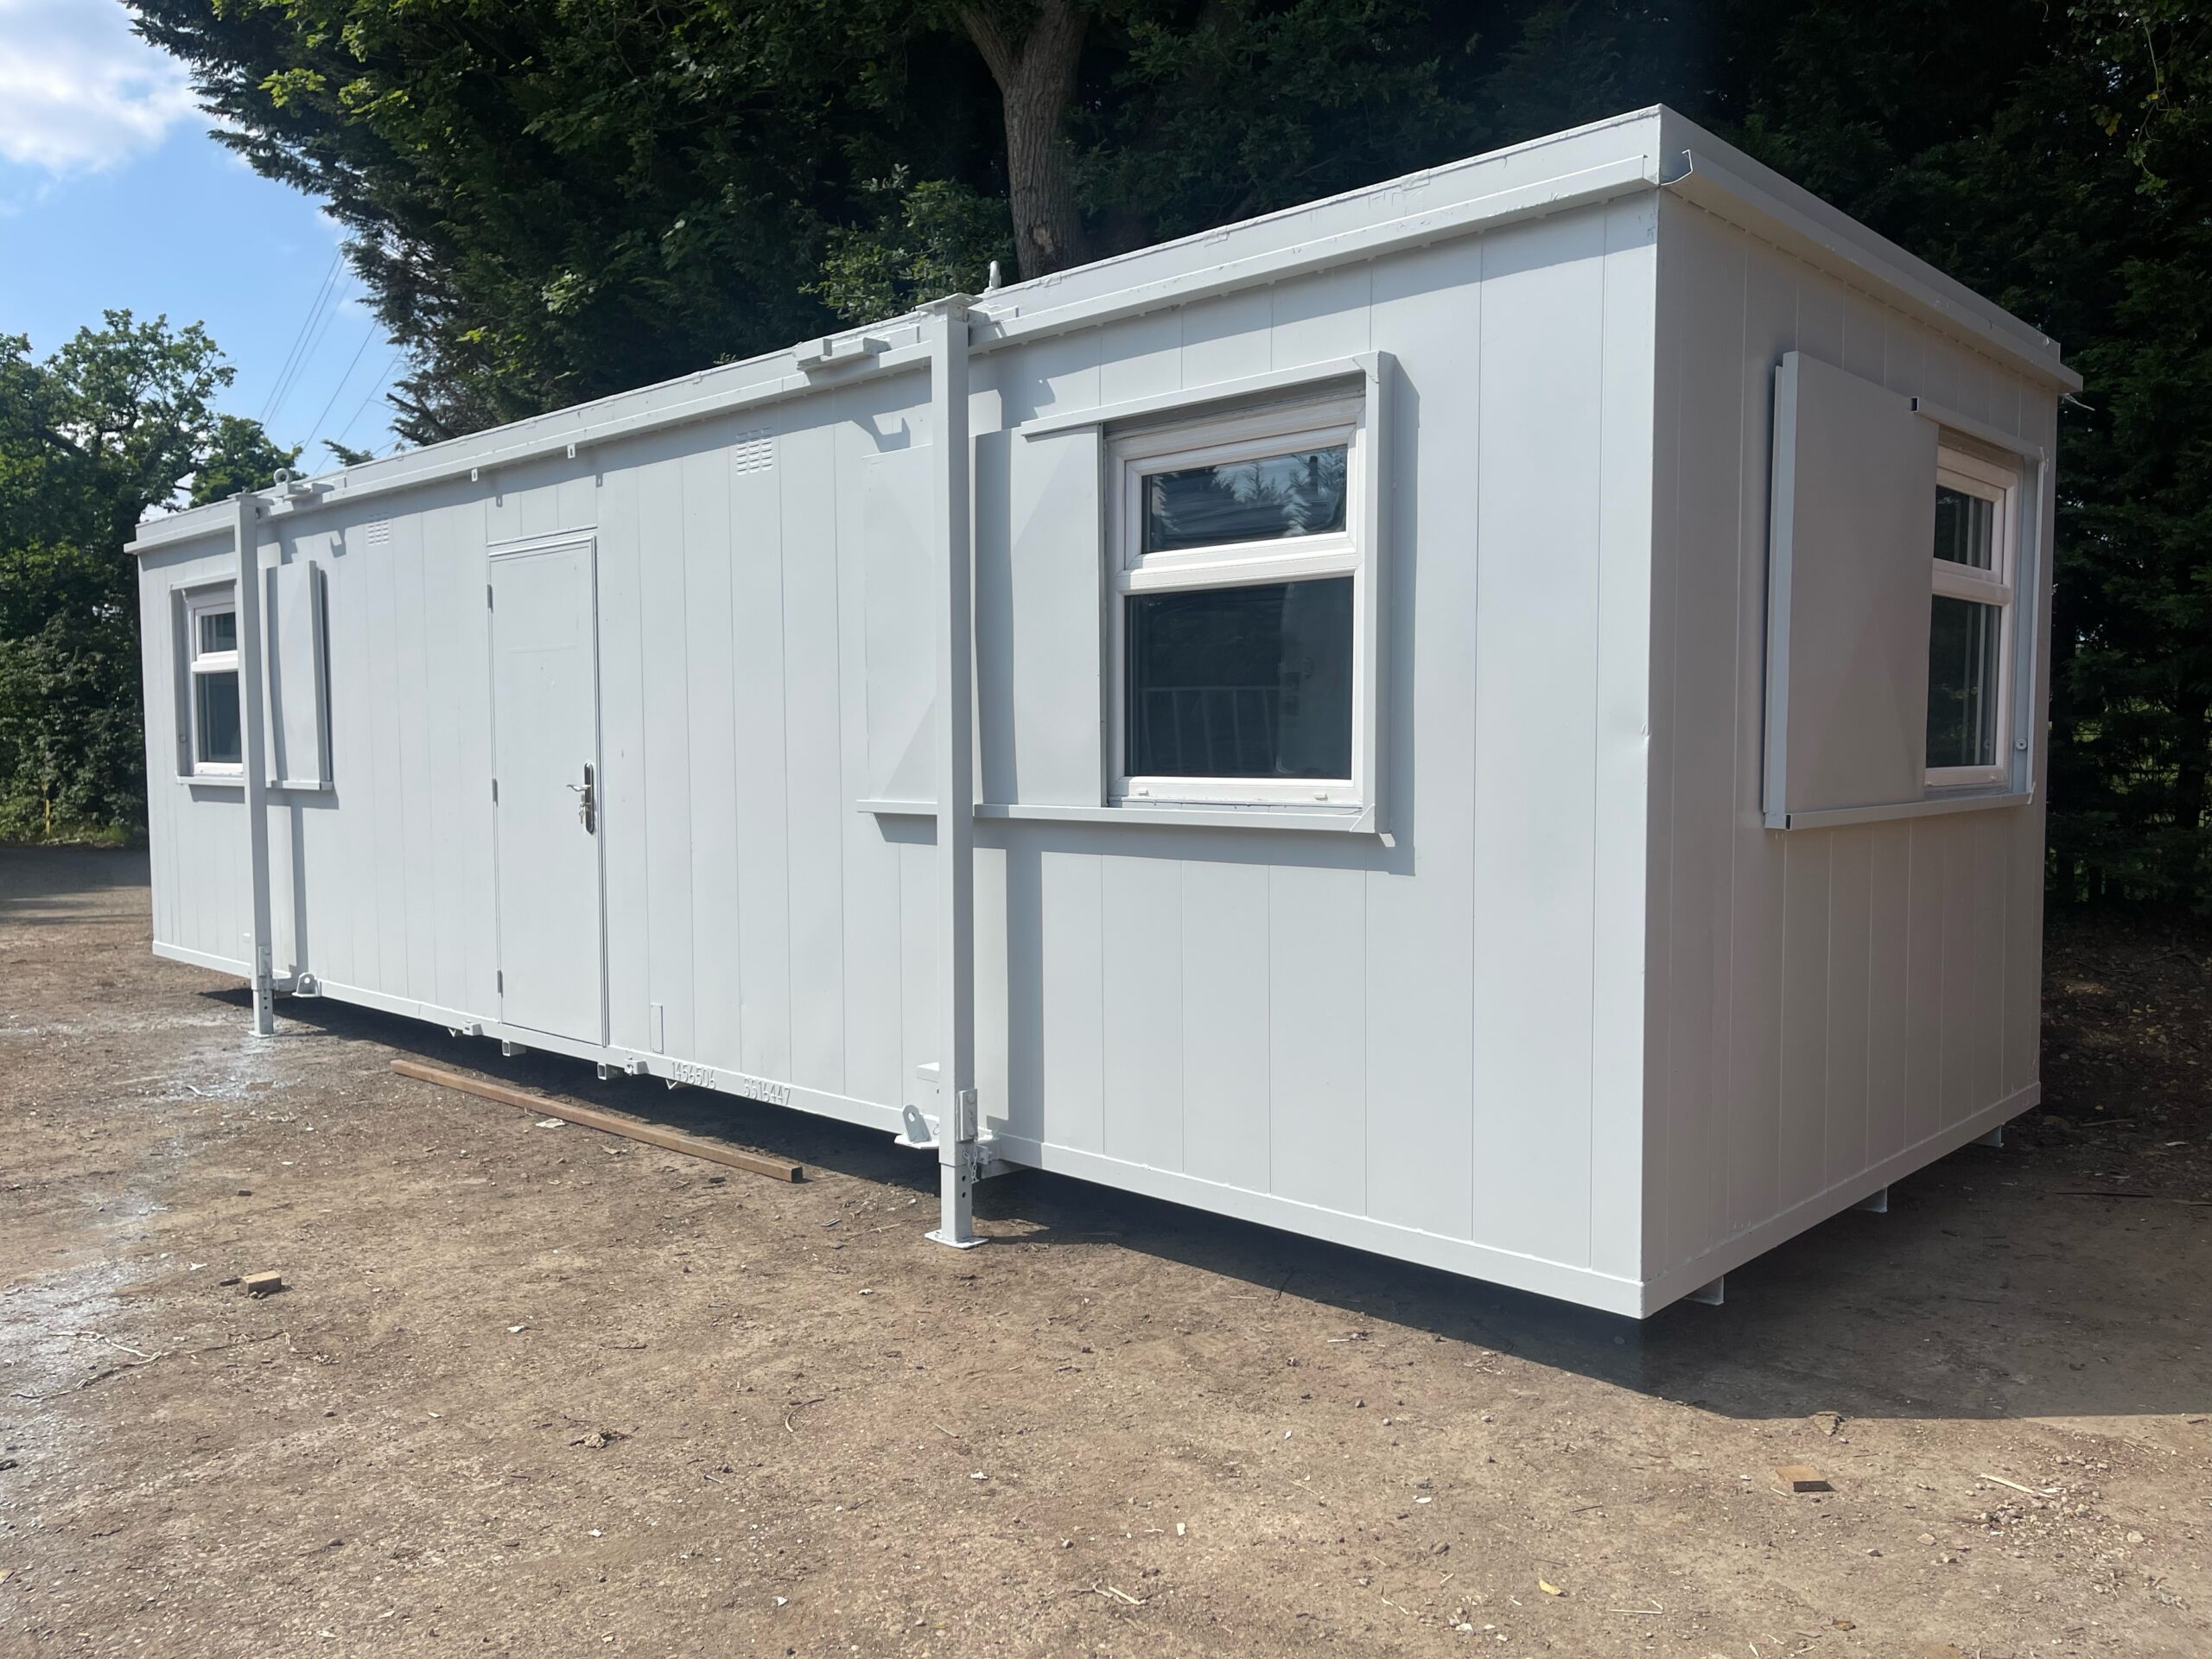
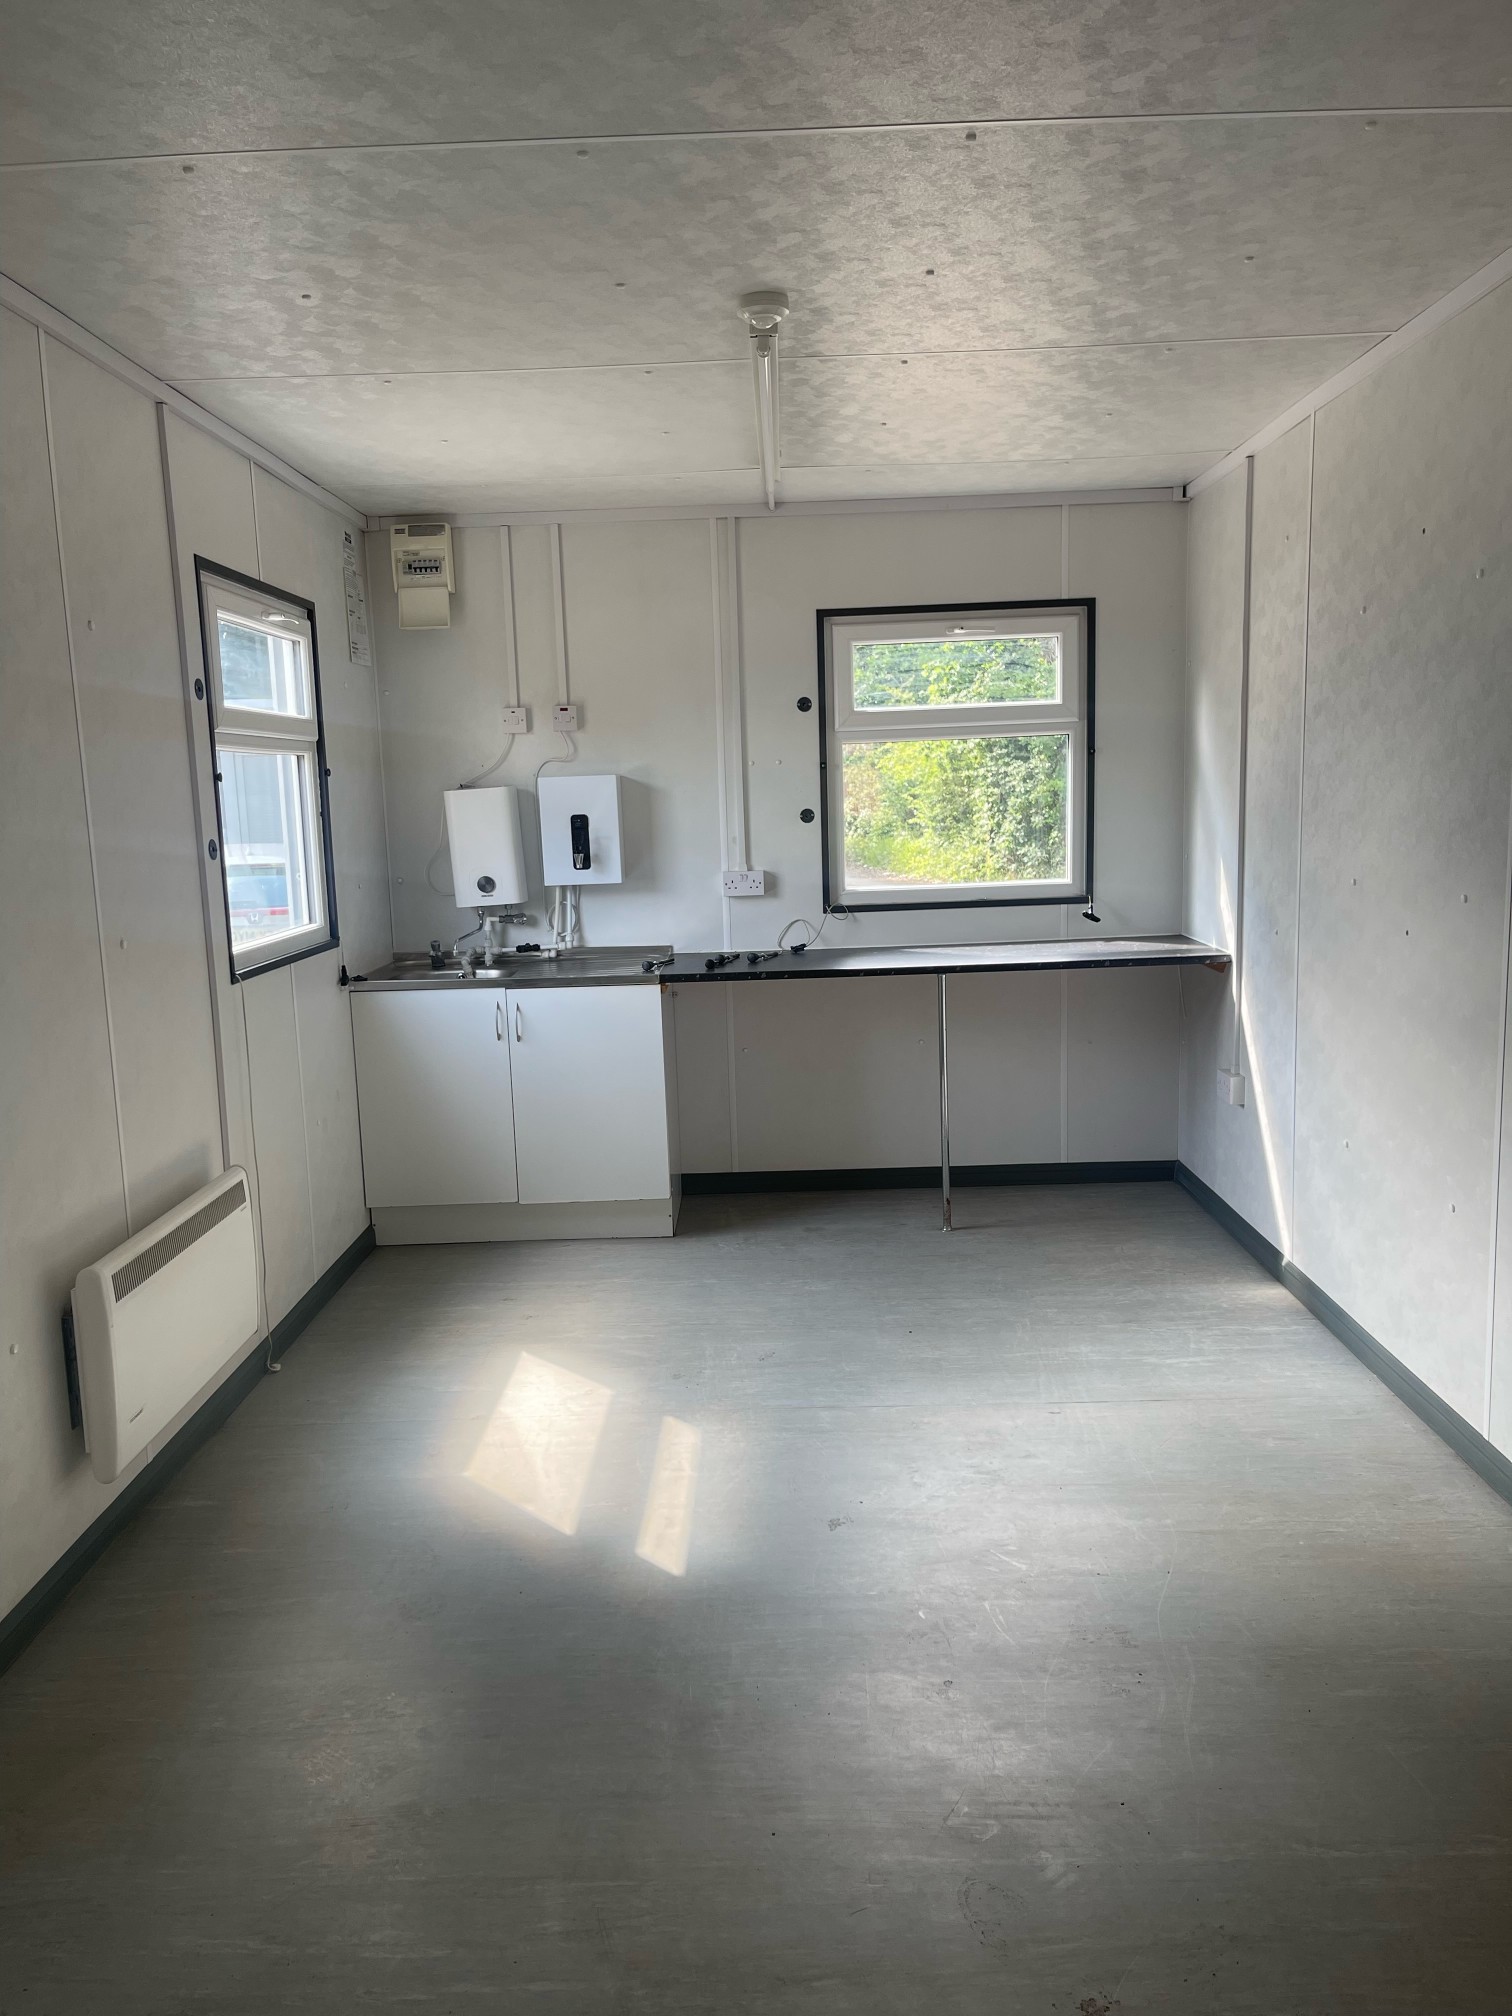
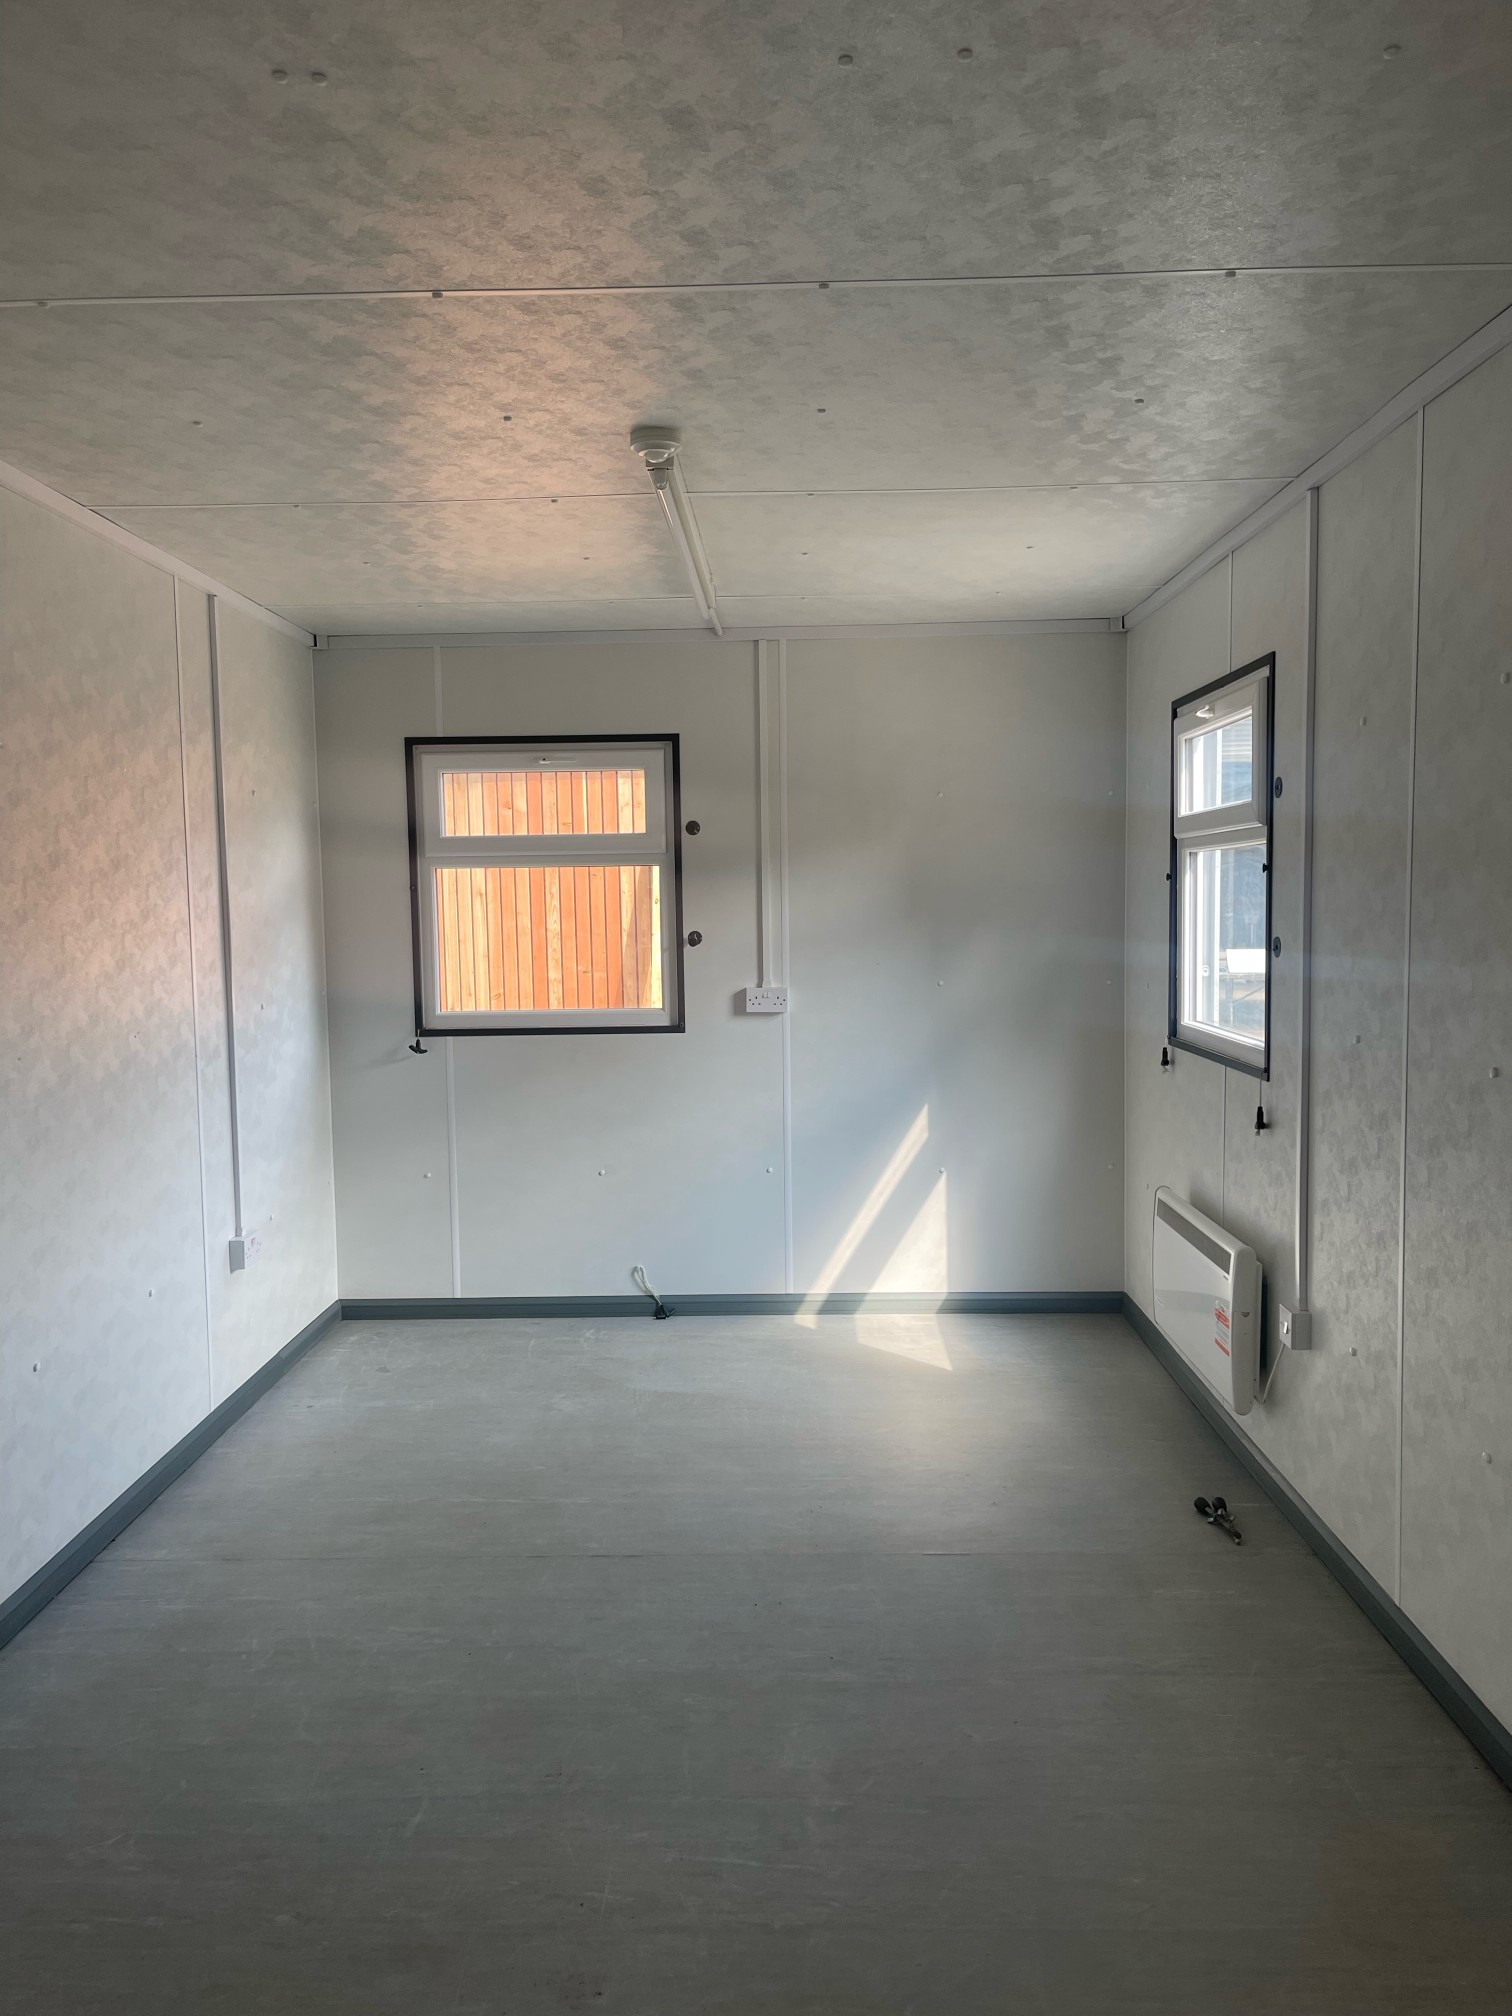
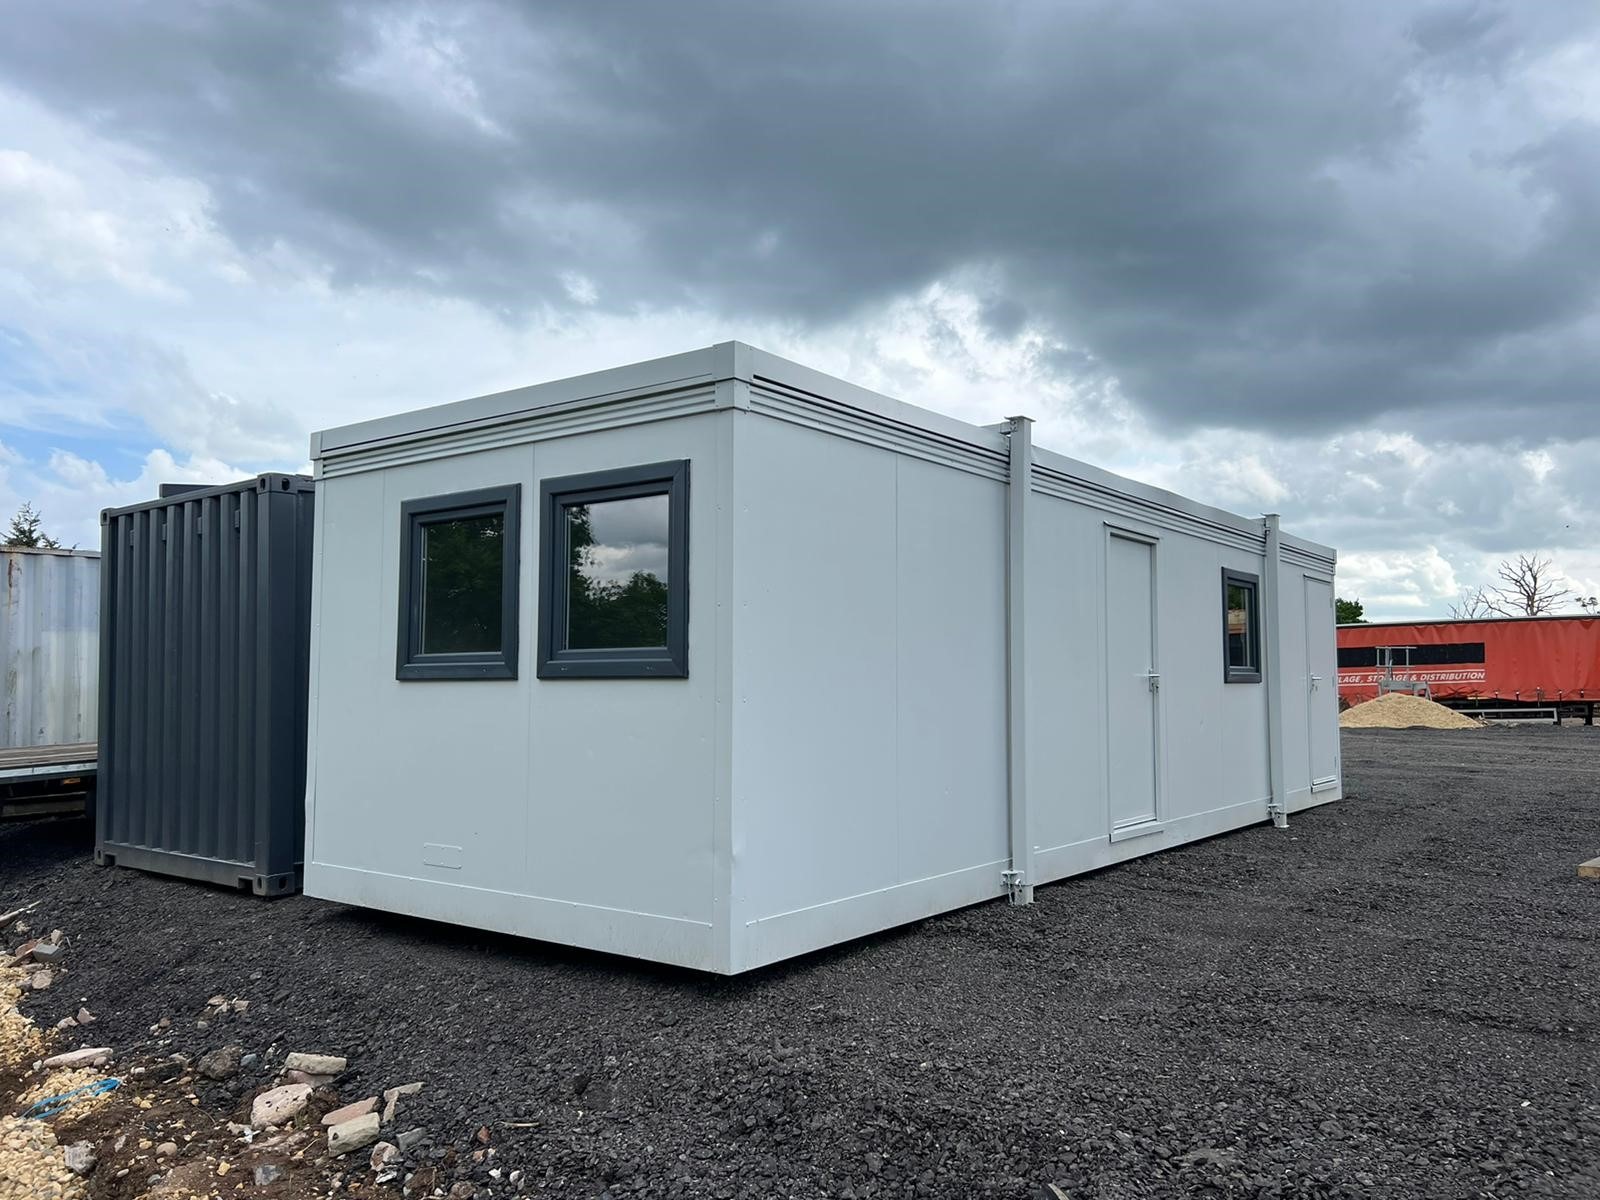
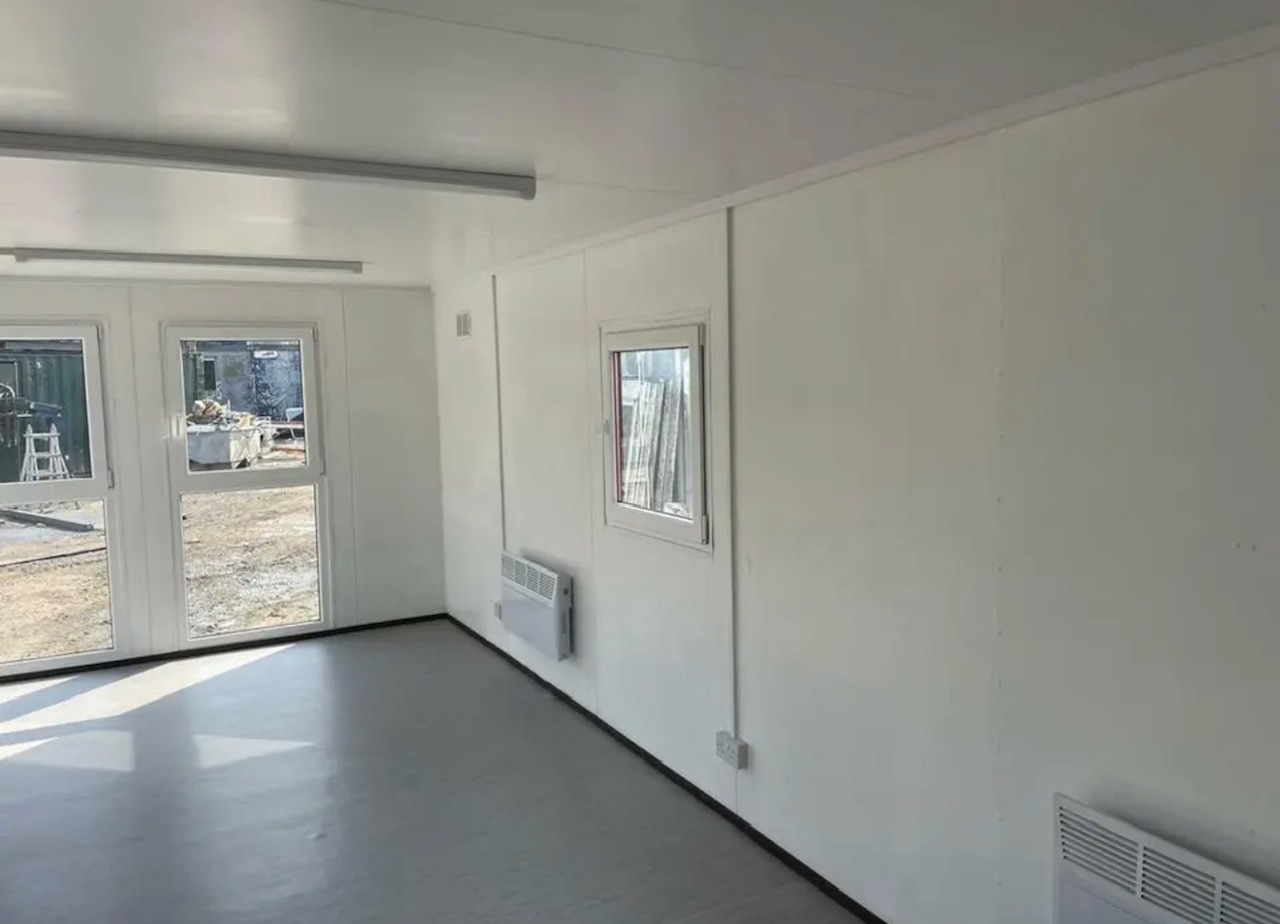
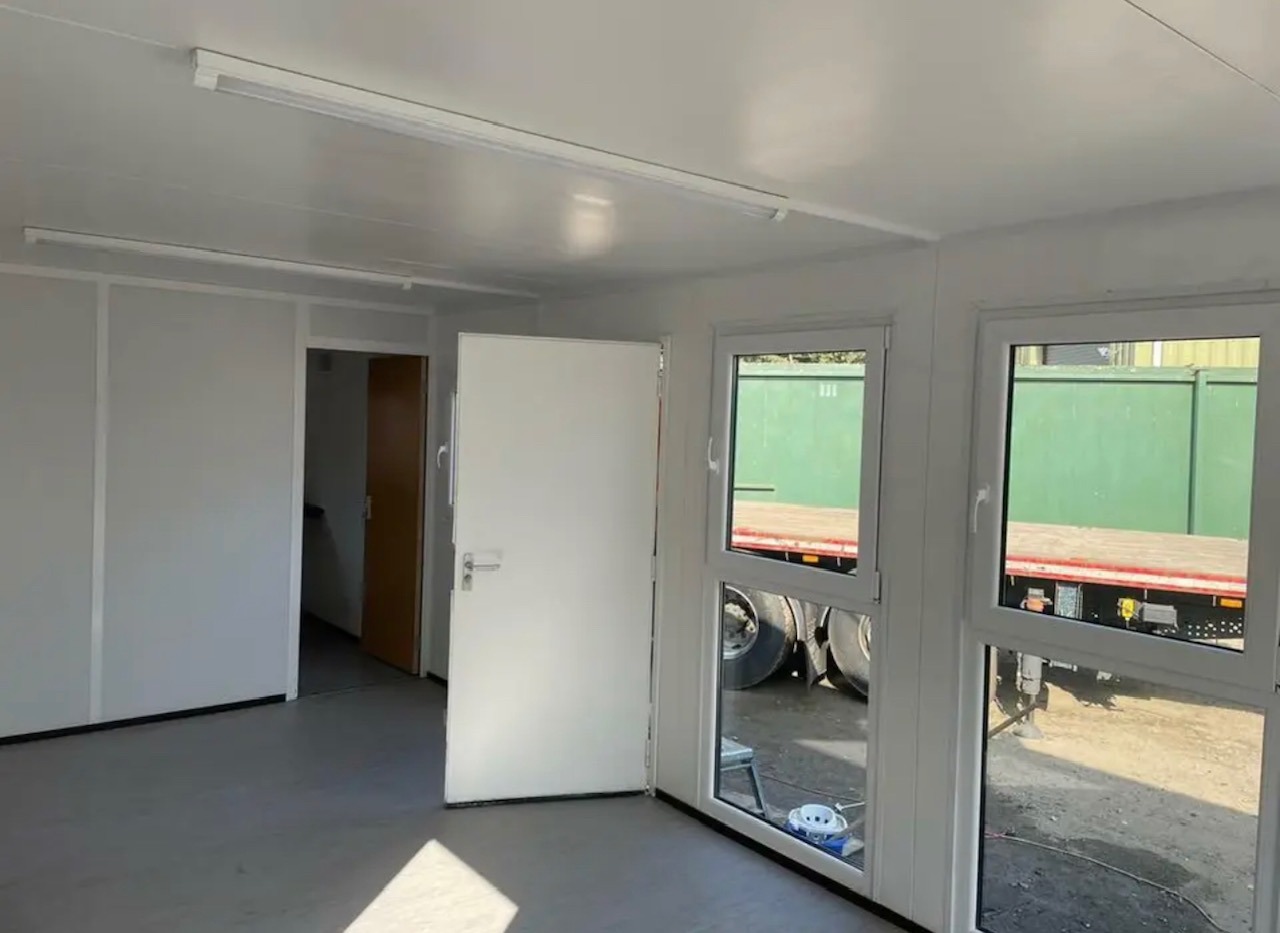
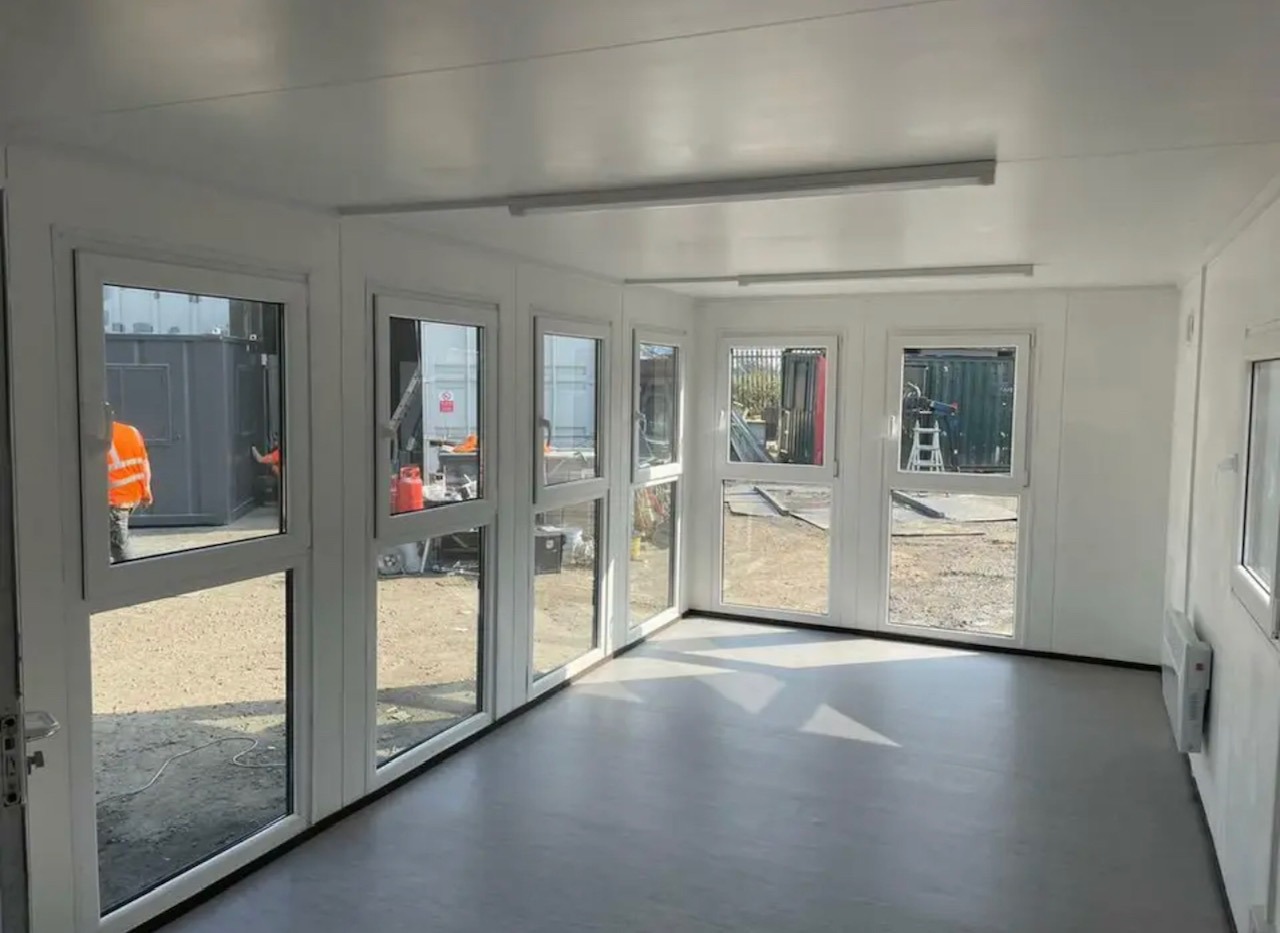
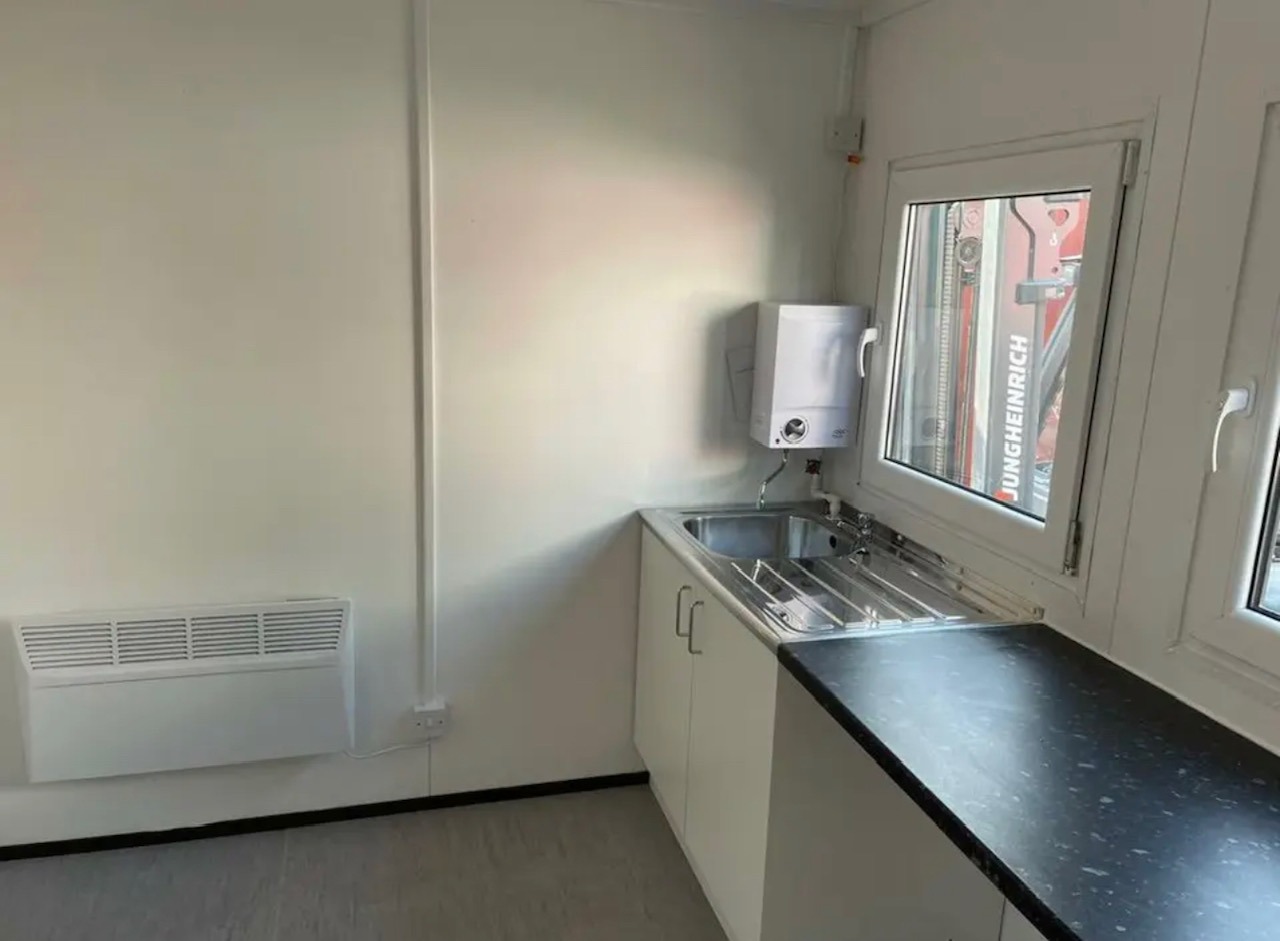
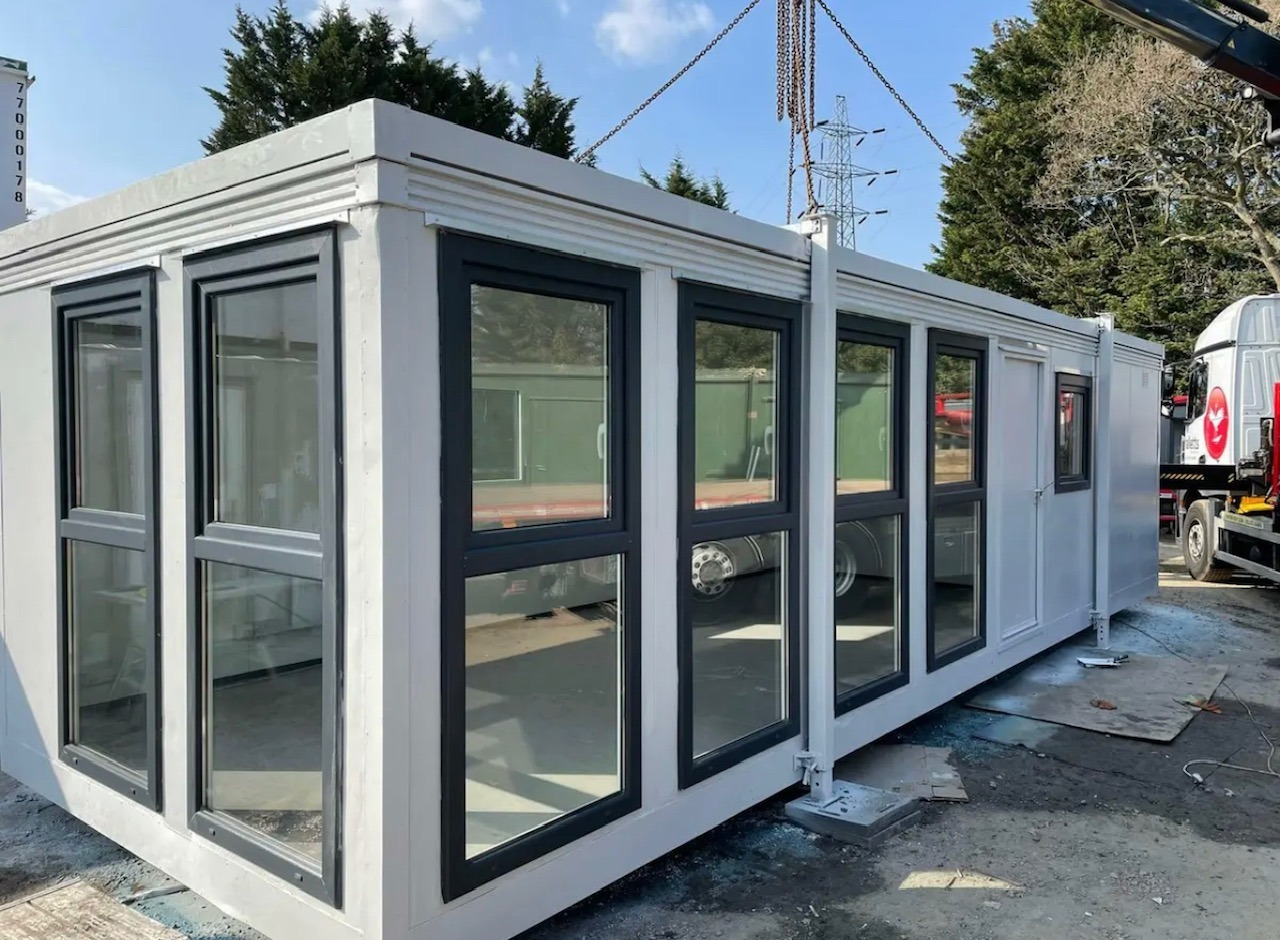
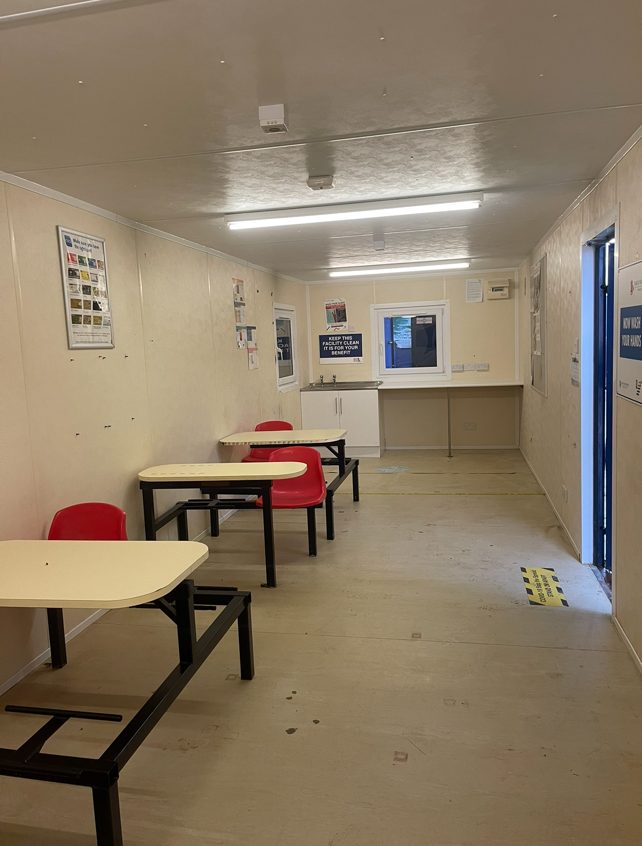
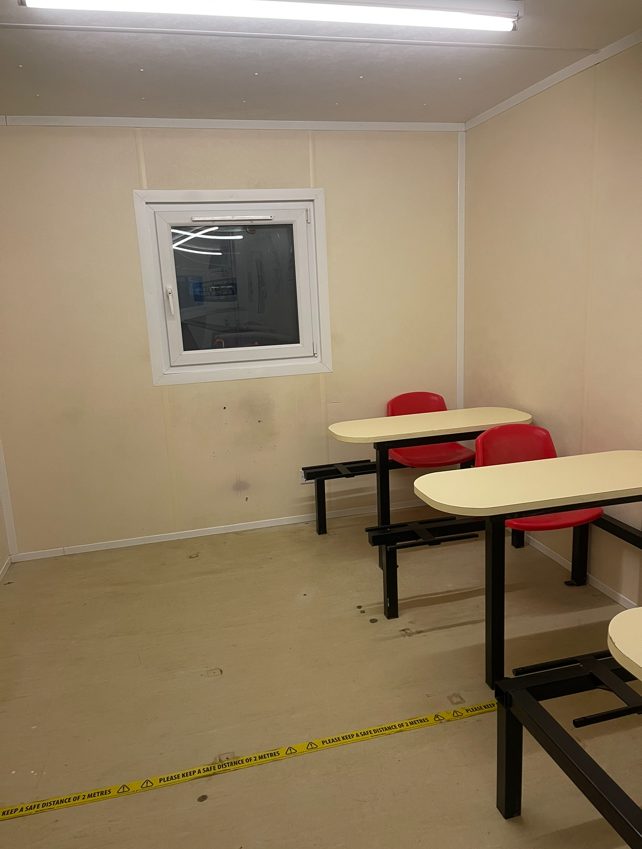
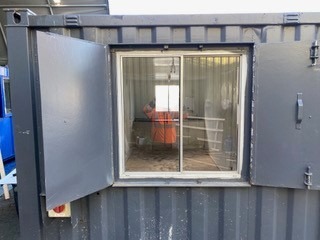
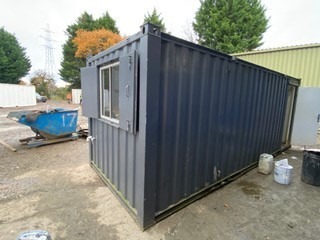
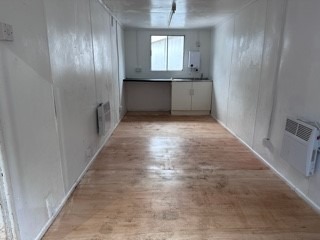
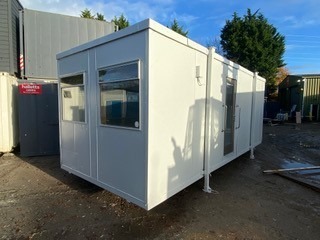
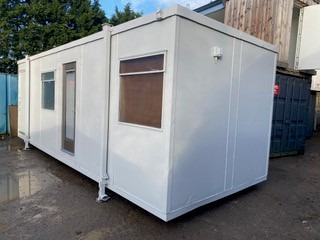
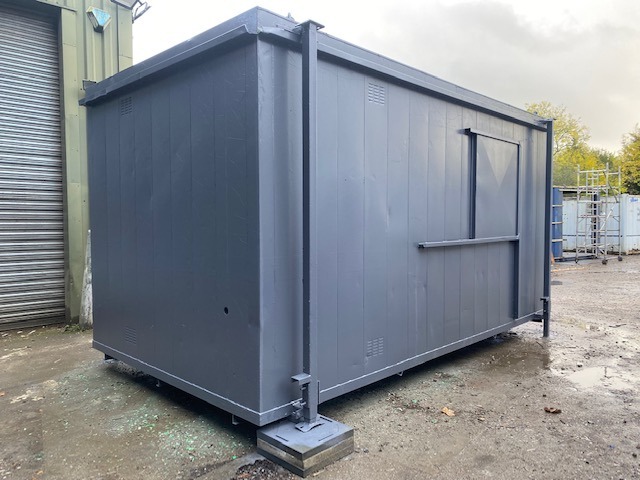
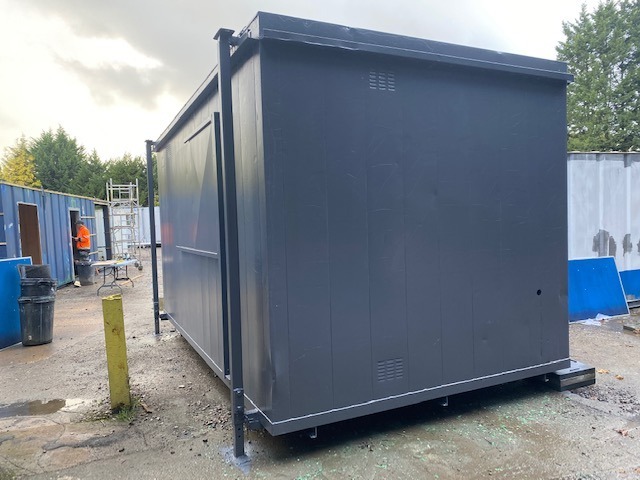
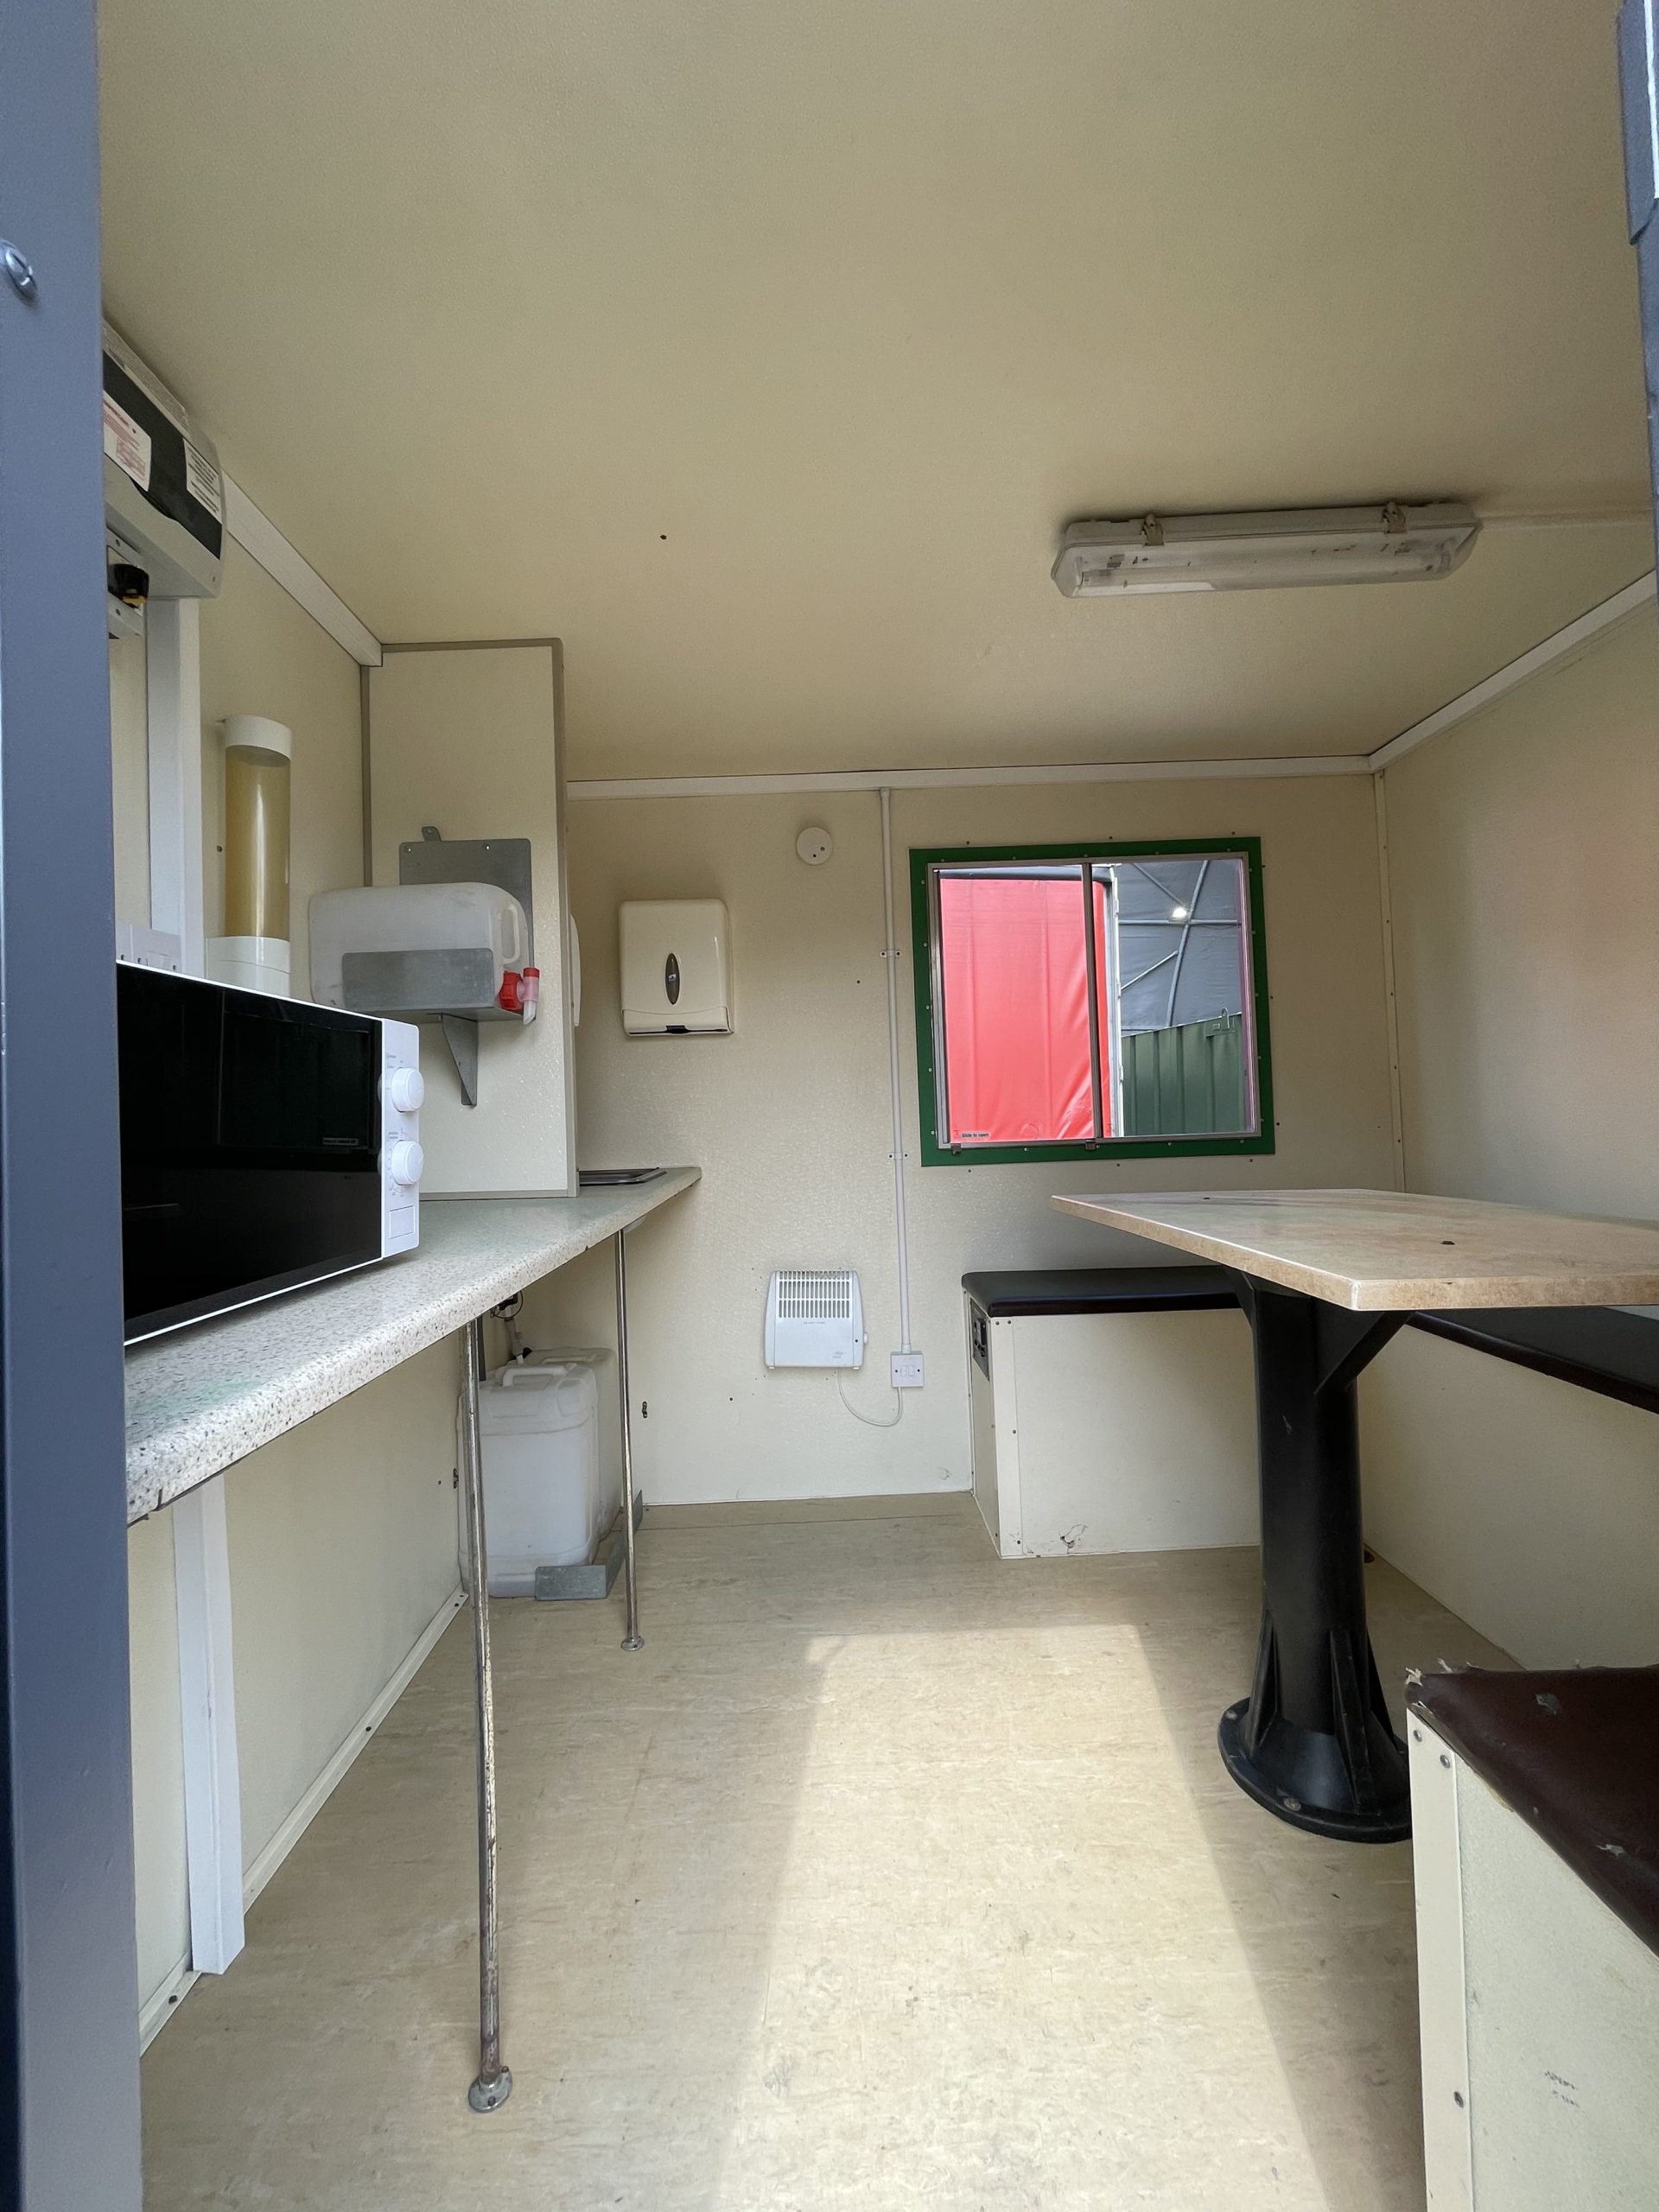
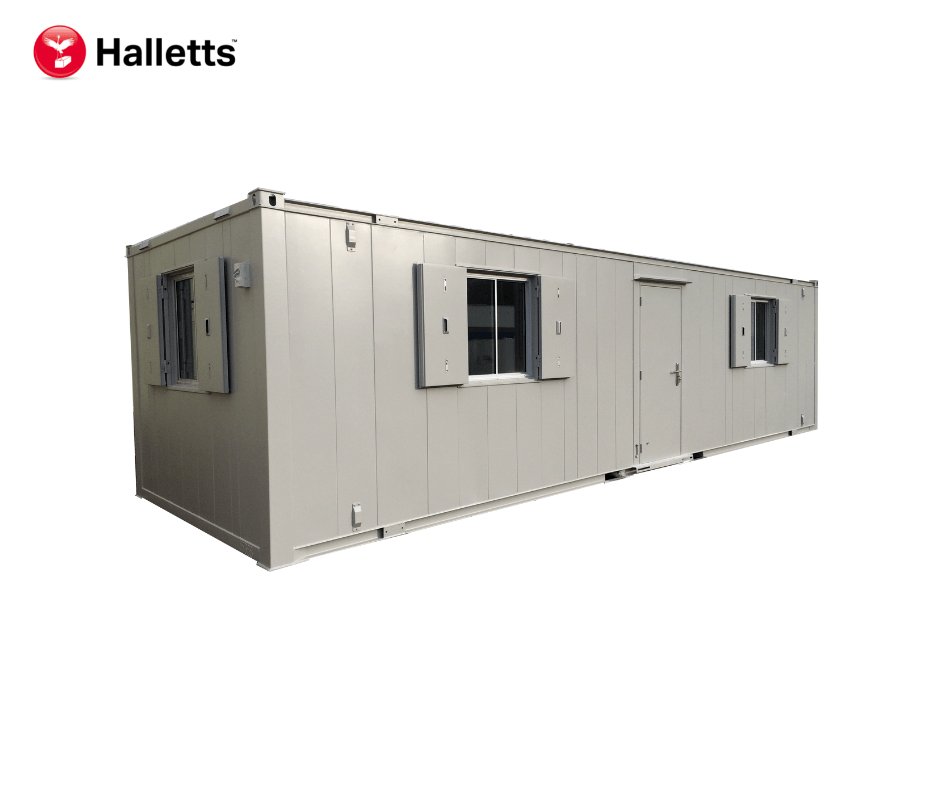
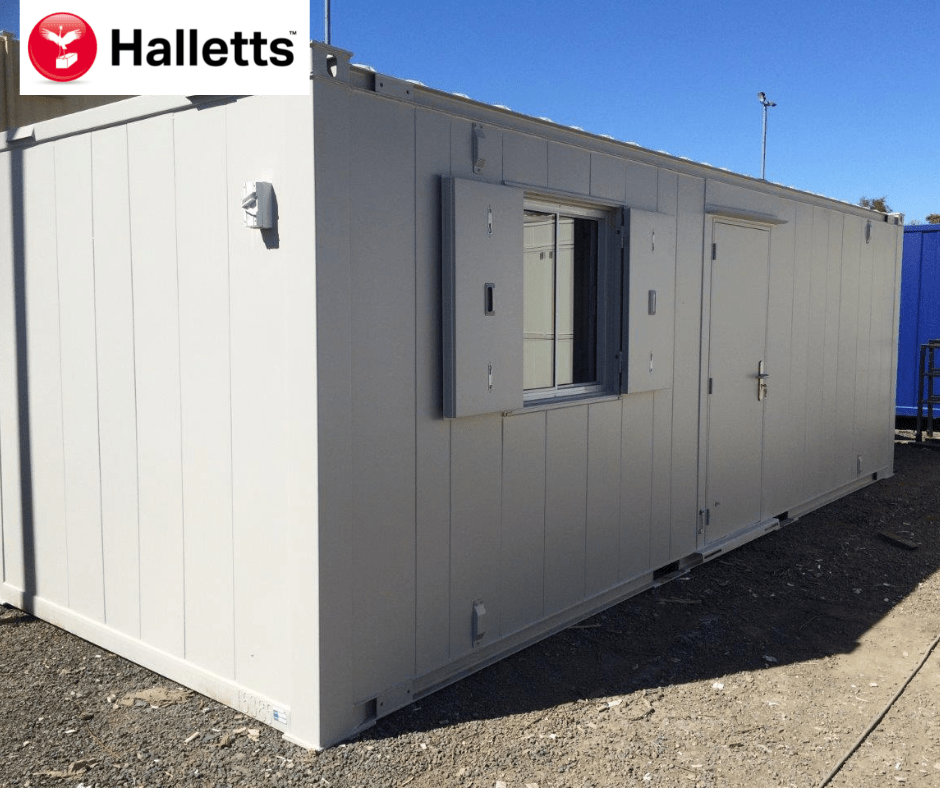
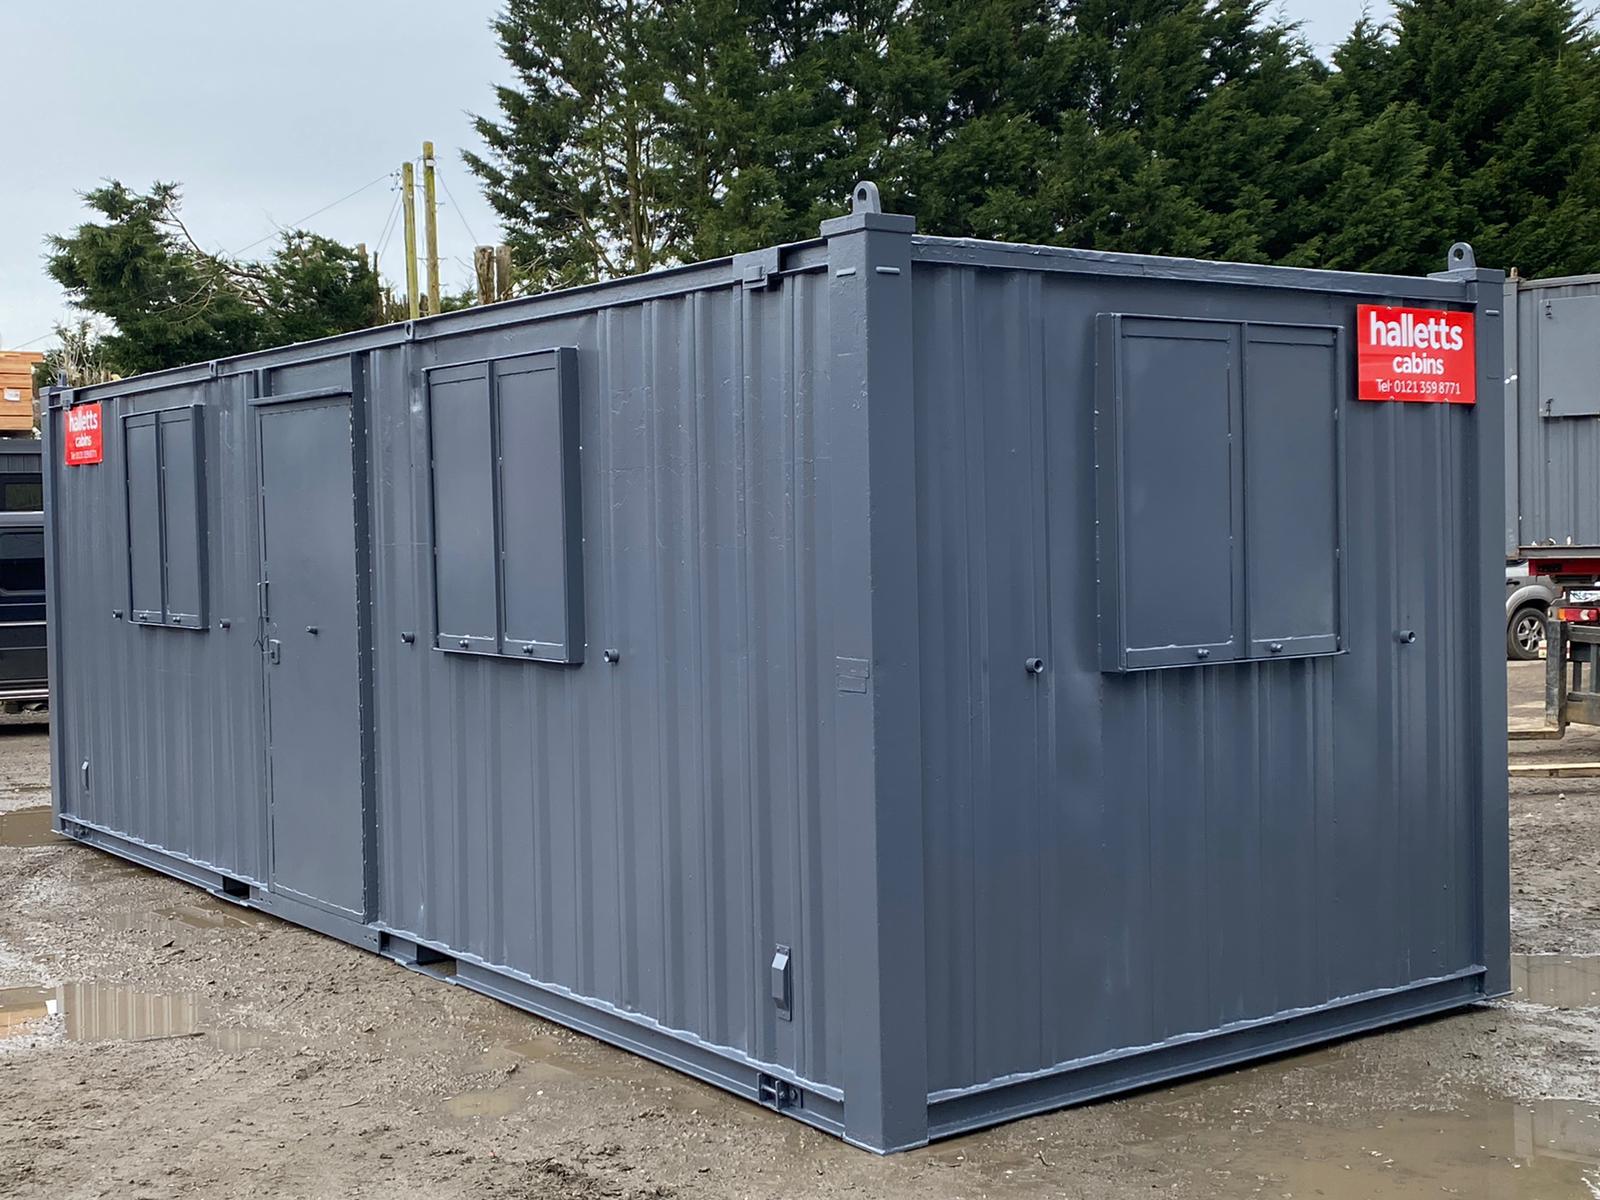
32ft x 10ft Anti Vandal Canteen/Office

  • Complete with tables and chairs
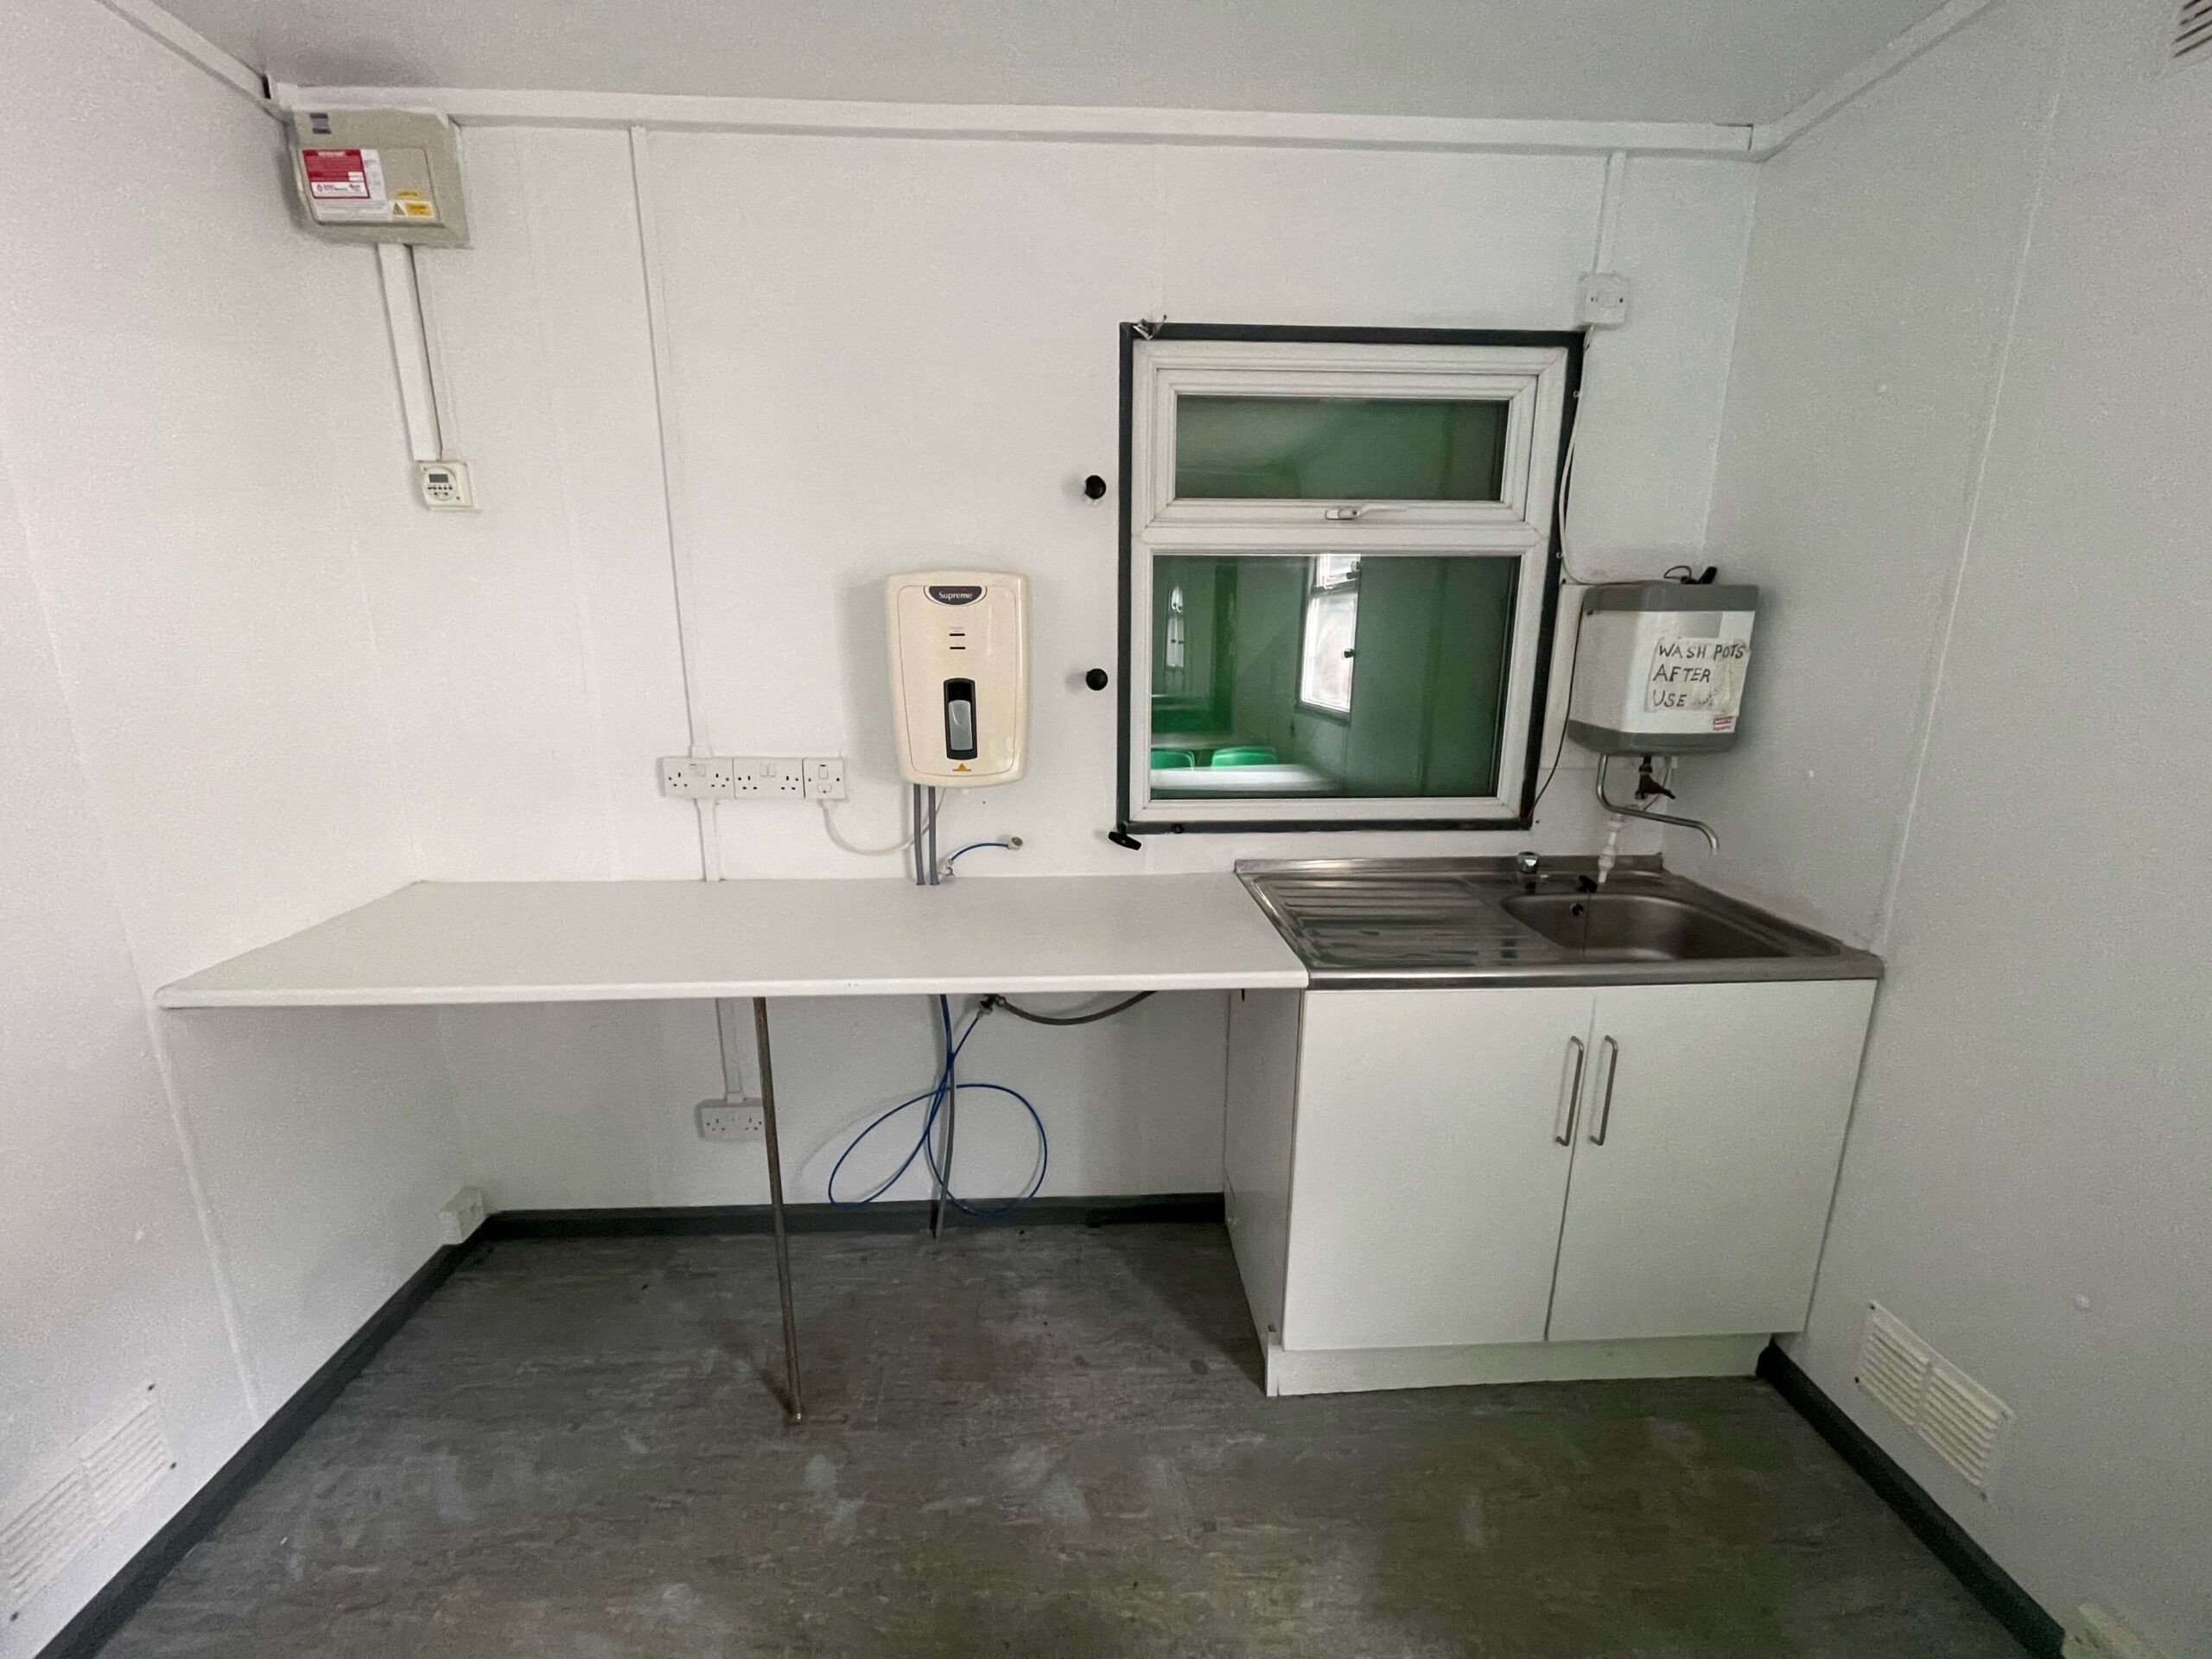
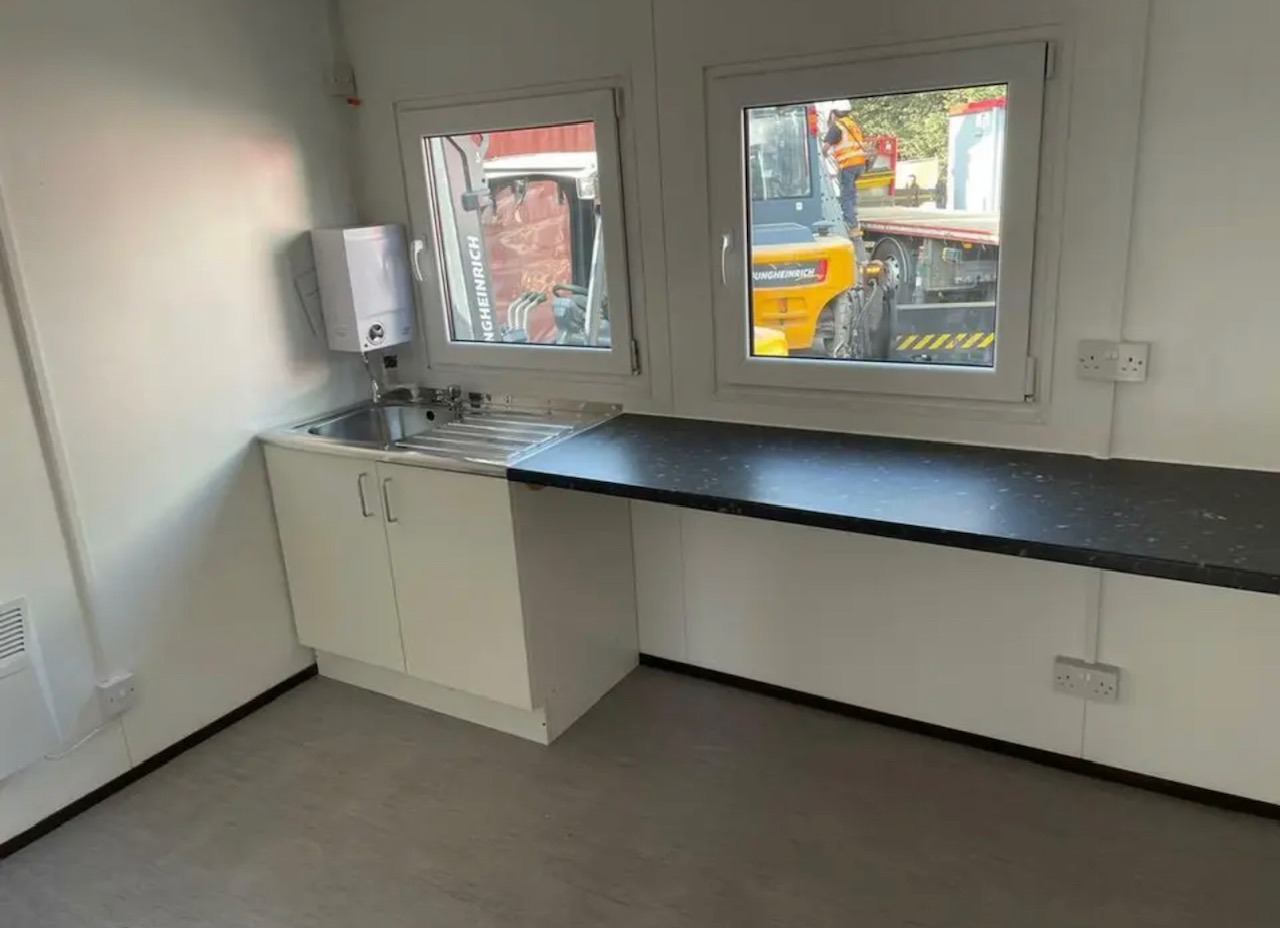
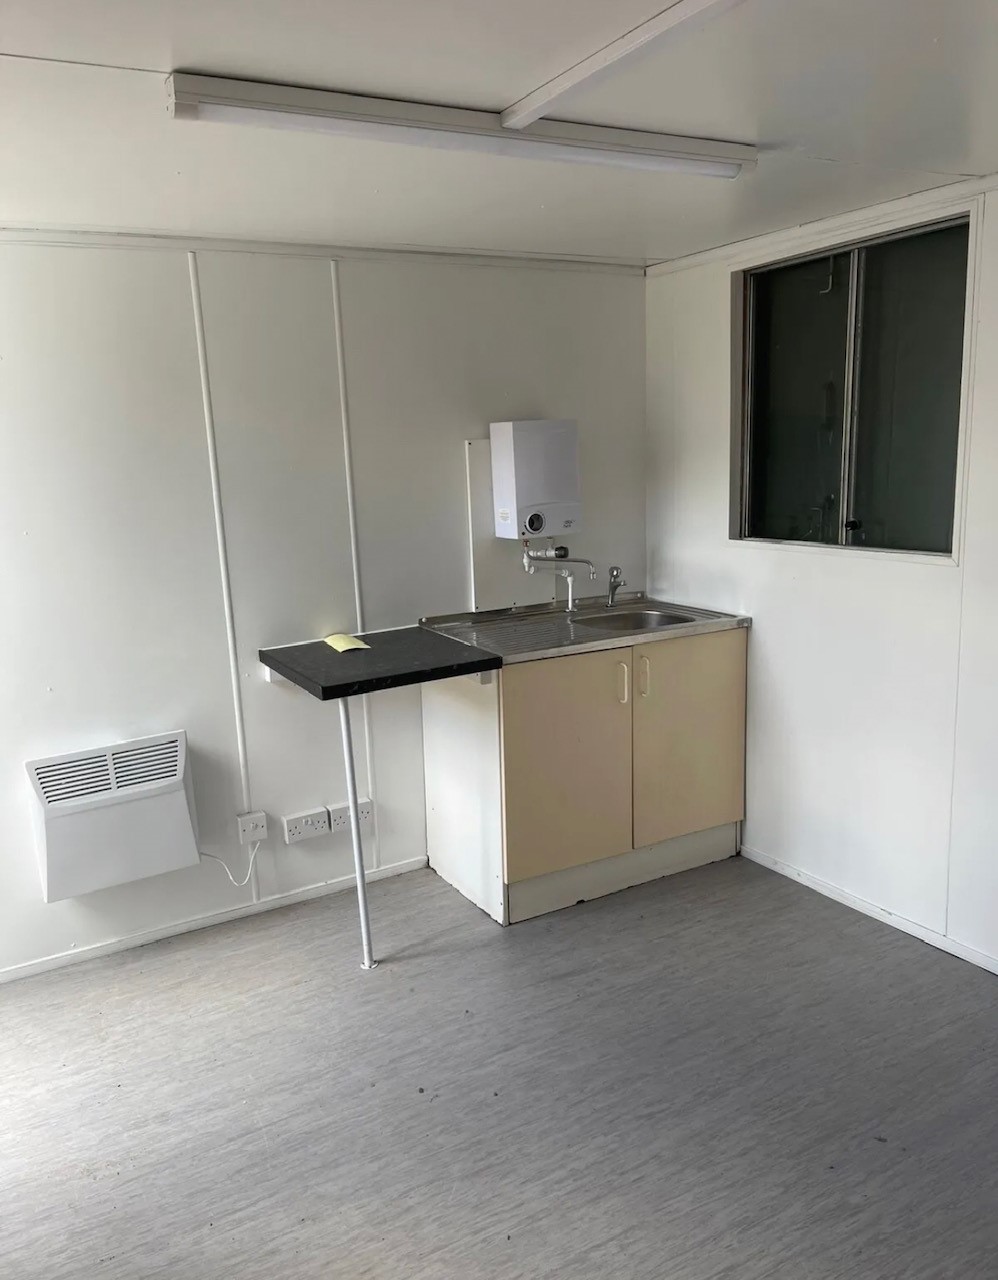
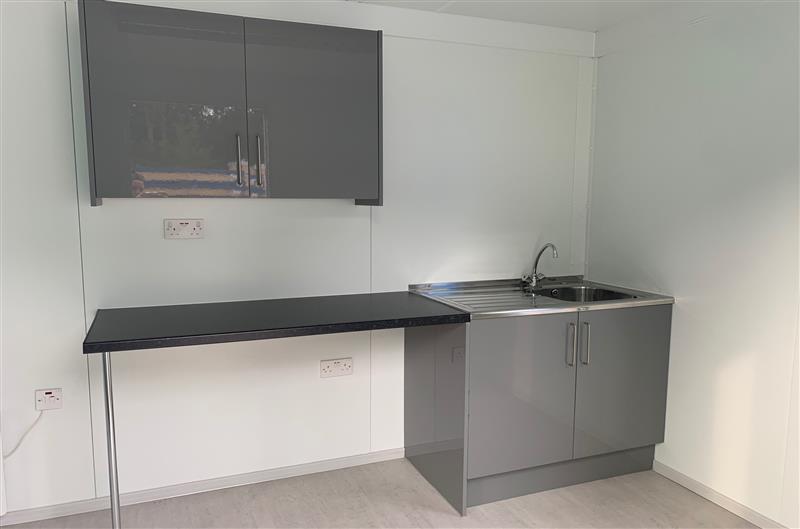
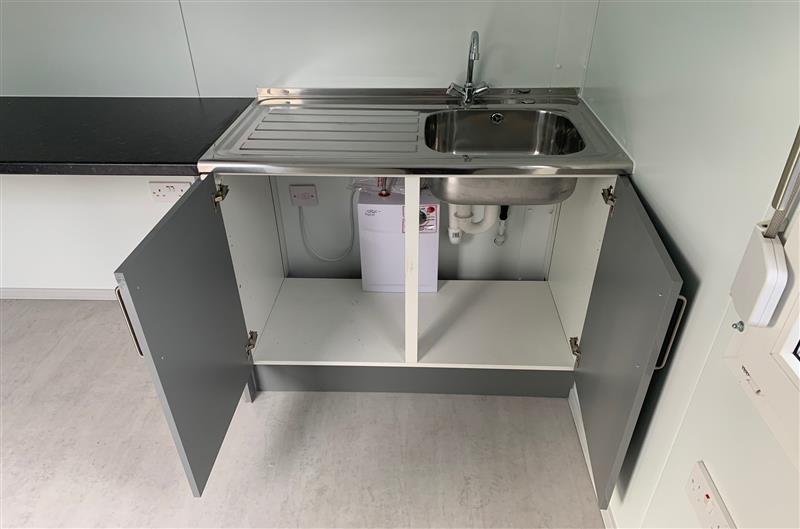
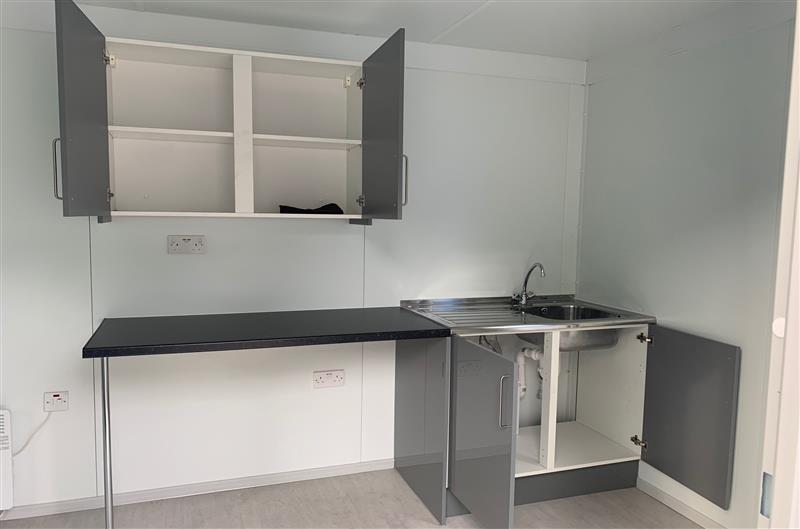
  • Kitchen with sink worktop, cupboard and water heater
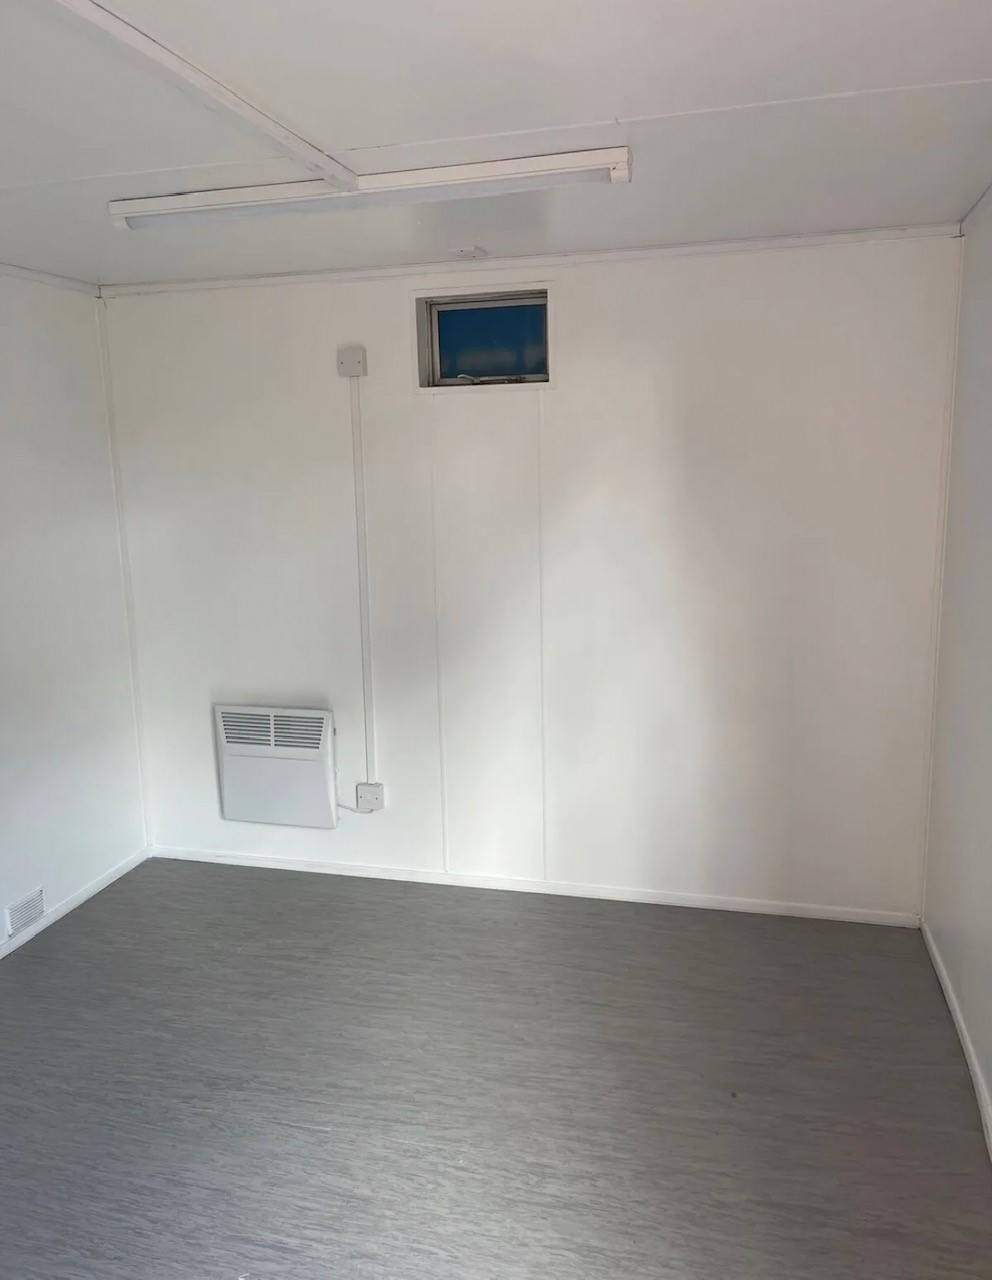
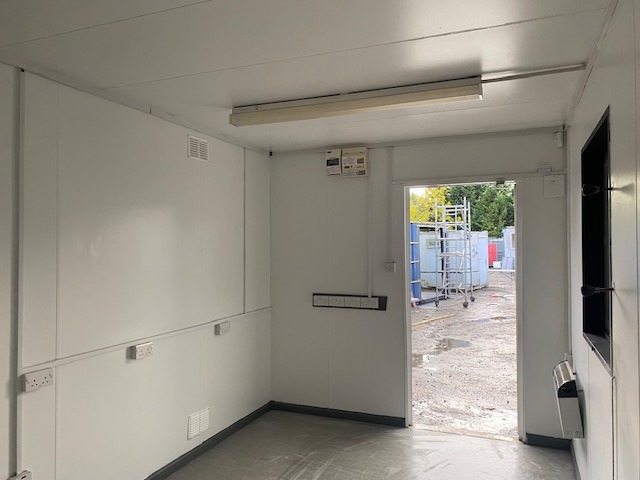
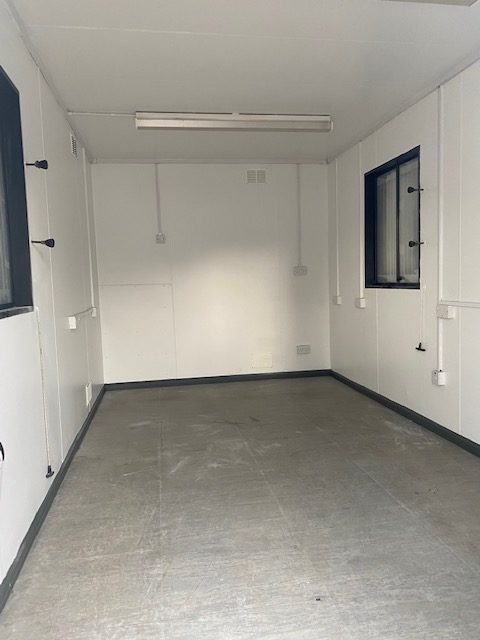
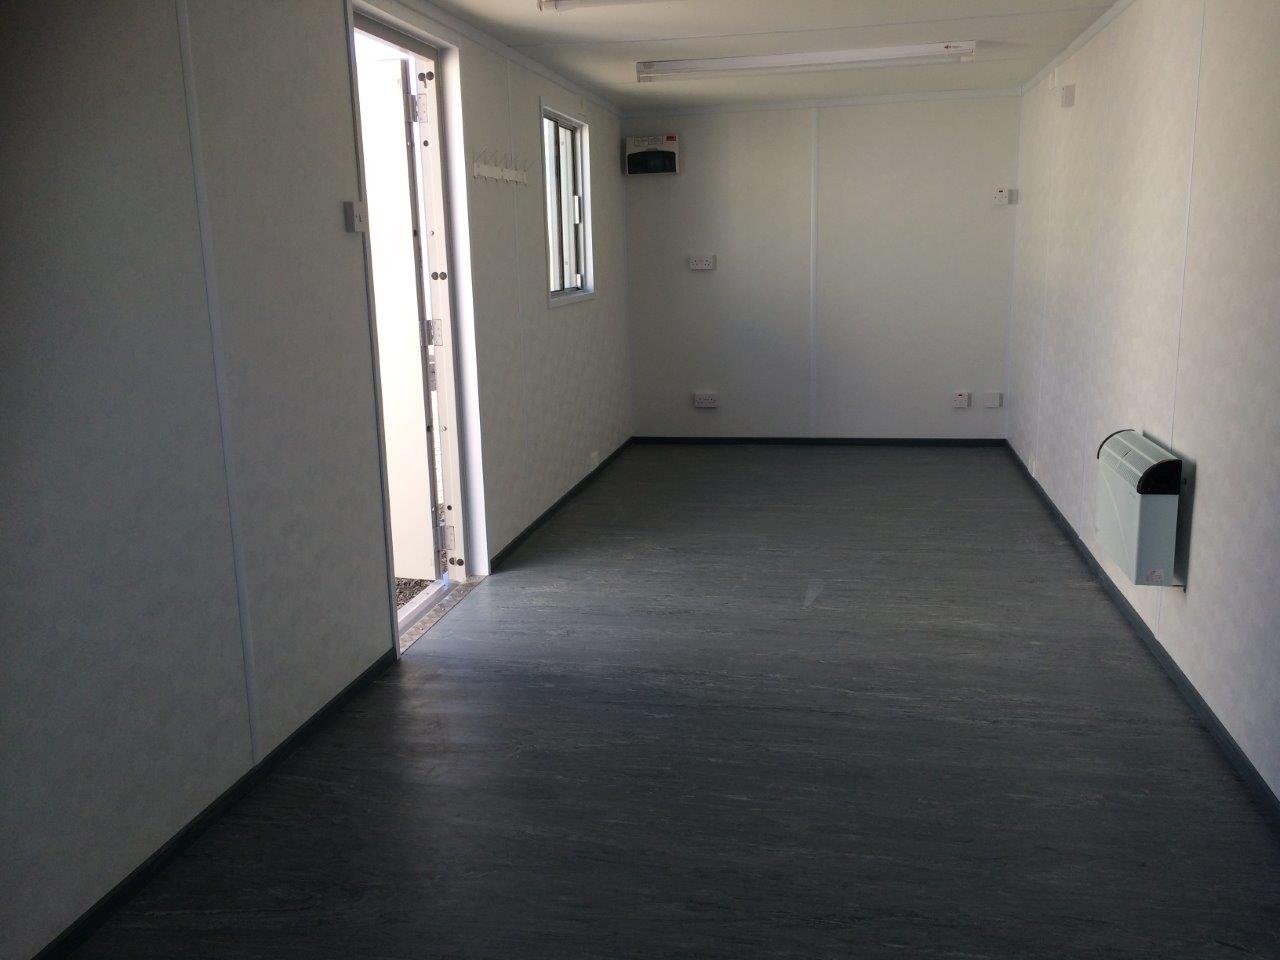
  • Insulated with electric sockets, lighting and heating
  • White upvc double glazing
  • External re spray in dark grey

Location: Nationwide

£6,500 + vat

Not Available for Hire

We can deliver for a cost please ask and send us post code.

Call for an instant quote!

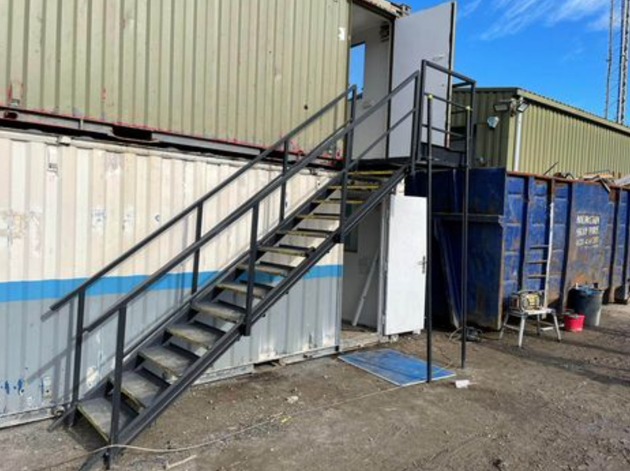
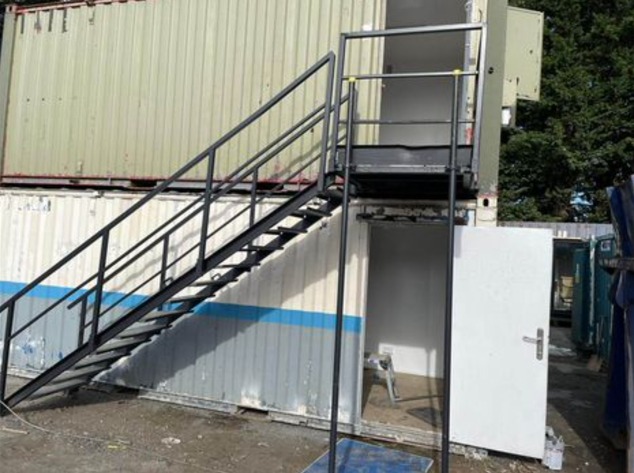
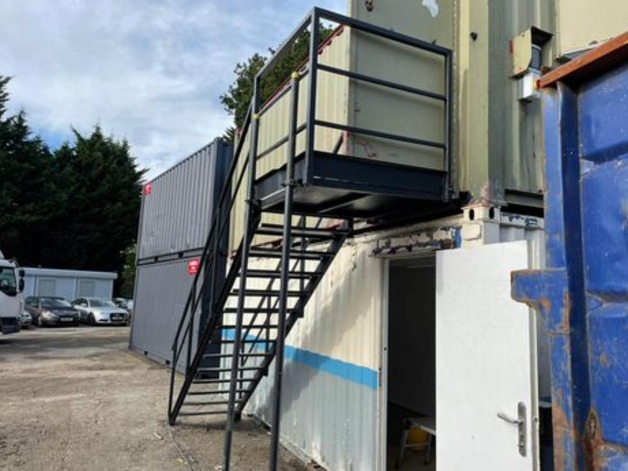
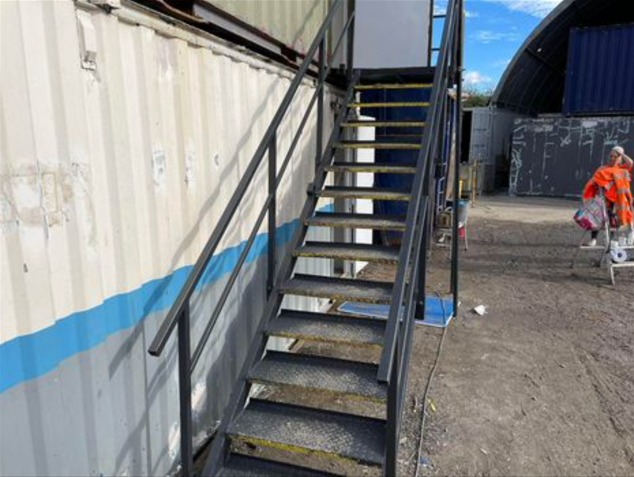
Steel Cabin Staircases, in various sizes

  • 13 tread

  • 14 tread

  • 15 tread

Location: Nationwide

£1,200.00 + vat

Not Available for Hire

Call for an instant quote!

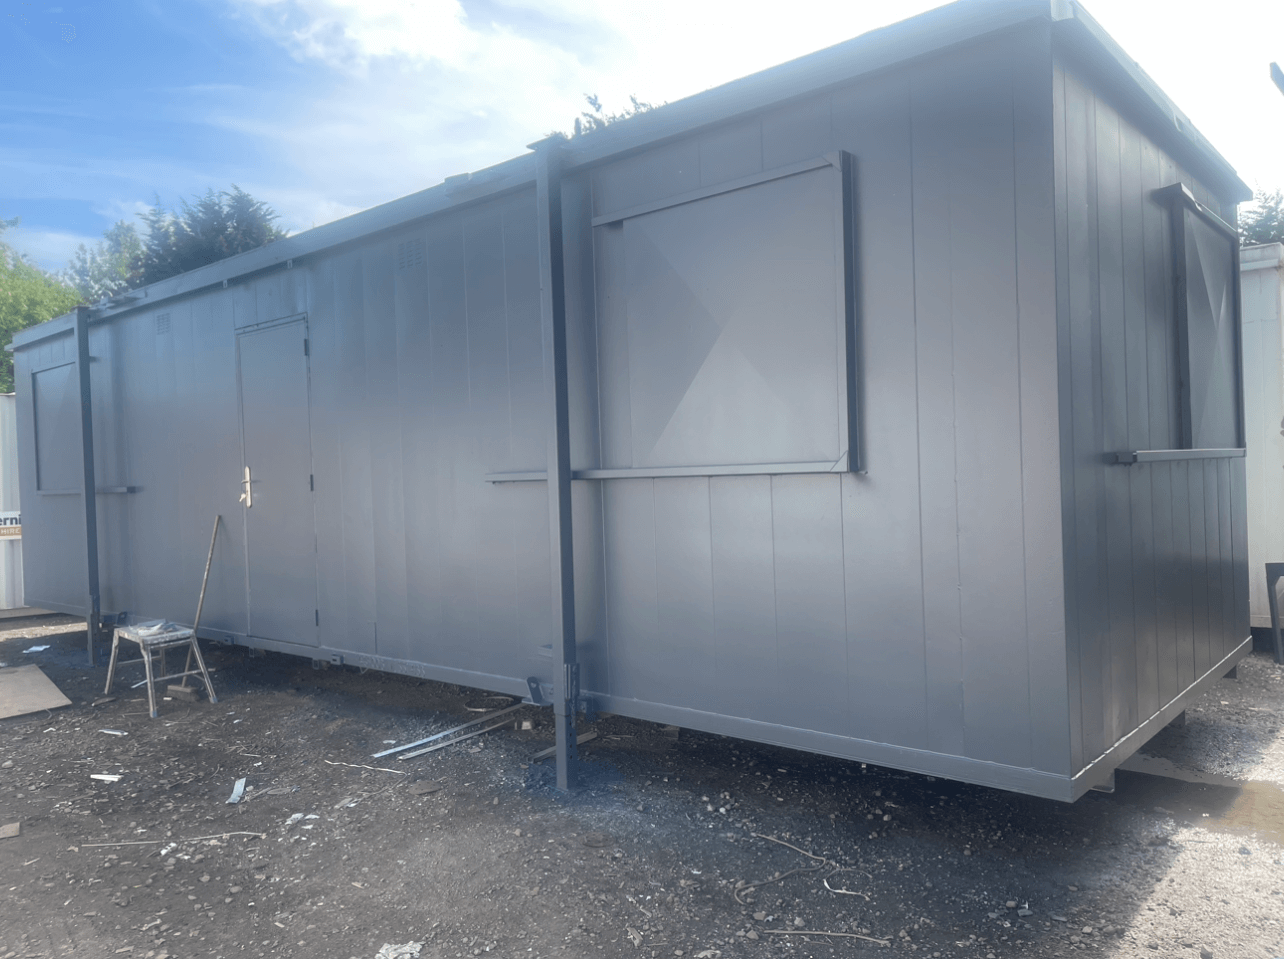
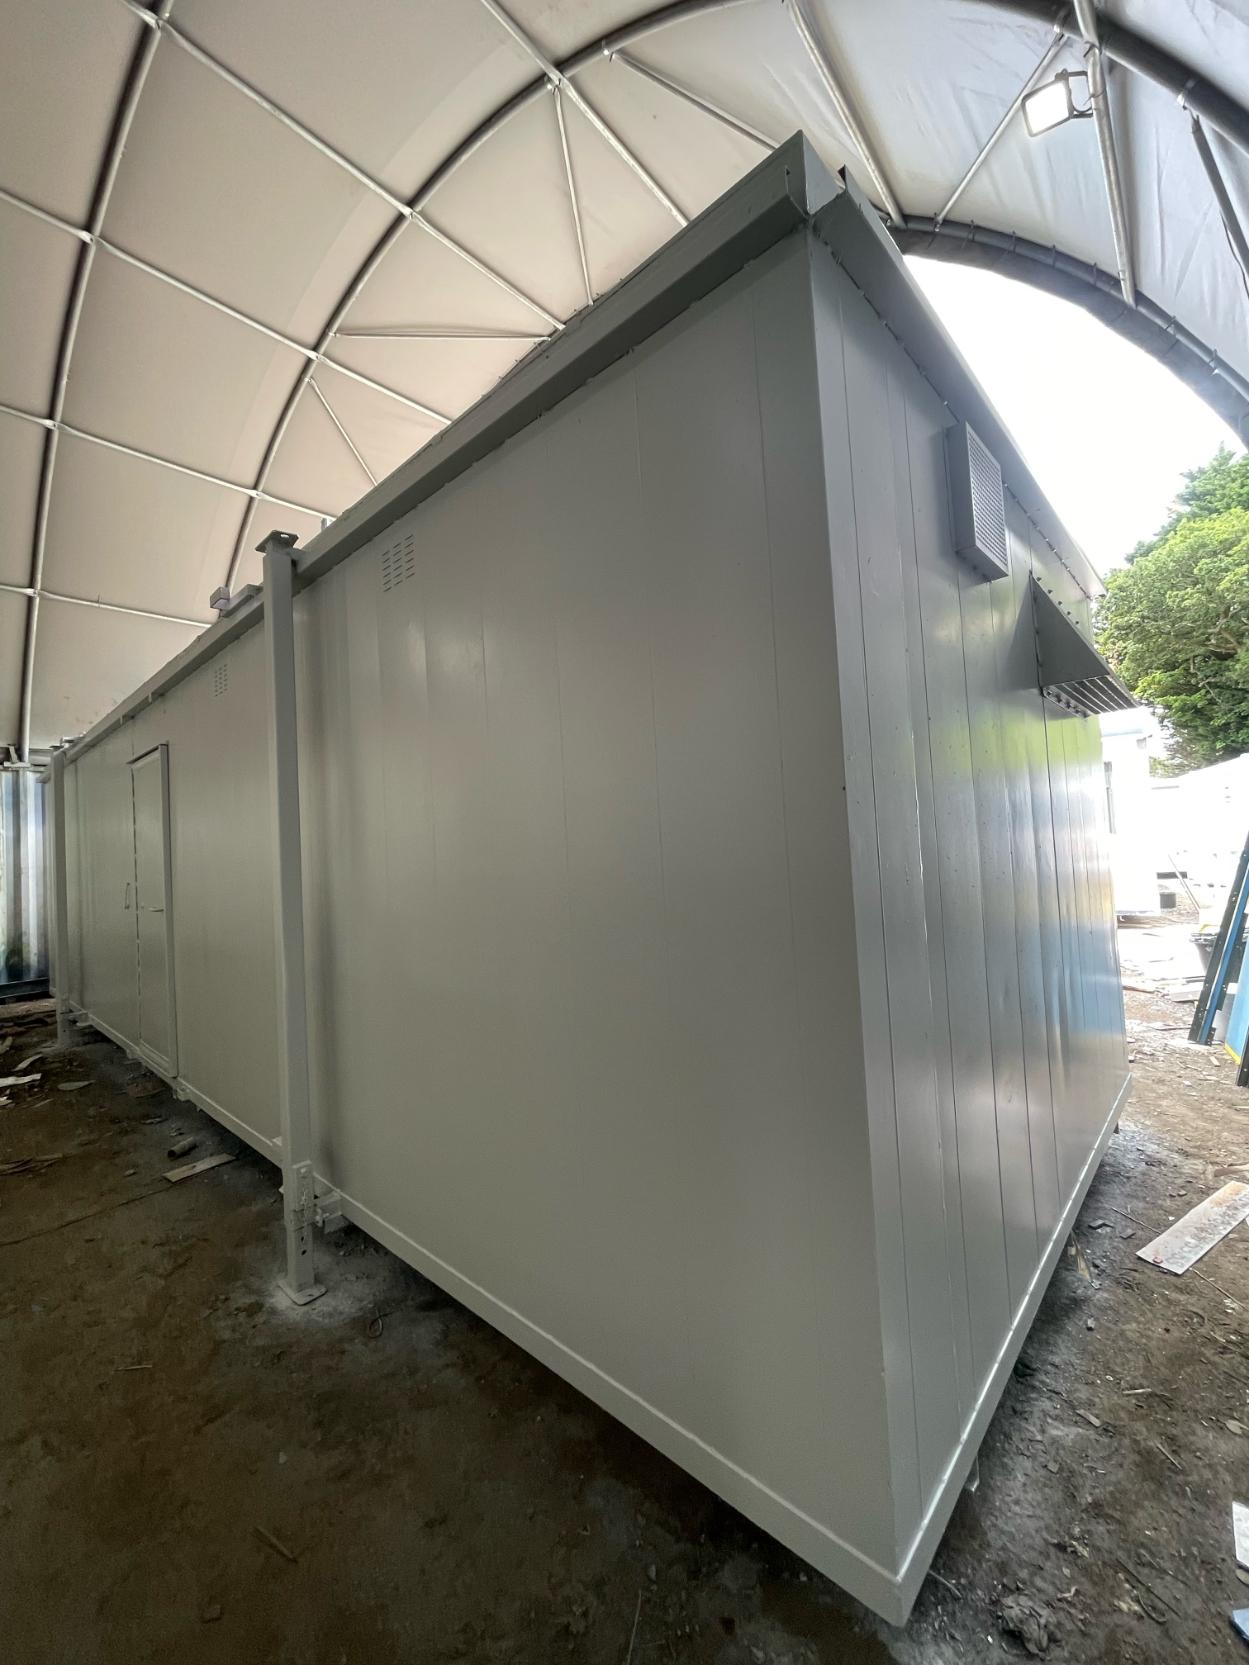
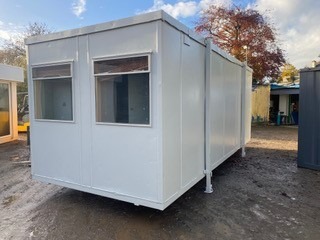
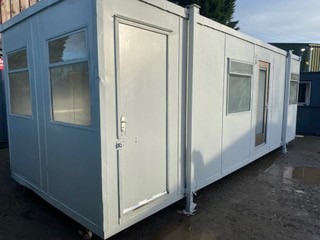
32ft x 10ft Anti Vandal Canteen/Office

    • Price: £5,995 + VAT
    • Description: 32ft x 10ft Anti Vandal Canteen/Office
  Part refurbished including:
  • Electric sockets, lighting and heating
  • White upvc double glazing
  • Canteen
  • Open plan
  • External light grey re spray

Location: Nationwide

£5,995 + vat

Not Available for Hire

We can deliver for a cost please ask and send us post code.

Call for an instant quote!

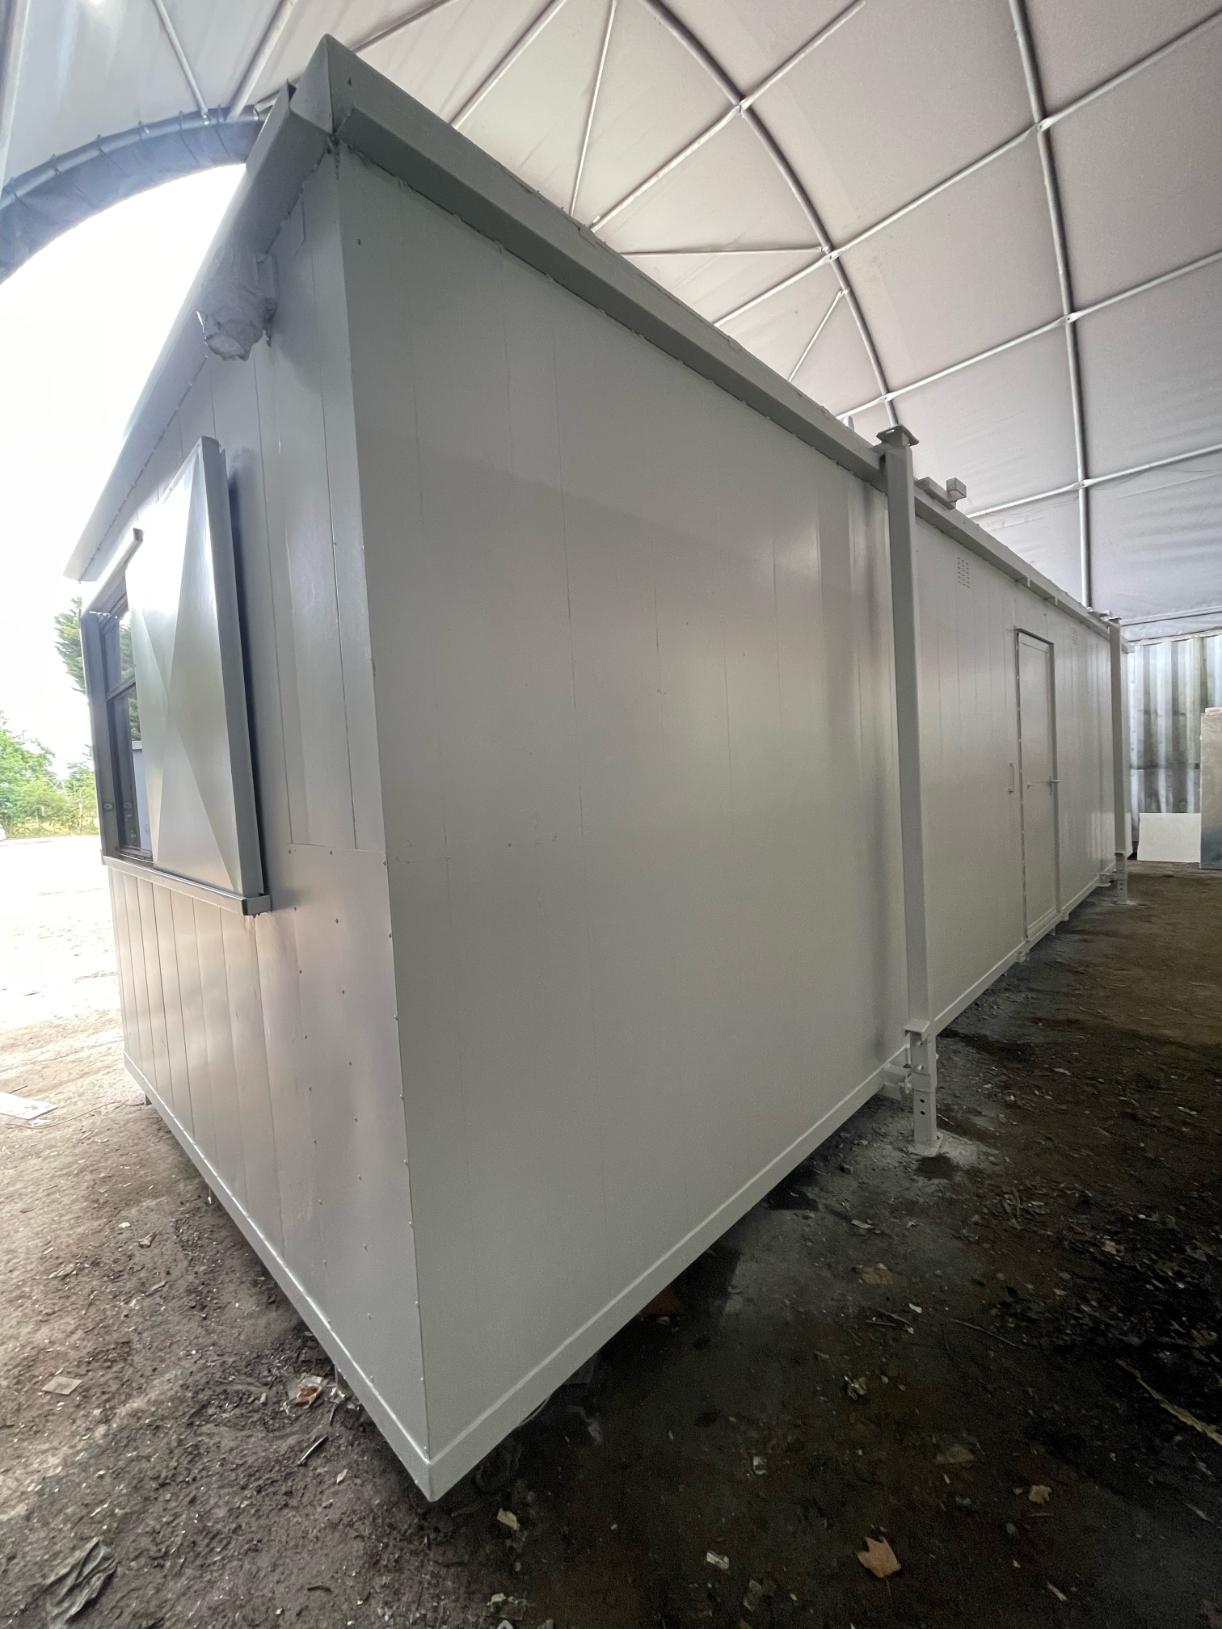
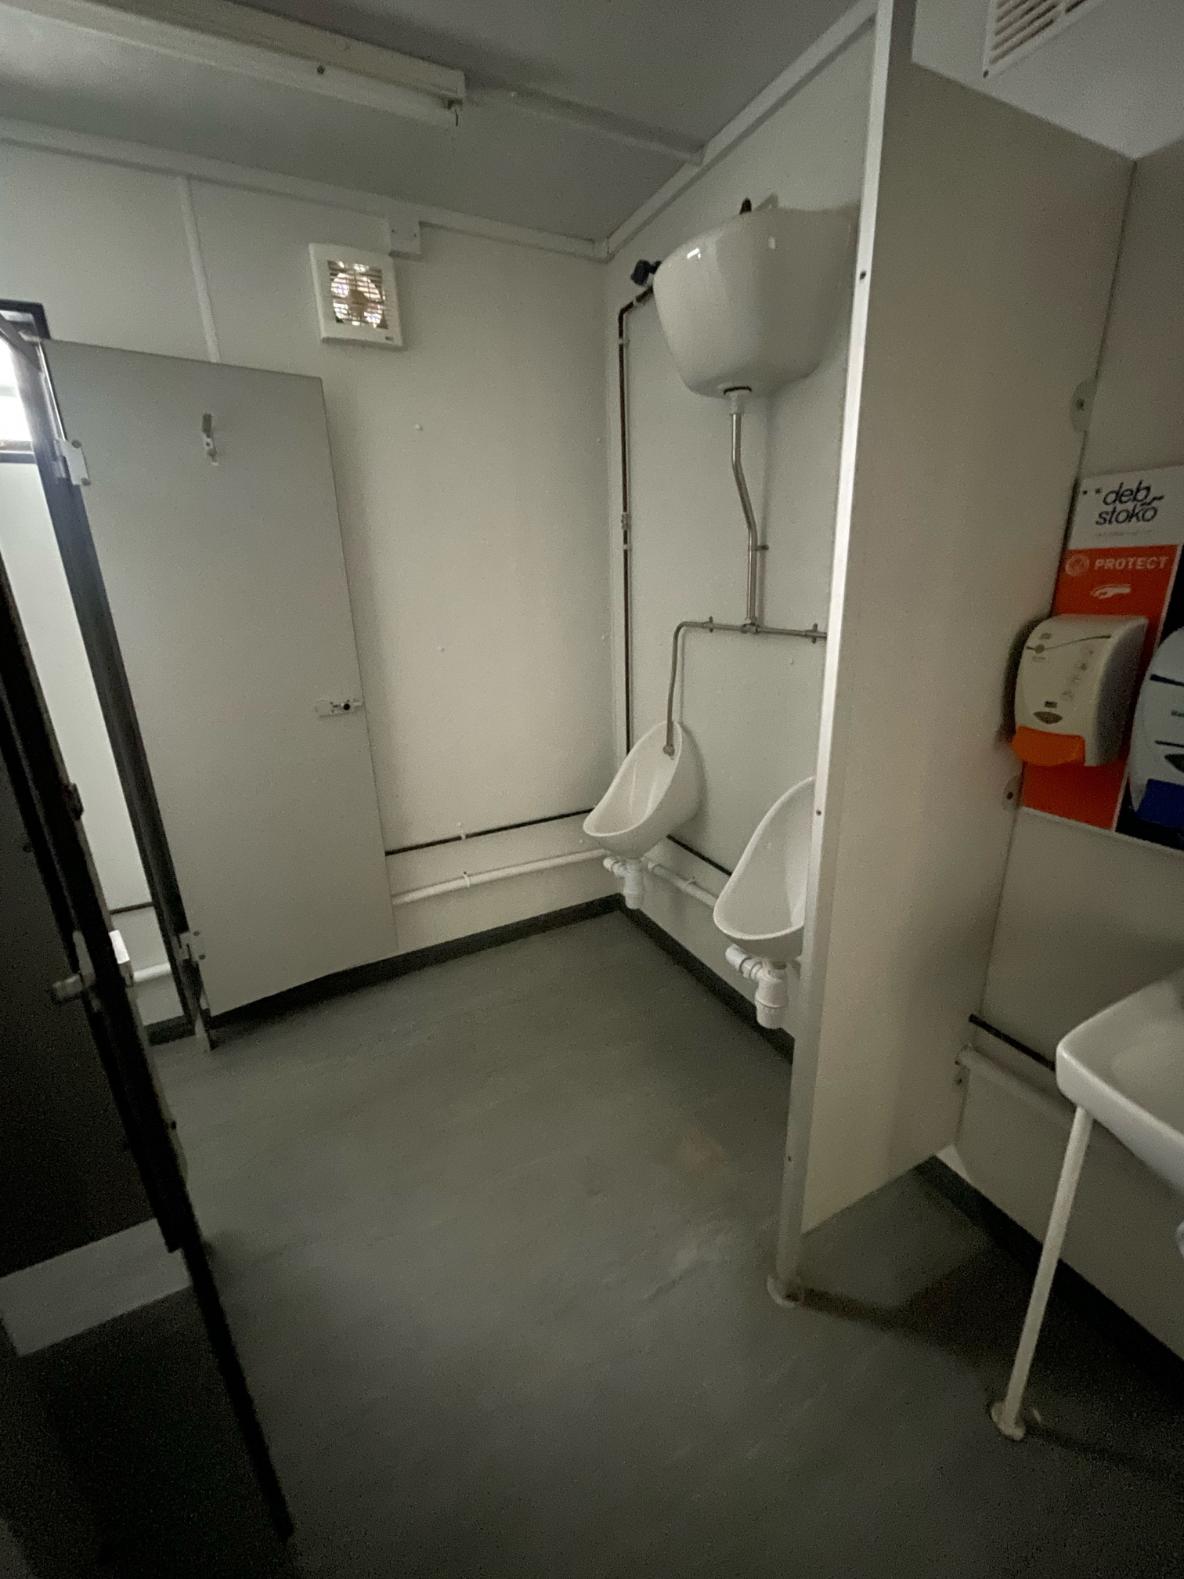
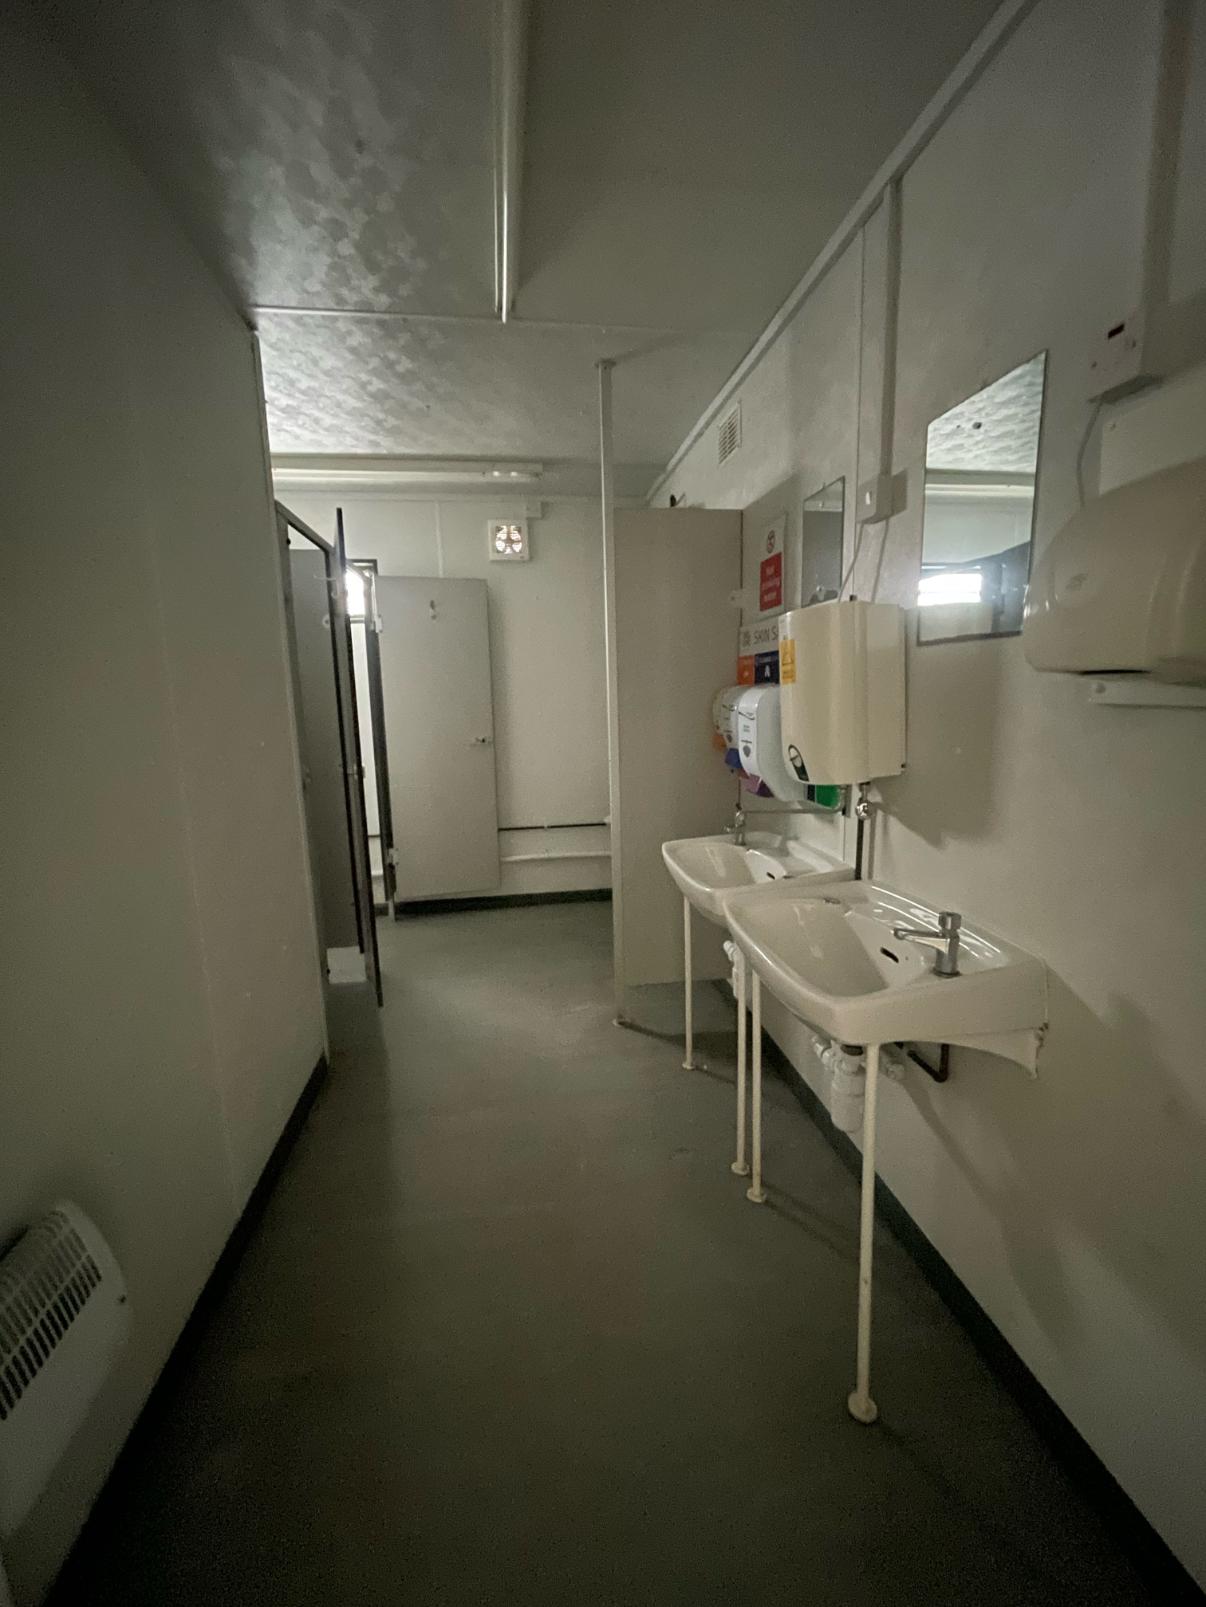
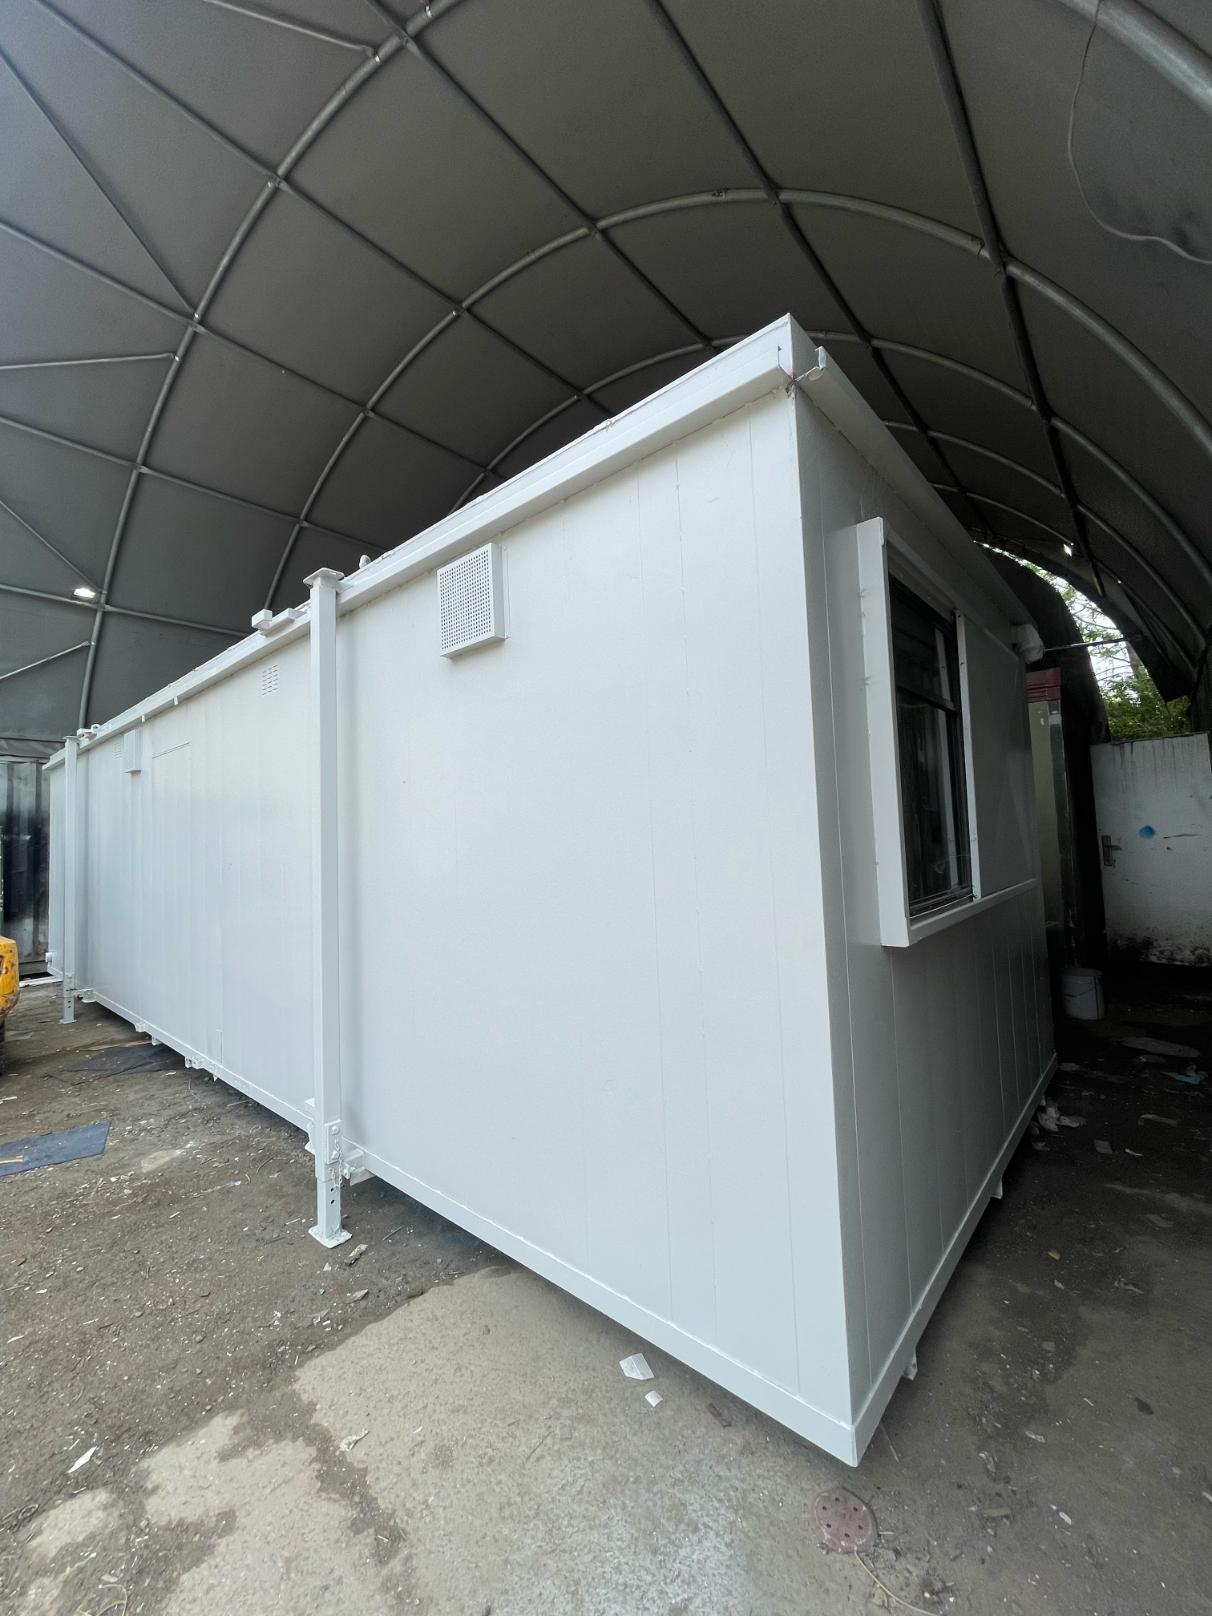
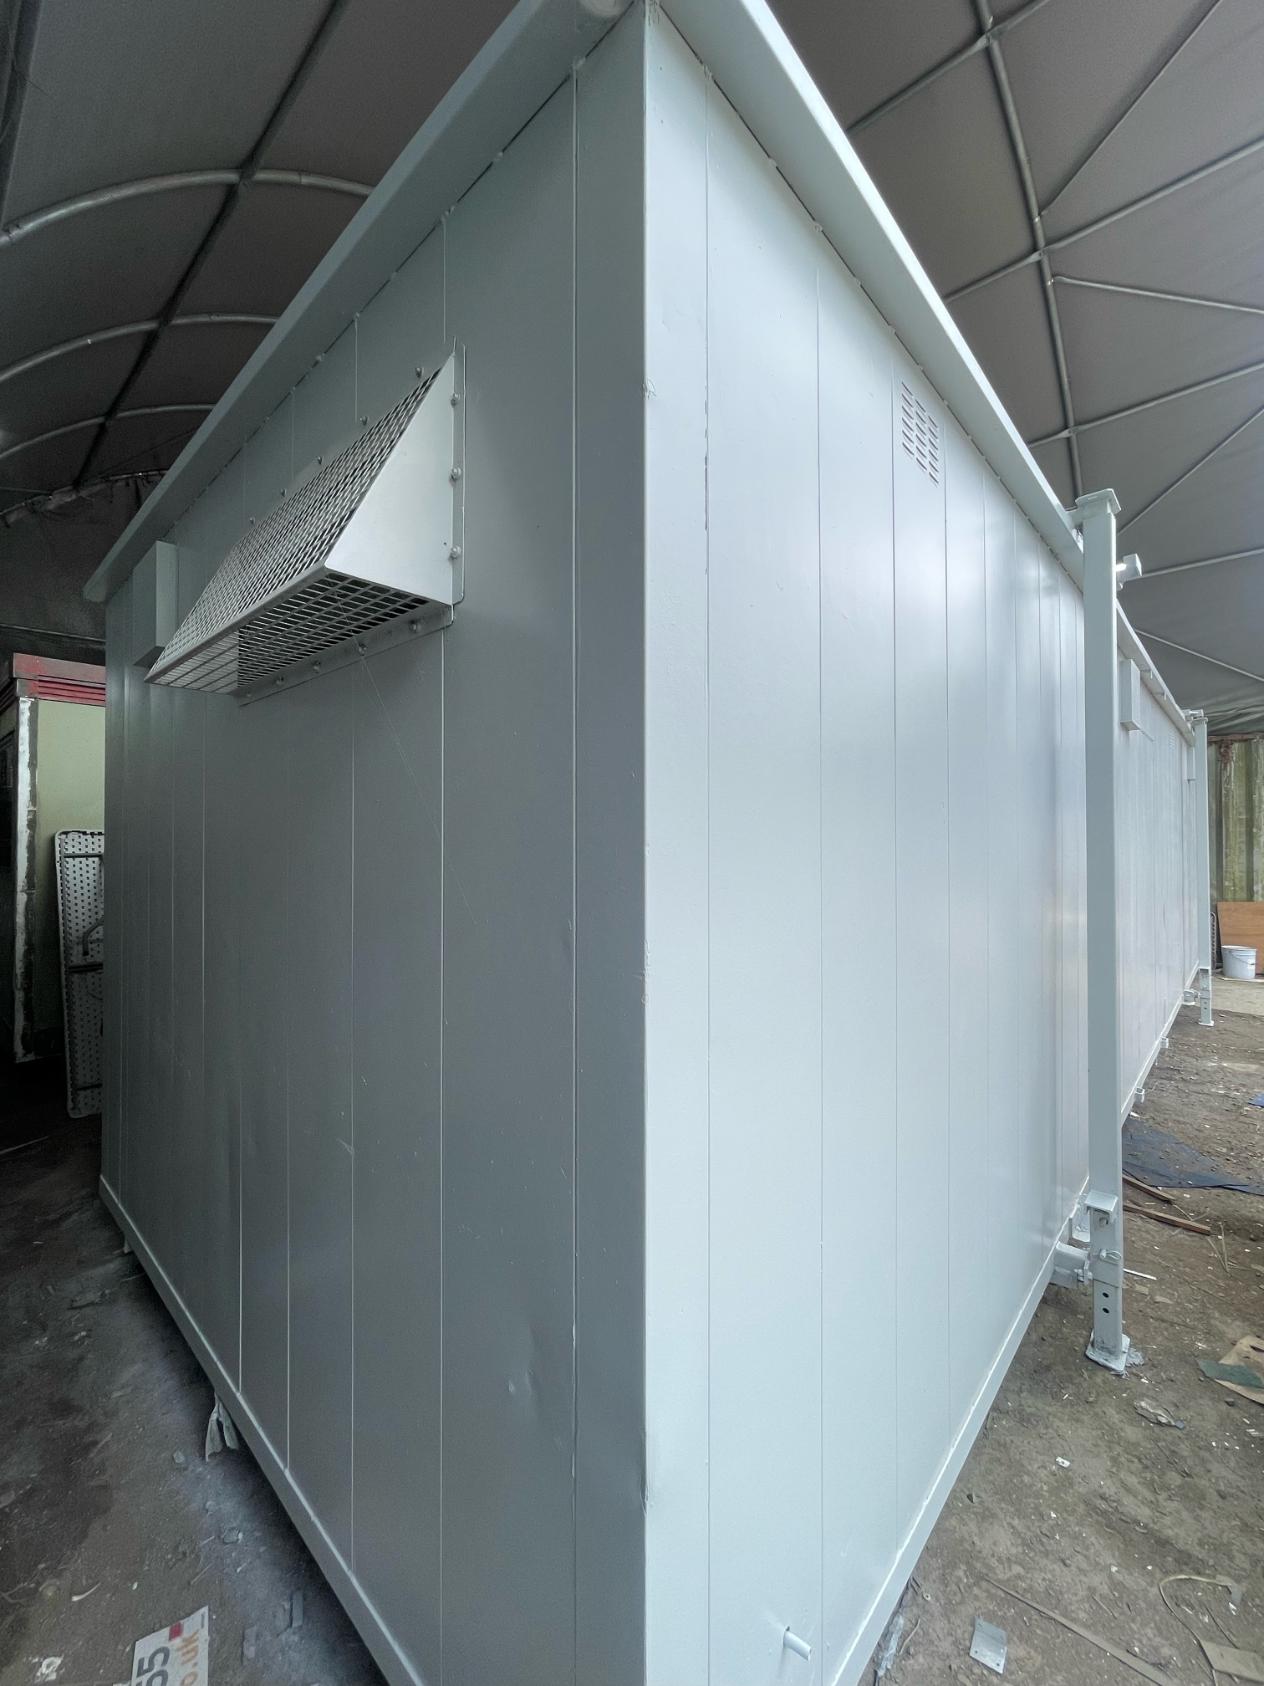
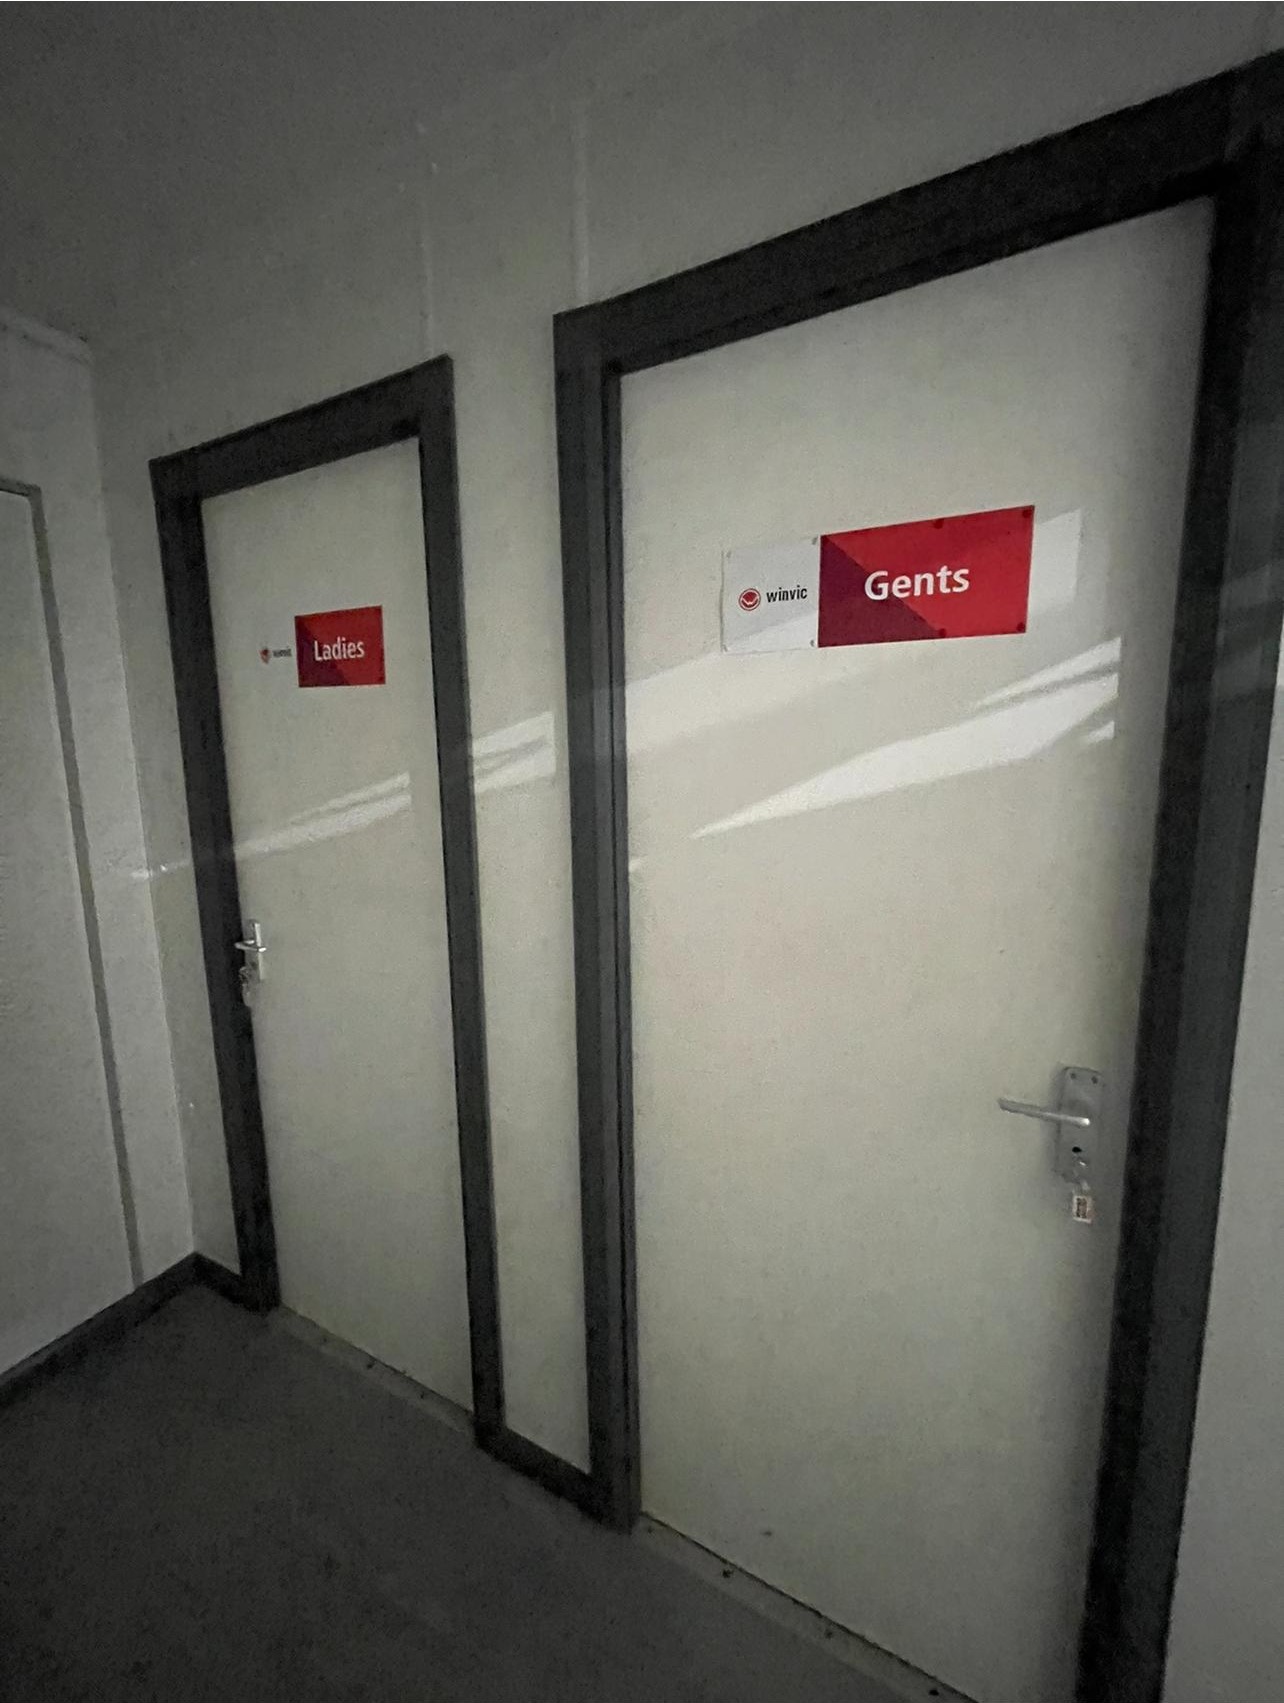
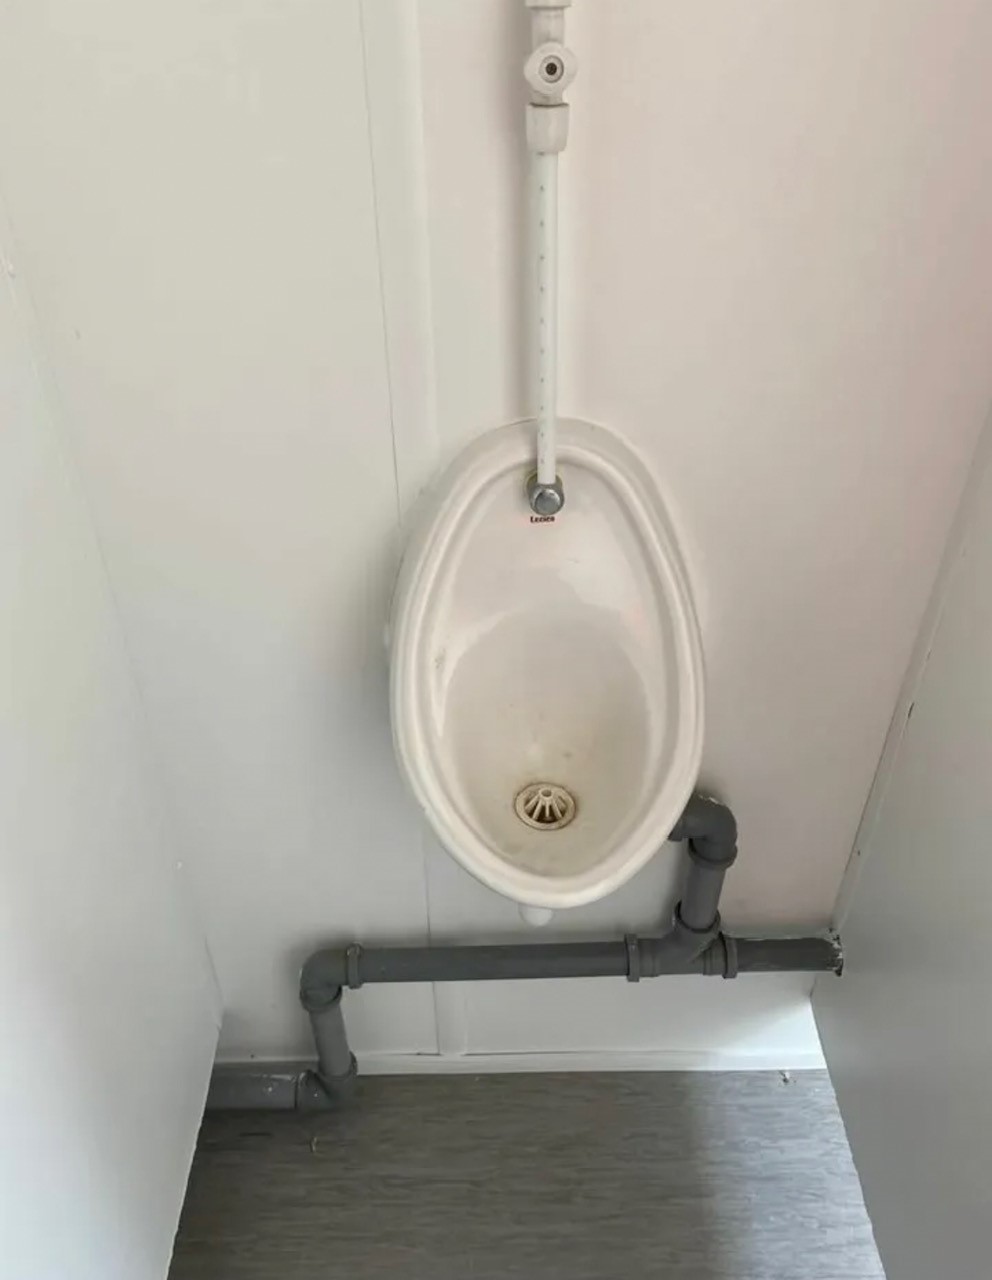
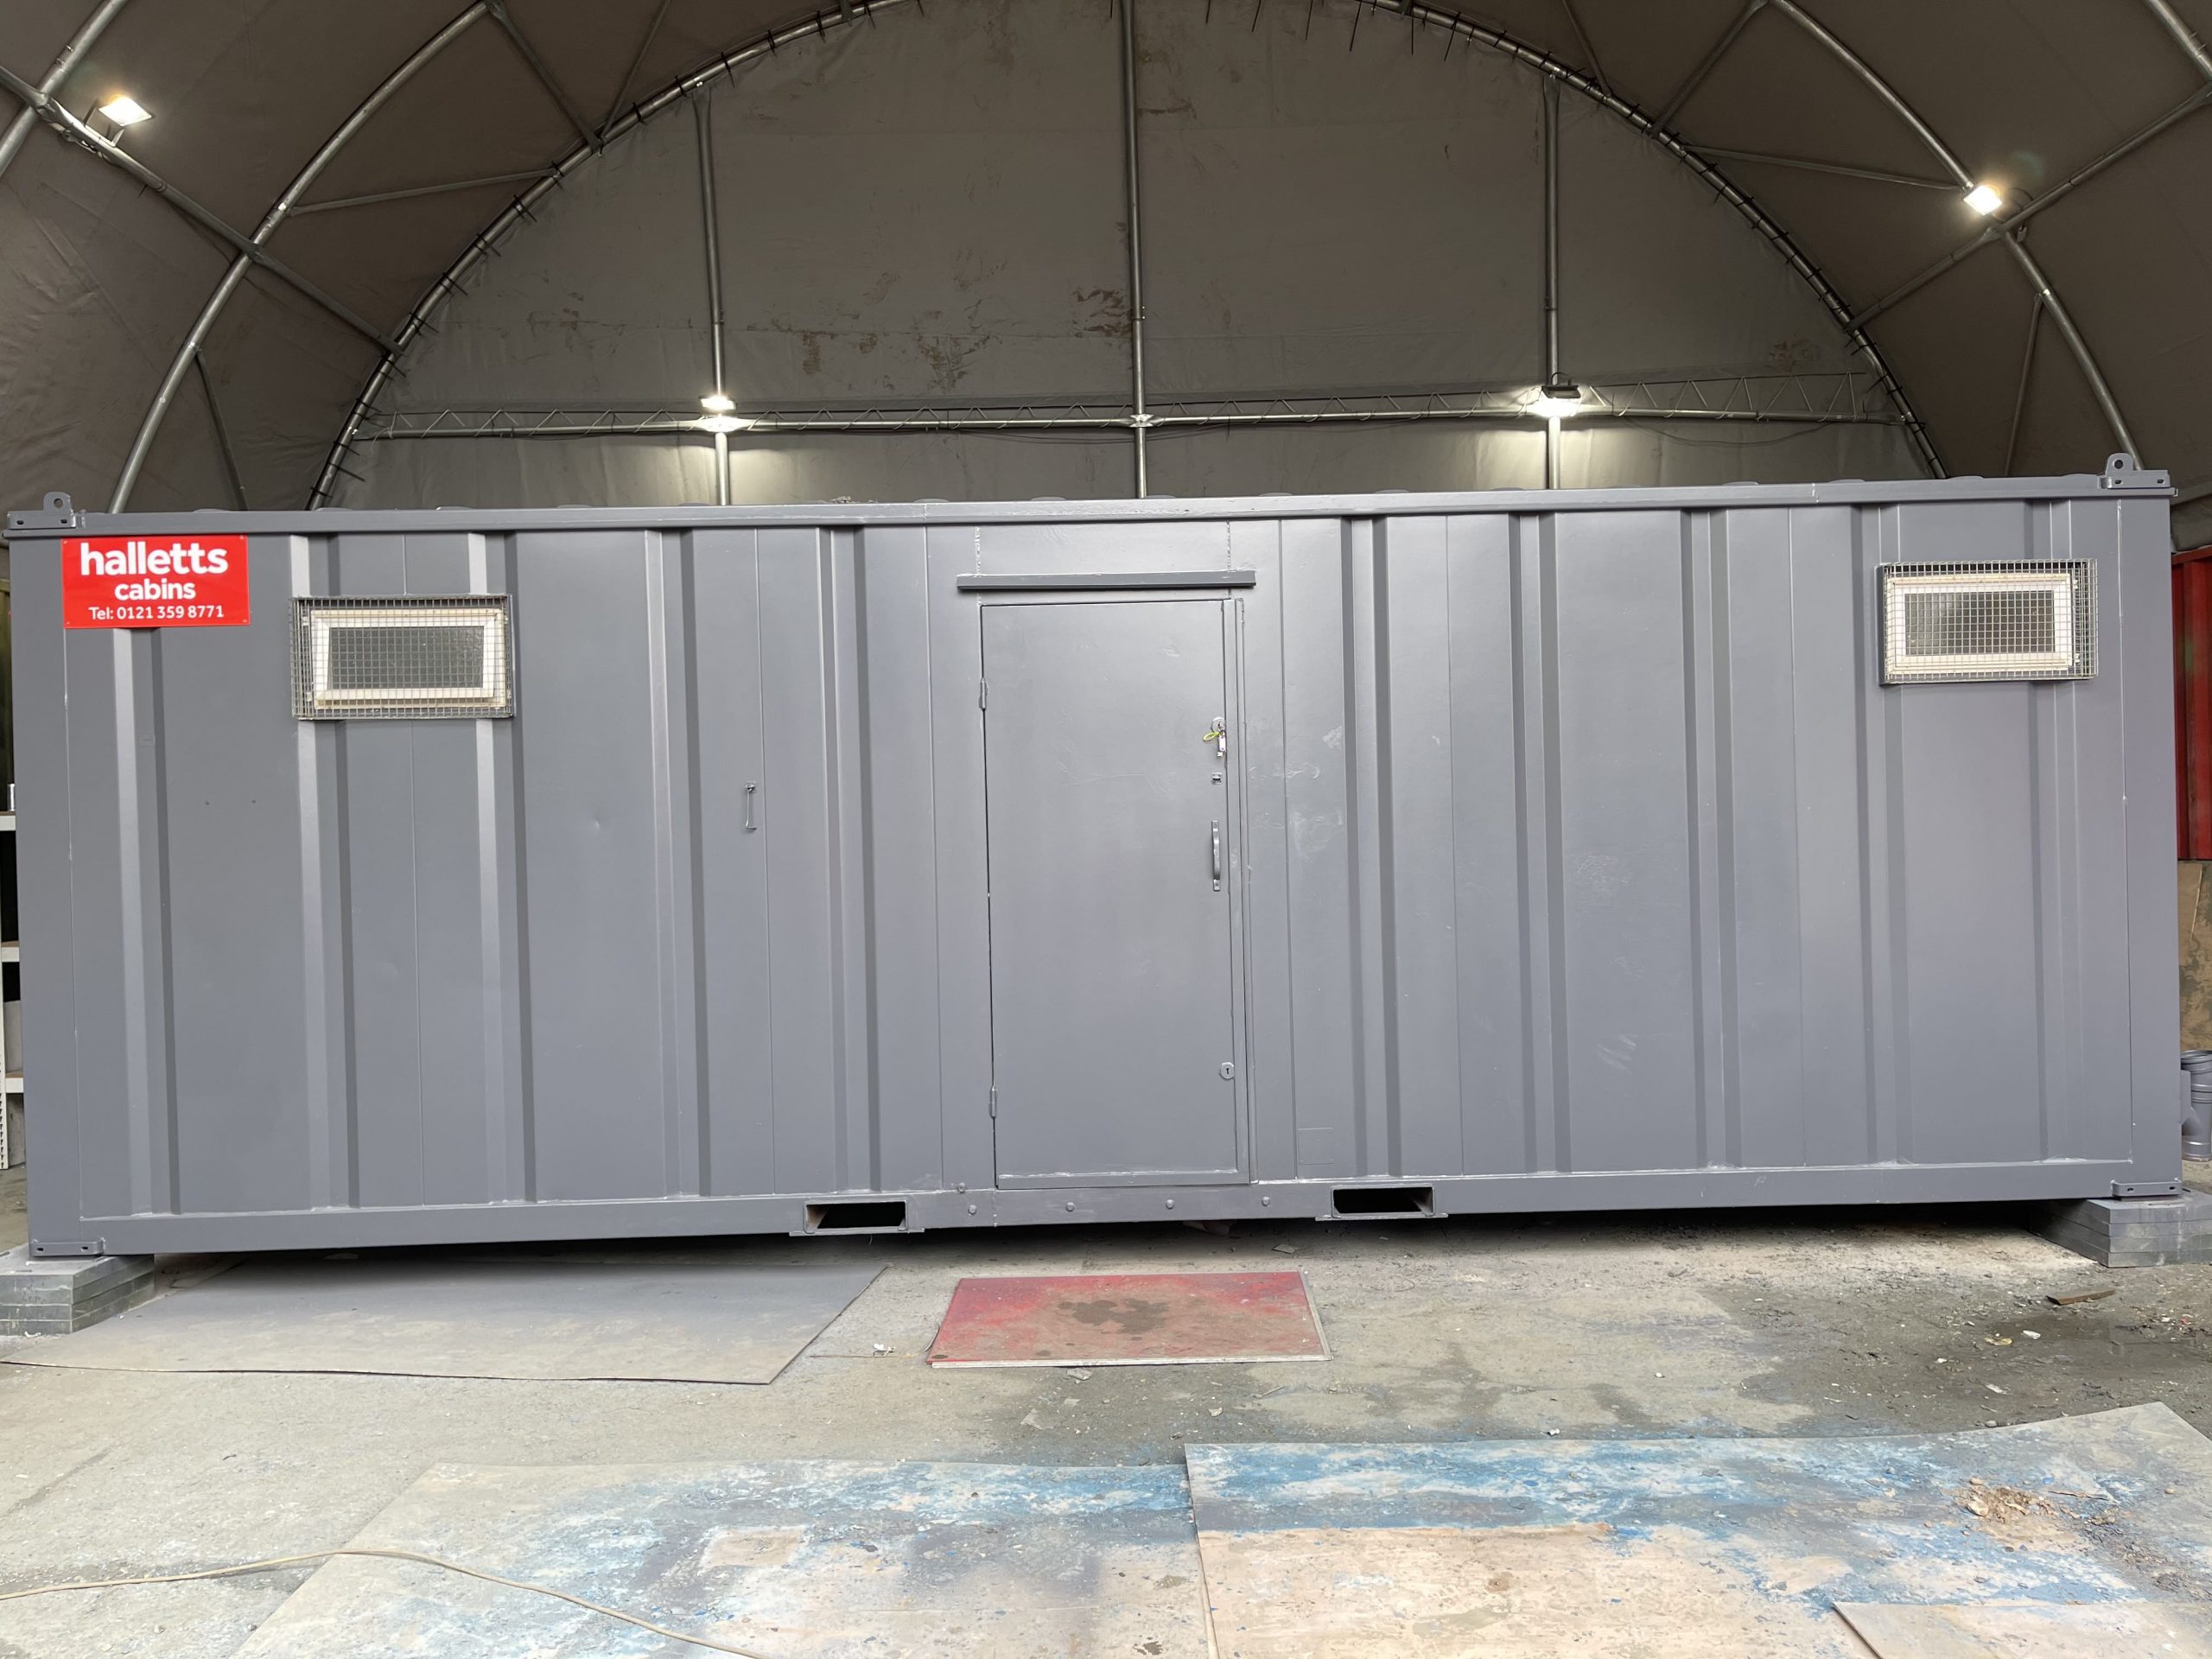
32ft x 10ft Drying Room, Toilet Block

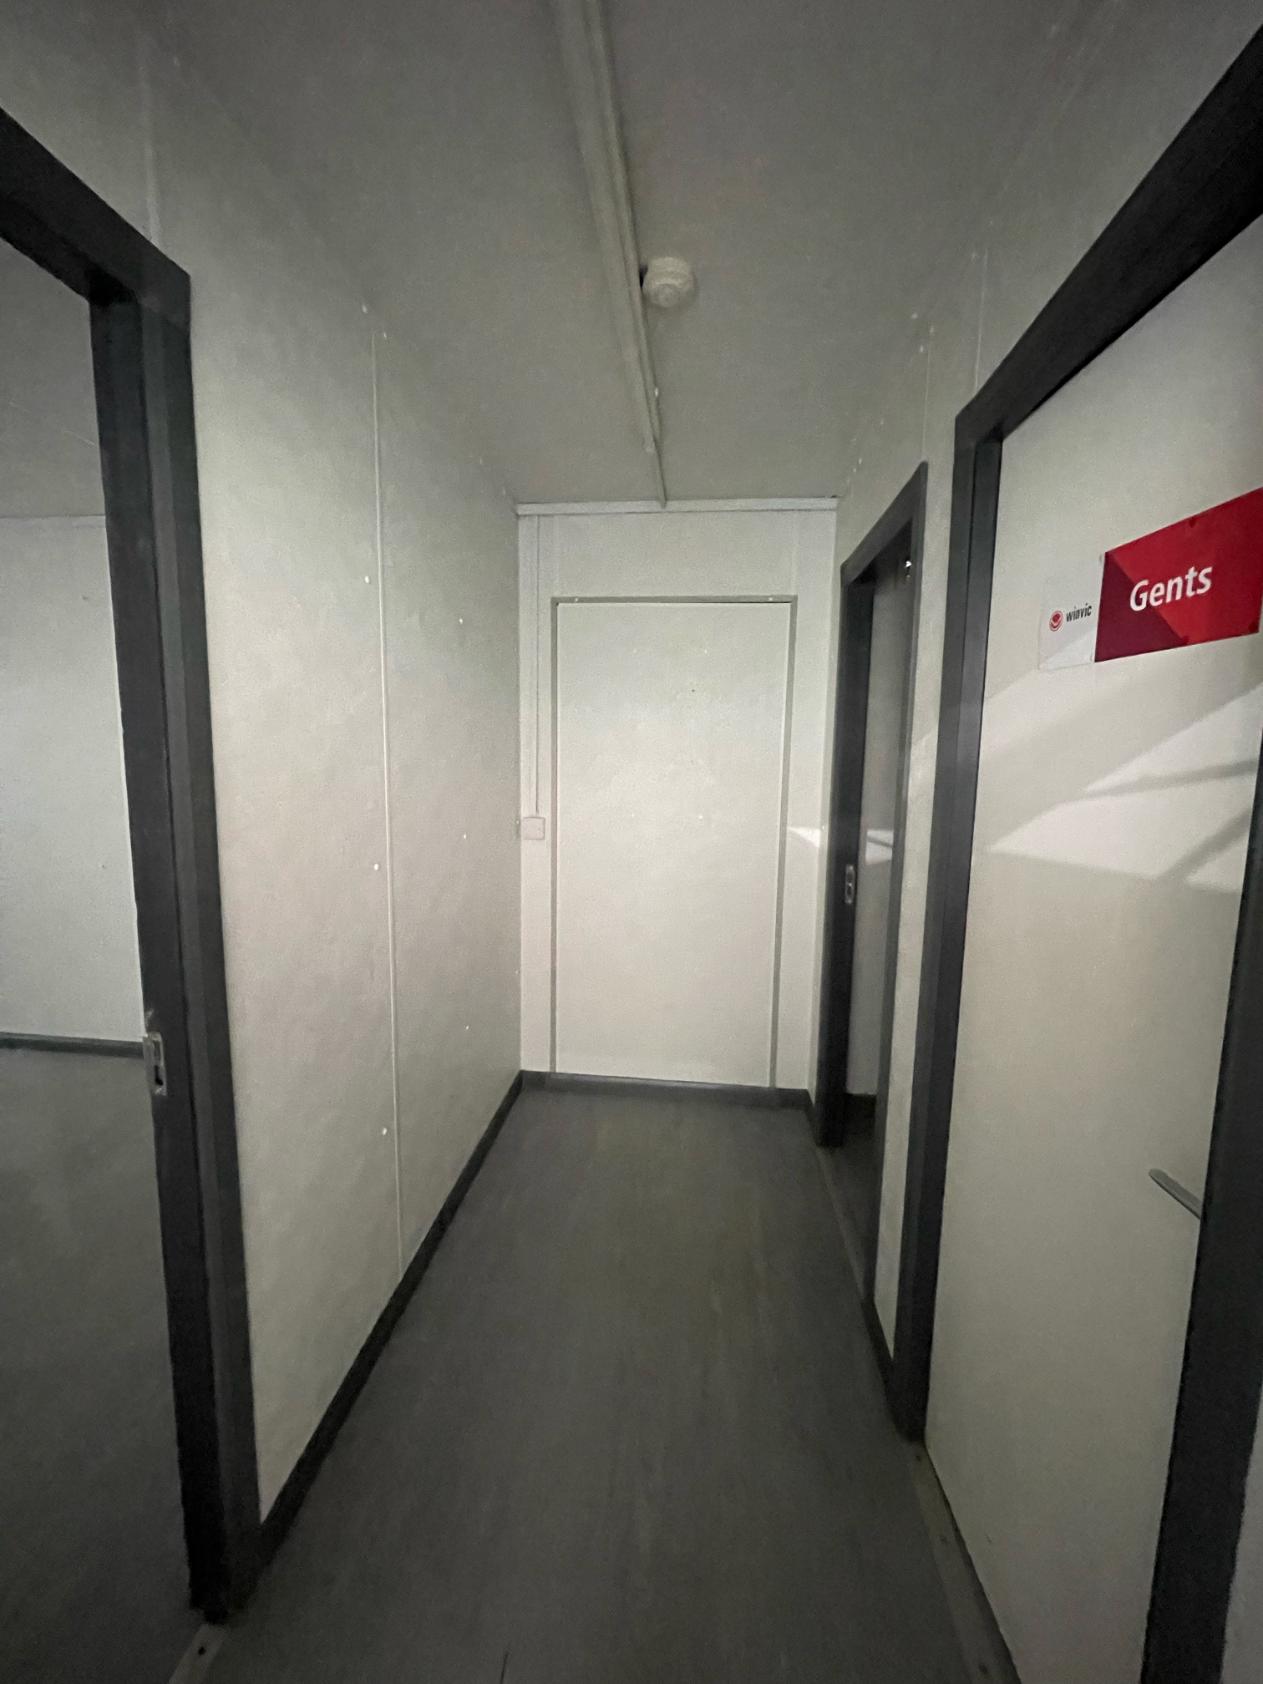
Hallway leading into:

  • Price: £6,500 + VAT
  • Half open plan drying room, or we could add in a canteen. (additional cost)
  • Female Single toilet
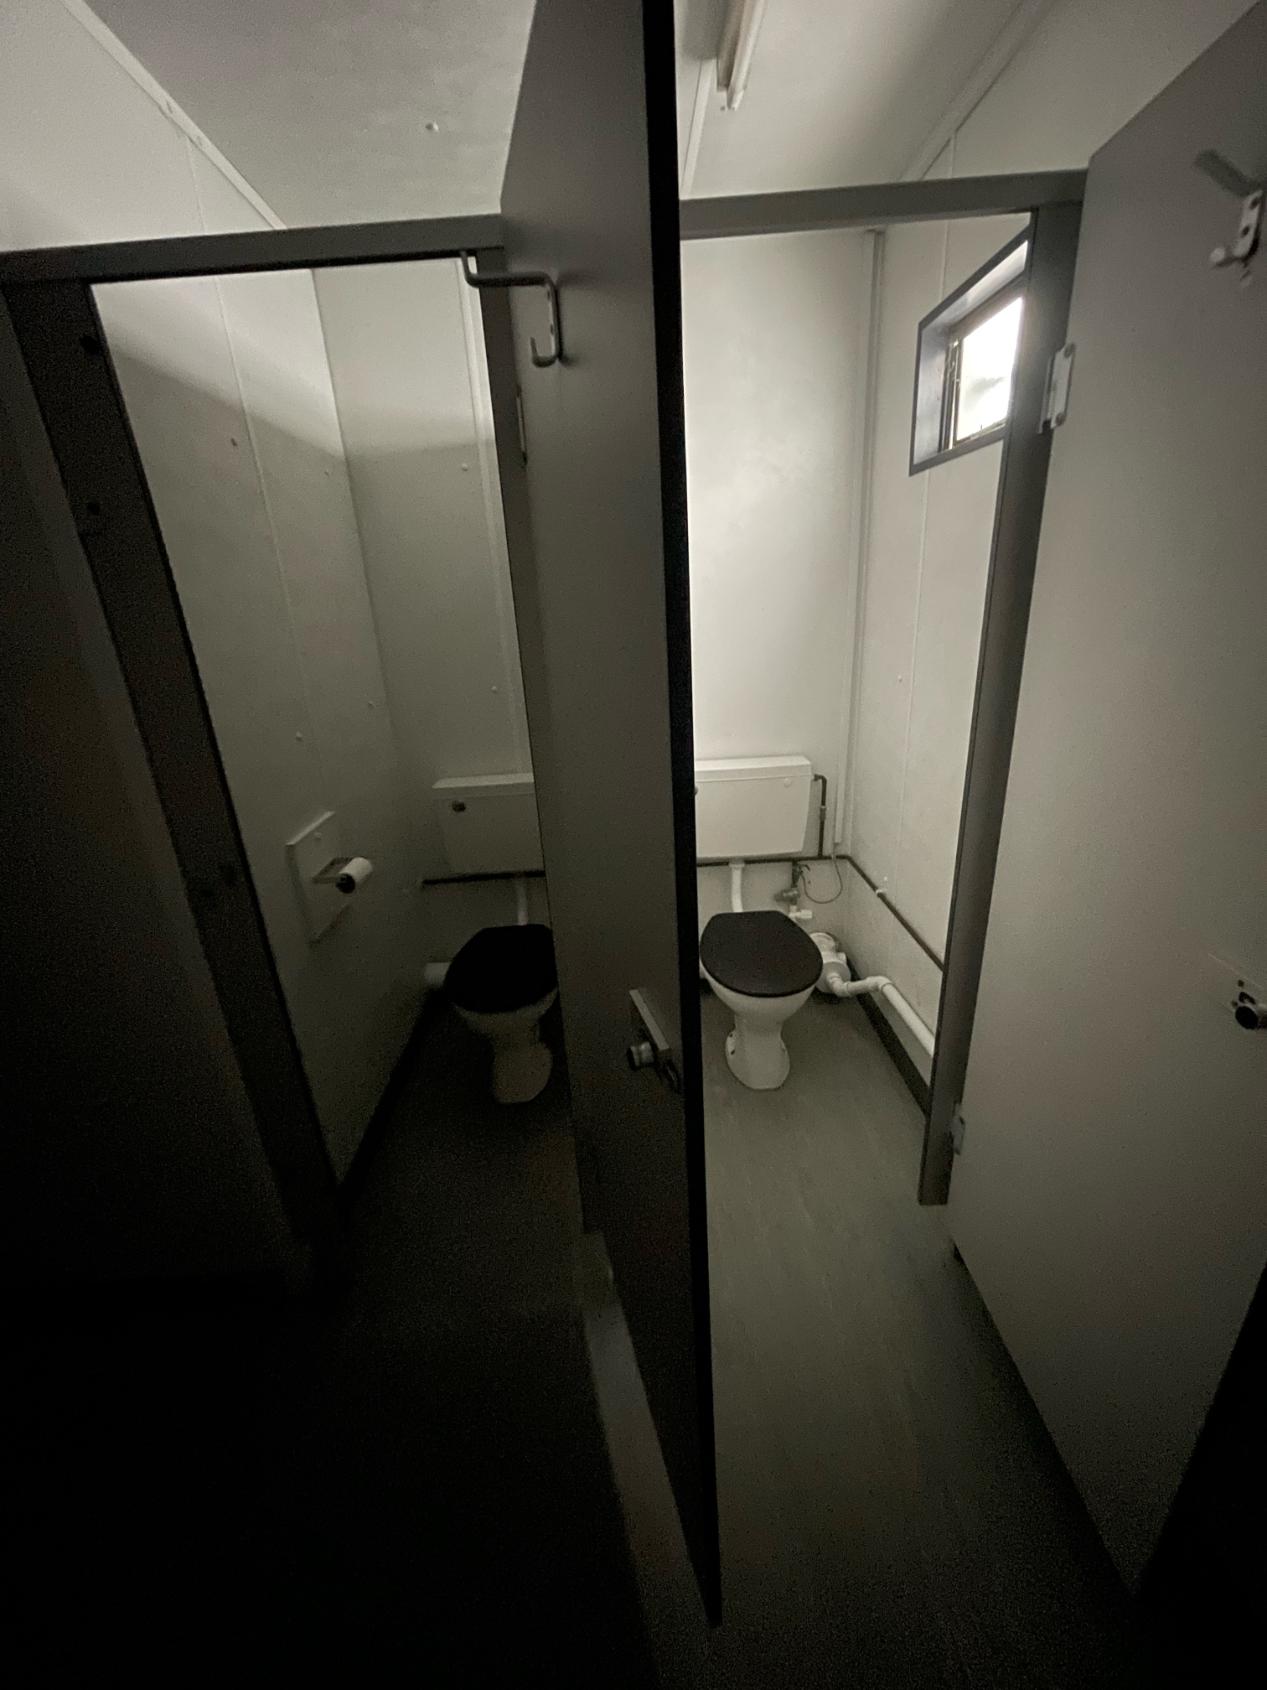
  • Male toilets including 2 x cubicles, 2 x urinals and 2 x sinks
  • External light grey spray
  • Deep cleaned
  • Ready to use
  • Excellent overall condition

Transport can be arranged please ask.

Location: Nationwide

£6,500.00 + vat

Not Available for Hire

Call for an instant quote!

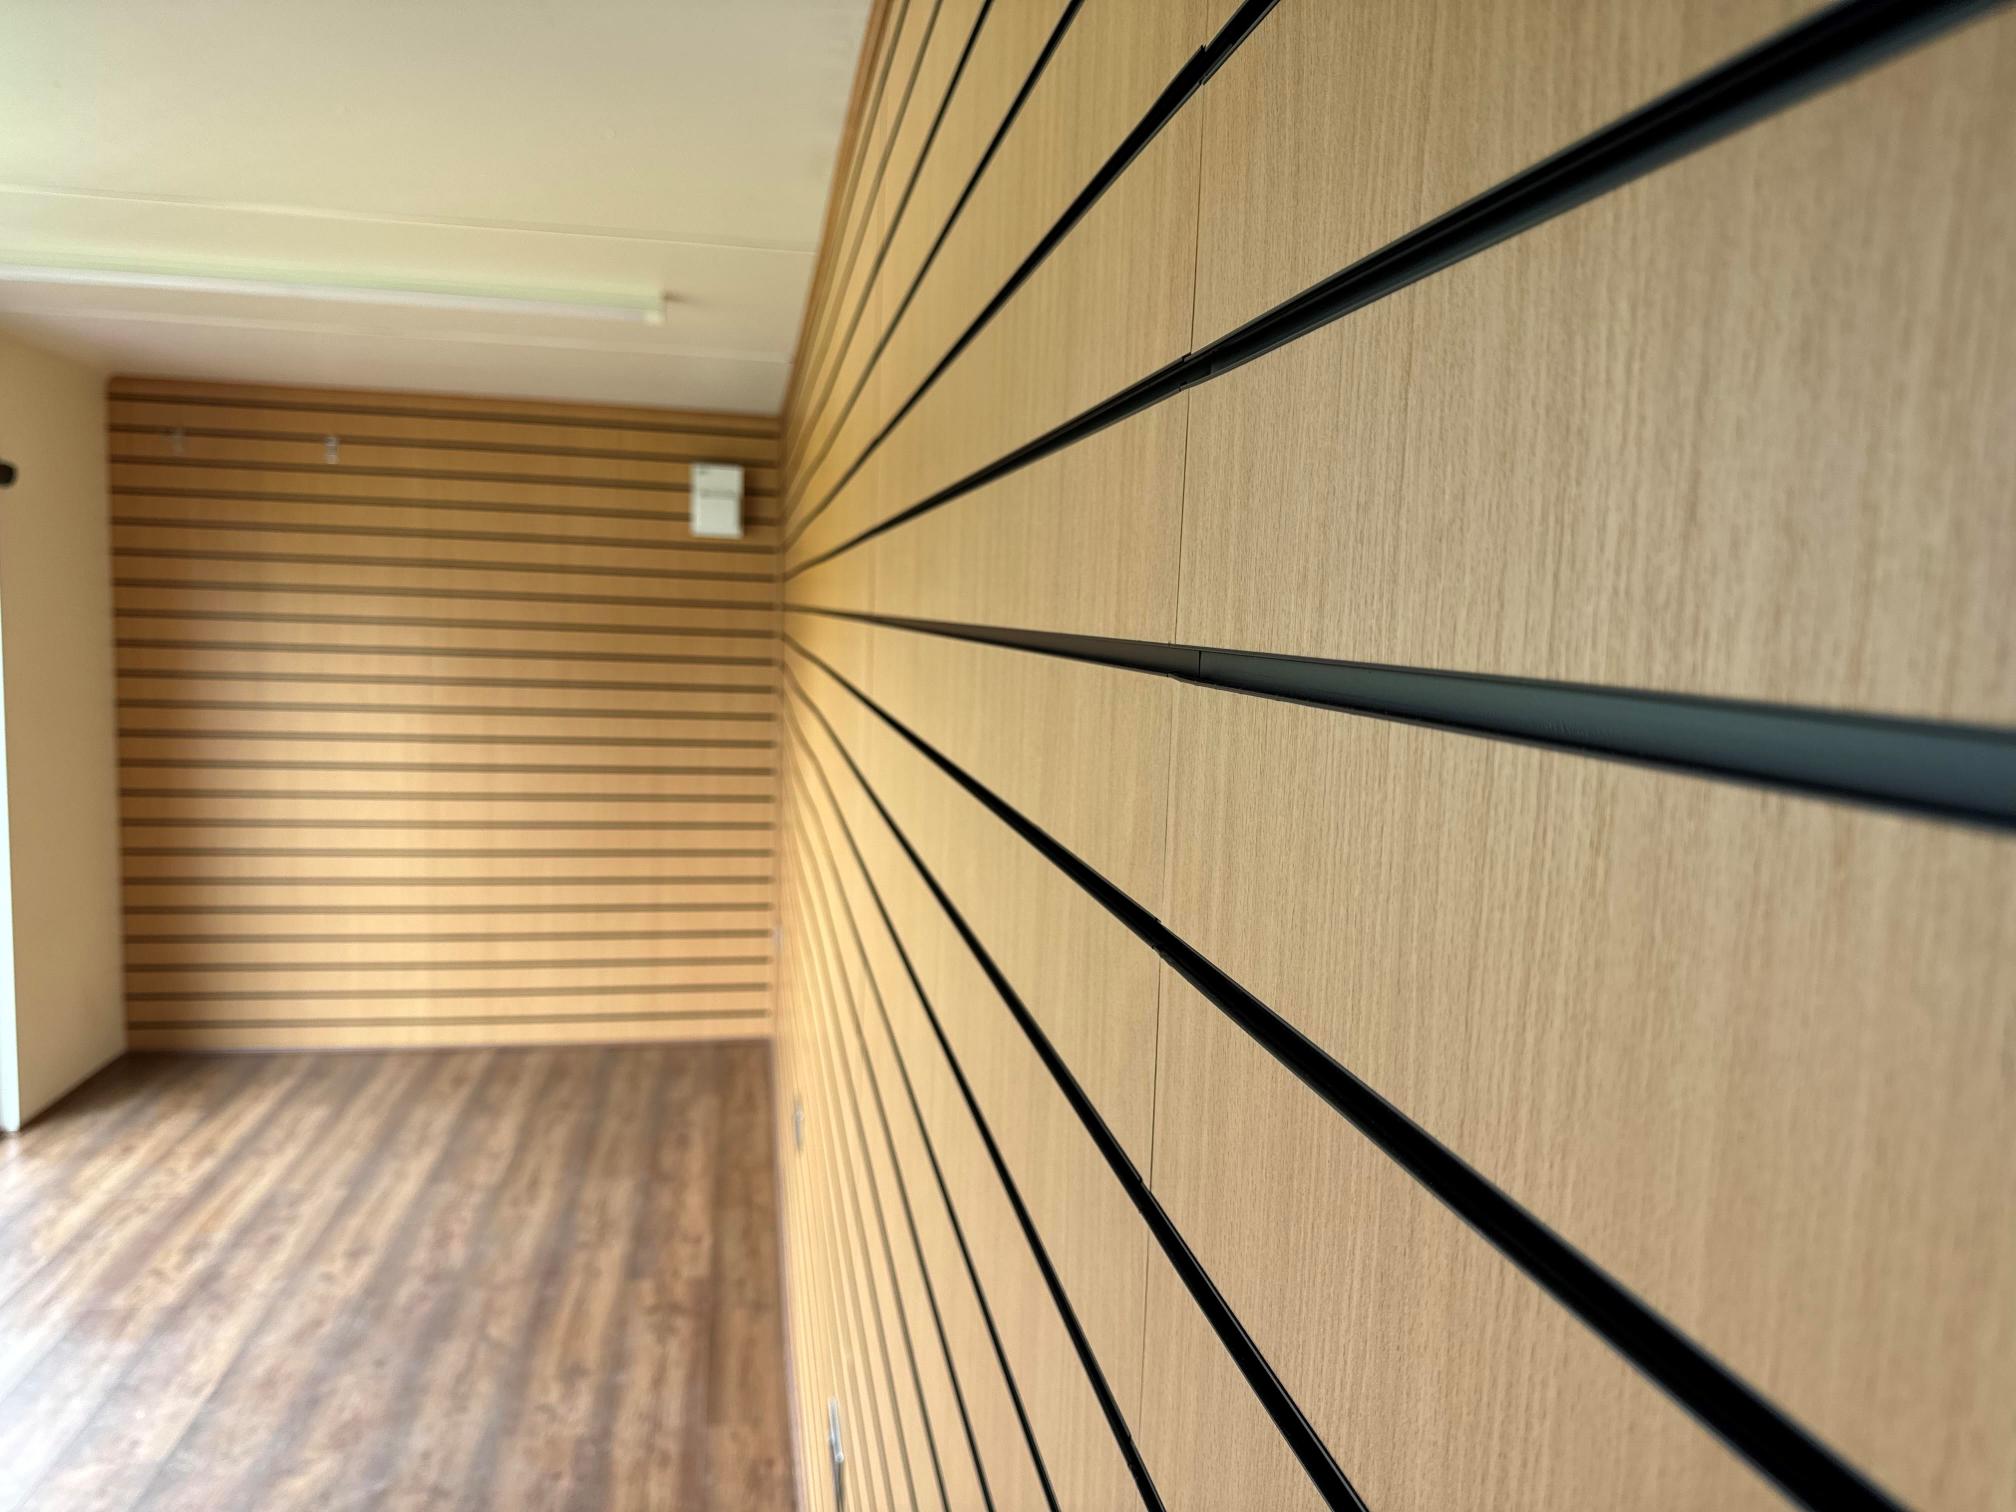
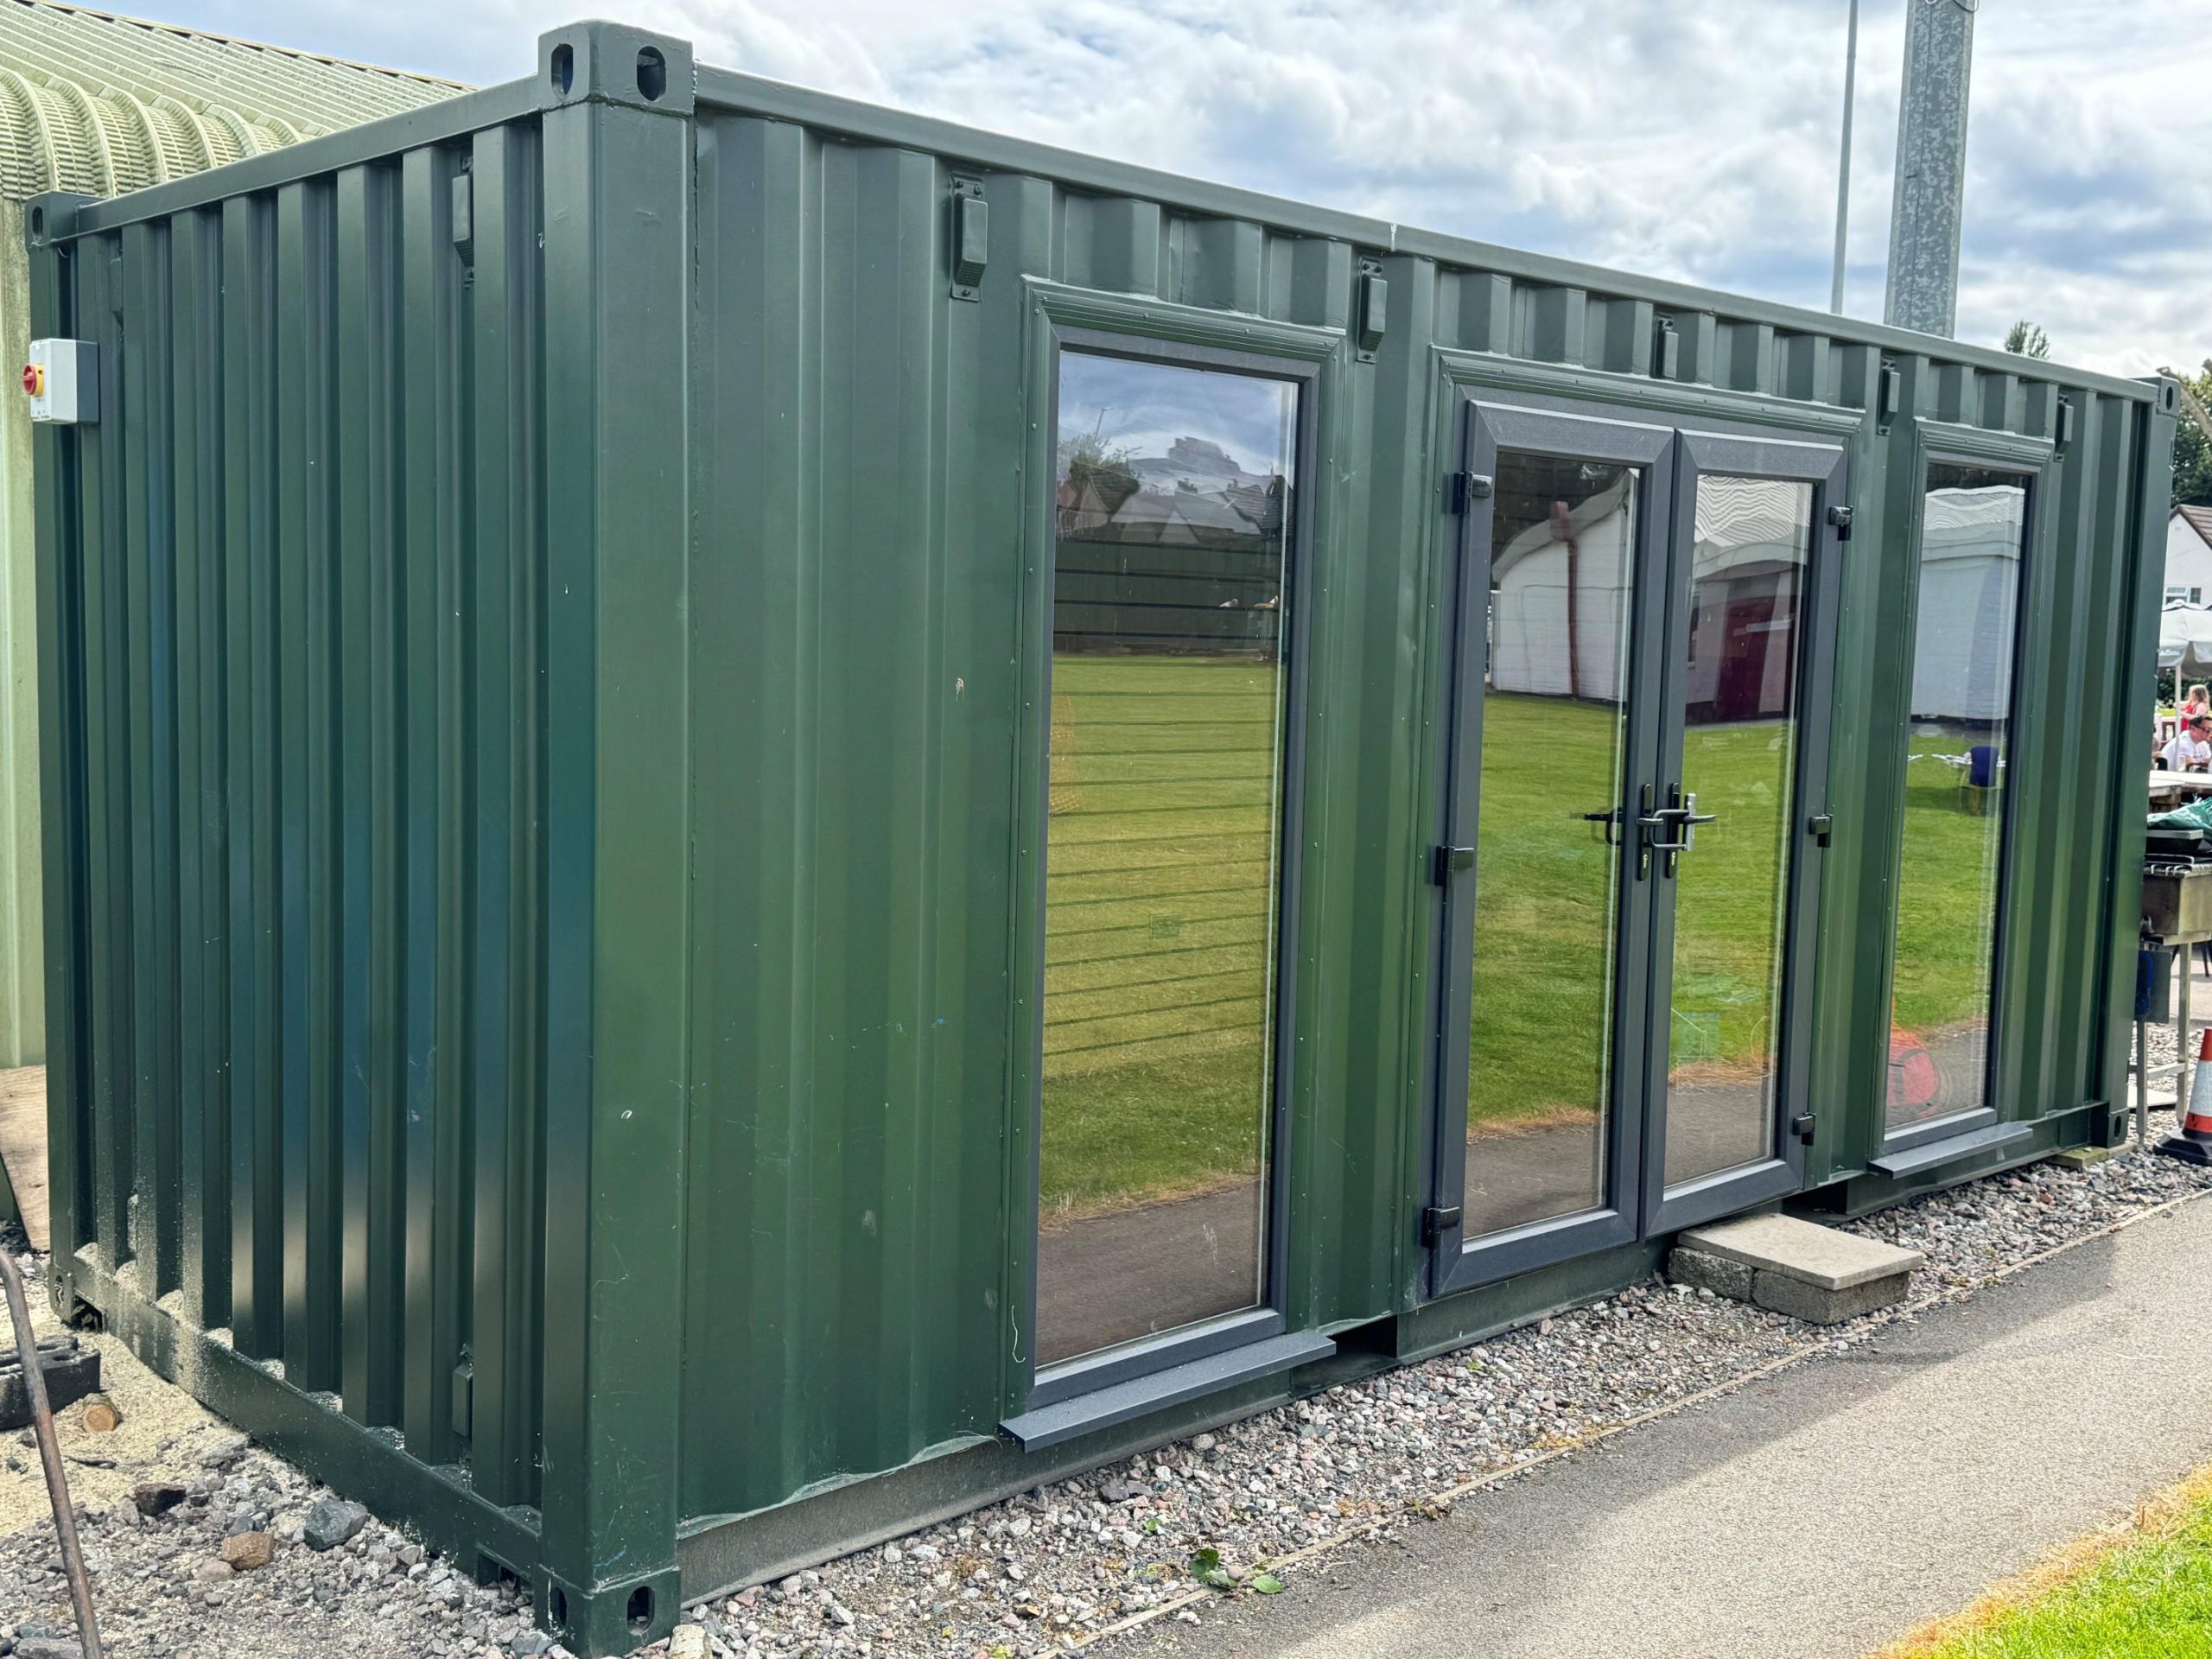
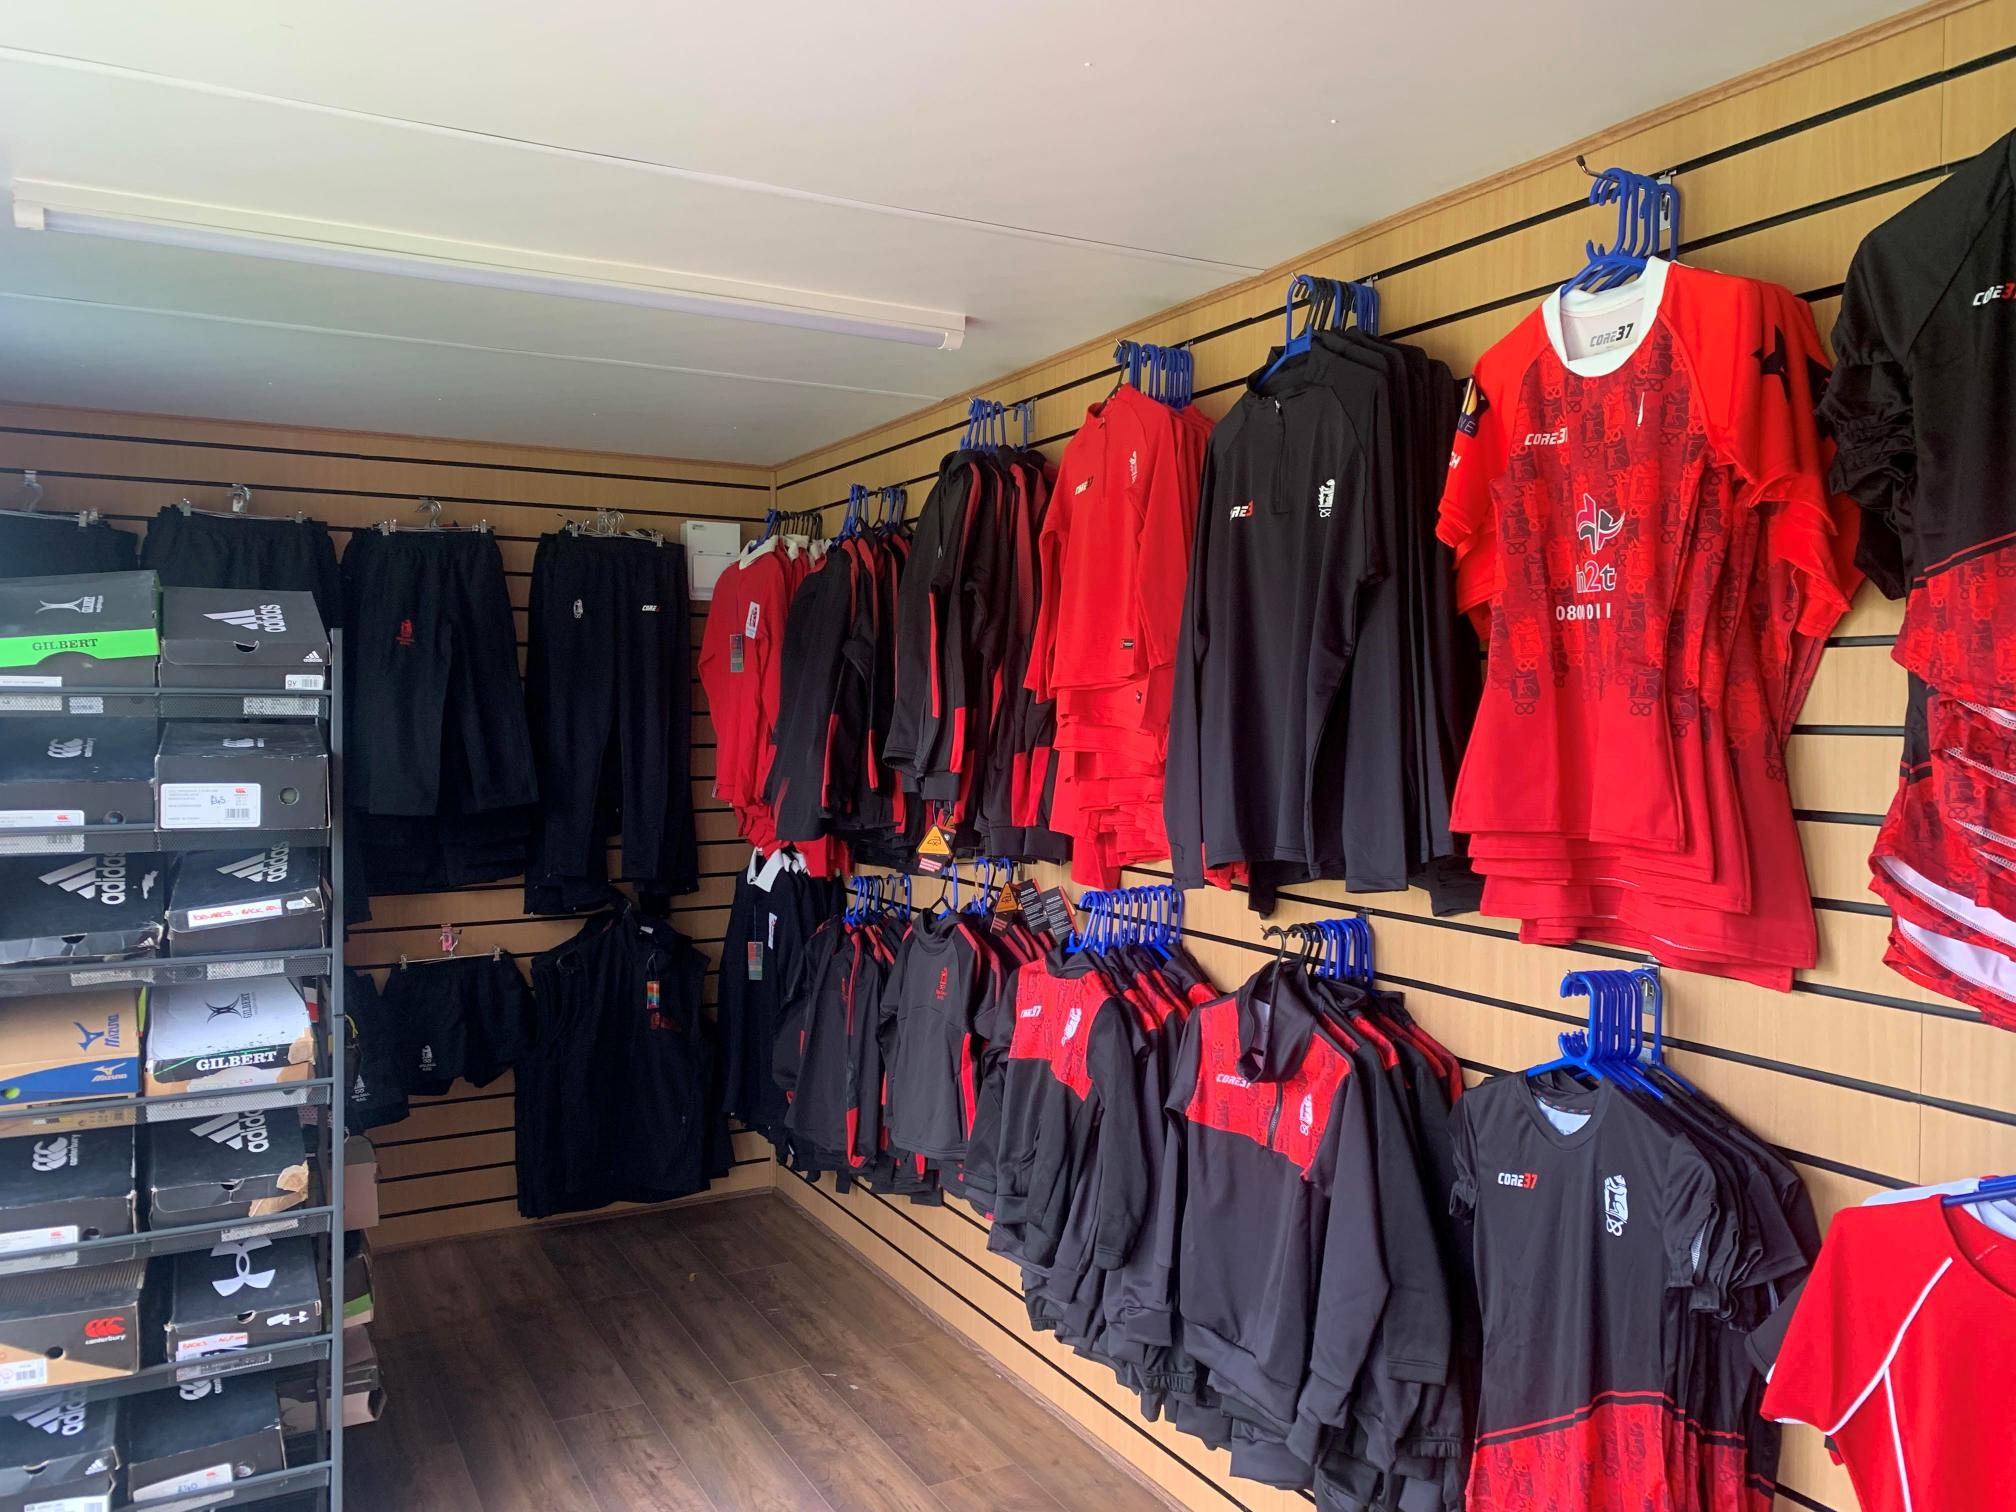
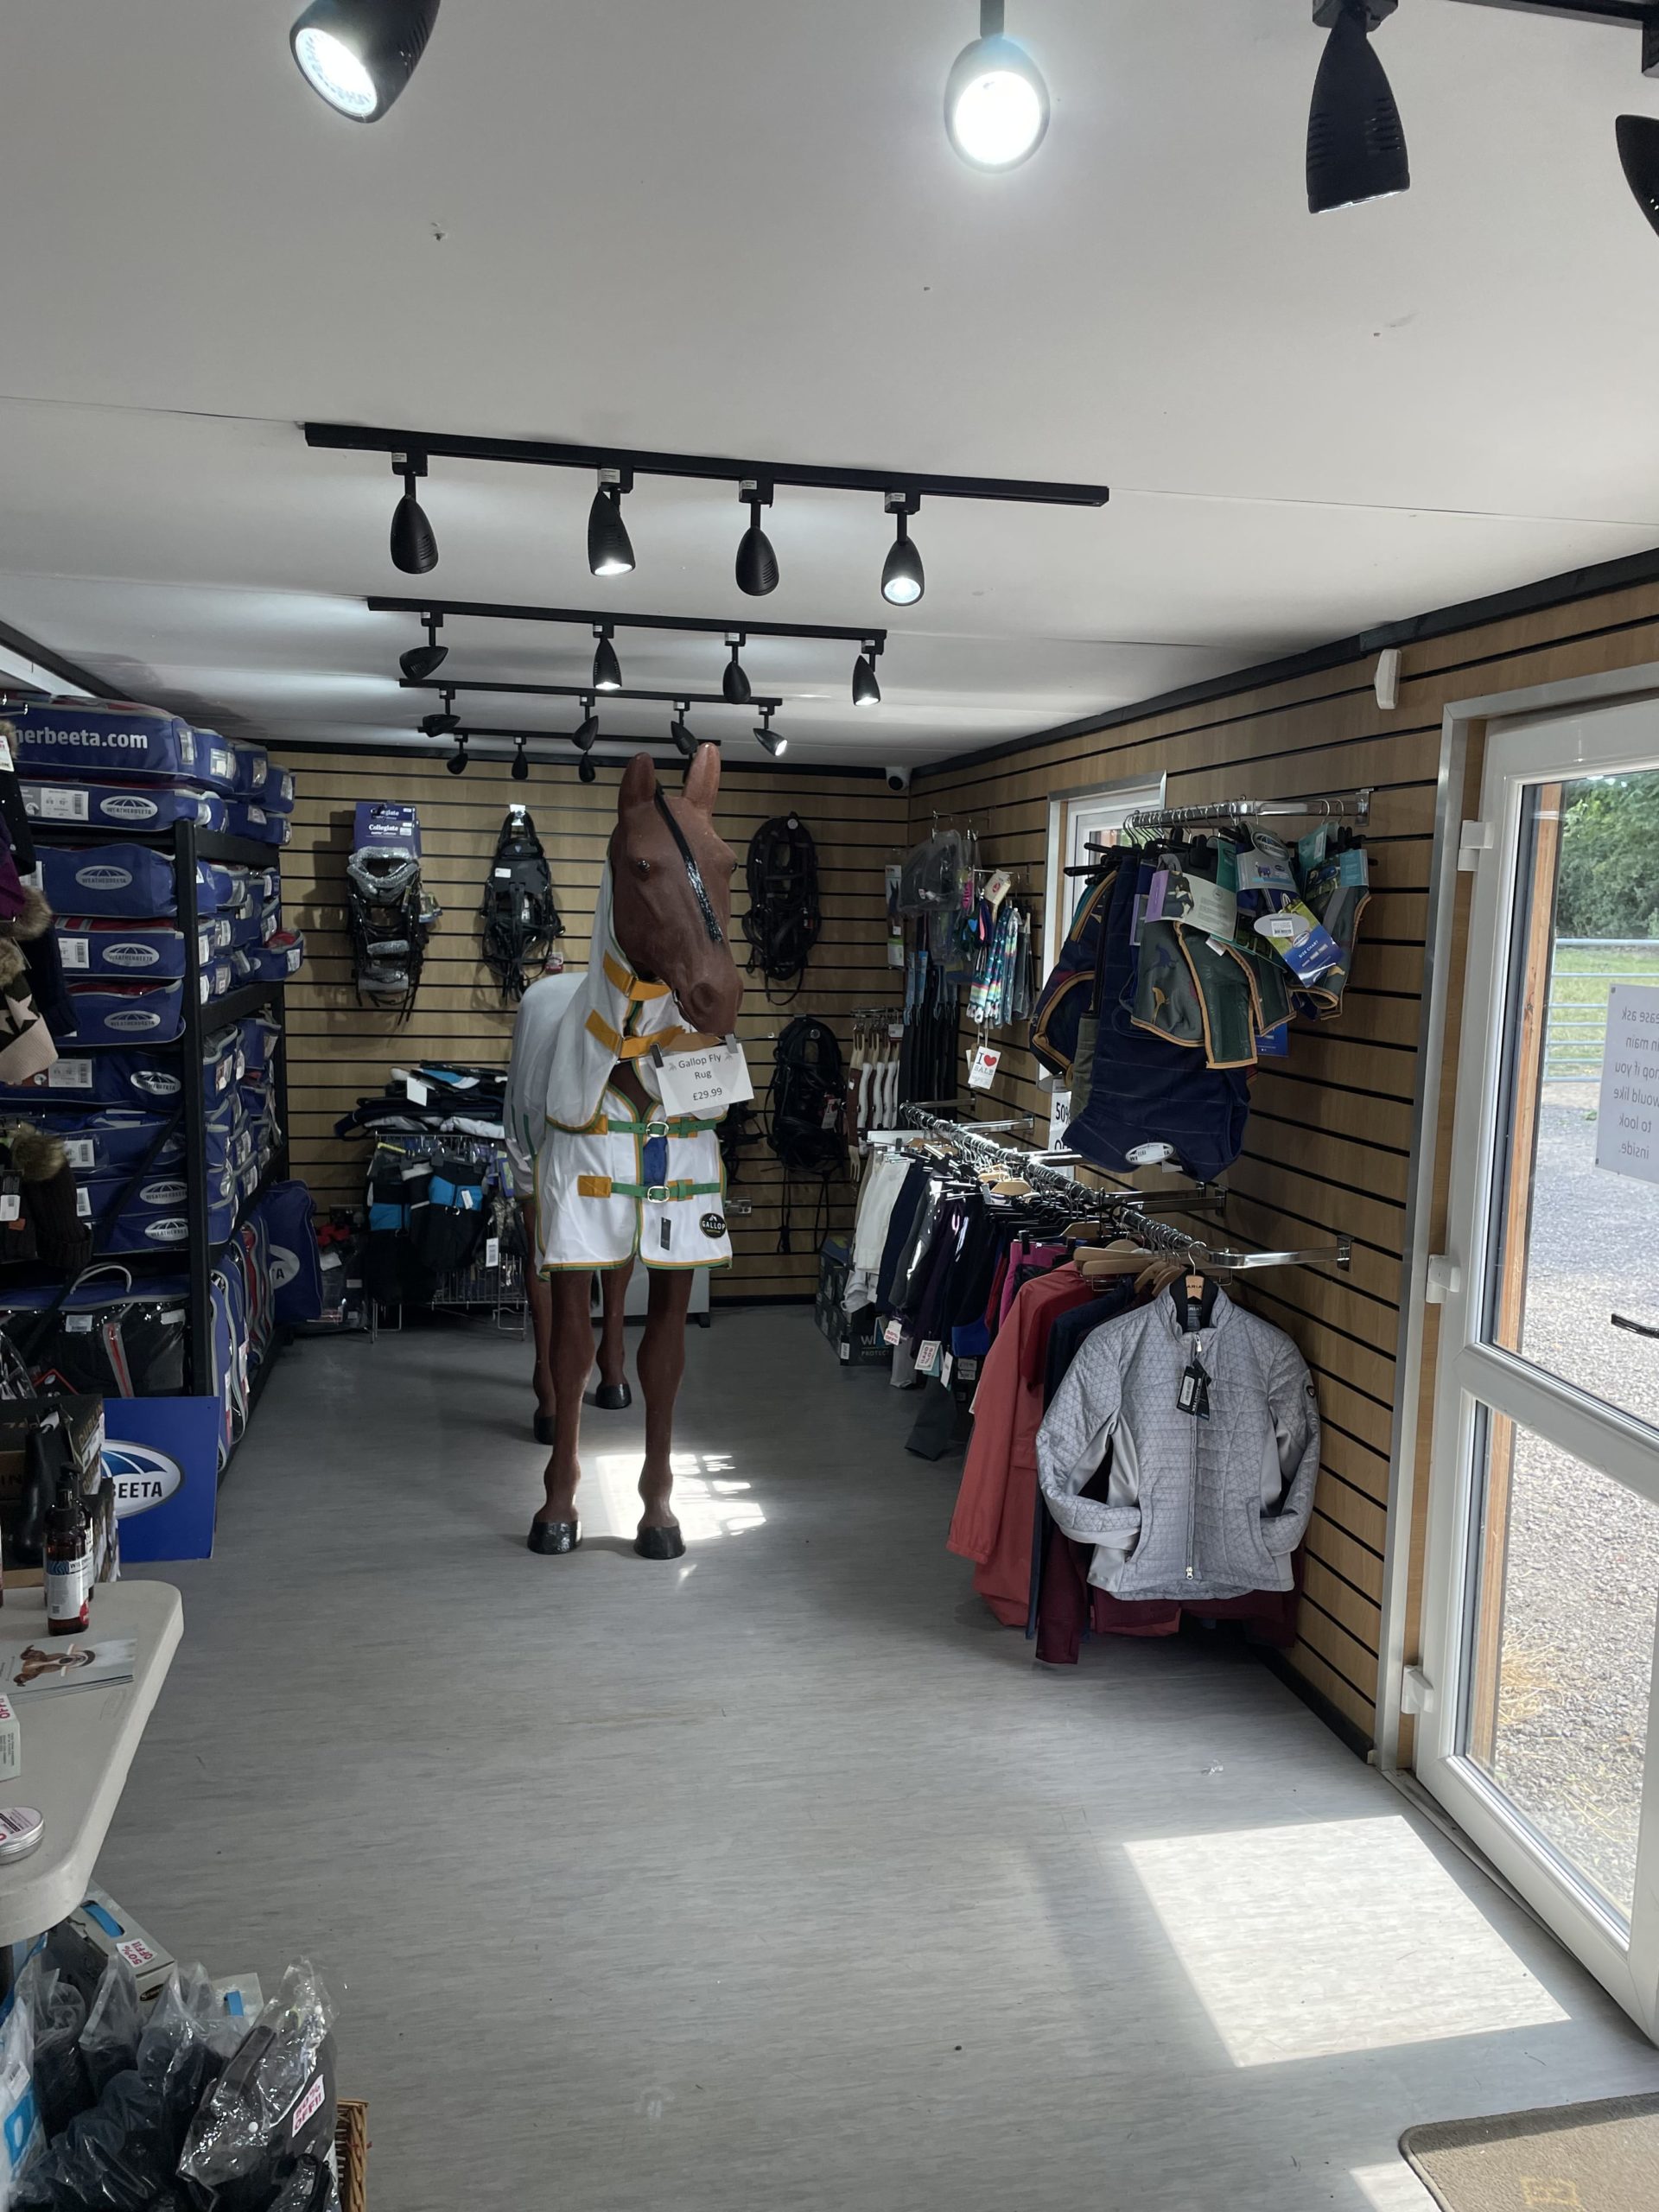
  • 20ft x 8ft Container Conversion Retail Shop

  • UPVC Double glazed Windows + French Doors

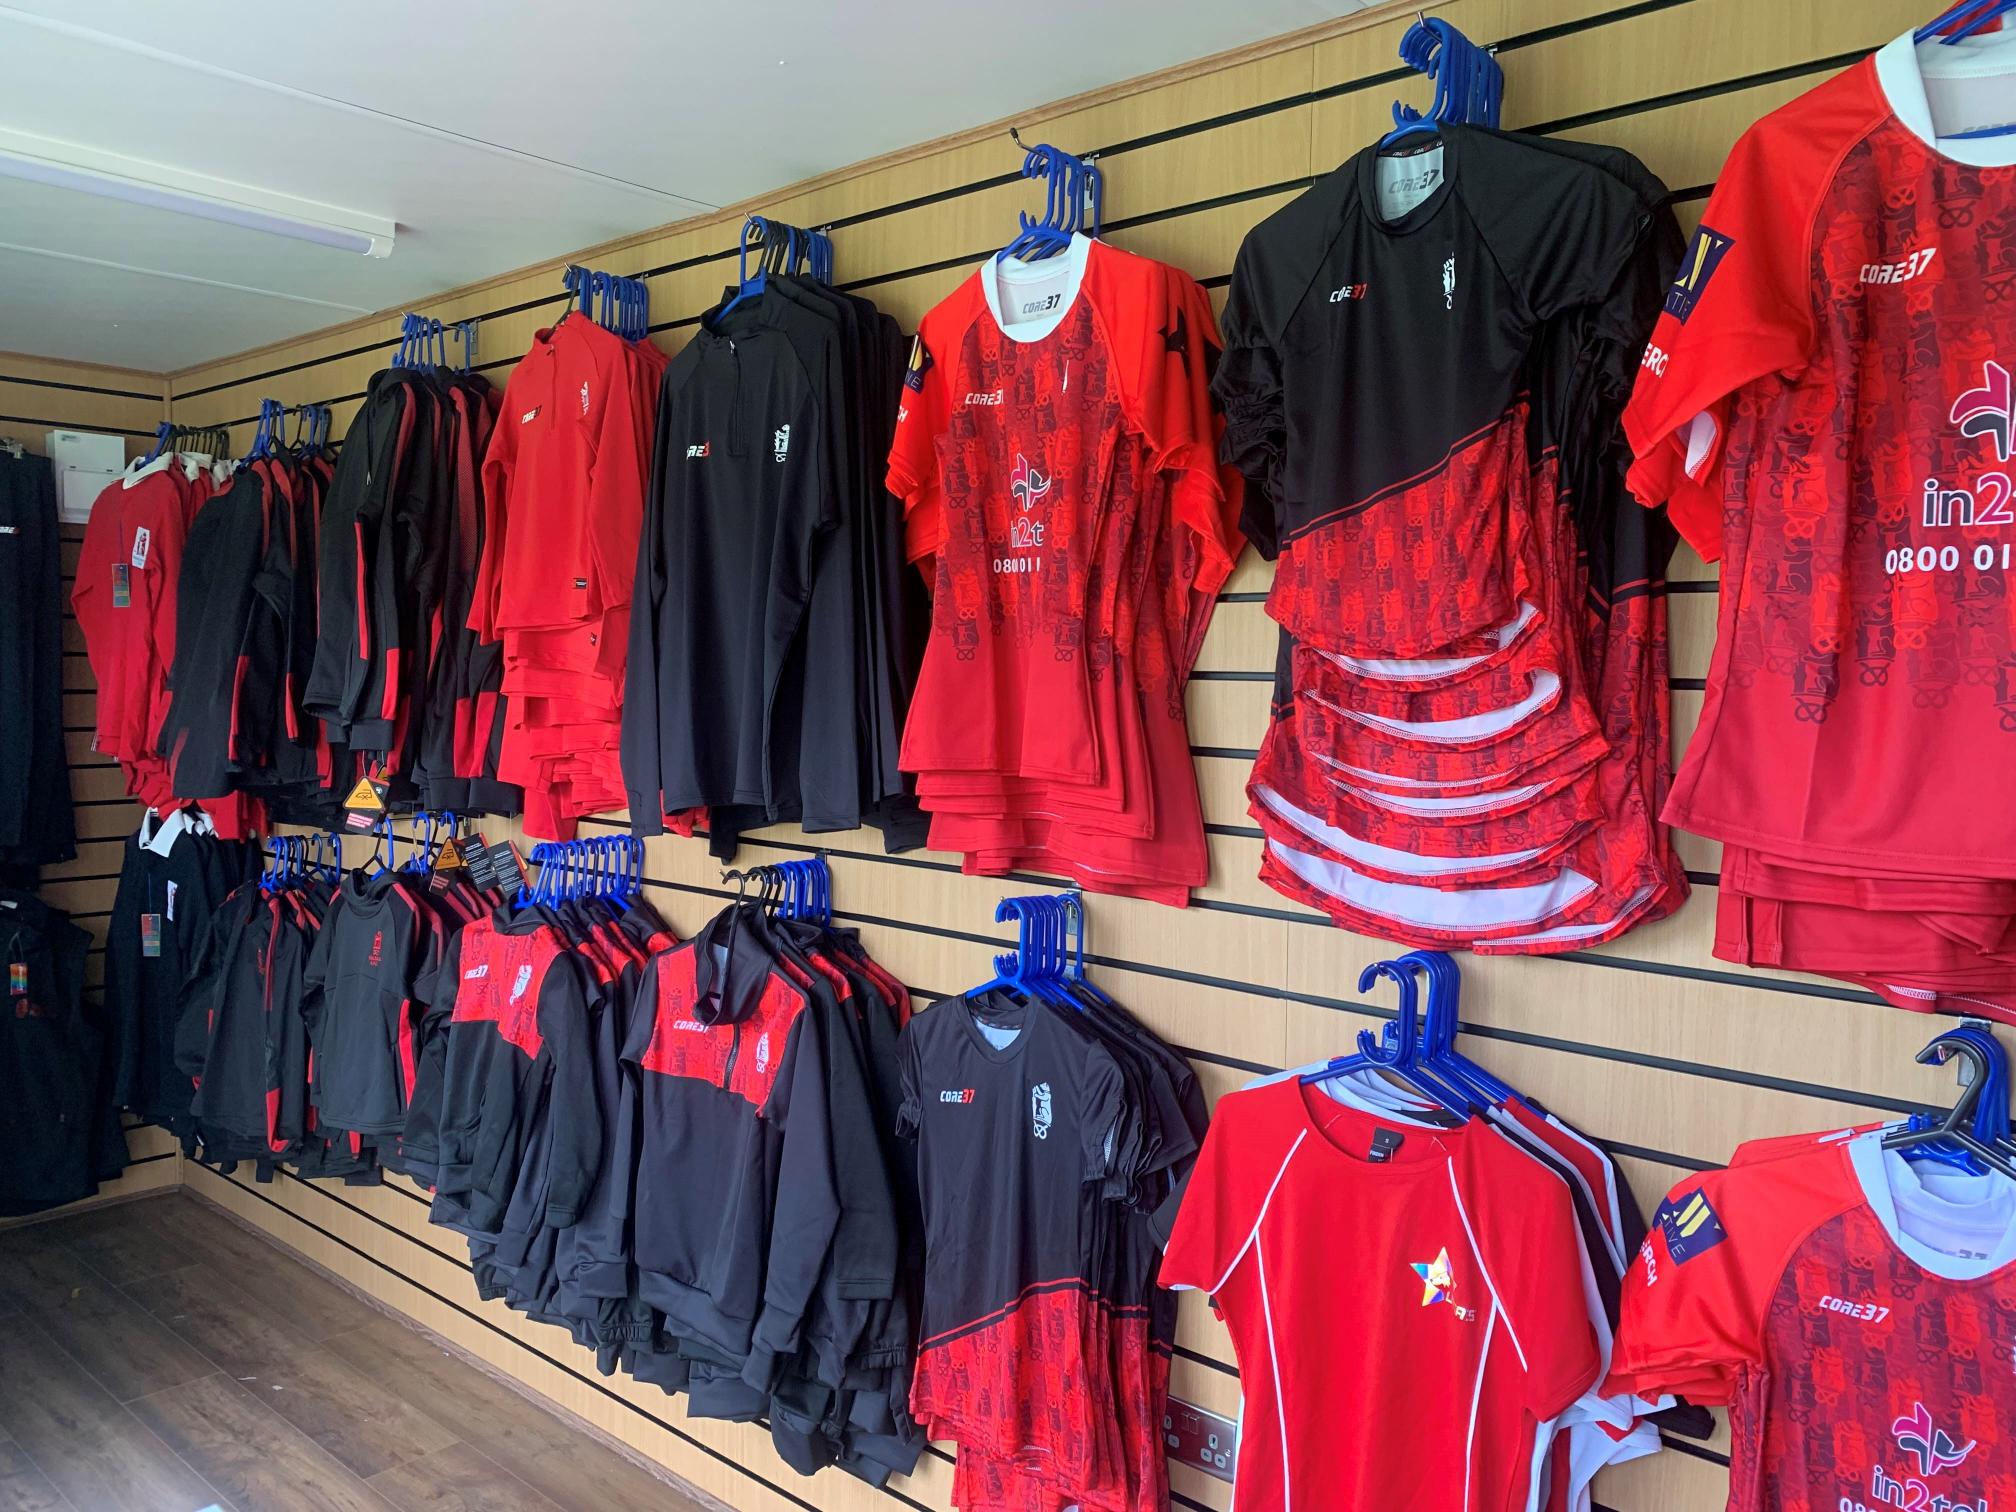
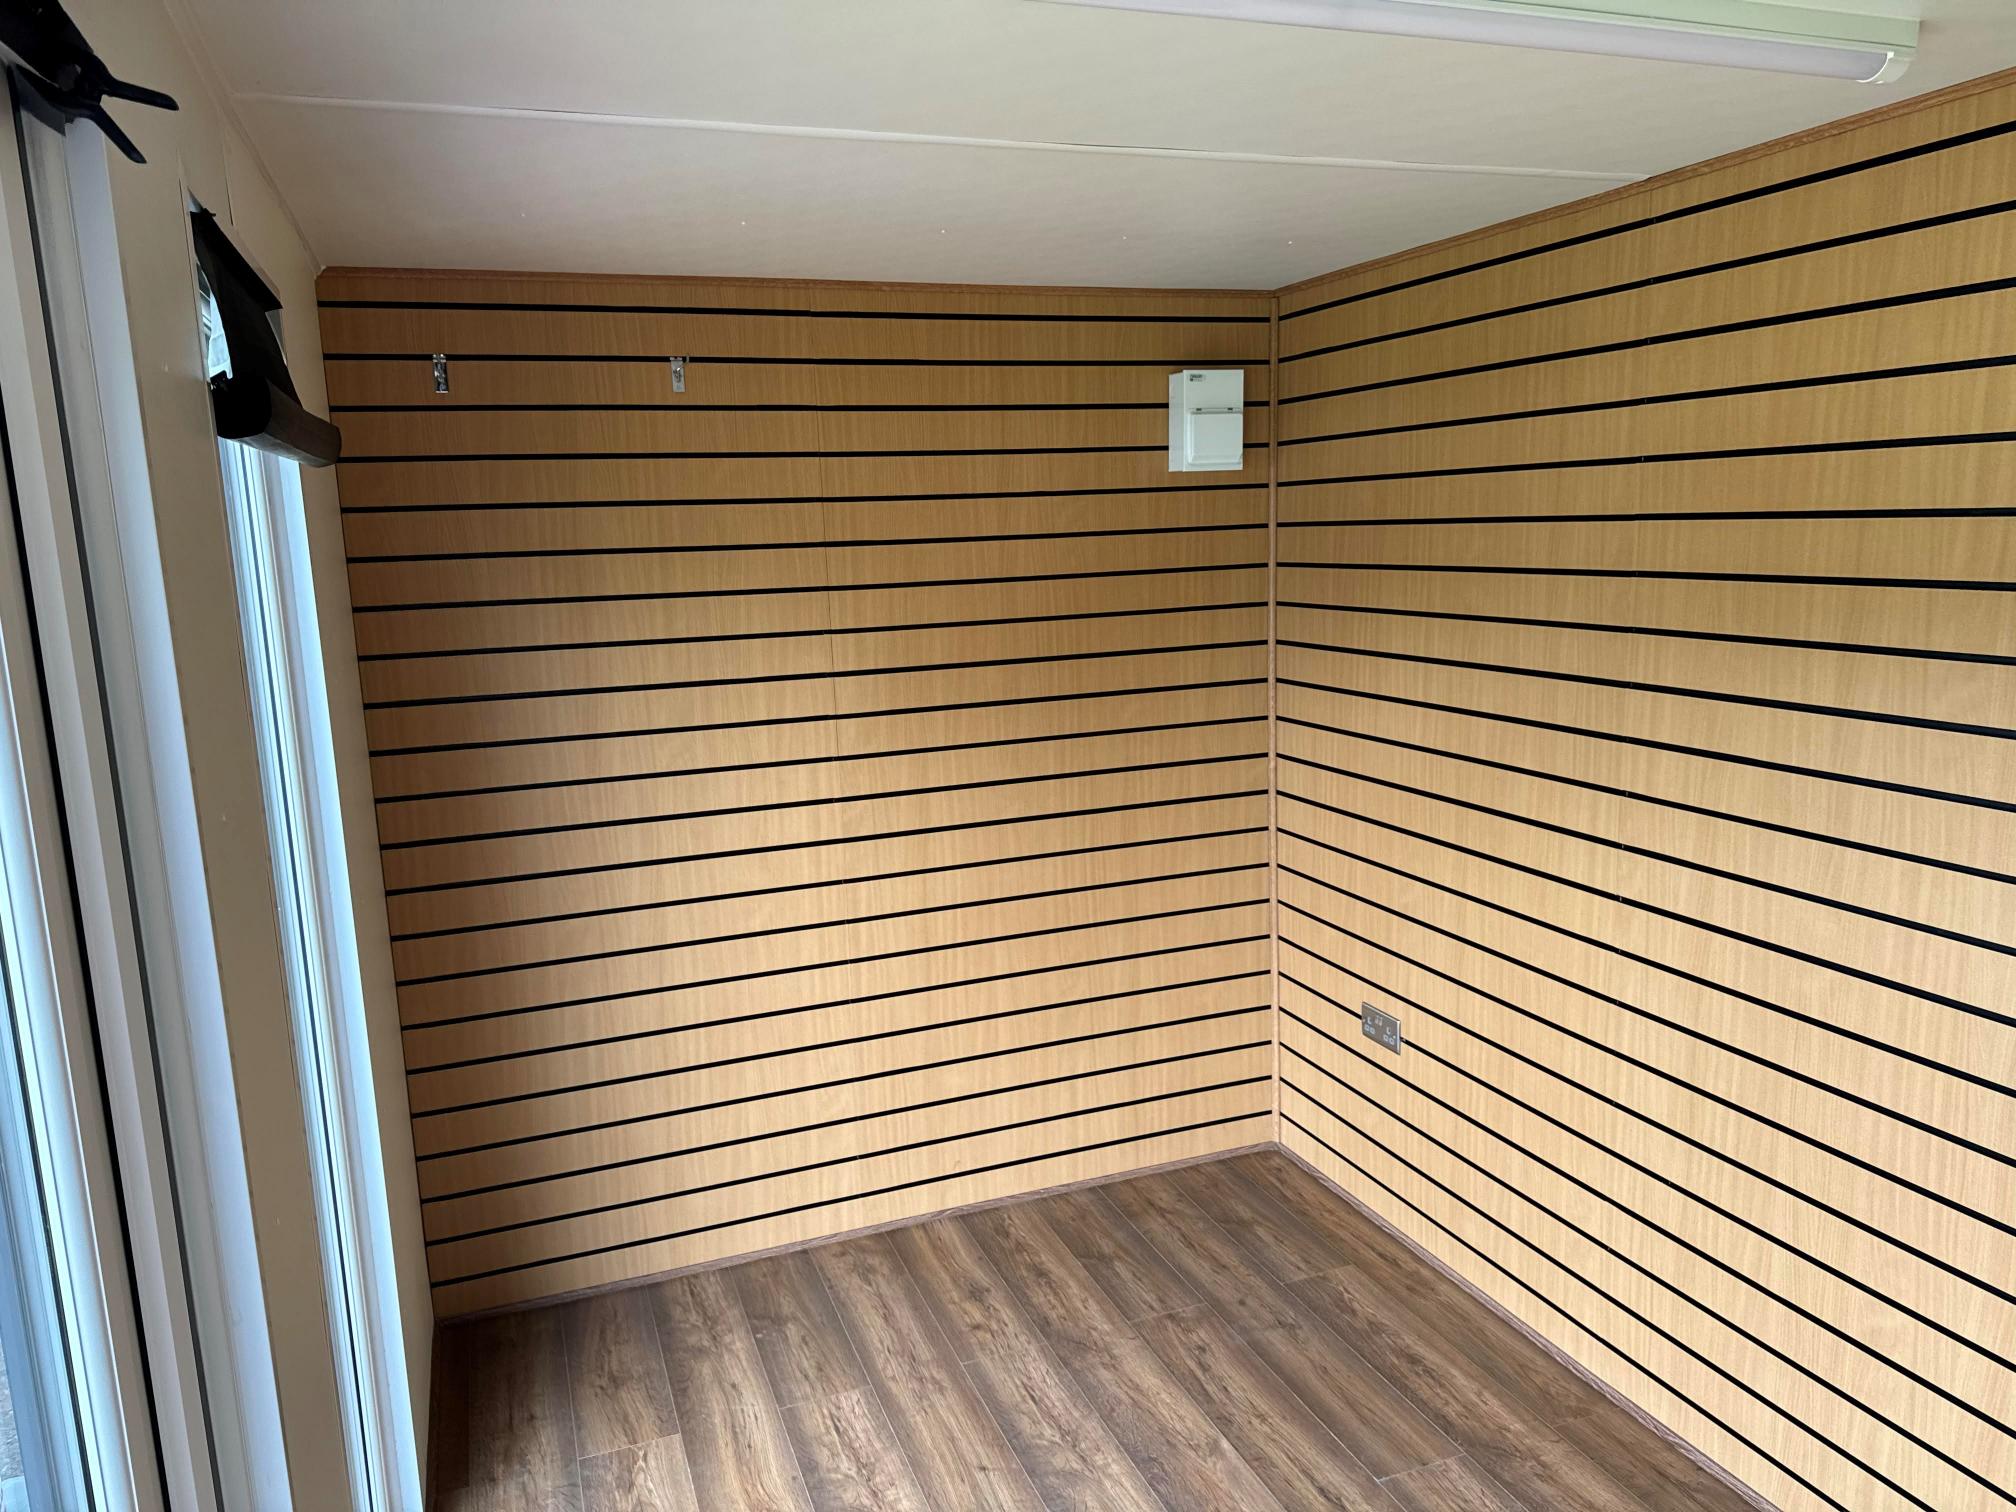
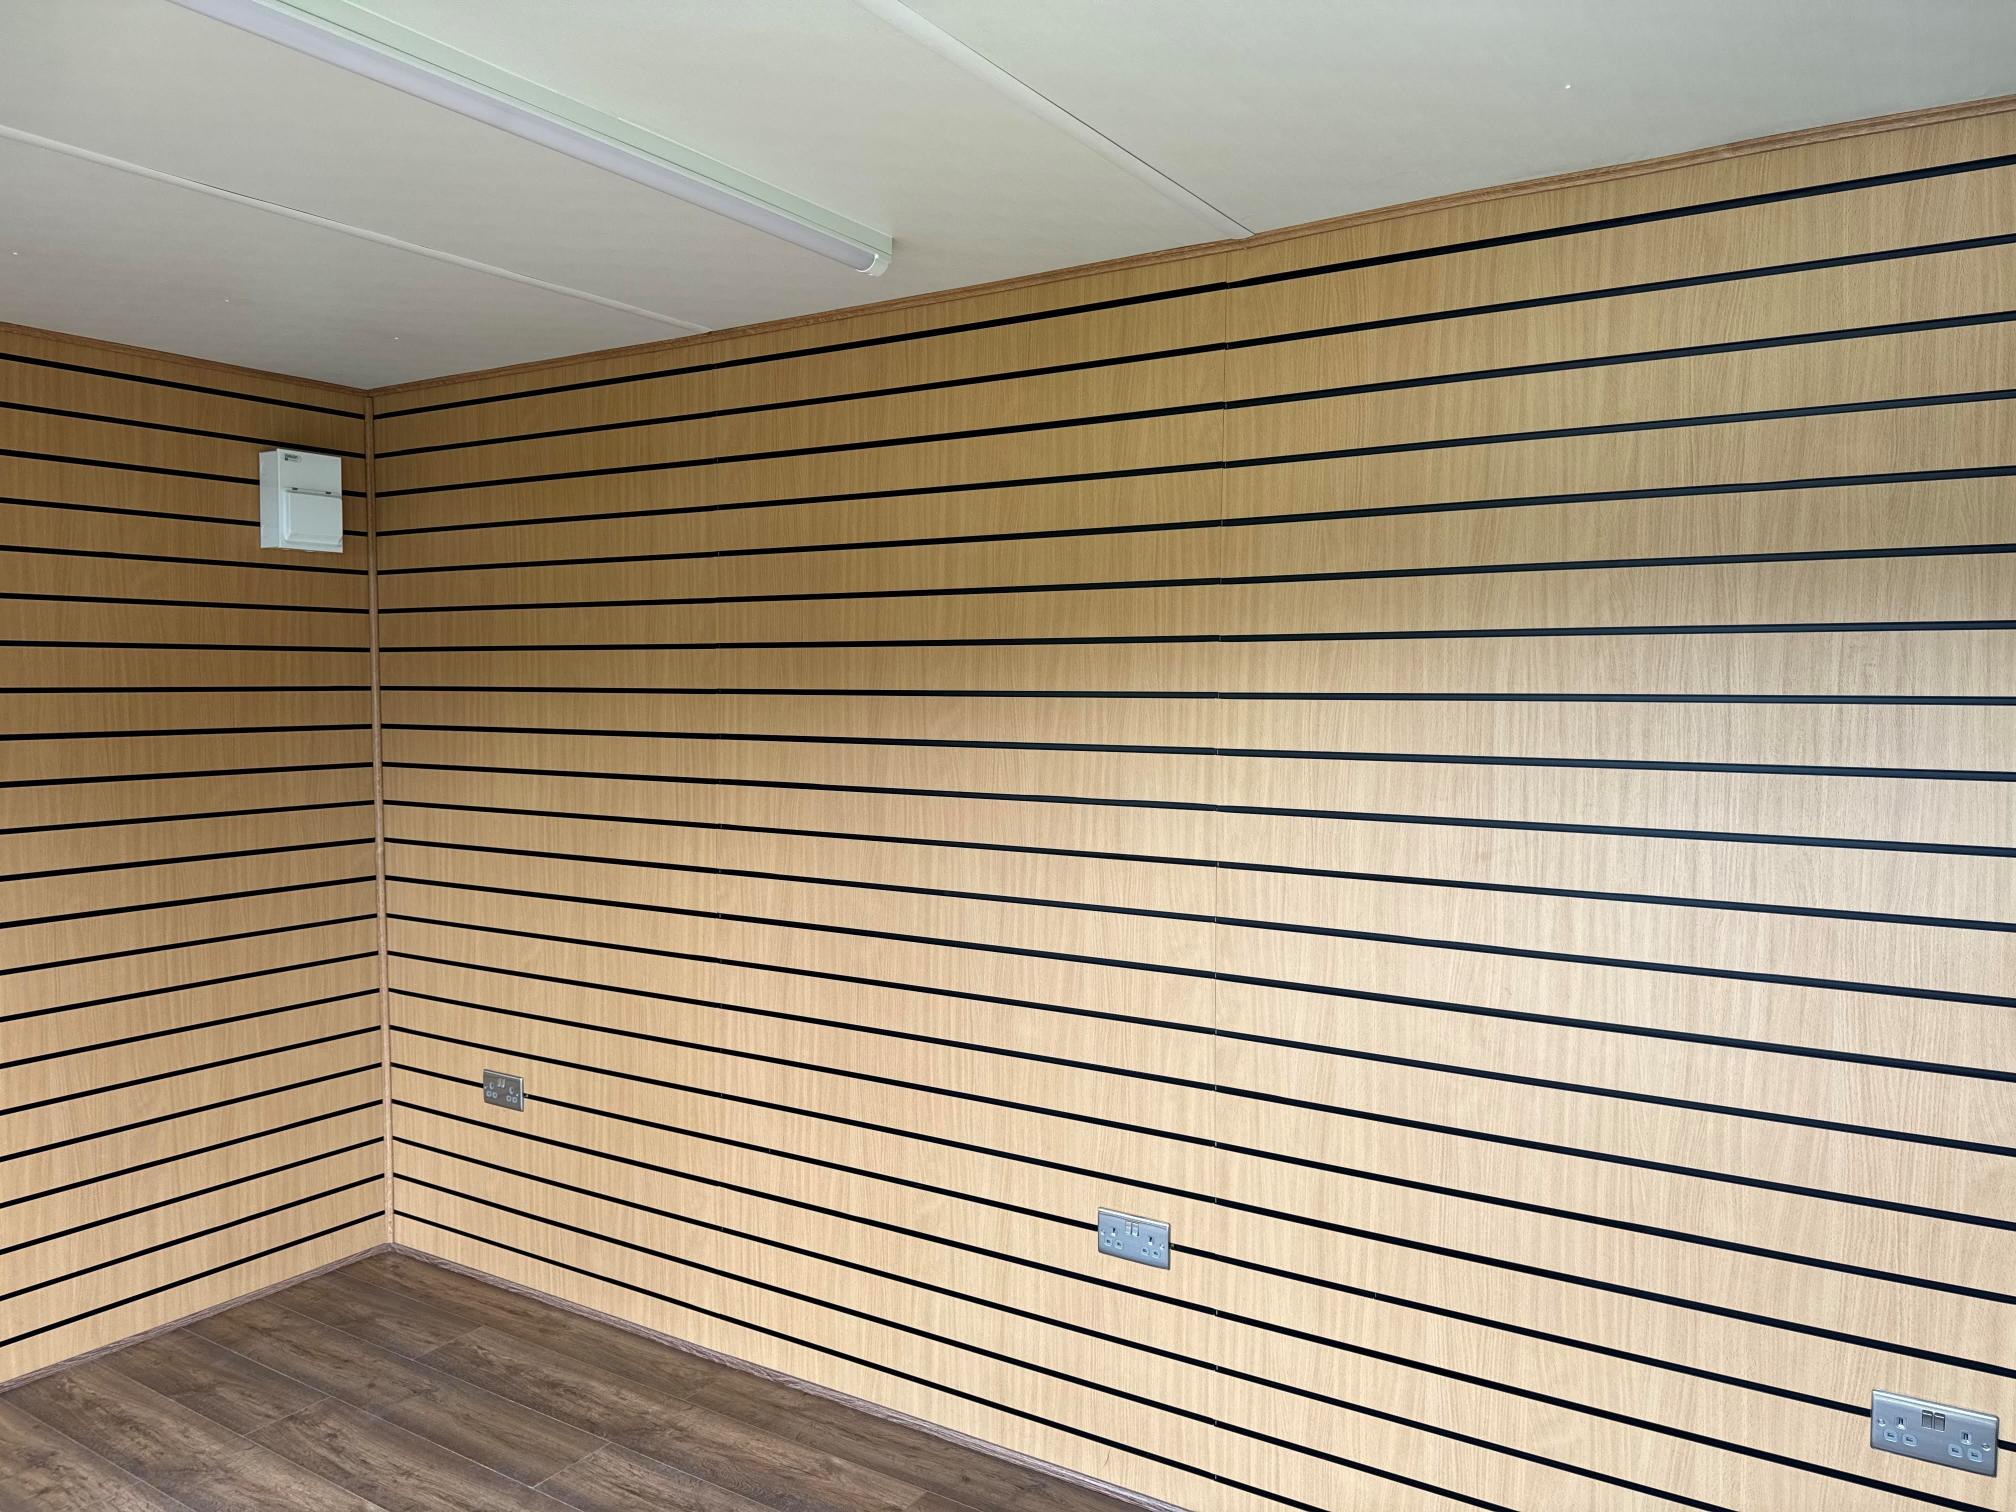
  • Slat Wall for retail fixings and Merchandise

  • Electric Chrome Sockets, led lighting and heating.

  • Laminate Flooring

  • 12 months Warranty

  • Maintenance call out package included

  • Less than 2 years old

  • Still in Brand New Condition

Location: Nationwide

POA

Not Available for Hire

Call for an instant quote!

32ft x 10ft Jack Leg Cabin

  • Fully refurbished

  • Colour light grey

  • Slate grey anthracite upvc double glazed windows

Location: Nationwide


£15,000

+ VAT

Not Available for Hire

Call for an instant quote!

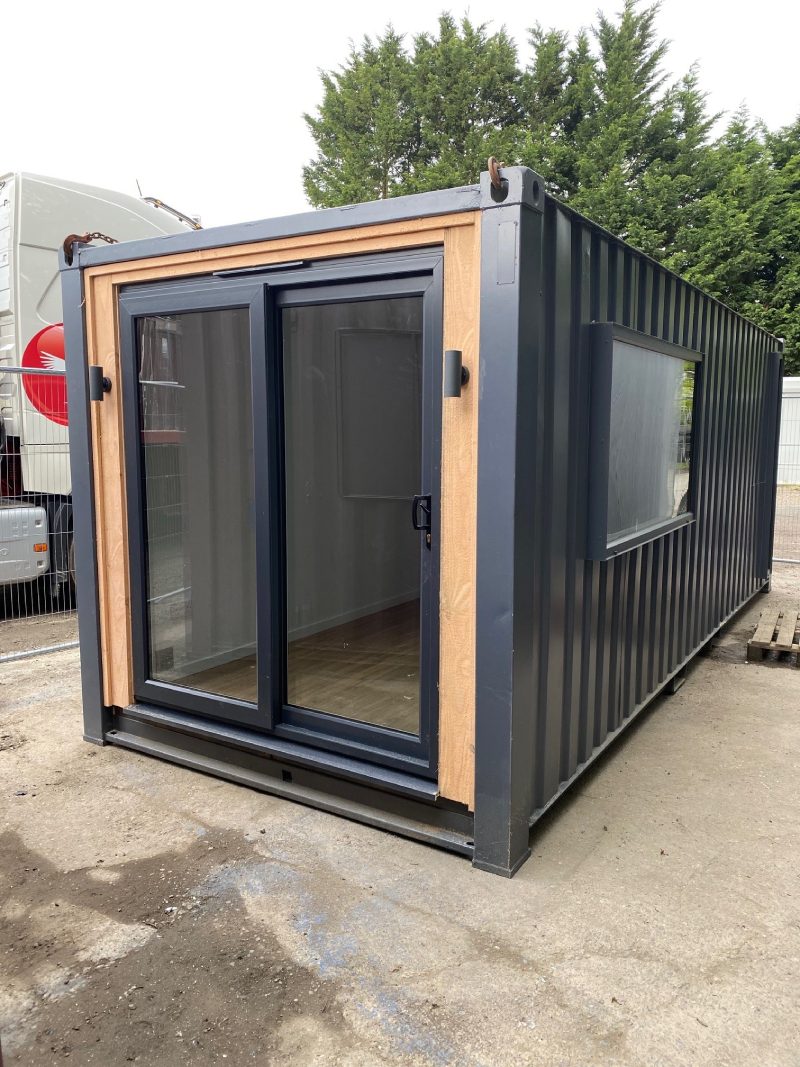
20ft x 8ft Container Office

  • Fully Insulated with electric sockets, spot lighting, and heating

  • Wood Flooring

  • UPVC Sliding Door + Windows

  • Lead Time for build 6-8 weeks

Location: Nationwide


£12,995.00

+ VAT

Not Available for Hire

Call for an instant quote!

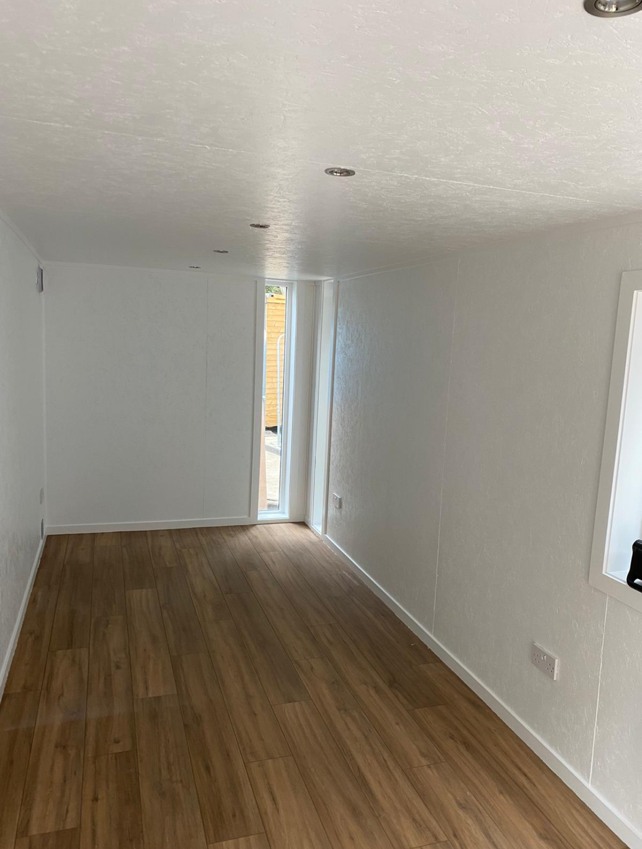
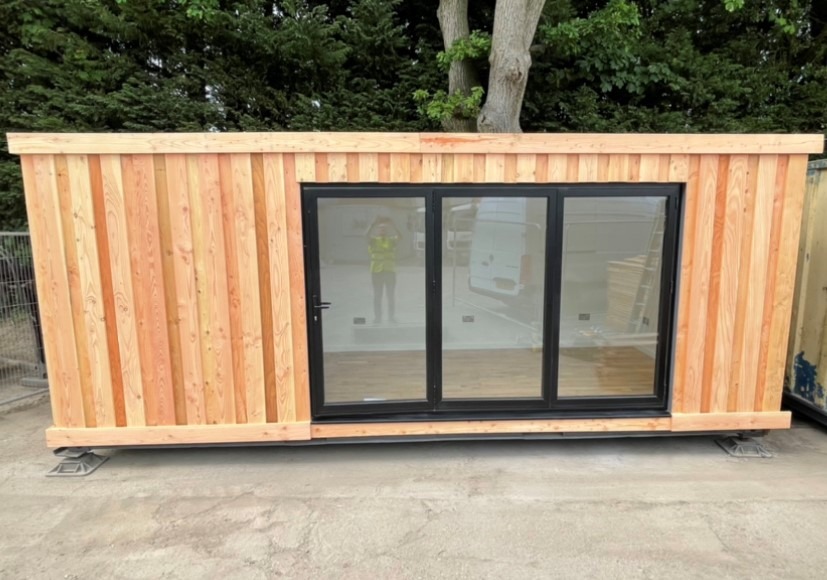
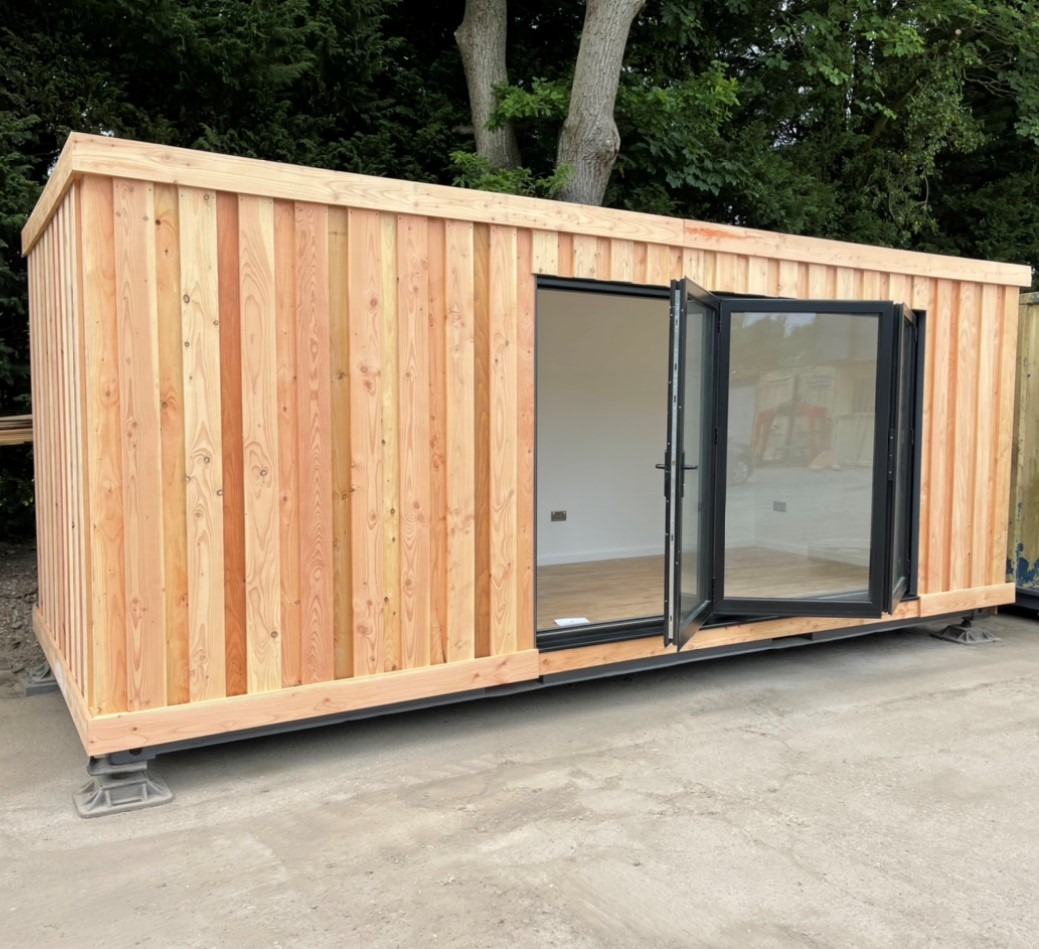
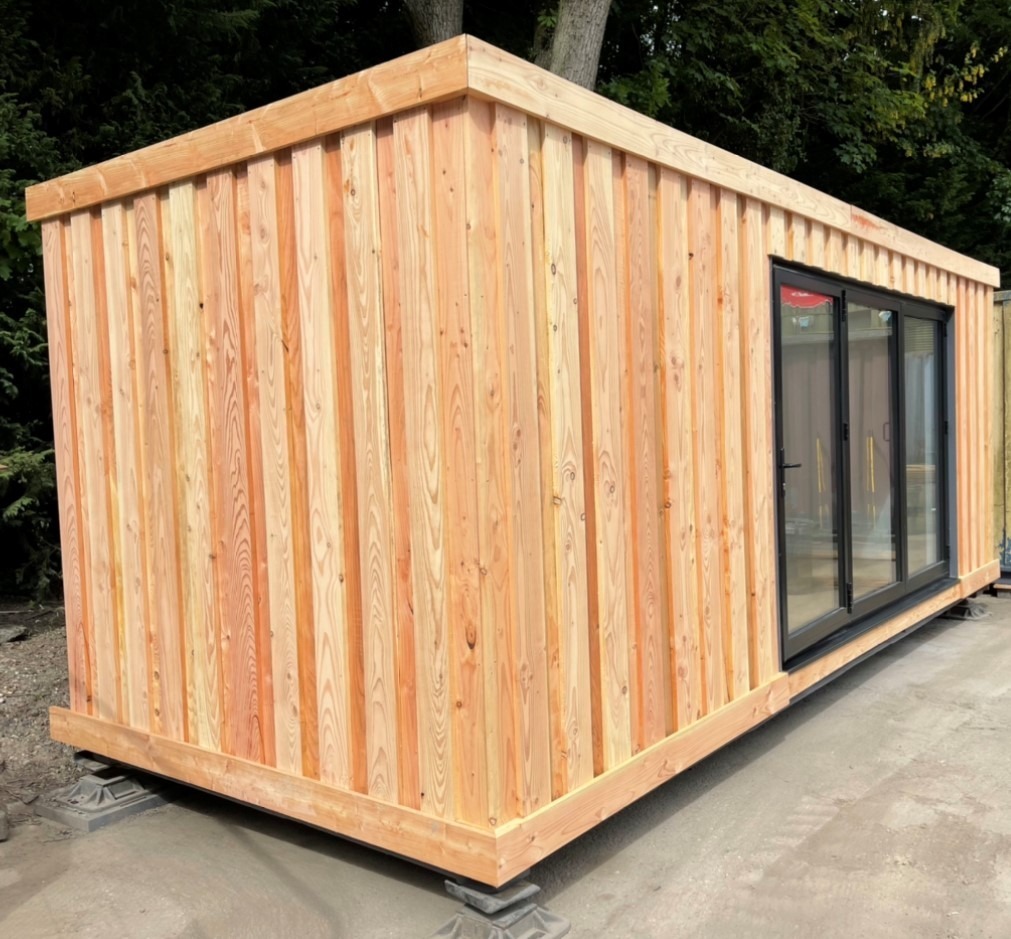
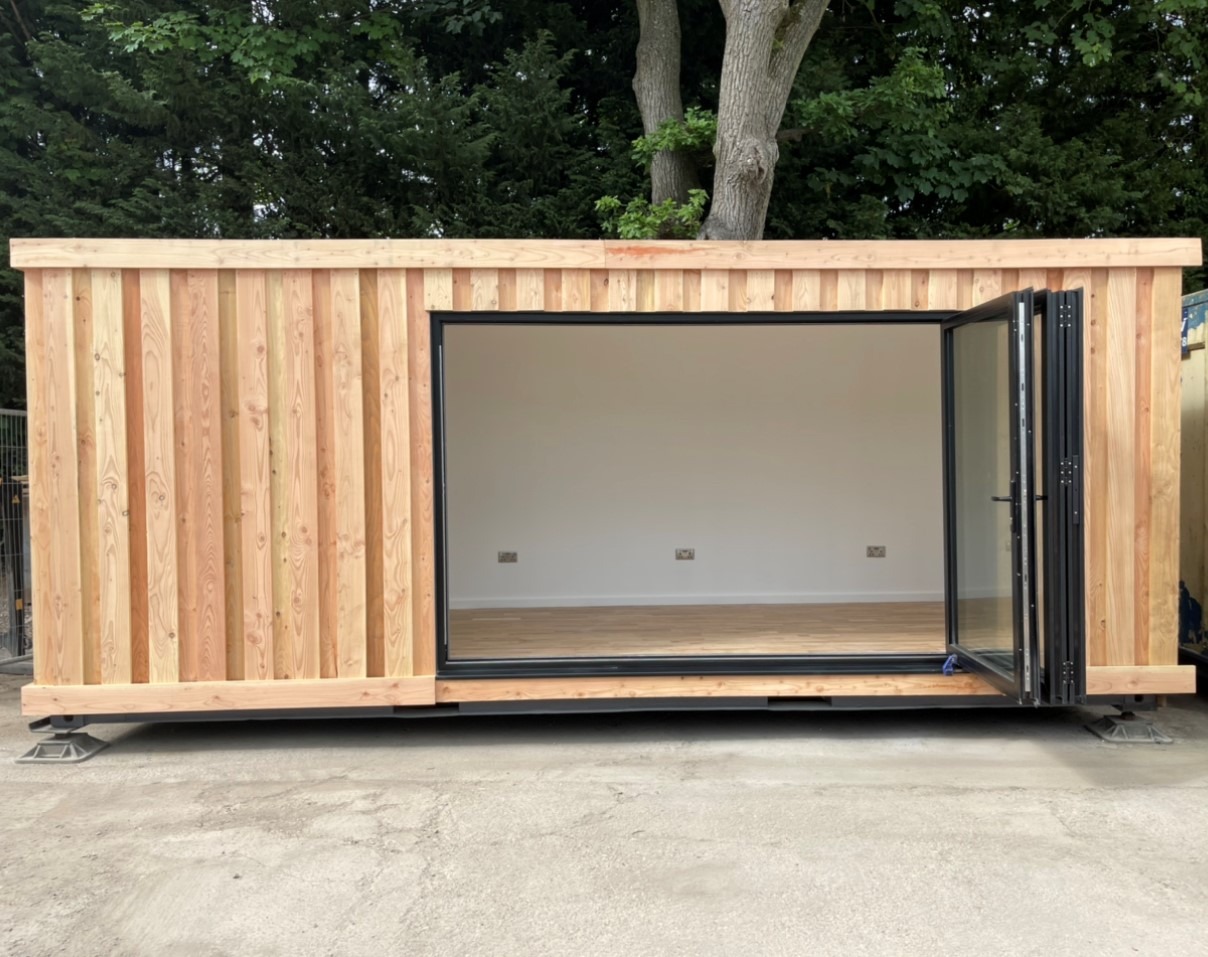
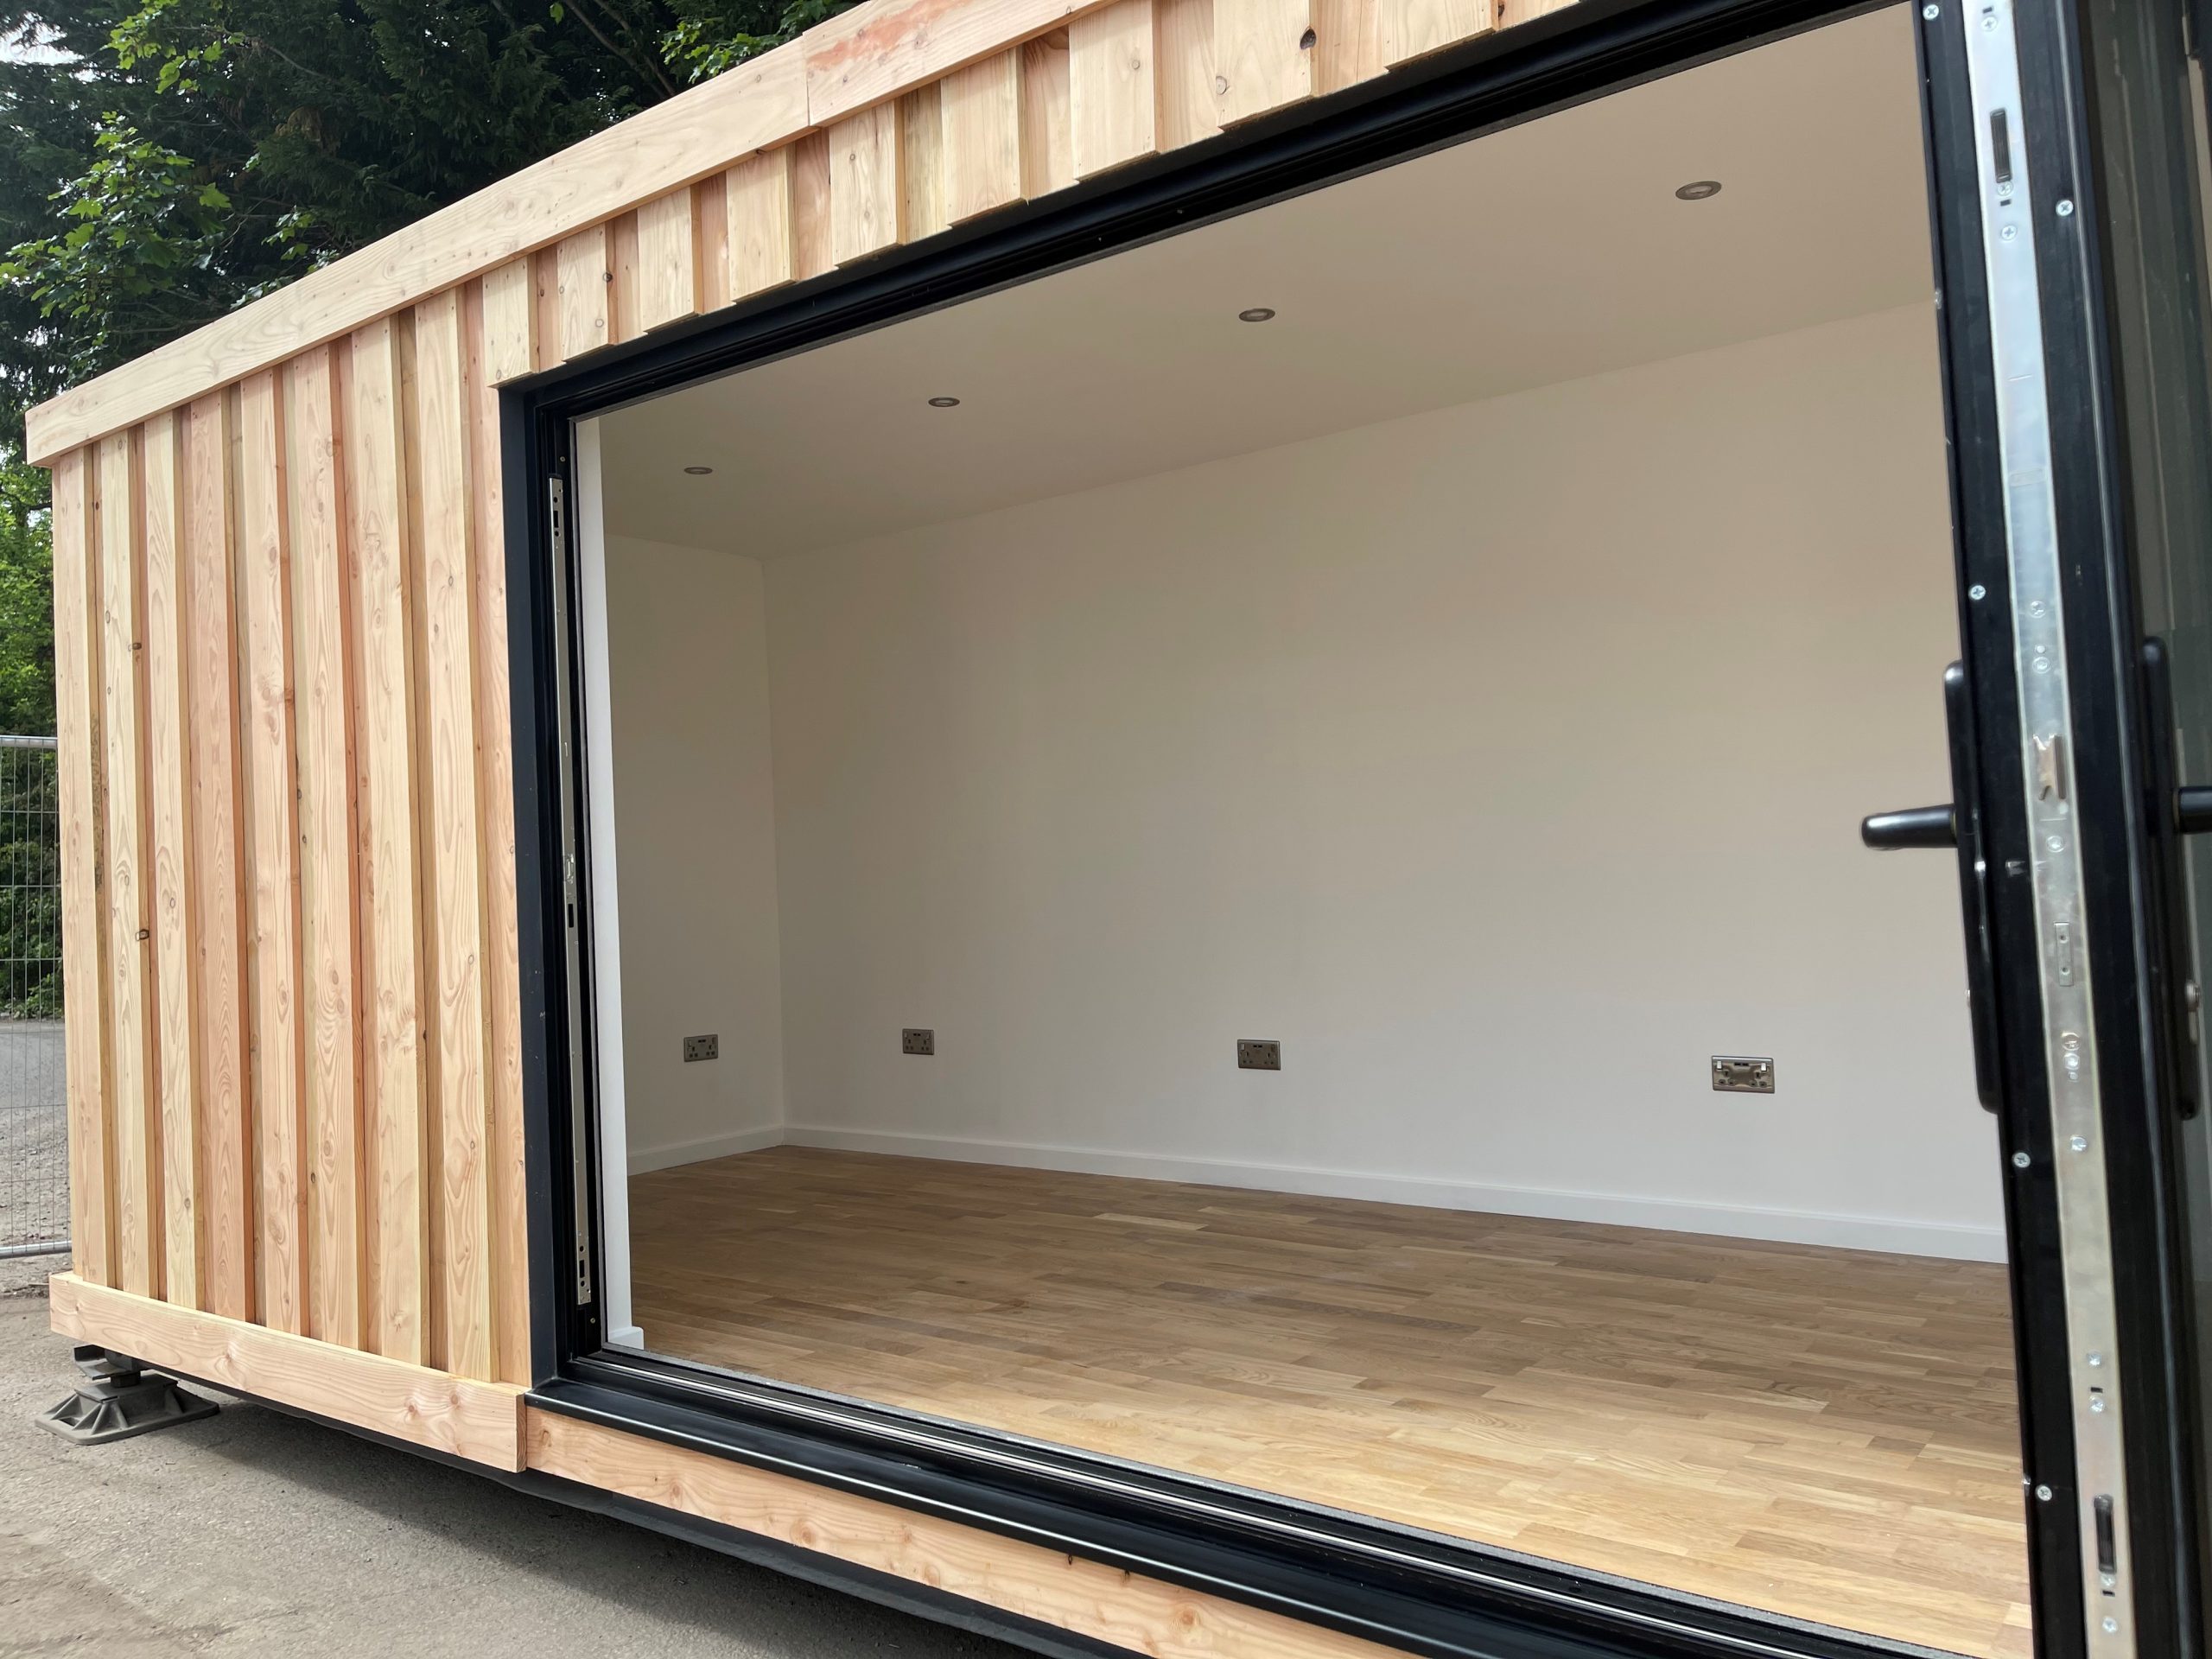
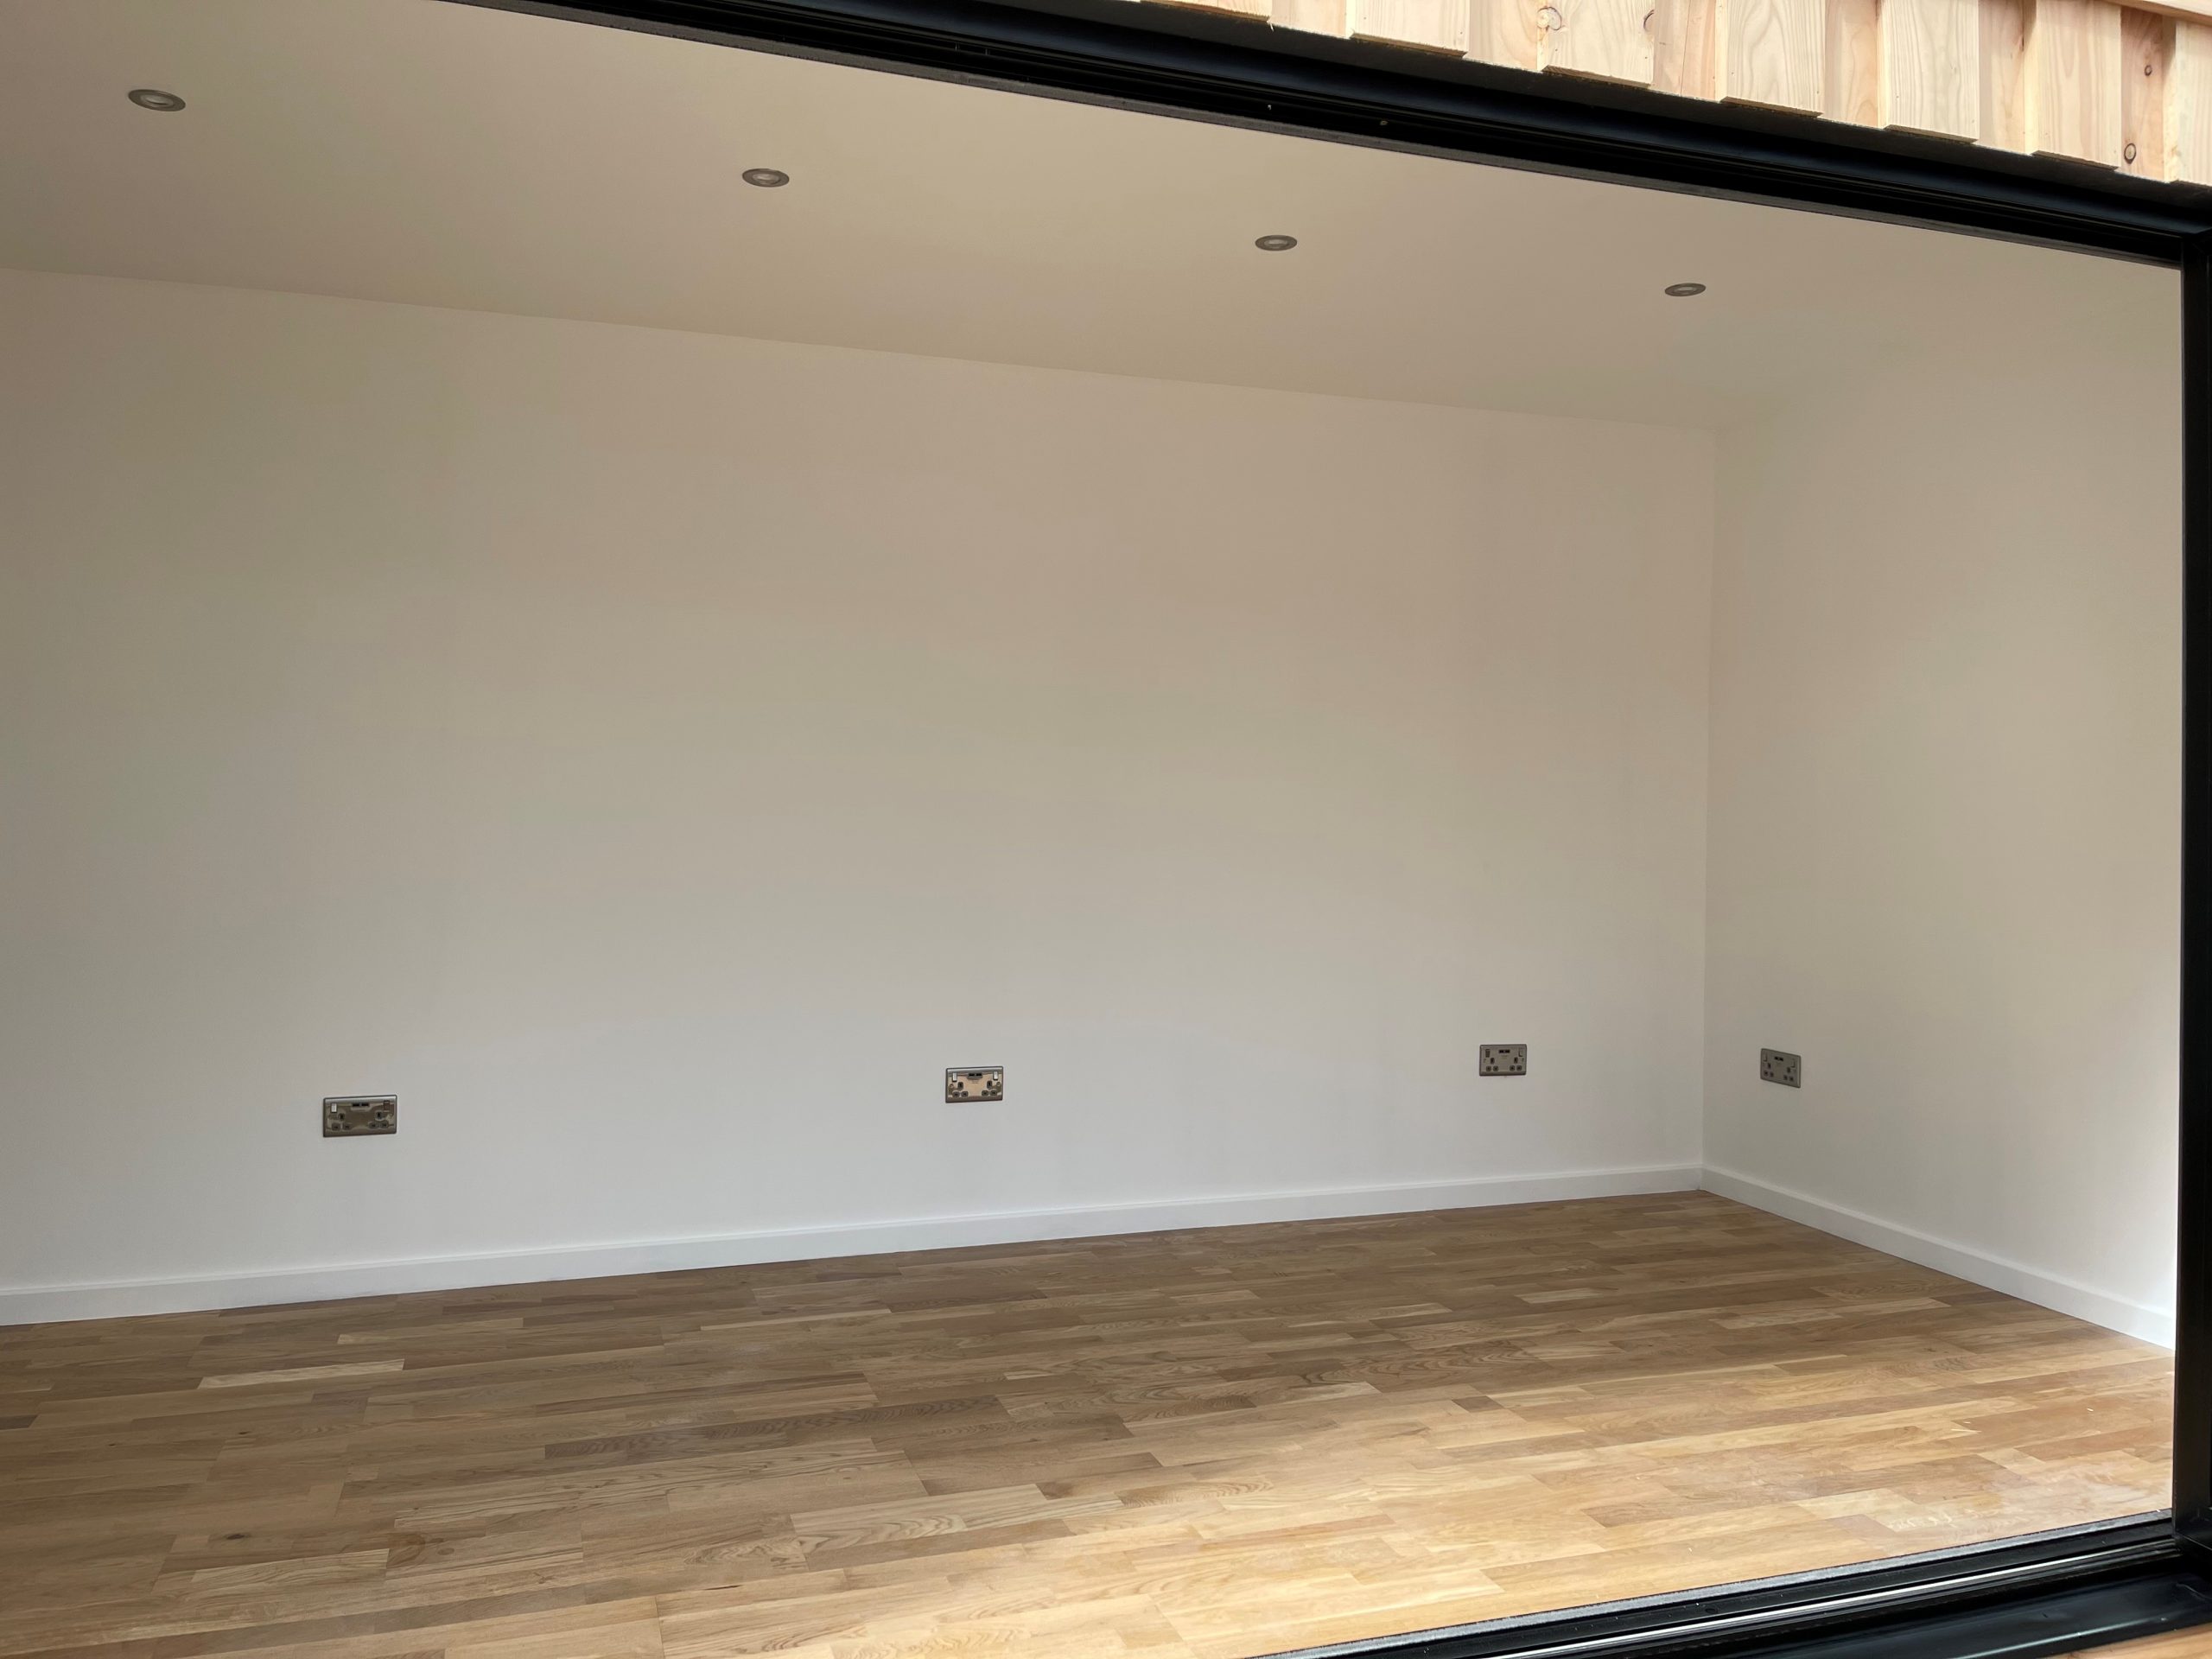
20ft x 8ft Container Office

  • Fully Insulated with electric sockets, spot lighting, and heating

  • Wood Flooring

  • Aluminium Bi Fold Doors

  • Fully wrapped in larch cladding

  • Lead Time for build 6-8 weeks

Location: Nationwide


£16,500.00

+ VAT

Not Available for Hire

Call for an instant quote!

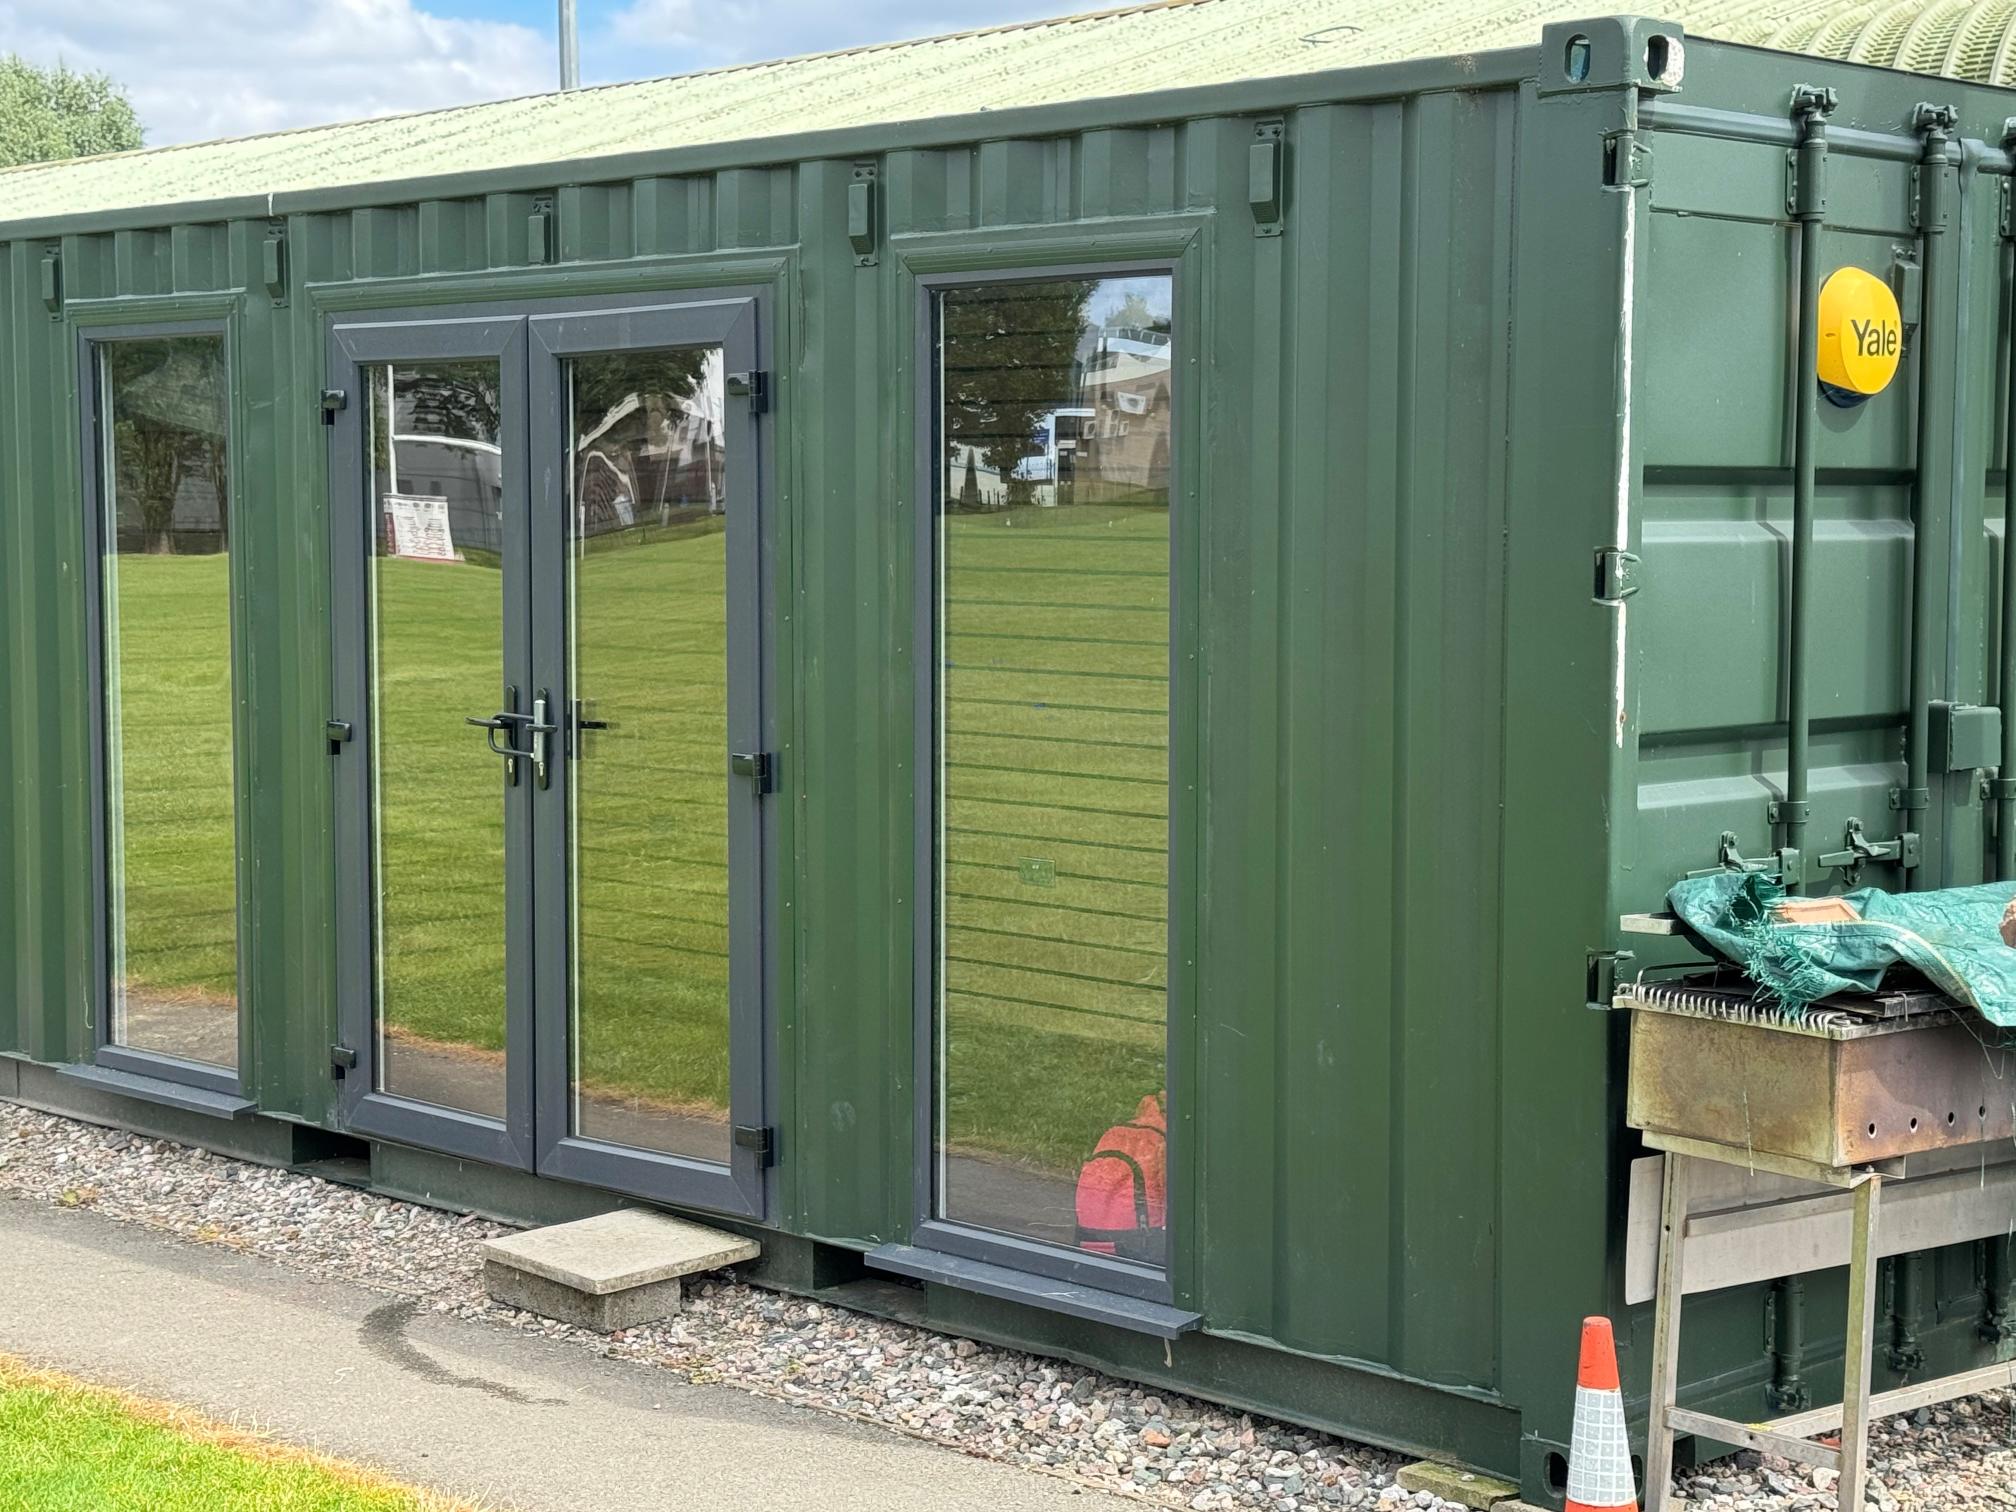
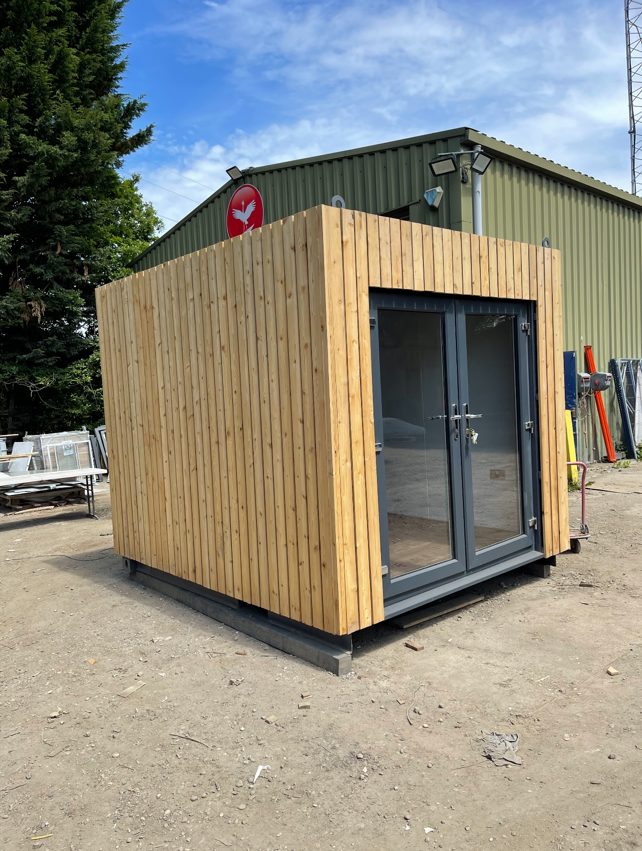
10ft x 8ft Container Conversion

  • Fully Insulated with electric sockets, spot lighting, and heating

  • Wood Flooring

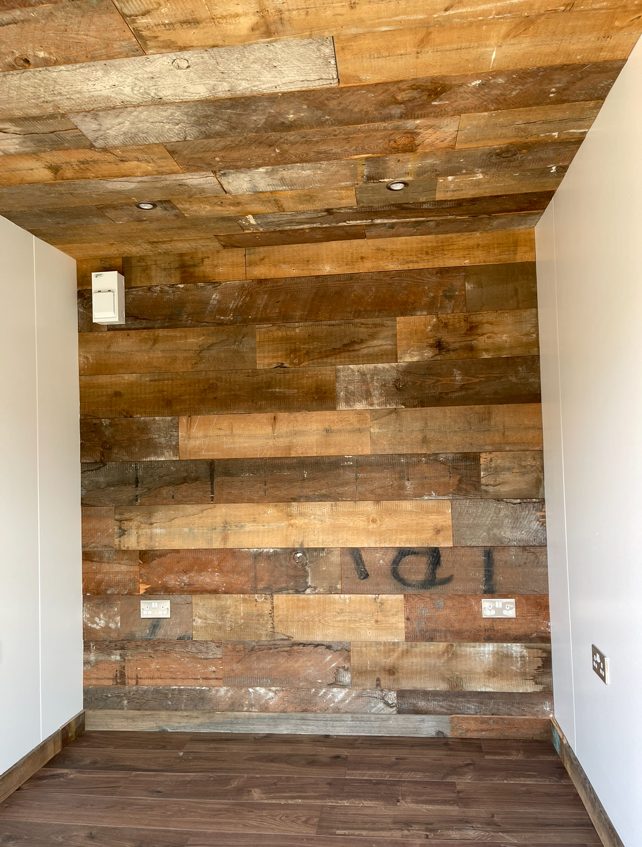
  • Feature Clad Wall and Ceiling

  • UPVC Double glazed French Doors

  • Fully wrapped in larch cladding

  • Lead Time for build 6-8 weeks

Location: Nationwide


£12,500.00

EX VAT

Not Available for Hire

Call for an instant quote!

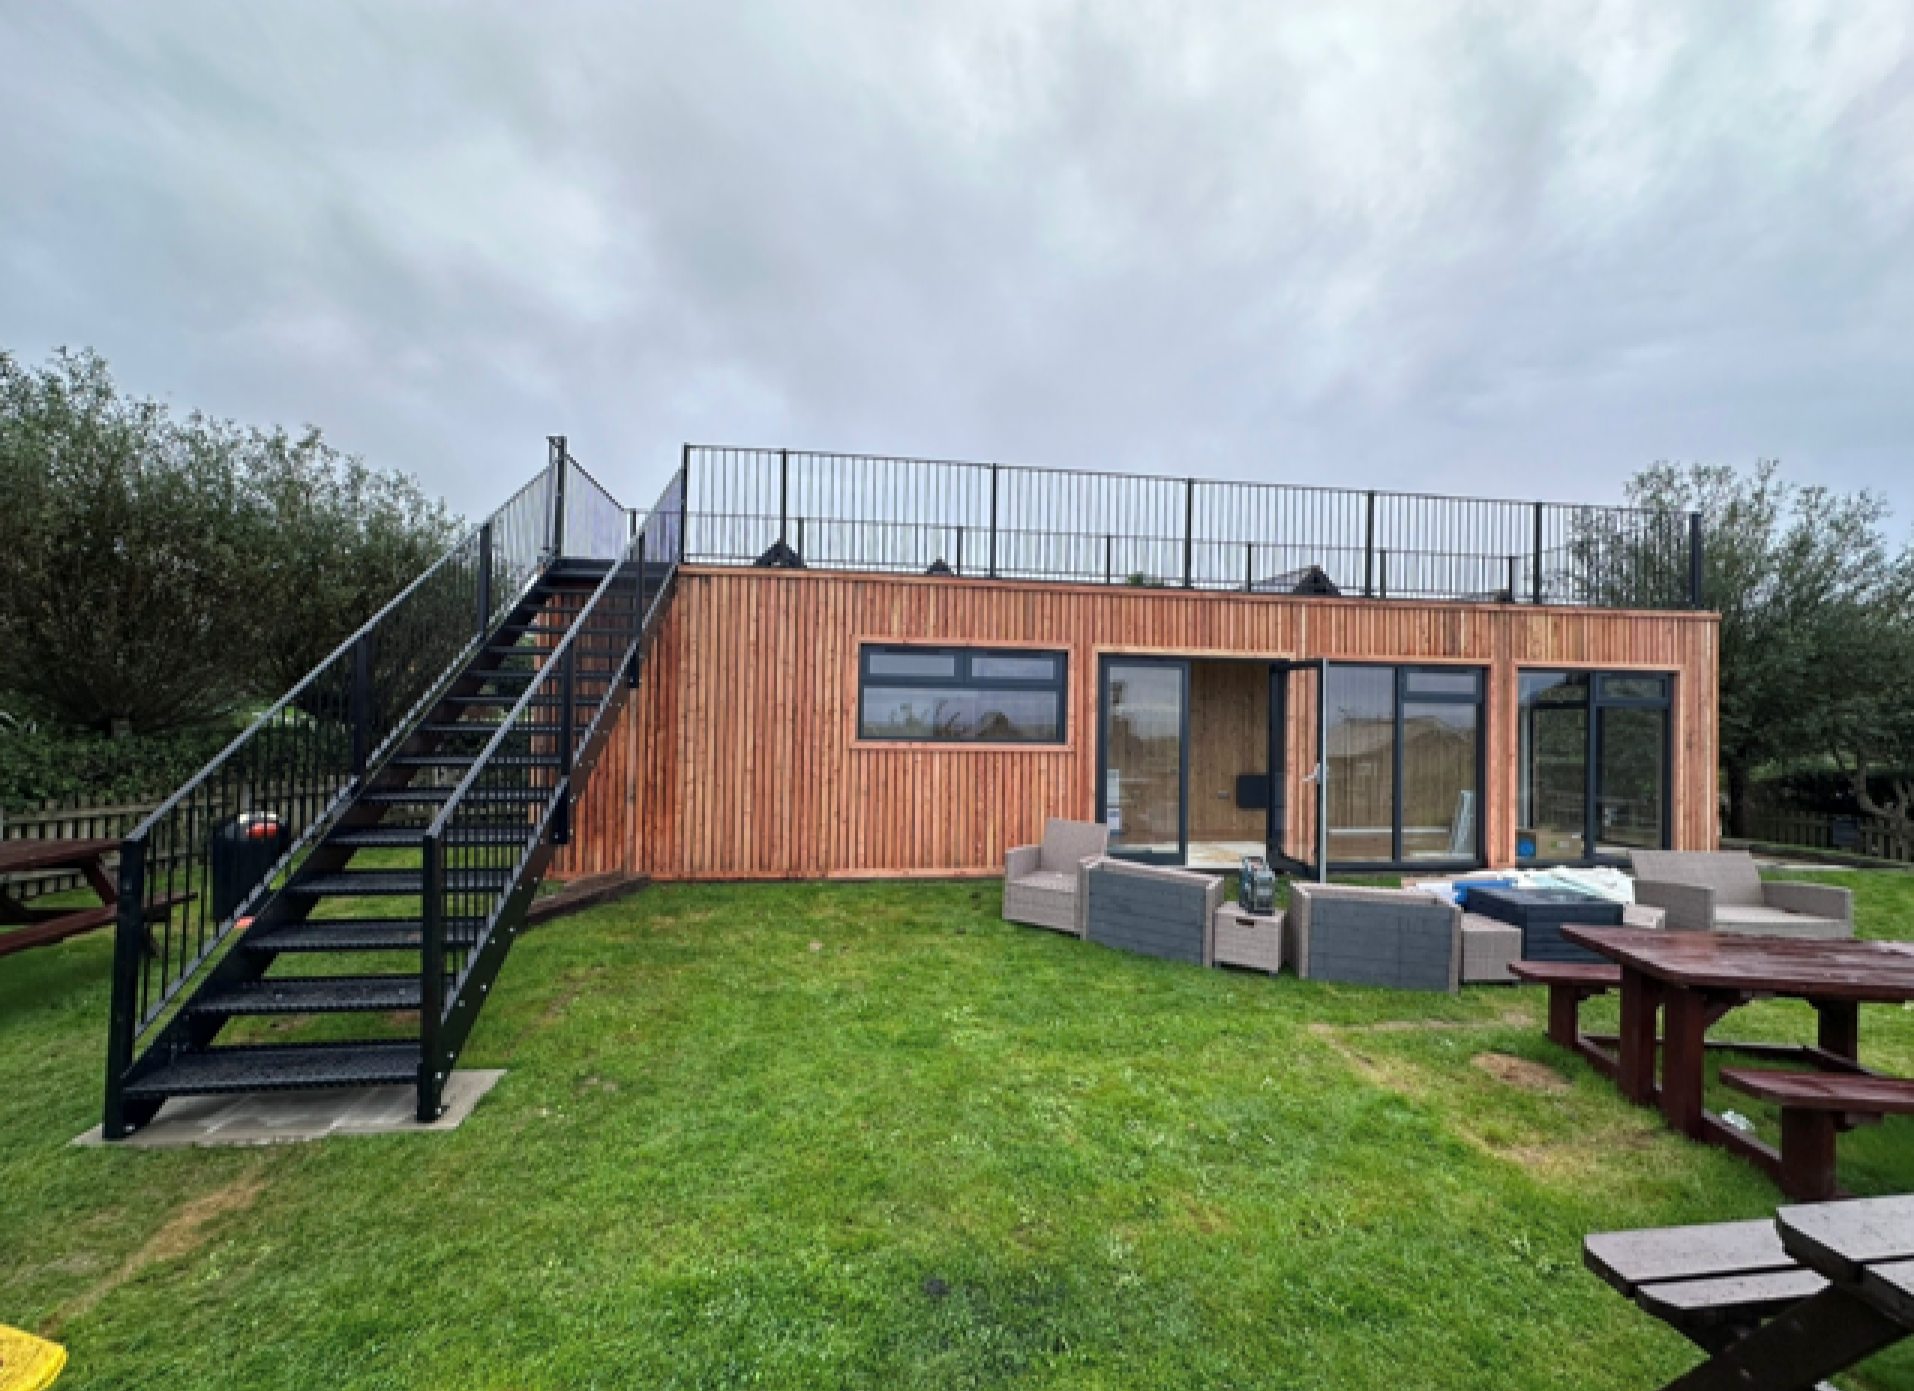
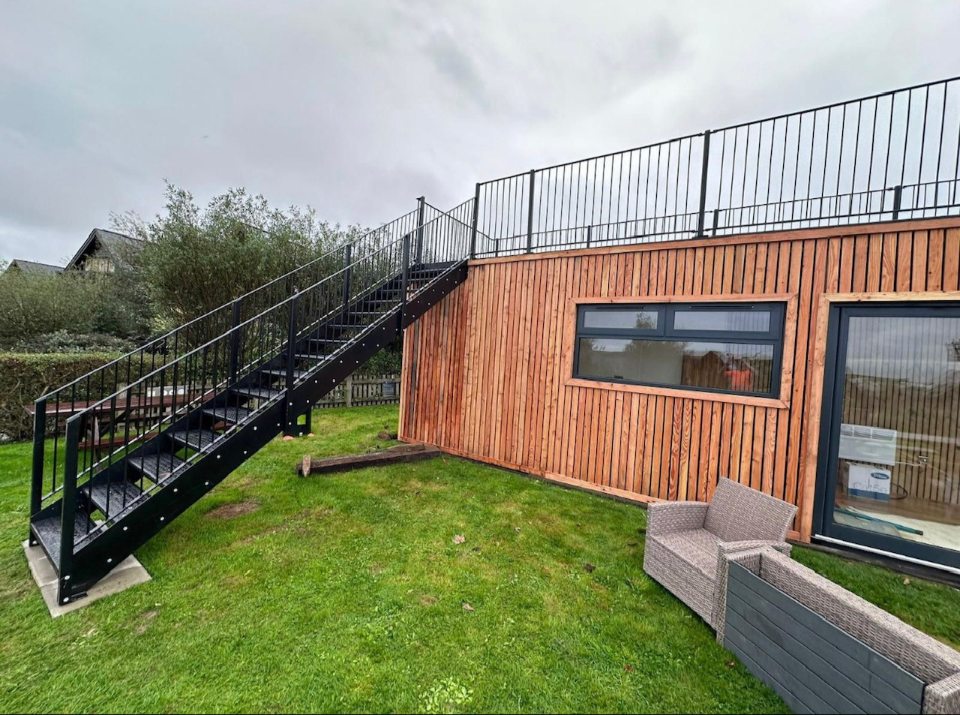
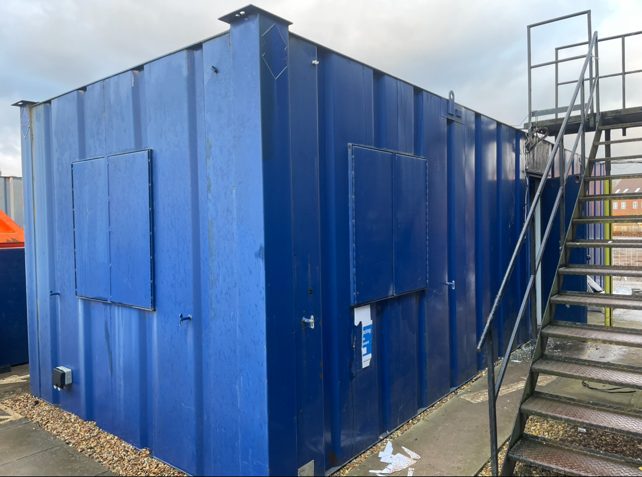
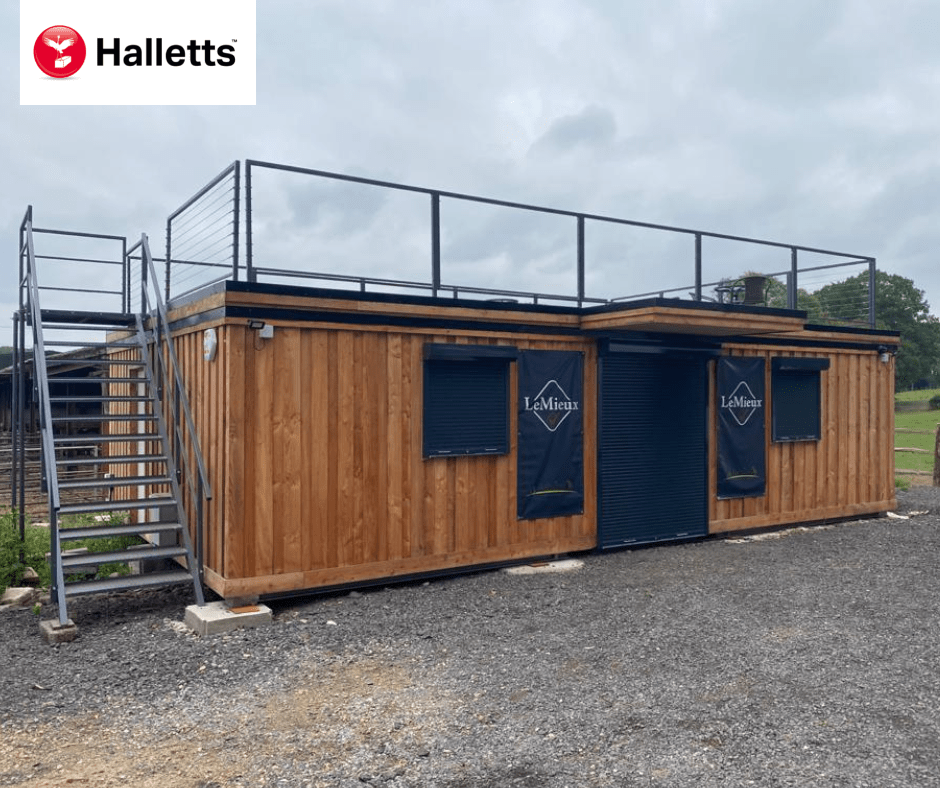
40ft x 8ft Rooftop Container Bar

  • 40ft x 8ft Rooftop Container Bar
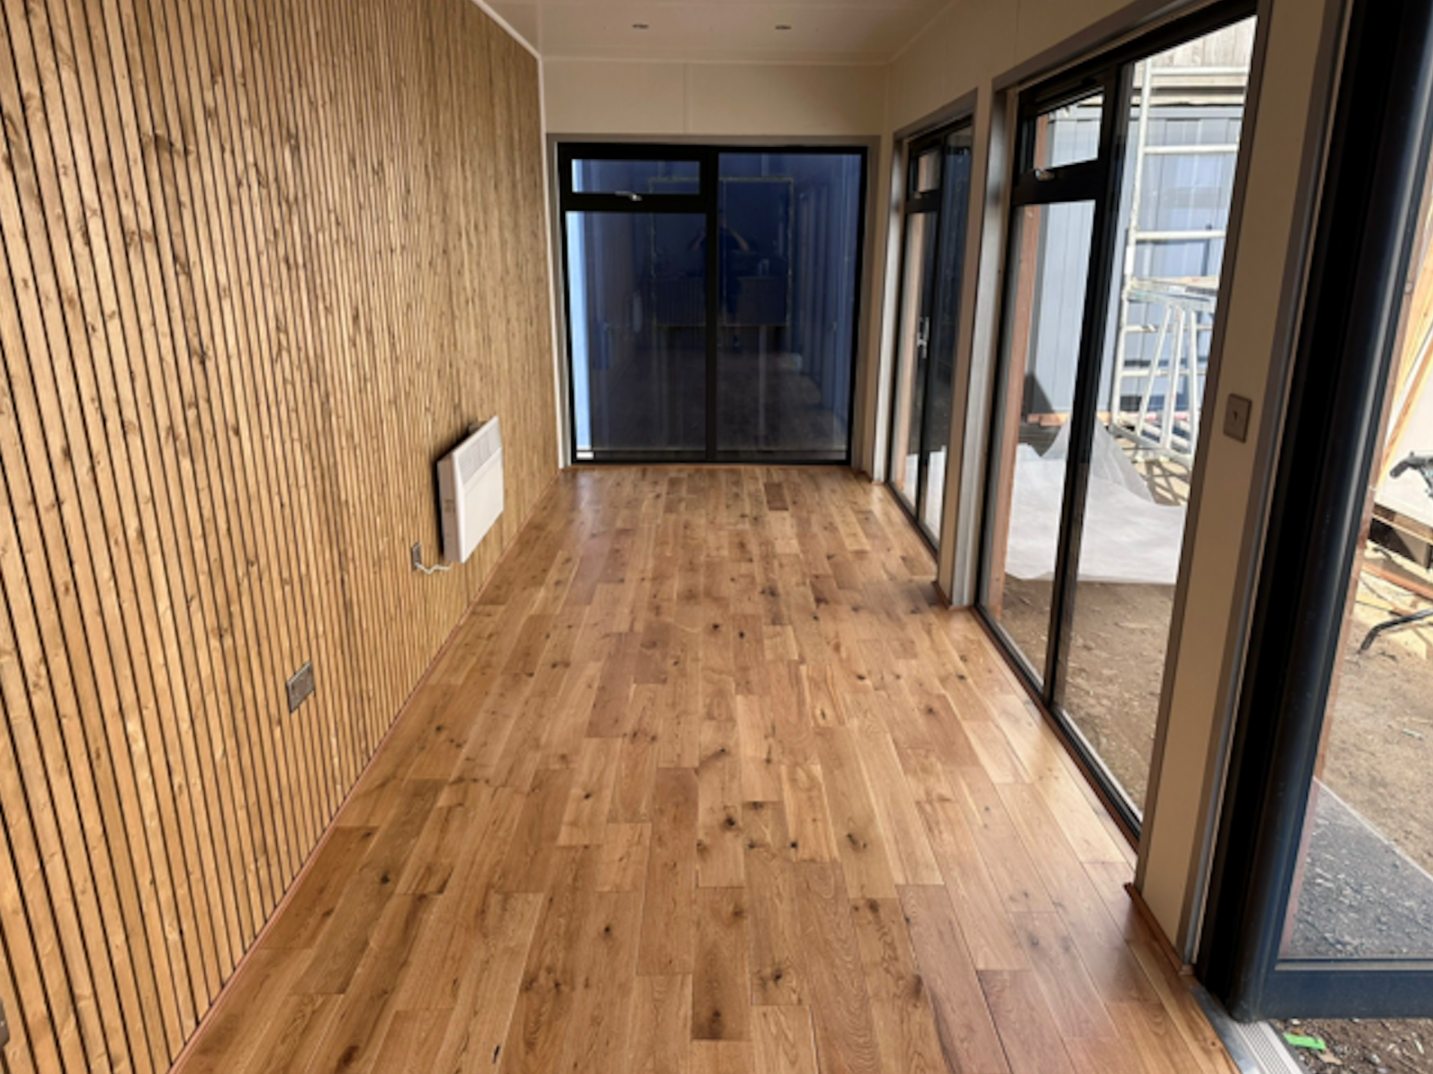
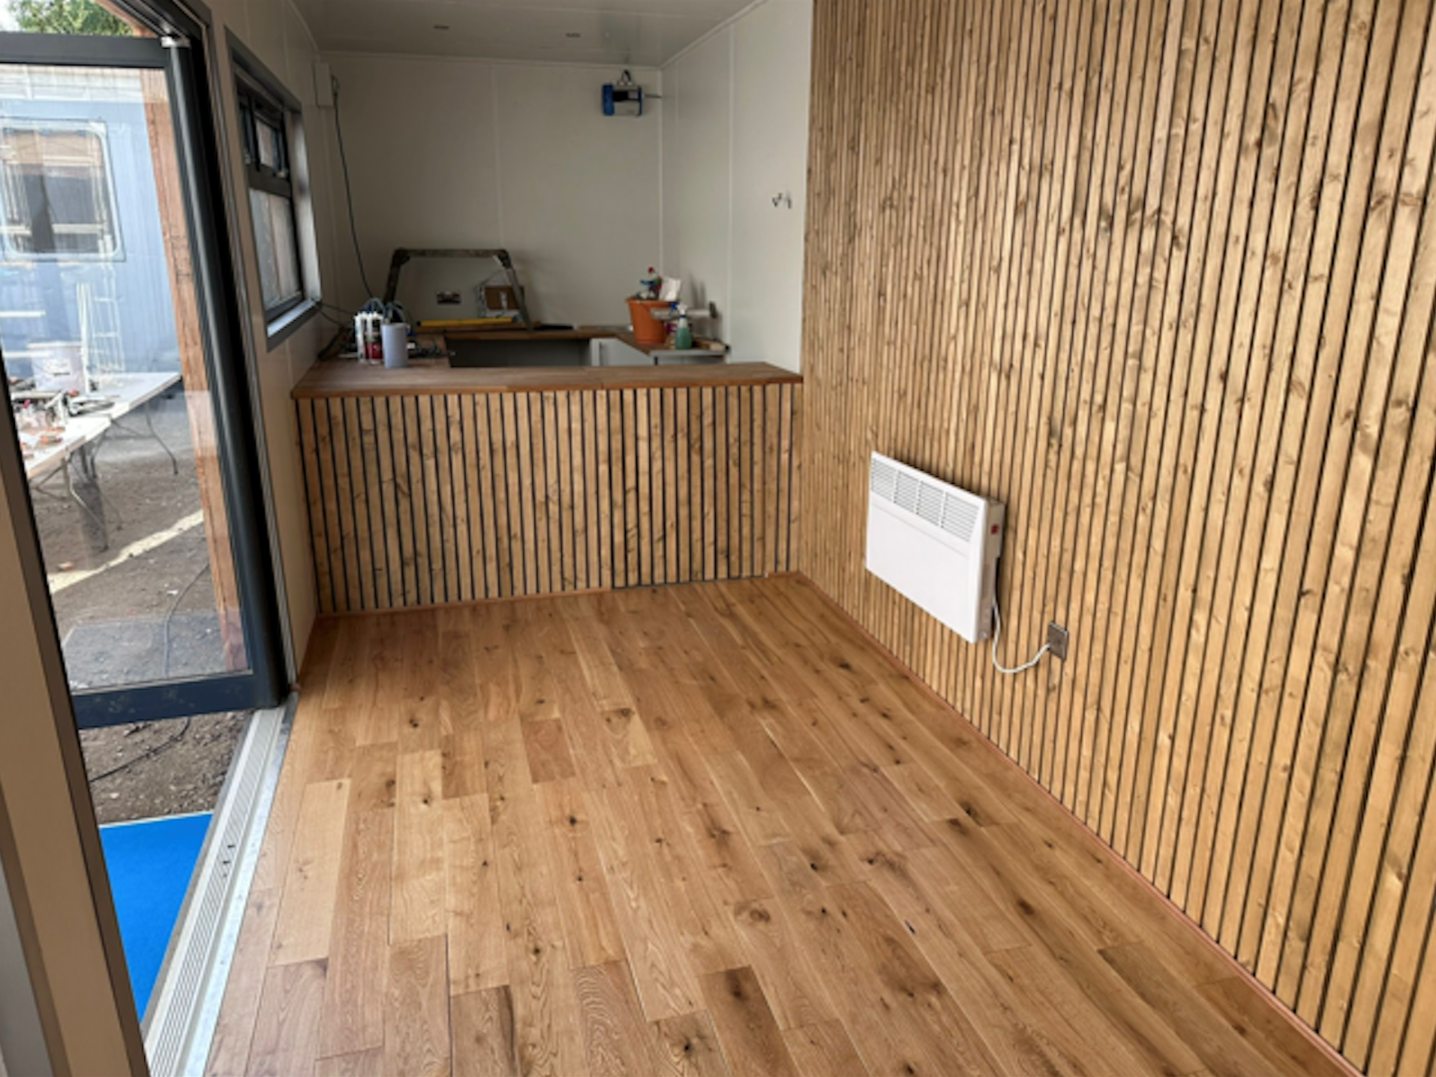
  • Fully Insulated with electric sockets, spot lighting, and heating
  • Built in Bar
  • Wood Flooring
  • Feature Larch Clad Wall
  • Aluminium double glazed premium windows and double French doors
  • Fully wrapped in larch cladding
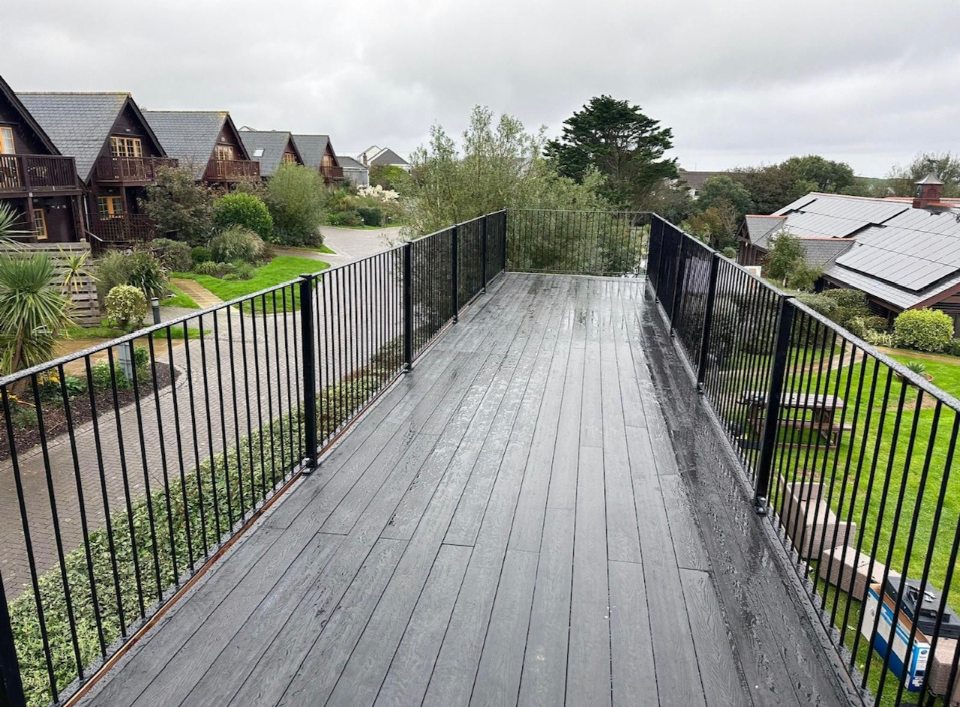
  • Steel staircase up to Rooftop terrace with full surrounding steel balustrade
  • Double container doors leading to cool room with Air Conditioning unit.
  • Lead Time for build 6-8 weeks

Location: Nationwide


£85,000.00

EX VAT

Not Available for Hire

Call for an instant quote!

  • Fully Refurbished
  • Zinc Roof
  • Colour Light Grey (Other Colour Options Available)
  • New Flooring
  • New Electric Sockets, Lighting and Heating
  • New UPVC Large and Small Windows
  • New Kitchenette with Partition
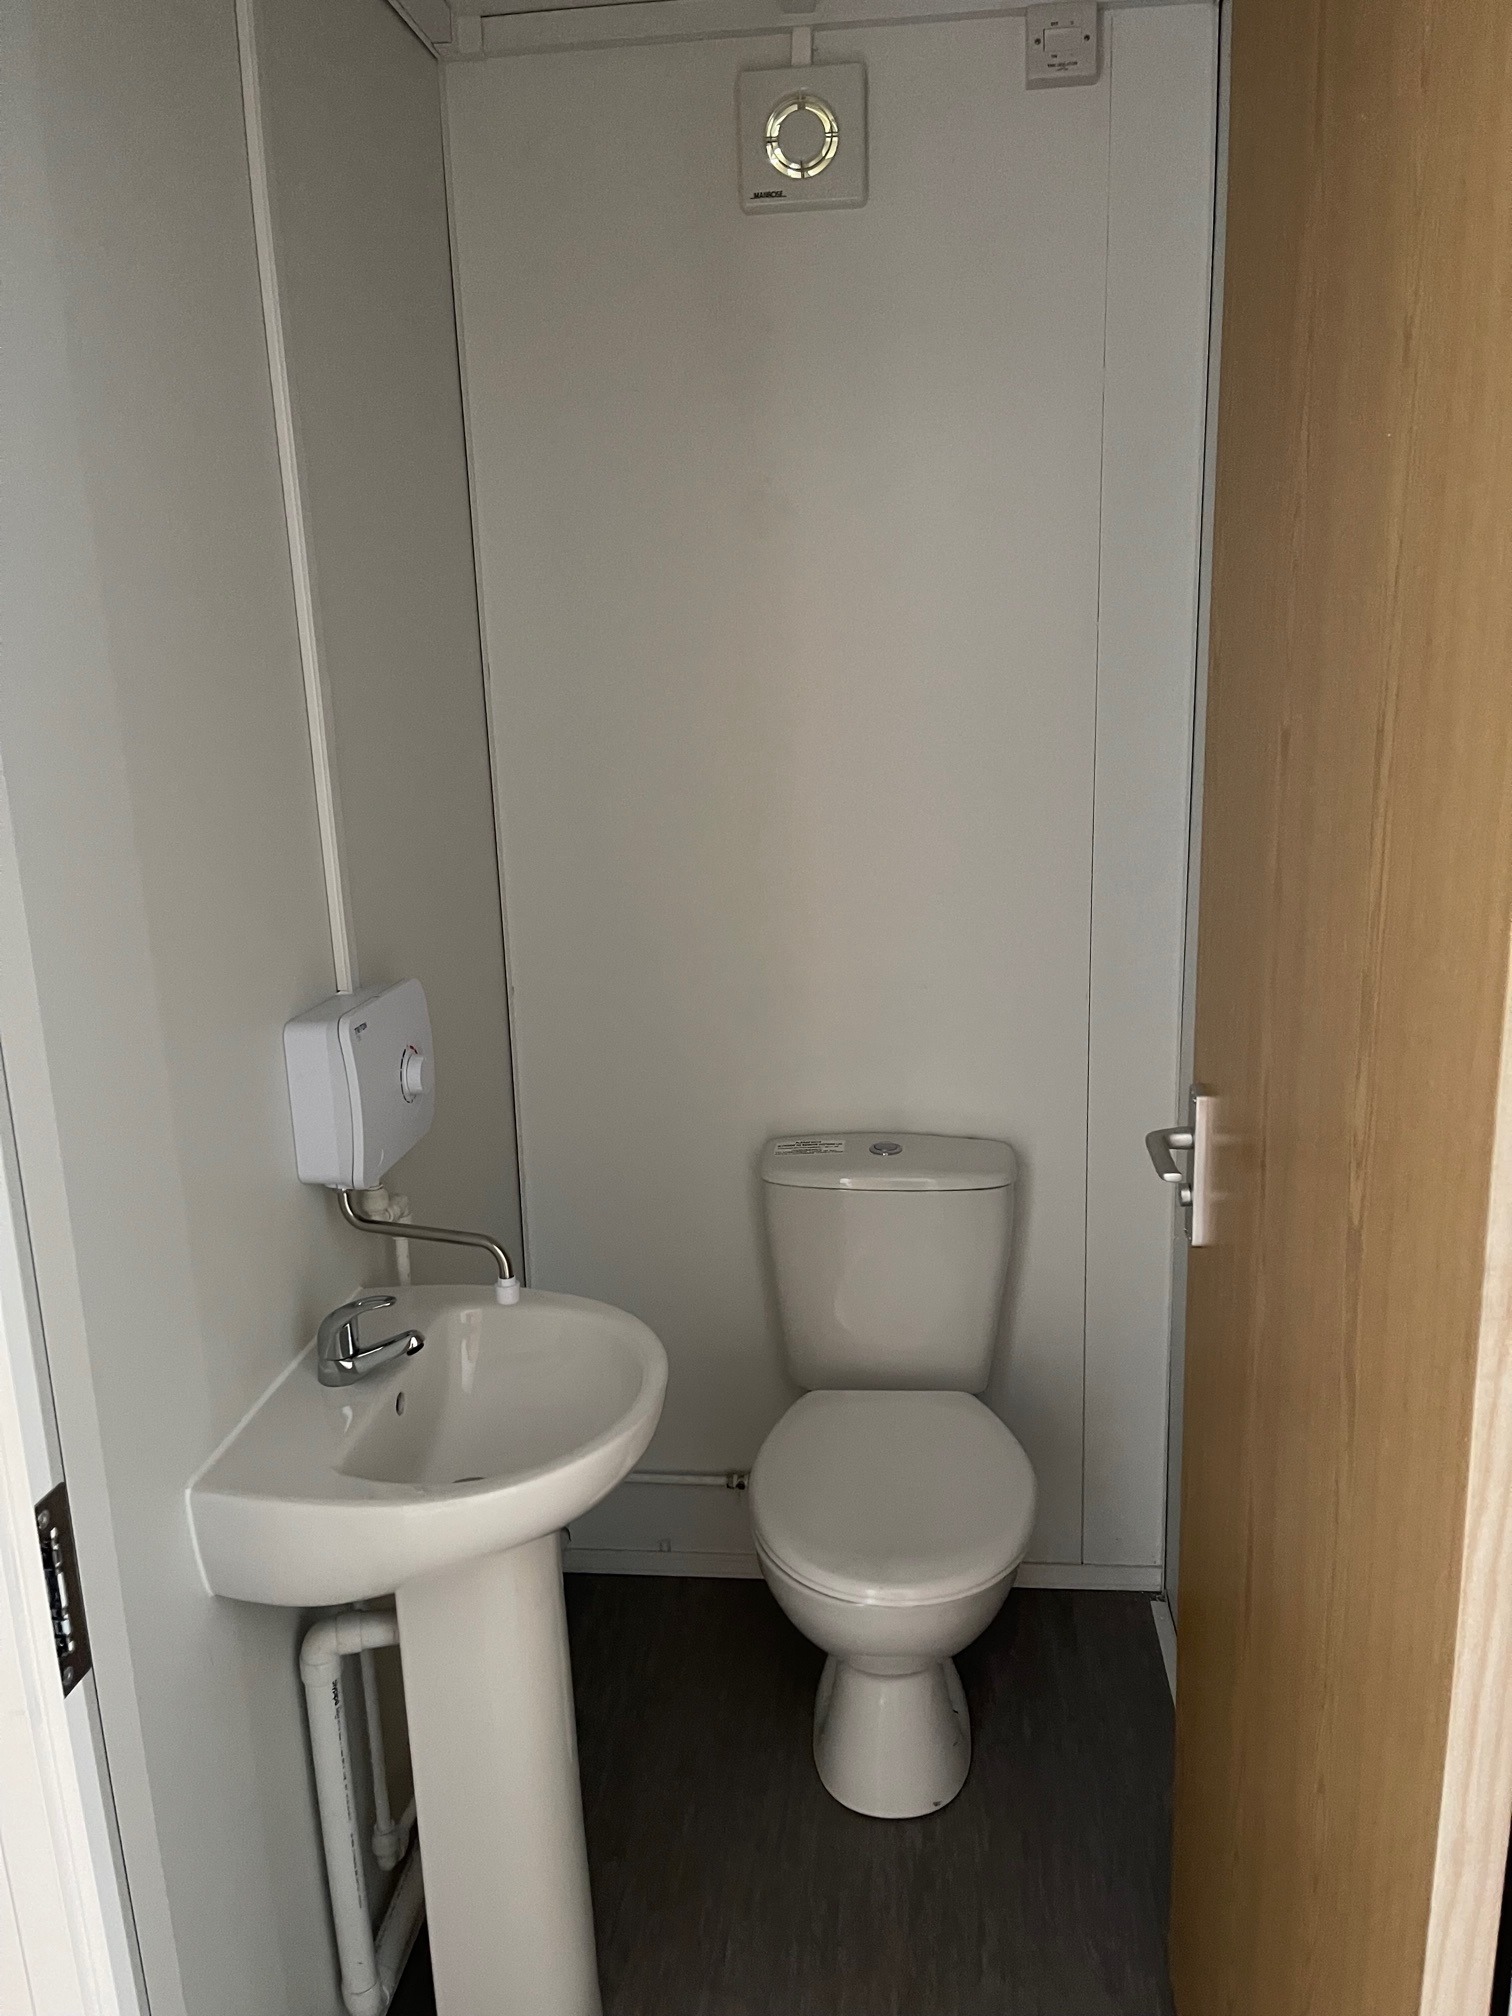
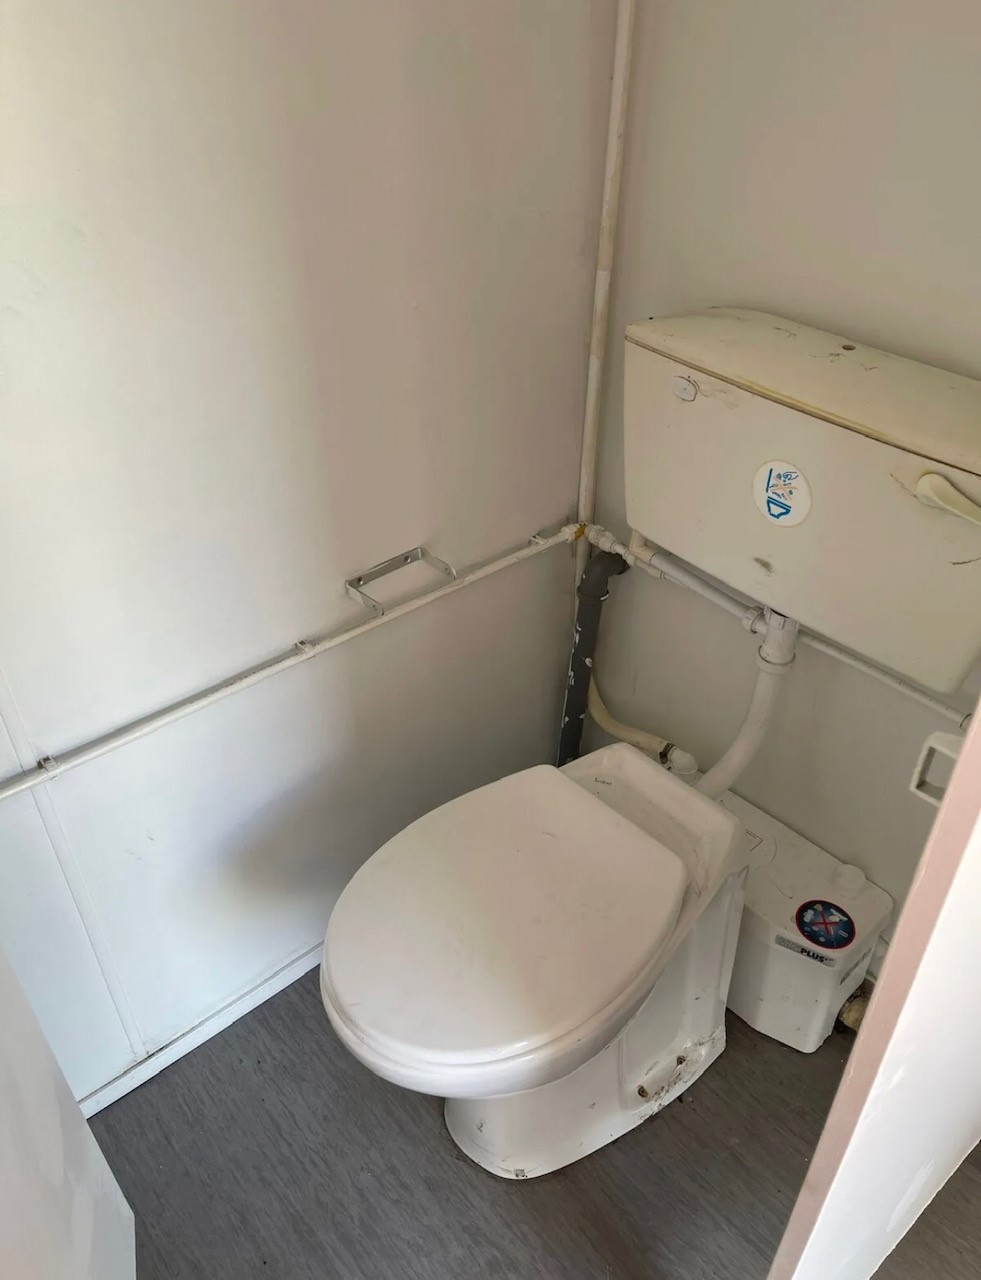
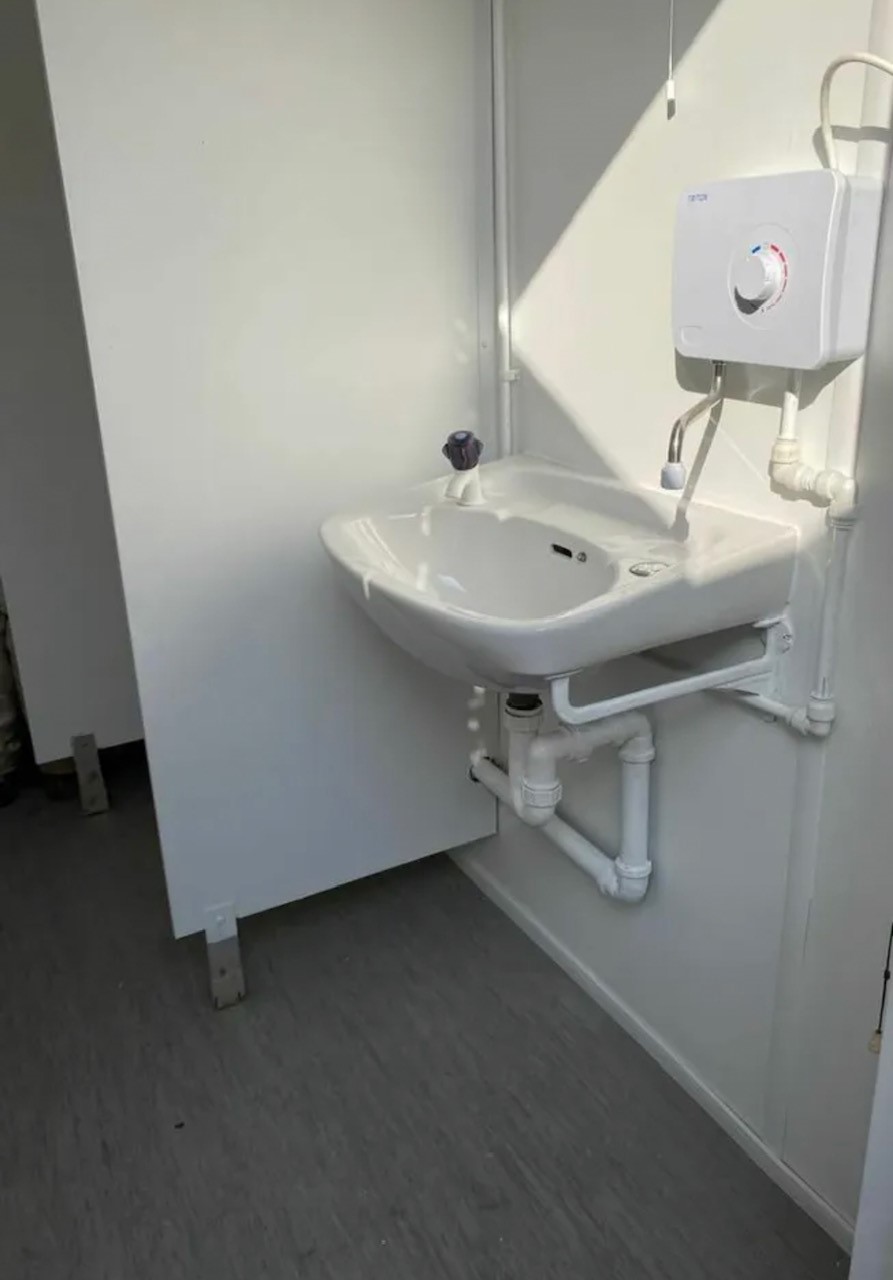
  • New Toilet Room with toilet, Sink, Water Heater and Fan

Location: Nationwide

£18,995

EX VAT

Not Available for Hire

Call for an instant quote!

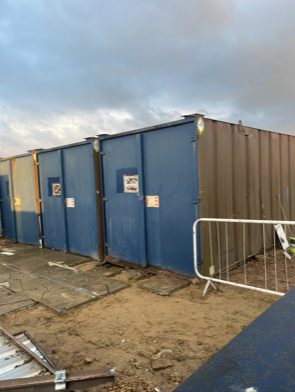
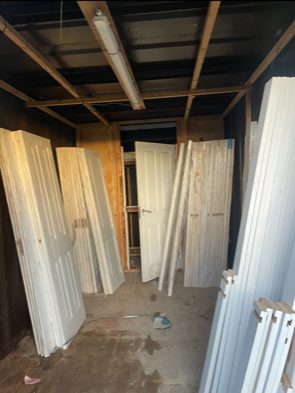
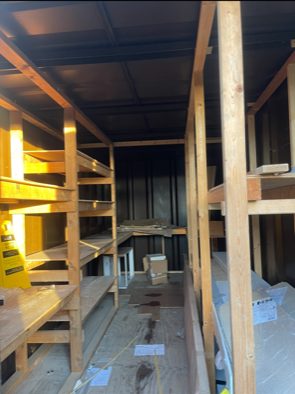
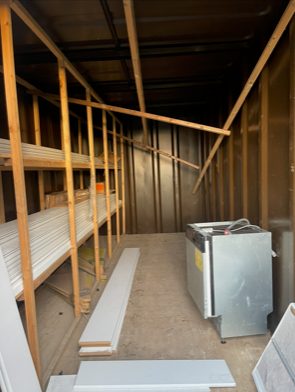
6 x 21ft x 8ft Container Stores

  • Wind and Water Tight
  • Very Good Condition
  • Some have racking inside
  • Floorings all good
  • Contents not included

Location: Nationwide


£1,500

EX VAT

Not Available for Hire

Call for an instant quote!

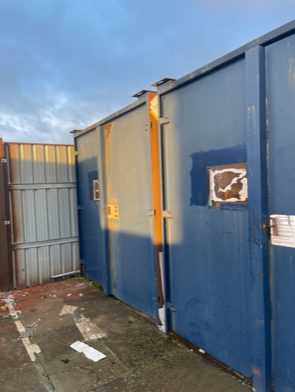
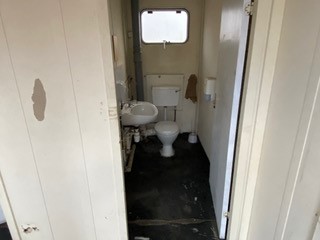
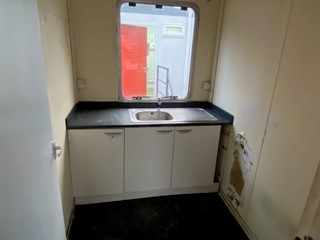
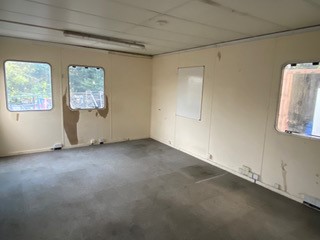
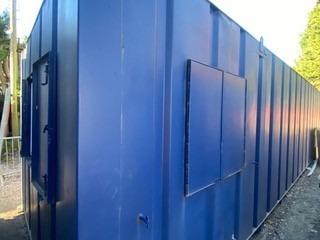
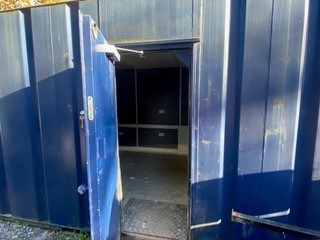
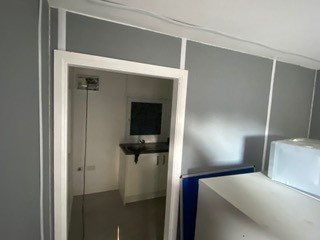
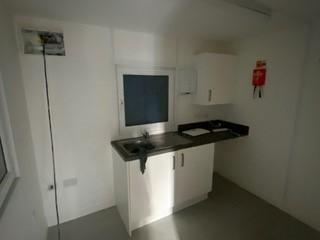
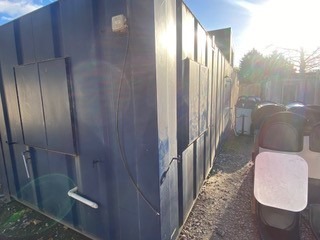
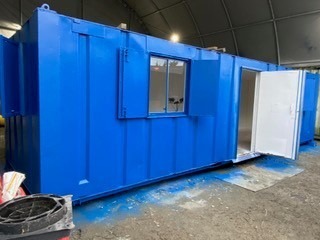
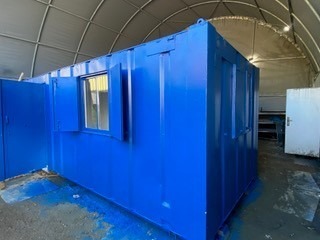
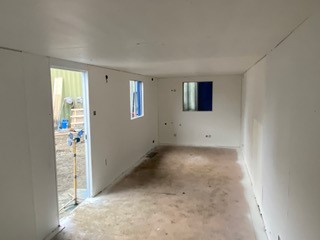
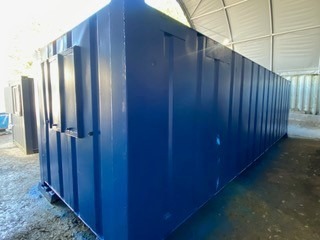
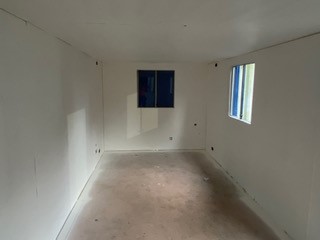
32ft x 10ft Anti Vandal Canteen in Blue

  • Used with electric sockets, lighting and heating
  • UPVC Double Glazed Windows
  • Furniture
  • Kitchenette 

Location: Nationwide


£4,995

EX VAT

Not Available for Hire

Call for an instant quote!

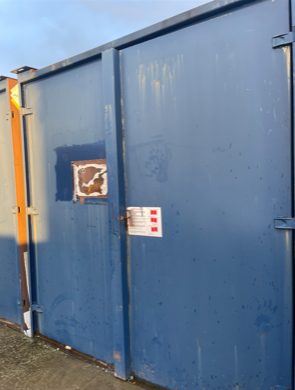
20ft Used Shipping Containers

  • Wind and Water Tight
  • Doors in good working Order
  • Random Selection
  • Lock Box and Lock additional cost.

Location: Nationwide


£1,500

EX VAT

Not Available for Hire

Call for an instant quote!

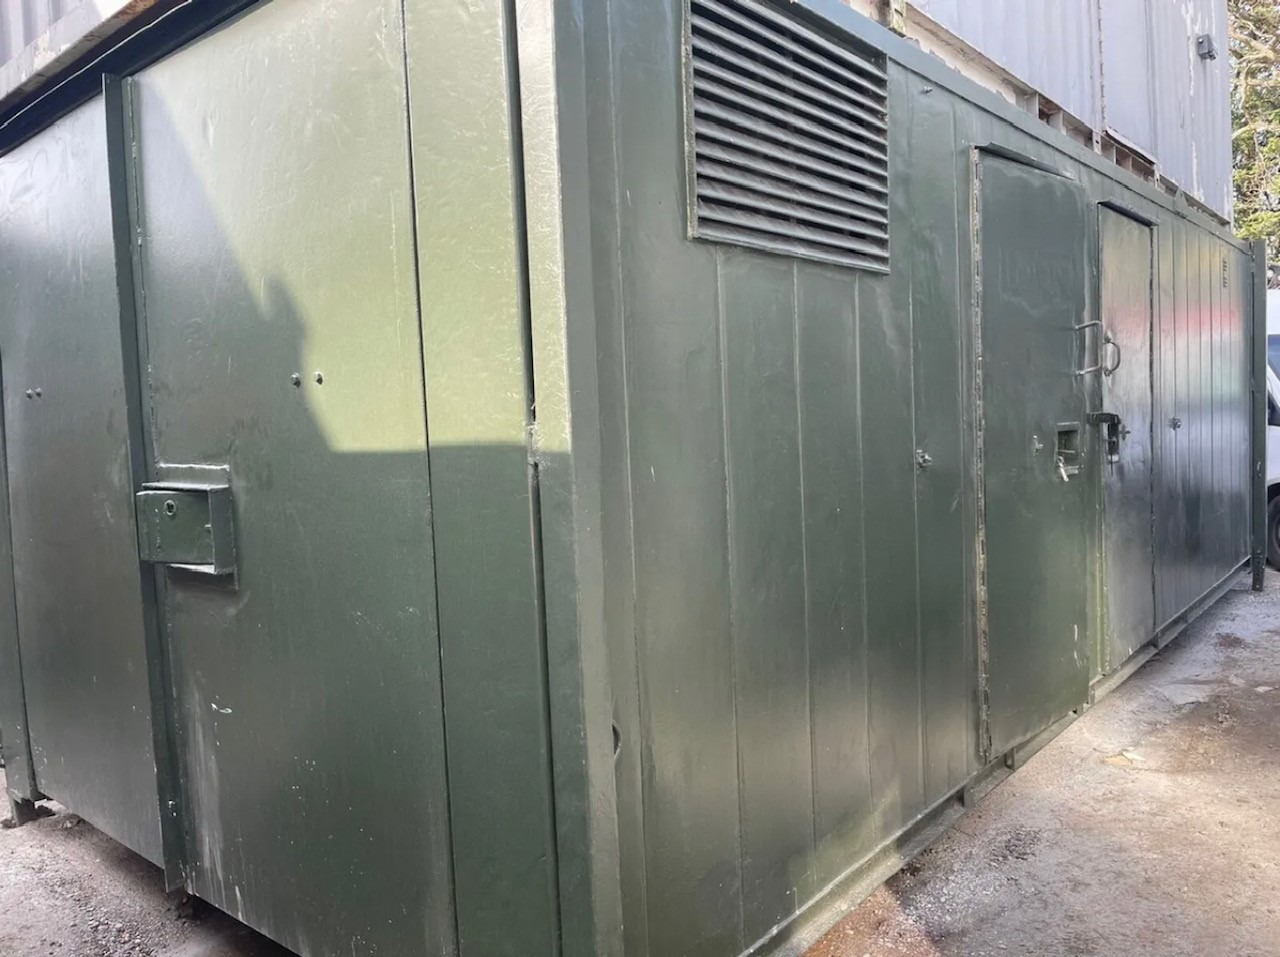
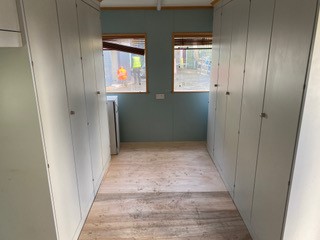
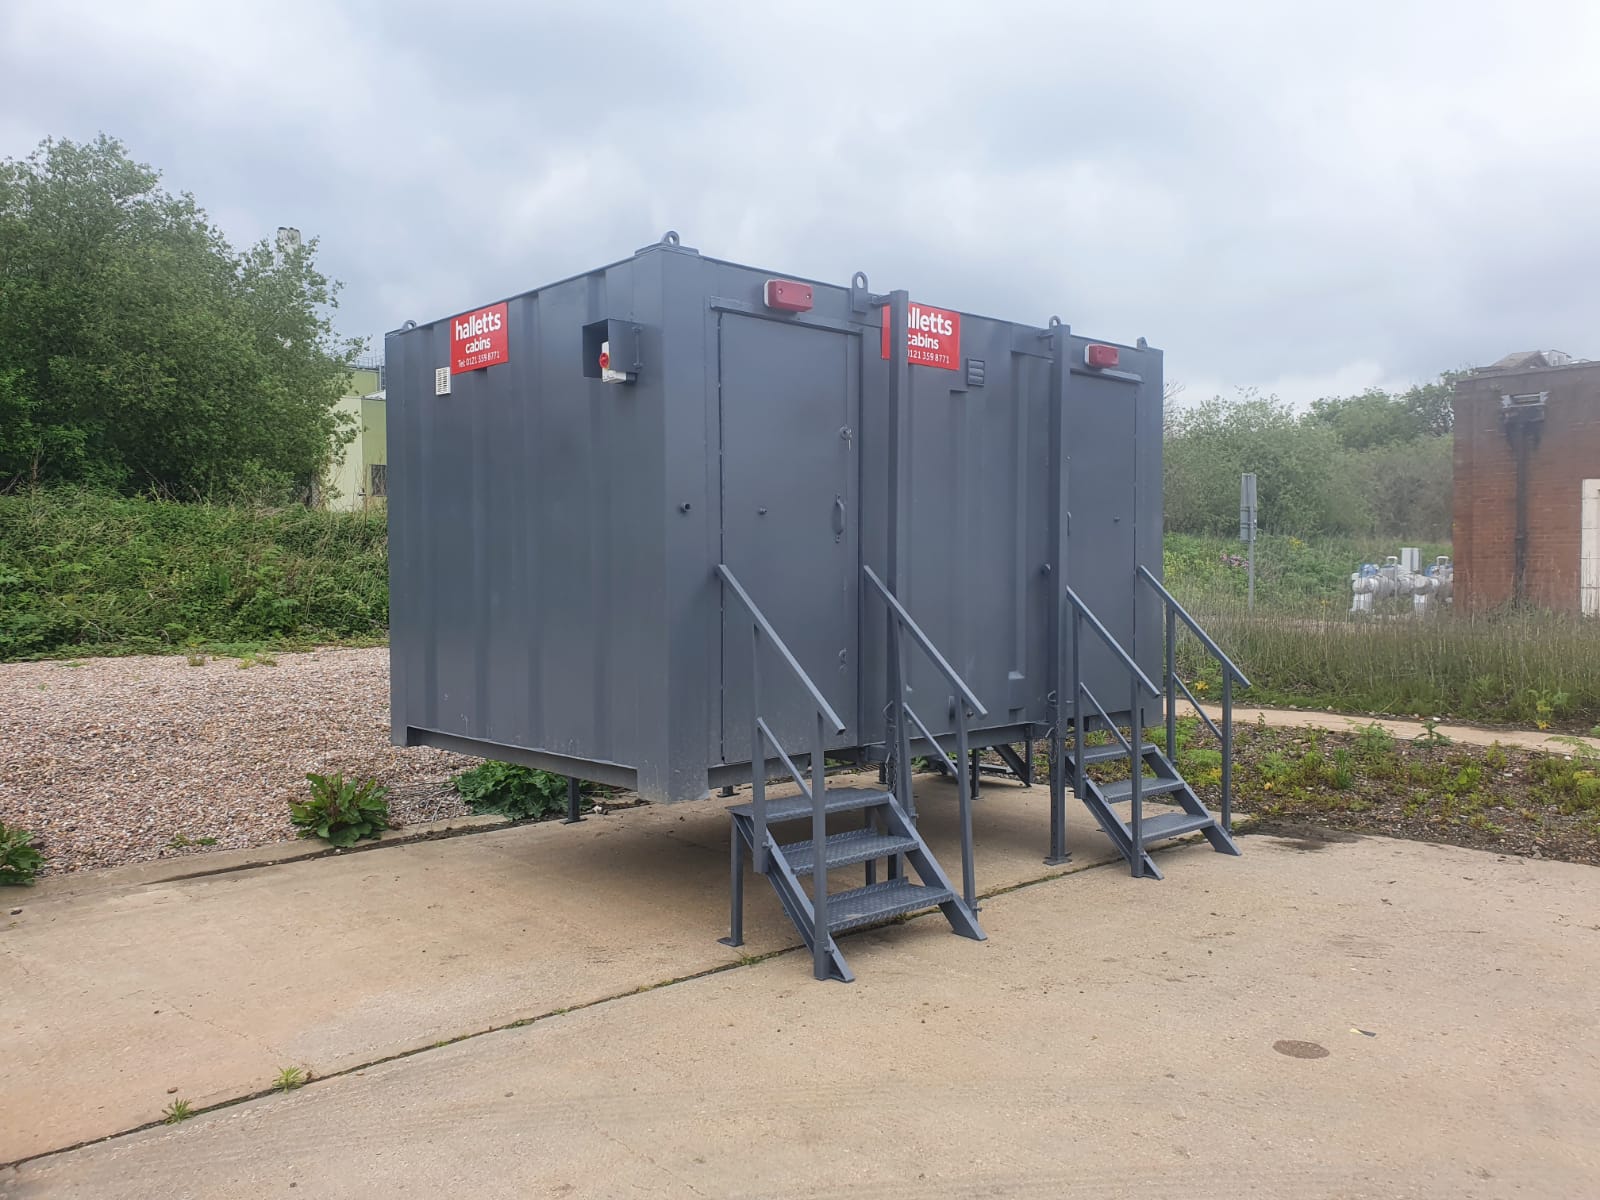
24ft x 10ft Jack Leg Anti Vandal Canteen/Toilet/Storage

  • Split entrance for Canteen room and WC which includes single cubical, urinal and sink.
  • Container door end with storage.
  • Electric Sockets, Lighting and Heating
  • Fitted Floor to Ceiling Cupboards
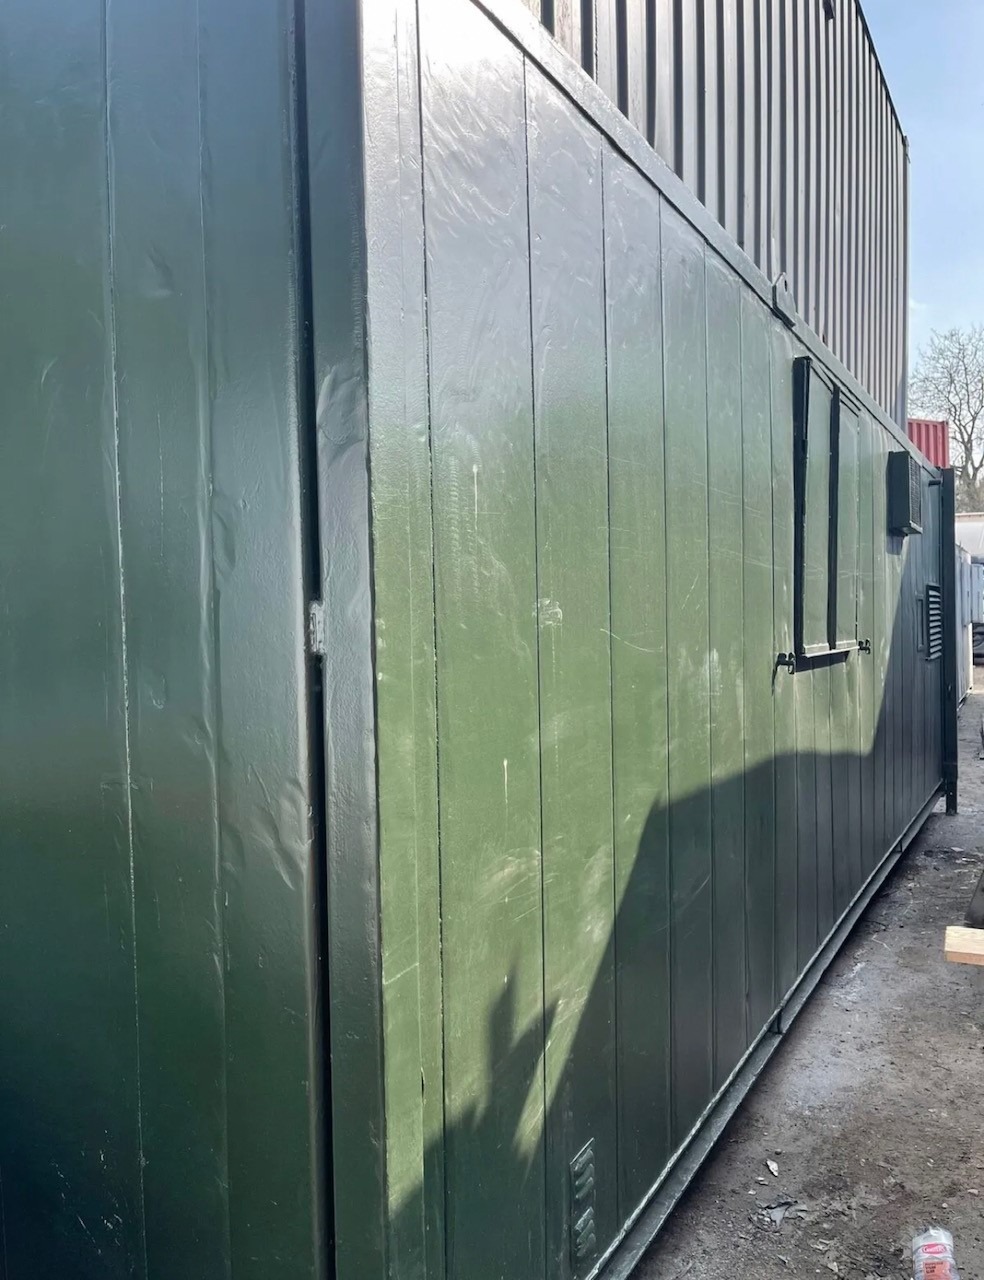
  • Colour: Dark Green

Location: Nationwide


£5,000

EX VAT

Not Available for Hire

Call for an instant quote!

40ft x 12ft Jack Leg Genuine Portakabin Pullman

  • 2 x Offices, Canteen and WC
  • Electric Sockets, Lighting and Heating
  • Colour: Light Grey
  • Full or Part Refurbishment option is available please ask.

Location: Nationwide


£9,500

EX VAT

Not Available for Hire

Call for an instant quote!

32ft x 10ft Anti Vandal Split Canteen/Office

  • Canteen approx 10ft – Office approx 22ft
  • Electric Sockets, Lighting and Heating
  • UPVC Double Glazing
  • Colour: Dark Blue

Location: Nationwide


£5,500

EX VAT

Not Available for Hire

Call for an instant quote!

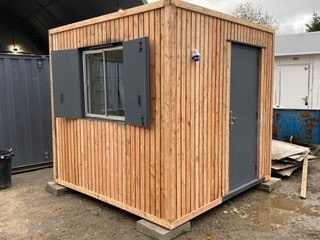
8ft x 8ft Anti Vandal Gate House/Office

  • Open Plan
  • Electric Sockets, Lighting and Heating
  • Colour: Clad in New Larch Timber

Location: Nationwide


£5,500

EX VAT

Not Available for Hire

Call for an instant quote!

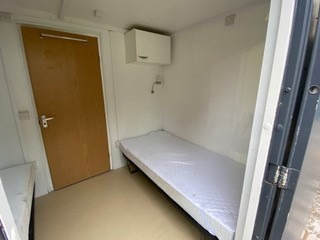
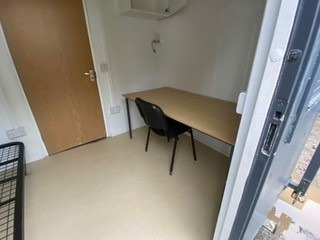
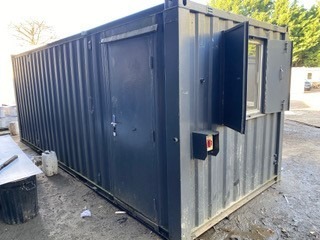
20ft x 10ft Anti Vandal Sleeper Unit

  • Split sides with two entrances, each side has its own room and Shower Toilet Facility
  • Electric Sockets, Lighting and Heating
  • Colour: Dark Grey

Location: Nationwide


£6,500

EX VAT

Not Available for Hire

Call for an instant quote!

21ft x 8ft Anti Vandal Canteen

  • Open Plan
  • Electric Sockets, Lighting and Heating, Hot water Unit + kitchen with cupboards and work top.
  • Colour: Dark Grey 

Location: Nationwide


£4,200

EX VAT

Not Available for Hire

Call for an instant quote!

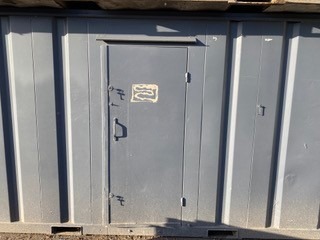
30ft x 9ft Anti Vandal Fire Rated Office

  • Open Plan Refurbished
  • Electric Sockets, Lighting and Heating
  • Colour: Dark Blue

Location: Nationwide


£6,500

EX VAT

Not Available for Hire

Call for an instant quote!

24ft x 9ft Anti Vandal Office

  • Open Plan
  • Electric Sockets, Lighting and Heating
  • Colour: Dark Grey

Location: Nationwide


£4,200

EX VAT

Not Available for Hire

Call for an instant quote!

22ft x 9ft Jack Leg Portable Cabin

  • 22ft x 9ft Jack Leg Portable Cabin
  • Open Plan
  • Electric Sockets, Lighting and Heating
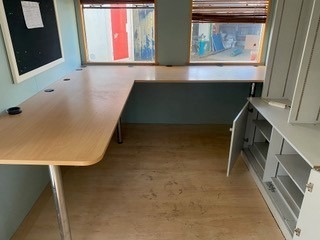
  • Fitted Desk and Floor to Ceiling Cupboards
  • Colour: Light Grey

Location: Nationwide


£4,995

EX VAT

Not Available for Hire

Call for an instant quote!

24ft x 9ft Jack Leg Portable Cabin

  • 24ft x 9ft Jack Leg Portable Cabin
  • Split Offices with two entrances
  • Electric Sockets, Lighting and Heating
  • Fitted Floor to Ceiling Cupboards
  • Colour: Light Grey

Location: Nationwide


£5,500

EX VAT

Not Available for Hire

Call for an instant quote!

10ftx8ft – £5950 + Vat / 16ftx8ft – £7950 + Vat / 20ftx8ft – £9000 + Vat / 24ftx8ft – £12000 + Vat / 30ftx8ft – £13500 + Vat

  • Reinforced doors and windows with secure locking
  • Open plan with electric sockets and lighting
  • Any Extras available: Canteen, Partitions, Toilets.

Location: Nationwide


From £5,950

EX VAT

Not Available for Hire

Call for an instant quote!

  •  Electric Sockets, Lighting and Heating
  •  Wind & watertight
  •  Sprayed Dark Grey

Location: Nationwide


£4,995

EX VAT

Not Available for Hire

Call for an instant quote!

  • 12ft Towable Gound Hog
  • Includes: toilet, canteen and seating area
  • Full working generator, fully serviced and in great condition


Location: Nationwide


£6,500

EX VAT

Not Available for Hire

Call for an instant quote!

  • Reinforced doors with secure locking 
  • Electrics and lights included
  • Sink and water boiler included

Location: Nationwide

Quantity: ∞

£15,000

EX VAT

Not Available for Hire

Call for an instant quote!

• Reinforced doors and windows with secure locking
• Open plan with electric sockets and lighting
• Ral Code Colour of choice

• Any Extras available : Canteen, Partitions, Toilets.

Location: Nationwide


£11,995

EX VAT

Not Available for Hire

Call for an instant quote!

• Reinforced doors and windows with secure locking

• Open plan with electric sockets and lighting

• Ral Code Colour of choice

• Any Extras available : Canteen, Partitions, Toilets.

Location: Nationwide


POA

Not Available for Hire

Call for an instant quote!

test

• Reinforced doors with secure locking
• Sink and water boiler included

Location: Nationwide

Quantity: ∞

£12,495

EX VAT

Not Available for Hire

Call for an instant quote!

32ft x 20ft Cabin

  • Reinforced doors with secure locking 
  • Electrics and lights included
  • Sink and water boiler included
  • Electric Roller Shutters
  • Roof top terrace 
  • Store Room 
  • Slatwall installation 

Location: Nationwide


£39,000

EX VAT

Not Available for Hire

Call for an instant quote!

Looking to Buy or Hire?

Get a Quick Container Quote Now!

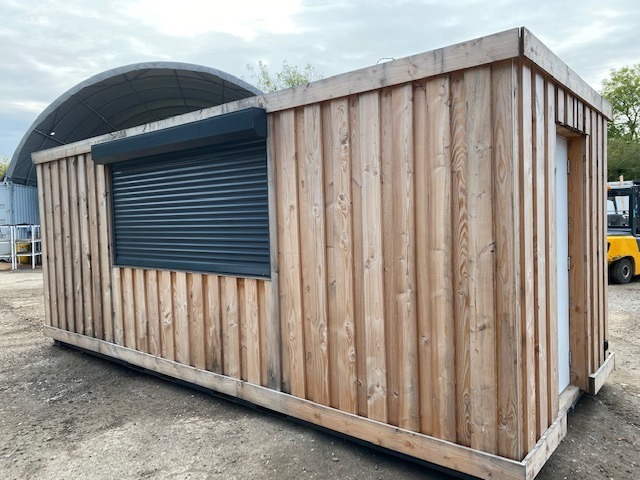
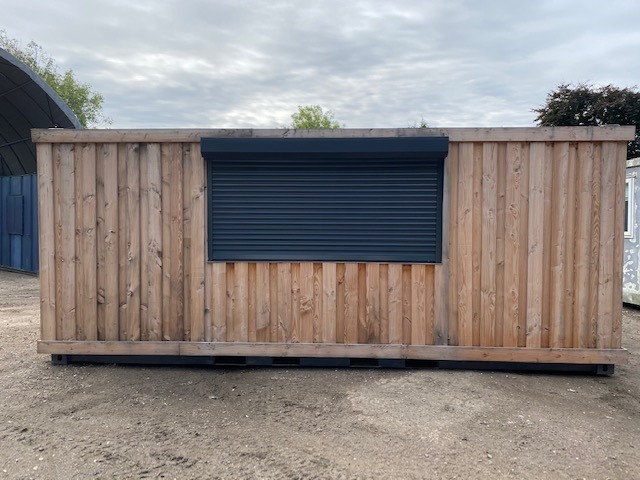
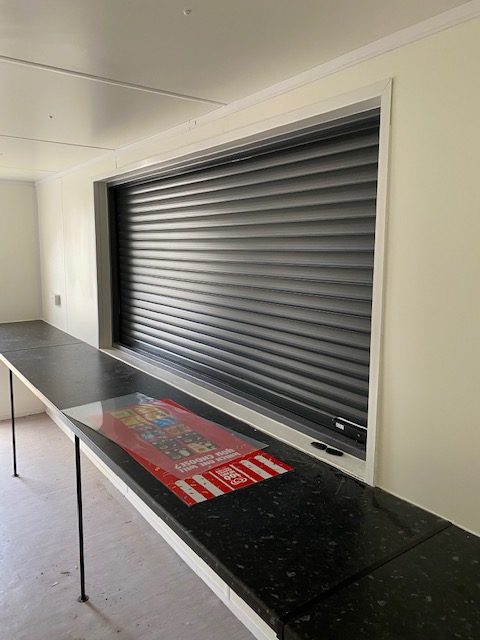
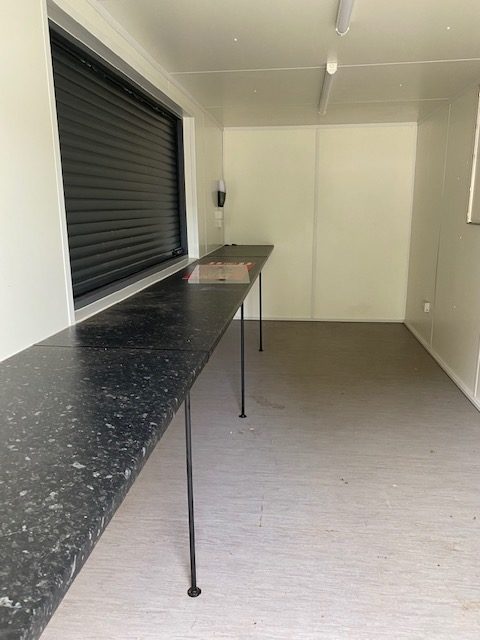
20ft x 8ft Container Kiosk

  • Open plan layout with worktop serving area
  • Electric roller shutter with remote control
  • Electrics and lights included

Location: Nationwide


£15,000

EX VAT

Not Available for Hire

Call for an instant quote!

Looking to Buy?

Get a Quick Container Quote Now!

Newsletter Signup Form

Be the first to discover our exclusive offers and latest company updates by signing up to our email newsletter. Every month we’ll keep you informed of our best prices, industry updates, customer’s container projects, national shows we’ll be exhibiting at, and much more.

Looking to Buy or Hire?

Get a Quick Container Quote Now!